

Quick answer: An ammunition chest is sized inside out: load per shelf and clear interior first, then span, wall thickness, rib pitch, door gap and stacking.
Table of contents
- Start with payload and clear interior
- Wall thickness follows span, not habit
- Door frame, locking and the closing gap
- Coating and stacking limits
- FAQ
1. Start with payload and clear interior
Most ammunition chest drawings begin with overall length, width and height, which is backwards. The envelope is an output; load per shelf, largest outline and tier count are the inputs.
Load must be stated as uniform or concentrated. The same 110 kg spread over a shelf and one 30 kg item on a 200 by 200 mm patch ask for different steel.
Clear interior is the largest outline plus 25 mm of handling clearance, split both sides. Depth loses another 30 mm to the door lip and lock bar. A centre post eats 40 mm of width, which must come off the clear figure.
| Load per shelf | Clear width × depth | Tiers | Shelf span | Wall thickness |
|---|---|---|---|---|
| 60 kg | 900 × 500 mm | 3 | 900 mm | 1.2 mm |
| 110 kg | 1050 × 550 mm | 4 | 1050 mm | 1.5 mm |
| 180 kg | 1200 × 600 mm | 3 | 600 mm with centre post | 2.0 mm |
Tier count is squeezed by the room: tallest item plus 80 mm of clearance; at 2.2 m of store height, four 450 mm tiers fit.
2. Wall thickness follows span, not habit
Thickness on an ammunition chest is calculated. A shelf on two posts acts as a simply supported beam: deflection rises with the fourth power of span and falls with the cube of thickness, so those exponents decide what to change first.
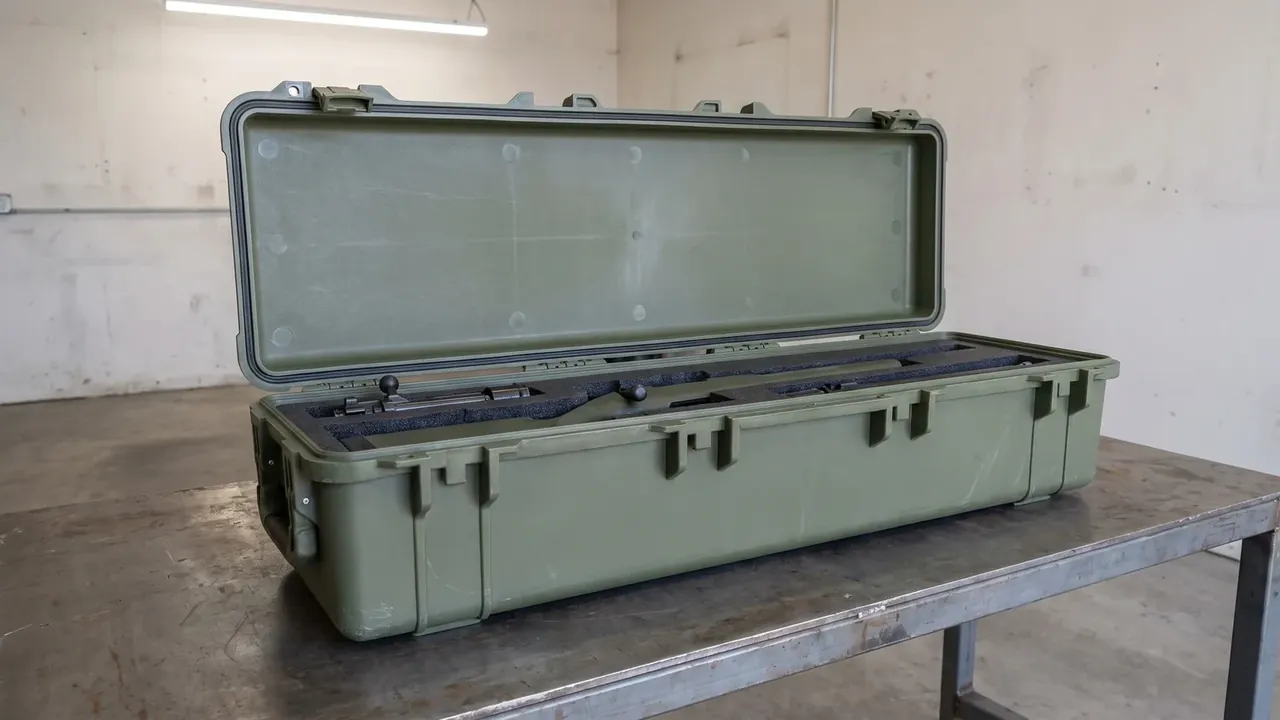
Take span from 900 mm to 1800 mm and deflection grows sixteen times. Going from 1.2 mm to 1.5 mm cuts deflection to 51 percent for 25 percent more weight. A single 12 mm rib gets close to a full thickness step for the price of a few bends. That is why a 1050 mm span runs 1.5 mm steel at 250 mm pitch. Halve the span with a post and deflection drops to one sixteenth. Spend the same money on thicker plate with the span untouched and you get the worst result per kilogram.
The trial runs in four steps, and the order matters:
- Span: clear width minus 25 mm at each post.
- Limit: span divided by 420, so 1050 mm allows 2.5 mm.
- Thickness: 1.2 mm calculates at 3.6 mm under 110 kg, 1.5 mm returns 2.4 mm.
- Stiffening: failing that, tighten pitch from 300 mm to 250 mm.
Only after thickness is fixed does fabrication have a target. A 1.5 mm sheet with a 15 mm flange and one with 8 mm are not in the same stiffness class.
3. Door frame, locking and the closing gap
The door fails first, because it is opened and pulled every day. A 2.0 mm panel, one step above the side walls, buys pry resistance; a 15 mm return flange stiffens the joint so the gap can stay small.
Keep the gap between 1.0 and 1.5 mm and judge it with feeler gauges. Below 1.0 mm the door binds once the body takes up moisture; above 1.5 mm the bolt does not enter deep enough.
| Feature | Target | How it is judged | What goes wrong |
|---|---|---|---|
| Closing gap | 1.0–1.5 mm | feeler gauge, three points per side | past 1.5 mm the bolt barely engages |
| Lock bars | 16 mm diameter, 20 mm travel | caliper and travel scale | three-point locking drops to one |
| Frame flange | 15 mm | caliper sample | a bar finds purchase and spreads the gap |
Lock bars run 16 mm in diameter with 20 mm of travel, set top, middle and bottom. Three hinges carry an 80,000 cycle test, after which no corner may drop more than 1 mm.
4. Coating and stacking limits
Coating is the one stage that cannot be corrected after assembly, so pretreatment and film build must be right on the line.
Phosphating runs at 2.5 g per square metre, powder build at 90 to 110 microns, edges at 130. Salt spray is accepted at 480 hours without red rust, twice the usual 240, for 12 extra minutes per unit.
Stacking data belongs on the drawing with weight and time: four tiers, 225 kg each, 900 kg total, held 24 hours, then diagonal distortion against a 2 mm limit. The base stands 100 mm off the floor on M12 feet.
A body that fails the distortion check will not close its door squarely. Run the stack test before coating, then repeat it after.
Conclusion
Sizing an ammunition chest is a chain, not a table: payload sets span, span sets thickness and rib pitch, thickness sets the door and lock fits, coating and stacking come last. Skip a link and the rest is copied rather than derived. Every dimension on an ammunition chest should trace to its origin.
This article discusses only the container (case body) side of specifications and design intent, and does not cover any handling, loading or use of the contents.
Related Reading
- Choosing a chest by capacity, dividers and locking
- Where a chest stops and alternatives begin
- Sizing a transfer case for ammunition
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models