

Quick answer: Over 500,000 shots case mould steel splits by 338,000 CNY, or 0.68 CNY a part: P20 needs two tools at 906,000 CNY, 718 one tool at 568,000 CNY. Break-even sits at the 320,000-shot step.
Table of contents
- Two Ledgers for Case Mould Steel
- Hardness and Polishability
- Texture Uniformity and Weld Repairs
- Cost per Shot at Two Volumes
- Which Grade Fits Which Volume
- FAQ
1. Two Ledgers for Case Mould Steel
A 600 mm × 420 mm × 130 mm case tool costs 420,000 CNY in P20 and 560,000 CNY in 718. Over 500,000 shots the P20 route needs a second tool after 320,000, so two tools plus polishing plus two changeovers total 906,000 CNY; the 718 route runs one tool to 650,000 and totals 568,000 CNY.
The 338,000 CNY gap is 0.68 CNY a part; only 140,000 CNY is block price, the rest accumulates shot by shot.
Block cost is paid once; polishing hours and downtime grow with volume, so short orders never amortise the one-off.
| Item | P20 | 718 |
|---|---|---|
| Pre-hardened hardness (HRC) | 30–32 | 34–38 |
| Polishable finish (μm Ra) | 0.10 | 0.05 |
| Texture deviation (mm) | 0.012 | 0.006 |
| Weld repairs at one spot | 3 | 5 |
| Block price (10,000 CNY) | 42 | 56 |
| Usable shots (10,000) | 32 | 65 |
| 500,000-shot total (10,000 CNY) | 90.6 | 56.8 |
2. Hardness and Polishability
P20 arrives at 30 to 32 HRC and 718 at 34 to 38 HRC, four Rockwell points apart. 718 holds sulphur below 0.005% with little banding, so a cavity reaches Ra 0.05 μm in 31 hours; P20 at 0.008% needs 38 hours and still leaves three 0.2 mm pits opposite the gate.
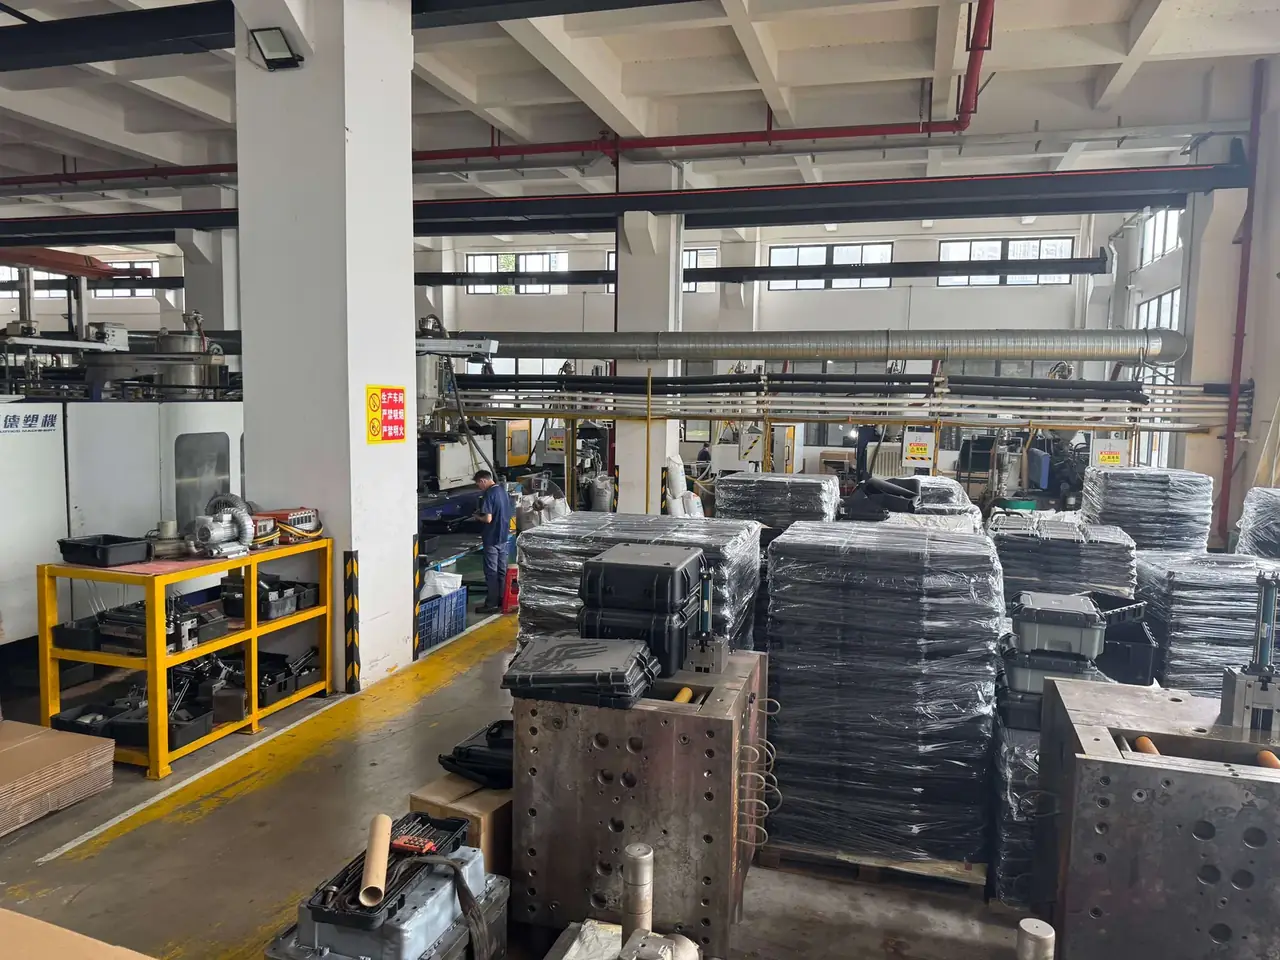
Inclusions, not the wheel, cause those pits; etching opens them into 0.01 mm patches.
Harder is not automatically better: 718 at 34 HRC holds an R2 corner, a 48 HRC grade chips there.
Polishing is budgeted per tool: six forming inserts take 156 hours in P20 against 186 in 718, 3,600 CNY more at 120 CNY an hour. Across 320,000 shots P20 needs four rounds and 718 two, swinging 4,700 CNY back.
Read the mirror at 60 degrees: past round three P20 hazes 0.03 mm, 718 at round five.
3. Texture Uniformity and Weld Repairs
One etch across a 300 mm × 200 mm face varies 0.006 mm in 718 and 0.012 mm in P20; 6 μm shows as a dark band along the flank.
A P20 repair drops the heat-affected zone to 26 HRC across 8 mm and will not re-etch cleanly; 718 after three repairs still holds 31 HRC across 5 mm.
Write the rule into the drawing: three repairs per spot, 0.4 mm build-up per pass, temper at 480 ℃ for 2 hours; a fourth pass joins the zones into one soft patch at 28 HRC.
P20 takes TIG at 1.2 kJ/mm, 718 takes laser at 0.3 kJ/mm, narrowing the zone from 8 mm to 5 mm.
4. Cost per Shot at Two Volumes
Up to 300,000 shots one P20 tool suffices: 420,000 CNY of block plus 14,000 of polishing, or 1.45 CNY a shot. 718 also runs one: 560,000 plus 5,000, or 1.88 CNY.
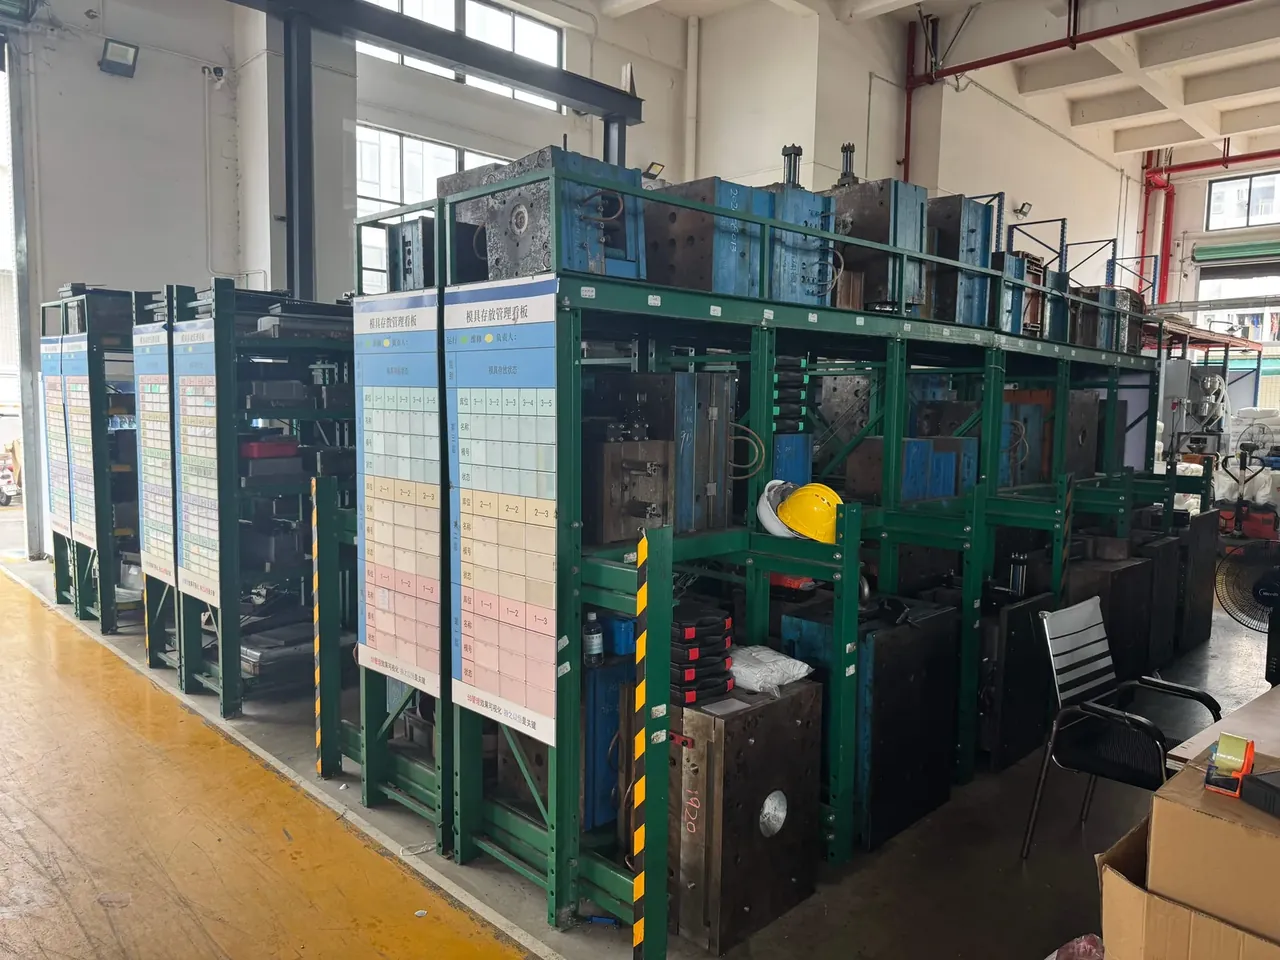
At a million shots P20 needs four tools: 1.68 million of blocks, 51,000 of polishing, three changeovers at 129,600 CNY, total 1.861 million or 1.86 CNY a shot. 718 needs two: 1.12 million, 16,000 of polishing, one changeover at 43,200 CNY, total 1.179 million or 1.18 CNY.
| Shots | Grade | Tools | Blocks | Polish | Downtime | Total | Per shot |
|---|---|---|---|---|---|---|---|
| 300,000 | P20 | 1 | 42.0 | 1.4 | 0 | 43.4 | 1.45 |
| 300,000 | 718 | 1 | 56.0 | 0.5 | 0 | 56.5 | 1.88 |
| 1,000,000 | P20 | 4 | 168.0 | 5.1 | 12.96 | 186.1 | 1.86 |
| 1,000,000 | 718 | 2 | 112.0 | 1.6 | 4.32 | 117.9 | 1.18 |
Columns 4 to 7 are in 10,000 CNY; downtime runs 2,400 CNY an hour over the 18 hours a changeover takes, teardown and 30 trial shots included.
The crossover sits at 320,000 shots: at 319,000 P20 has spent 435,000 CNY against 565,000, still 130,000 ahead; one step later it adds 420,000 and falls 290,000 behind.
5. Which Grade Fits Which Volume
Below 300,000 shots P20 pays 140,000 CNY less up front and 0.43 CNY less a part.
From 320,000 to 650,000 shots 718 takes over: P20 needs a second tool, handing back the 130,000 CNY it saved plus 18 hours of downtime.
Above 650,000 both need a second tool: 718's reaches 1.3 million shots, P20's fourth arrives at 1.28 million, and at a million shots the gap is 680,000 CNY.
A hybrid exists: P20 body with 718 inserts opposite the gate and at the corners, 480,000 CNY of block, life still 320,000 shots, and it pays only above 40% visible-surface content.
Purchase clause: under 300,000 shots order P20 at 30 HRC; from 300,000 to 650,000 order 718 at 34 HRC minimum with sulphur at 0.005% maximum; above that, 718 plus two spare insert sets.
Conclusion
Case mould steel selection reduces to a step function. The P20 curve jumps 420,000 CNY at 320,000 shots, the 718 curve 560,000 CNY at 650,000, and whichever jump arrives first decides the order. At 500,000 shots 718 saves 338,000 CNY; at 200,000 P20 saves 140,000. Three inputs settle it: total shots, visible-surface share, and whether an 18-hour changeover fits the schedule. Play those numbers and the 140,000 CNY on the quotation stops looking like pure cost.
This article discusses container-side specifications and design implications only, and does not cover any handling, loading or use of the contents.
Related Reading
- What drives protective case tooling cost
- P20 versus 718H mould steel selection
- How mould material affects case accuracy
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models