

Quick answer: Three molding variables set the price of an injection molded plastic tool box before resin grade matters: cavity count, cycle seconds and clamp force. Under 8,000 units a year a single cavity wins; four pay back near 50,000. A 0.8 mm wall step costs an assembly line three minutes an hour.
Table of contents
- Cavities and Tonnage Fix the Unit Cost
- Where the Cycle Seconds Go
- Uneven Walls Stop the Assembly Line
- Sink Marks and Flash at Assembly
- Matching Case Footprint to Machine Tonnage
- Three Volume Bands
- FAQ
1. Cavities and Tonnage Fix the Unit Cost
Tooling arrives as one number but behaves like a curve: a four-cavity mold for an injection molded plastic tool box body runs RMB 260,000 against RMB 86,000 for a single cavity, and only volume closes that gap.
| Annual volume | Cavities | Tooling | Tooling per unit |
|---|---|---|---|
| 3,000 | 1 | RMB 86,000 | RMB 28.70 |
| 12,000 | 2 | RMB 145,000 | RMB 12.10 |
| 50,000 | 4 | RMB 268,000 | RMB 5.40 |
Tooling is the down payment; clamp force decides whether the mold runs. Too little and the halves breathe apart, flash spills from the parting line and trimming must be staffed; too much and machine time climbs from RMB 0.6 to 0.9.
Neither end is cheap.
2. Where the Cycle Seconds Go
The cycle splits into four stages. The part must also walk onto the assembly line: if residual stress bows the lid past 1 mm, the seconds saved return at trial fit.
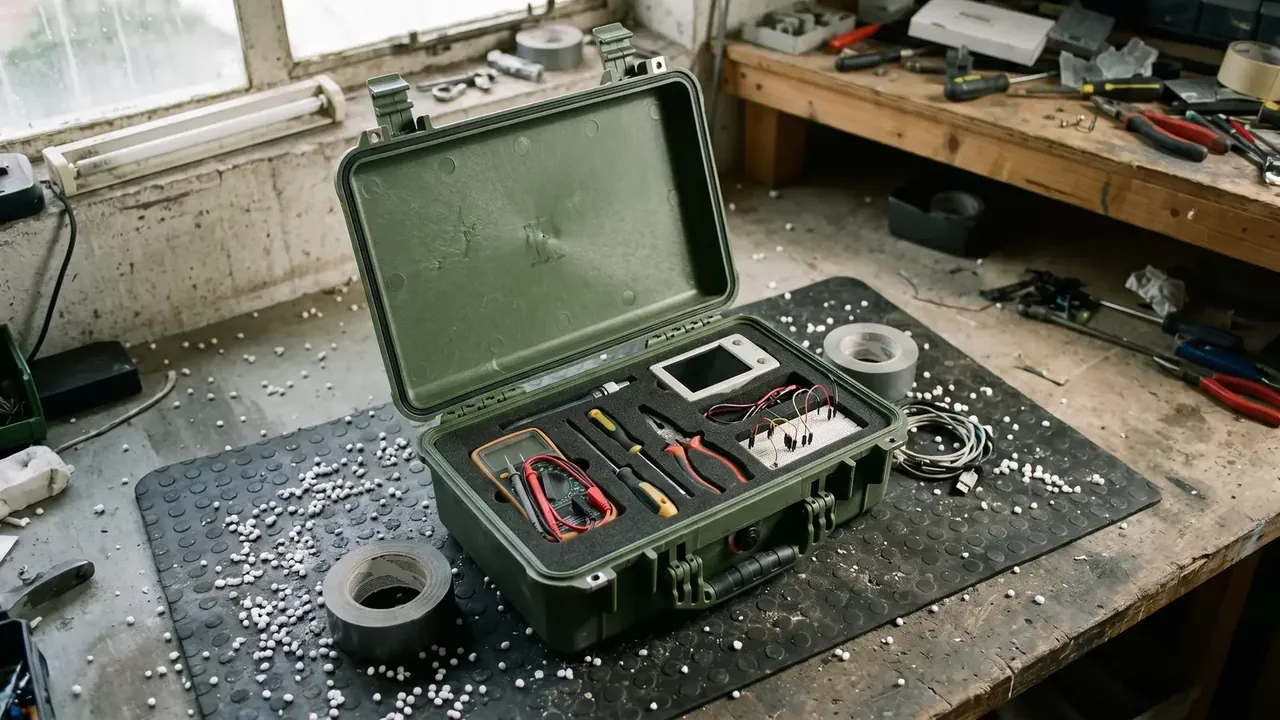
- Injection, 4 s: no slack; steal 0.5 s and a weld line shows.
- Packing, 9 s: 60 to 35 MPa saves 2 s, dimpling the bosses.
- Cooling, 22 s: the only stage with real room, the most wall-sensitive.
- Open and close, 7 s: robots help, big cases give least.
Cooling scales with the square of wall thickness: 22 seconds at 2.4 mm, 34 at 3.0 mm, so the cycle climbs from 42 to 54 seconds. Four cavities make machine time 10.5 seconds a unit, RMB 0.18 at RMB 1.0 a minute, 0.23 on the longer cycle. Twelve seconds of cycle is five cents a unit.
3. Uneven Walls Stop the Assembly Line
Wall variation in an injection molded plastic tool box is a design decision. A 2.4 mm lid against a 3.2 mm side wall cools 30 percent apart and lifts its corners 1.3 mm.
| Lid wall | Side wall | Cooling time | Corner warp |
|---|---|---|---|
| 2.4 mm | 2.4 mm | 22 s | 0.4 mm |
| 3.0 mm | 2.4 mm | 26 s | 1.3 mm |
| 3.4 mm | 2.4 mm | 30 s | 2.1 mm |
The bill comes at assembly: an edge 1 mm proud must be pressed by palm before a latch catches, adding six seconds a unit.
Flatness is accepted at 0.8 mm over 300 mm. Beyond that only cooling changes: split the lid circuit from series to parallel, and drop mold temperature to 45 degrees.
4. Sink Marks and Flash at Assembly
Sink marks hide at rib roots and bosses: invisible below 0.15 mm, a shadow past 0.3 mm.
Flash is judged at the parting line. Under 0.2 mm it can stay; at 0.4 mm it sits on the gasket land and the seam becomes a water path. Trimming an injection molded plastic tool box runs 12 seconds a unit.
5. Matching Case Footprint to Machine Tonnage
Clamp force on an injection molded plastic tool box is projected area times cavity pressure, at 300 kg per square centimeter. A 600 by 400 mm case projects 2,400 square centimeters, which gives 720 tonnes and an 800-tonne machine.
| Case outline | Projected area | Calculated clamp | Suggested machine |
|---|---|---|---|
| 300 x 200 mm | 600 cm2 | 180 t | 250 t |
| 450 x 350 mm | 1,575 cm2 | 473 t | 530 t |
| 600 x 400 mm | 2,400 cm2 | 720 t | 800 t |
Deep cases must also clear shot size: a 600 by 400 body weighs 1.6 kg in polypropylene, and a 22:1 barrel plasticizes 2.8 kg a shot. A 1,300-tonne press backfires, since melt sits three minutes before injection.
6. Three Volume Bands
Bands follow whether an order runs twelve months unbroken.
- Under 3,000 a year: single cavity, P20 steel, no hot runner, manual demolding, tooling under RMB 90,000.
- 10,000 to 20,000: two cavities, hot runner, robot demolding, 48-second cycle, tooling near RMB 150,000.
- Above 50,000: four cavities, beryllium copper rib inserts, zone-controlled mold temperature, unit cost near RMB 4.
A two-month gap erases the case for the four-cavity tool.
Conclusion
Tooling, machine time and trimming on one sheet show the cost structure of an injection molded plastic tool box: resin is about thirty percent, and cavities, cycle, tonnage and yield split the rest. Volume decides: single cavity below 8,000 units, four above 30,000. What gets priced is the injection molded plastic tool box itself.
This article discusses only the container (case body) side of specifications and design intent, and does not cover any handling, loading or use of the contents.
Related Reading
- How wall thickness and ribs are set on a molded case
- Molded protective cases in storage and transport
- Which dimensions to check first when choosing a molded case
- Factory purchasing and audits for molded plastic boxes
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models