

Quick answer: For large moulded boxes the quote follows press tonnage and cycle time, the minimum is counted in pallets, and lead time splits into tooling, trial and production. A 600×400×320 mm box of 2.75 kg runs one cavity on a 1,000-tonne press at 95 seconds, lands near 52 CNY a piece, starts at 300 pieces and takes 70 days first time, 25 on a repeat.
Table of contents
- Machine Tonnage and Mould Size in Plastic Box OEM Manufacturing
- Cycle Time and Part Weight Into Daily Capacity
- Batch Consistency and Colour Difference Acceptance
- Pallet-Based MOQ and Pallet Specification
- Quotation Breakdown and Lead Time Milestones
- FAQ
1. Machine Tonnage and Mould Size in Plastic Box OEM Manufacturing
In plastic box OEM manufacturing, fix the press before arguing price. A 600×400×320 mm box presents 2,400 cm²; at 350 kg/cm² it needs 840 tonnes of clamp, so a 1,000-tonne machine keeps a 16 percent margin while an 800-tonne press flashes within 200 shots.
Mould size follows the tie-bar gap: an 850×650 mm base in a 900×900 mm opening leaves 25 mm of land, and 620 mm of thickness must sit inside the 400 to 900 mm window. Part weight sets the shot, 2.75 kg plus a 0.35 kg runner needing a 4.5 kg barrel.
| Matching item | This part | Buyer checks |
|---|---|---|
| Projected area | 2,400 cm² | Largest face only |
| Clamp needed | 840 tonnes | At 350 kg/cm² |
| Mould base | 850×650 mm, 620 mm | Tie-bar gap and window |
2. Cycle Time and Part Weight Into Daily Capacity
The 95 seconds split into 6 seconds of injection, 18 of packing, 55 of cooling and 16 for opening and ejection. Cooling owns over half, so only water and wall thickness shorten it; 2.5 mm walls reach 86 seconds and sag two high.
At 86 percent efficiency, 86,400 over 95 gives 909 shots, or 780 pieces a day and just past 20,000 a month, a contract figure rather than a sales line. Ramp-up runs 30 percent on trial day, 70 by day three, 86 on day seven, with a 4.5-hour change worth 160 pieces.
3. Batch Consistency and Colour Difference Acceptance
The risk in plastic box OEM manufacturing is not one part but the gap between part one and part one thousand. PP shrinks 1.6 to 1.9 percent and drifts another 0.3 percent over 48 hours, so recheck the 721 mm rim diagonal at 24 hours, where 1.2 mm of drift stops the lid sealing.
Thickness of 2.8 mm plus or minus 0.35 mm is checked at four spots: base corners, long-side middles, handle root and latch seat. Colour follows ΔE, 1.5 within a batch and 2.5 between, against three plaques; one part every two hours beats sorting a shipment.
4. Pallet-Based MOQ and Pallet Specification
In plastic box OEM manufacturing the pallet is the ordering unit: 1,200×1,000 mm, four boxes a layer, three layers for twelve pieces, 33 kg of product and an 18 kg pallet at 1,110 mm.
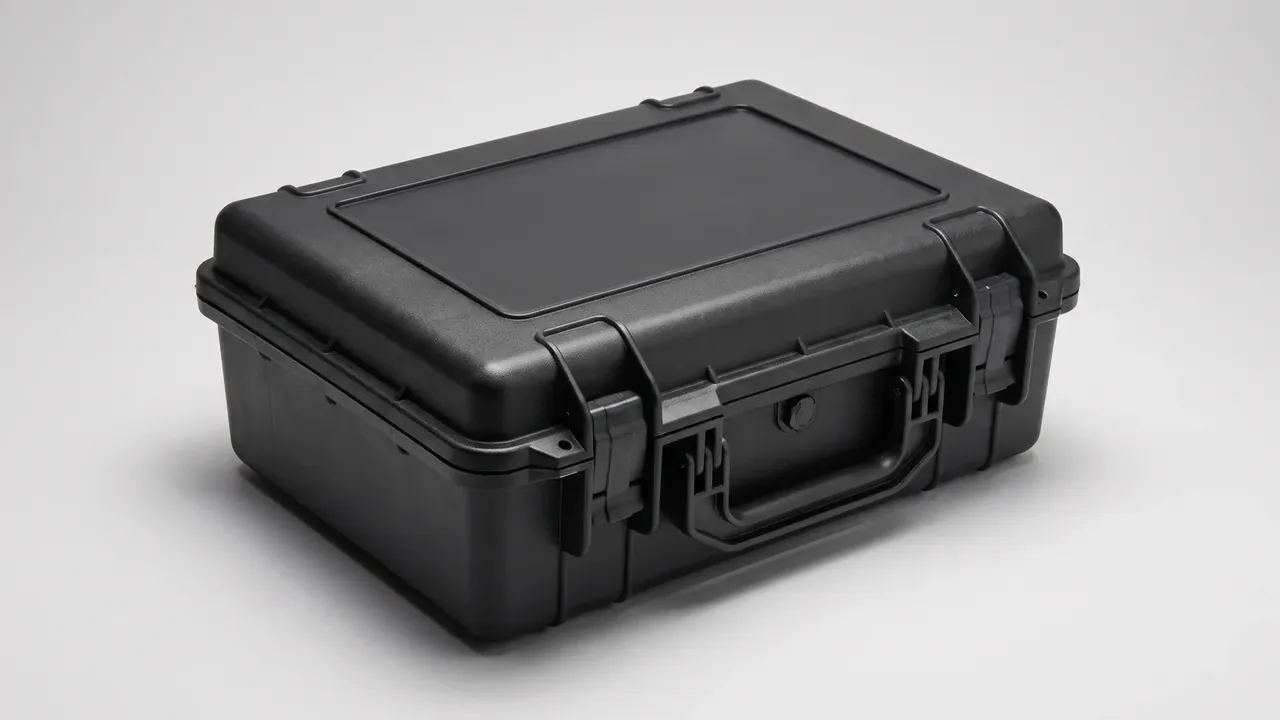
The minimum is 300 pieces, or 25 pallets, because a mould change takes 4.5 hours and start-up scrap runs 30 pieces. A 40-foot high cube holds 20 pallets, 240 pieces and 6.6 tonnes; volume fills its 76 m³ first.
5. Quotation Breakdown and Lead Time Milestones
A plastic box OEM manufacturing quote compares only when split six ways: material, moulding, tooling, secondary work, packing and freight. Material is 2.75 kg at 9,200 CNY a tonne, 25.3 CNY and 48 percent; moulding is 320 CNY an hour times 95 seconds over 3,600, or 8.4; tooling of 260,000 CNY adds 8.7 over 30,000 pieces but 0.87 over a 300,000-shot life.
Secondary work, packing and freight add 4.2, 2.6 and 3.4 for 52.6, so a 45 CNY quote hides tooling or thins the wall. Lead time chains five steps: drawings 3 days, tooling 35, trial 5, sign-off 7, production 20.
| Milestone | Days | Deliverable |
|---|---|---|
| Drawing approval | 3 | 3D file, wall chart |
| Tooling | 35 | Mould, trial notice |
| First trial | 5 | First-off parts |
| Sample sign-off | 7 | Signed sample, plaque |
| Production | 20 | Palletised shipment |
Conclusion
What a buyer negotiates is never the unit price but whether tonnage, cycle and tolerance line up. A press sized by projected area, a pallet-based minimum and a milestone-based lead time make quotes comparable. Put 1,000 tonnes, 95 seconds, 2.8 mm and 300 pieces into the contract annex, and plastic box OEM manufacturing becomes a clause anyone can enforce.
This article discusses only the container (case body) side of specifications and design intent, and does not cover any handling, loading or use of the contents.
Related Reading
- Matching press tonnage to clamp force
- Ramp-up from trial to mass production
- Pallet marking and full-pallet rules
- Colour standards and shade acceptance
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models