

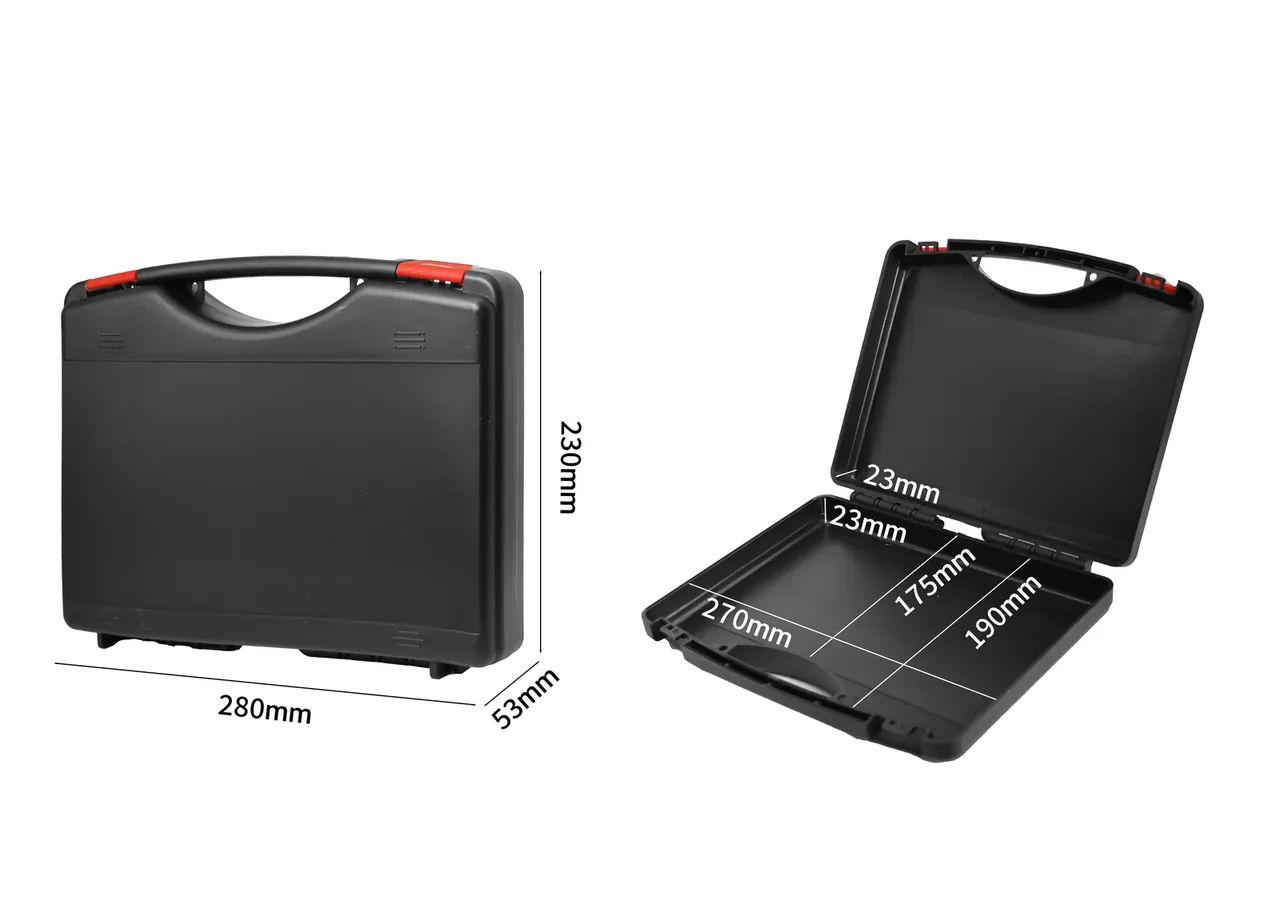
Quick answer: Case tooling for a 60 L body costs 80,000 to 150,000 CNY in aluminium over 45 to 70 days, against 350,000 to 600,000 CNY in steel over 60 to 110 days. The two curves cross near 5,000 units a year, so annual demand below 3,000 units stays on the rotomould side and above 5,000 moves to injection.
Table of contents
- Where Case Tooling Timelines Split
- What the 80,000 and 600,000 CNY Quotes Cover
- Piece Cost for a 60 L Case in Four Lines
- Why Case Tooling Break-Even Lands near 5,000 Units
- Changes, Life and Three Selection Rules
- FAQ
1. Where Case Tooling Timelines Split
The same 60 L case takes 45 to 70 days from drawing to first part in rotomoulded case tooling, and 60 to 110 days in steel. The gap is validation loops, not machining speed: an error in aluminium means recutting the form.
The aluminium route runs in five blocks: parting layout 5 to 8 days, cast blank 6 to 9 days, CNC finishing 12 to 18 days, coating 3 to 5 days, two first-article rounds 8 to 15 days. ZL104 at 10 to 12 mm is cast then milled, so draft and radii come out in one pass.
Injection adds 30 to 40 days in steel: 718H blocks arrive in 25 to 30 days, machining takes 25 to 35 days, hardening 7 to 10 days, and the T1 correction another 10 to 20 days.
| Stage | Aluminium form (days) | Steel mould (days) |
|---|---|---|
| Parting and layout | 5–8 | 8–12 |
| Blank and machining | 18–27 | 35–50 |
| Heat treatment | 3–5 | 7–10 |
| First article and rework | 8–15 | 15–30 |
| Total | 45–70 | 60–110 |
2. What the 80,000 and 600,000 CNY Quotes Cover
For a 60 L body, rotomoulded case tooling quotes at 80,000 to 150,000 CNY and steel at 350,000 to 600,000. Rotomoulding needs one female form; injection needs cavity, core, slides and water.
Aluminium carries most of its quote in the blank: a 900 to 1,300 kg casting at 35,000 to 50,000 CNY, CNC at 20,000 to 30,000, pattern and samples at 8,000 to 12,000, coating 4,000, trials 5,000.
Steel spreads across five packages: frame and stock 120,000 to 180,000 CNY, cavity and core 100,000 to 150,000, slides 40,000 to 60,000, hot runner 30,000 to 50,000.
Complexity moves the two prices differently: aluminium takes no slides, so an interior undercut costs draft angle and manual demoulding rather than money, while every side core in steel adds 30,000 to 60,000 CNY and 8 to 12 days.
Upkeep sits in the same ledger: the form is recoated every 800 to 1,000 shots at 3,000 to 5,000 CNY, steel is lapped every 20,000 shots at 2,000 to 4,000.
3. Piece Cost for a 60 L Case in Four Lines
Split piece cost into material, labour, energy and finishing and the rotomoulded body lands at 160 CNY against 65 CNY. The 95 CNY gap is shot weight and cycle, not labour rate.
Powder runs 6.8 kg at 14 CNY, or 95 CNY; one 290 °C cycle of 25 minutes on a biaxial carousel adds 9 CNY of energy; 35 minutes of labour at 36 CNY an hour adds 21 CNY; trimming and latch fitting add 35 CNY.
Injection uses 4.4 kg of PP copolymer at 10 CNY, or 44 CNY; a 6 minute cycle costs 5 CNY in labour and 3 CNY in energy; assembly adds 6 CNY and administration 7 CNY.
The 2.4 kg gap is structural. A rotomoulded wall needs 4 mm to survive a 5 kg drop from 1 m at -30 °C. Powder build-up runs to ±0.4 mm. Thinner walls chip at the corners. Injection holds 2.8 mm instead. Ribs carry the load there.
Cycle is the fixed cost: a 6 minute shot against a 25 minute oven cycle, so the same volume needs 3 to 5 forms, not one mould.
4. Why Case Tooling Break-Even Lands near 5,000 Units
Divide the 450,000 CNY difference in case tooling spend by the 95 CNY piece gap: 4,737 units. Add the 80,000 CNY of controllers and grippers only injection needs and break-even moves to 5,368 units.
| Annual volume | Rotomould all-in (CNY) | Injection all-in (CNY) |
|---|---|---|
| 500 | 400 | 1,325 |
| 2,000 | 220 | 380 |
| 5,000 | 184 | 191 |
| 20,000 | 166 | 97 |
The table assumes 100,000 CNY of aluminium plus 20,000 of jigs against 550,000 CNY of steel plus 80,000. At 500 units injection carries 1,260 CNY of tooling per part; by 20,000 it is 97 CNY against 166 CNY for aluminium.
Yield pushes the crossover right. At 92% good parts rotomoulding loses half its rejects to wall variation, half to unfused powder; injection holds 97%, with short shots and sink at 1.5% each.
Rhythm matters more than annual total. Five thousand units in four releases run on one form; injection needs 4 to 6 hours of setup and 30 to 60 kg of purge per change.
5. Changes, Life and Three Selection Rules
Moving one rib costs 3 to 5 days and 8,000 CNY in aluminium, against 10 to 20 days and from 30,000 CNY in steel, where the electrode is remade and the water circuit redrilled.
Life separates them by an order of magnitude. Case tooling in ZL104 runs 3,000 to 5,000 shots before the cavity pits, a 718H mould at 32 HRC runs 200,000 to 300,000. At 5,000 units a year the aluminium form is rebuilt inside 12 months.
| Situation | Aluminium form | Steel mould |
|---|---|---|
| Annual demand | Under 3,000 | Over 5,000 |
| Design changes | Still moving in 12 months | Frozen for 2 years |
| Wall | 4 mm and drop-rated | 2.6–3.0 mm and weight-led |
| Finish | Coarse texture, ±0.4 mm | Gloss, ±0.1 mm |
Demand is the hard line, design freeze the soft one, wall and finish the technical ones. Below 3,000 units steel never amortises, above 5,000 shot weight eats the margin.
The small-volume trade is counter-intuitive: because aluminium case tooling is cheap to change, a first form can carry three open features, sell for 6 months, then freeze, while two steel corrections cost more than the whole form.
Conclusion
Case tooling is not a quality contest but two cost curves: one cheap up front and expensive per part, one the reverse. Read demand first, then design freeze, then wall and finish. Below 3,000 units aluminium wins, above 5,000 steel does, and the band between them is arithmetic, not opinion.
This article discusses only the container (case body) side of specifications and design intent, and does not cover any handling, loading or use of the contents.
Related Reading
- What drives protective case mould cost
- Tooling and fixture cost structure for cases
- How to estimate custom case mould cost
- Mould life and rebuild thresholds
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models