

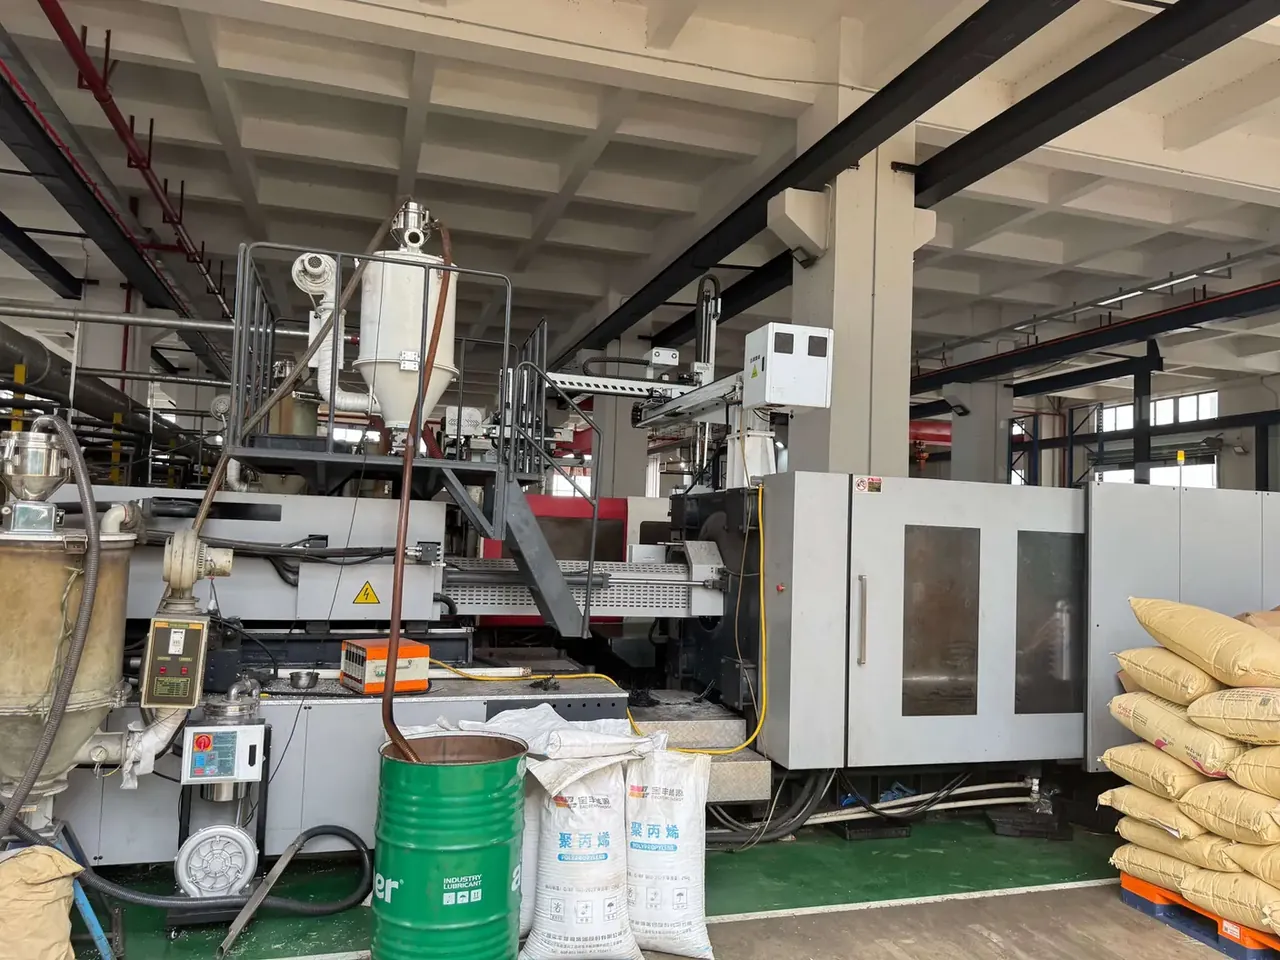
Quick answer: Service a Case Injection Molding Machine by running hours, not by calendar. A ten-minute daily check covers oil level, oil at 45 degrees Celsius and water at 4 bar; central lubrication cycles every 4 hours and tie bars take 8 g of grease per shift; water circuits are cleaned monthly with a 5 degree rise limit; thermocouples are replaced beyond 3 degrees.
Table of contents
- Why Case Injection Molding Machine Service Runs on Hours
- Daily and Weekly: Lube Points and Oils
- Monthly: Water Circuit and Temperature Rise
- Quarterly: Calibration and Spares
- Turning the Four Tiers into a Checklist
- FAQ
1. Why Case Injection Molding Machine Service Runs on Hours
A press running 6,000 hours a year cannot be serviced by date. Two idle weeks leave grease untouched, two 20-hour shifts wear every joint twice as fast, so count hours and map them onto dates.
Failure modes keep different clocks. A dry toggle pin turns blue within two hours, a fouled water circuit lifts the rise from 2 to 6 degrees Celsius in a month, and a probe drifting 5 degrees pushes the body out of tolerance while the display reads normal.
| Tier | Hours | Stop time | Main actions |
|---|---|---|---|
| Daily | 20 per shift | 10 minutes | oil level, oil heat, water pressure, gate |
| Weekly | 120 | 1 hour | filters, leaks, platen bolts |
| Monthly | 500 | 4 hours | water cleaning, oil sample, rise |
| Quarterly | 1,500 | 1 shift | calibration, heater bands, spares |
2. Daily and Weekly: Lube Points and Oils
The daily check is the only one a Case Injection Molding Machine gets every day: oil between the marks, oil at 45 degrees Celsius plus or minus 5, water at 4 bar, safety gate, stop button.
Central lubrication cycles every 4 hours at 40 bar; a blocked distributor pushes pressure to 60 bar with no grease moving, so trust the gauge. Tie bars take 8 g by hand each shift, toggle pins 2 g per point weekly.
Oils do not mix: lithium and calcium-complex greases separate and bearing heat jumps 10 degrees Celsius. Slideways take ISO 68 oil, and weekly work also washes the return filter and re-torques platen bolts to 480 N·m.
| Point | Lubricant | Interval | Amount |
|---|---|---|---|
| Tie bars | lithium NLGI 2 | each shift | 8 g per bar |
| Toggle pins | lithium NLGI 2 | weekly | 2 g per point |
| Slideways | ISO 68 oil | weekly | 20 ml |
| Central pump | lithium NLGI 2 | 4 hours | 3 ml per cycle |
3. Monthly: Water Circuit and Temperature Rise
Each month the Y-strainer is rinsed and scale looped out with 5 percent citric acid for 30 minutes, then neutralised and flushed; core and cavity circuits are cleaned separately.
Rise is the sensitive line: inlet 22 degrees Celsius and return 27 is the ceiling, and beyond it flow is short or a circuit bypasses. Each loop is accepted at 20 litres per minute, and 15 triggers a wash.
Fouled, the oil cooler oil climbs from 45 to 55 degrees Celsius and hydraulic life halves, so clean it quarterly and pressure-test at 6 bar.
| Inlet | Return | Rise | Action |
|---|---|---|---|
| 22 C | 26 C | 4 C | normal |
| 22 C | 28 C | 6 C | low flow, clean strainer |
4. Quarterly: Calibration and Spares
Drift never raises an alarm; it moves dimensions. Each quarter five probes across three barrel zones and the nozzle are compared with a standard thermocouple, and anything beyond 3 degrees Celsius is replaced rather than trimmed in software. Heater bands are checked by resistance and replaced beyond 10 percent.
Controller oil changes every six months; carbonised oil loses 30 percent of heat transfer, so a setpoint of 80 delivers 68 and flow marks appear.
Spares follow consumption: two band sets, five probes, one seal kit and six filters stay on the shelf, counted quarterly.
5. Turning the Four Tiers into a Checklist
A schedule works once it is on paper. Two sheets serve the Case Injection Molding Machine: one triggered by hours, carrying readings and verdicts; one signed per shift, carrying the name and time of whoever acted.
One 800 tonne press ran three months at a 6 degree rise, oil hit 58 degrees Celsius, and the charge lasted four months at an acid value of 2.4. Nobody had washed the strainer.
Judge maintenance by downtime, not forms: 8 hours a month down to 2 saves more output than the hours cost on a Case Injection Molding Machine.
Conclusion
Service on a Case Injection Molding Machine is a table measured in hours: five readings each shift, lube every 4 hours, 8 g of grease per tie bar, a monthly strainer wash holding the rise at 5 degrees Celsius, and quarterly calibration inside 3 degrees. Get the intervals right and unplanned downtime falls from 8 hours a month to 2.
This article discusses only the container (case body) side of specifications and design intent, and does not cover any handling, loading or use of the contents.
Related Reading
- Protective Case Maintenance Guide
- Cleaning and Care for Protective Cases
- Mould Trial Run Guide
- Incoming Batch Inspection for Case Bodies
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models