

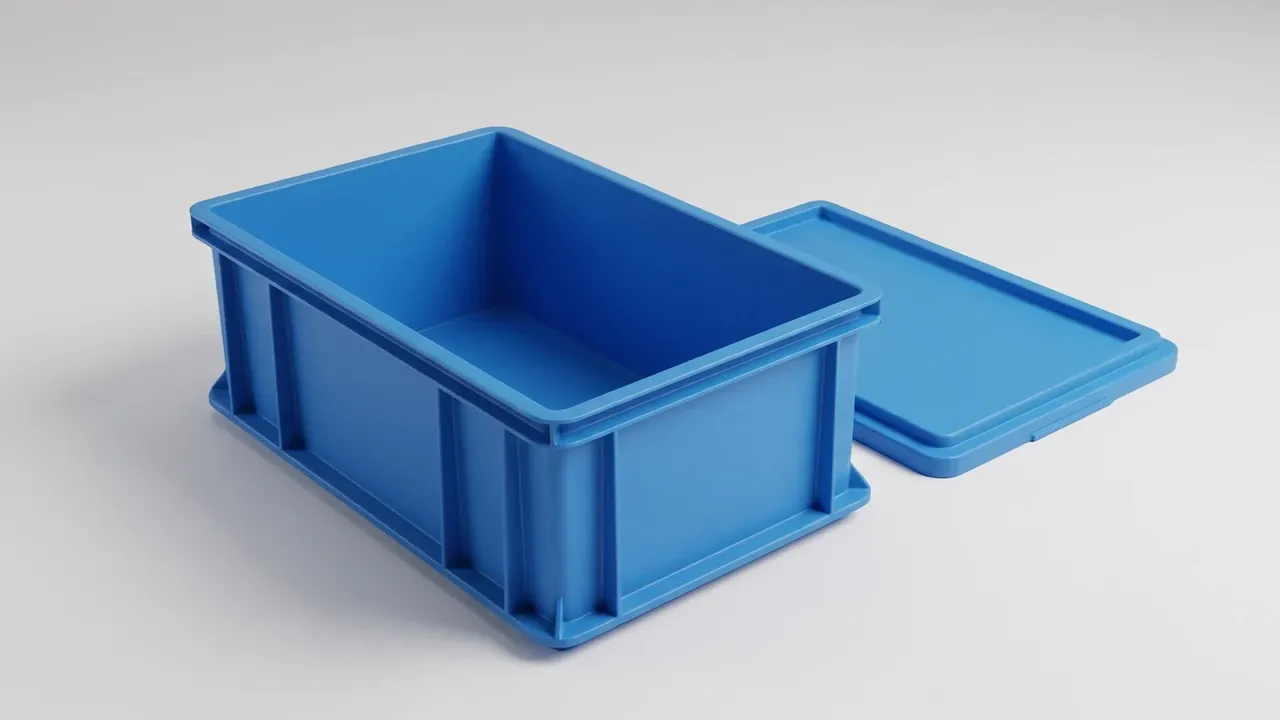
Quick answer: A customized blow molded plastic case is specified in three moves: scale the cavity for 1.8 percent shrinkage, set the wall through parison control points, and write the rating as a stack test with a temperature derating.
Table of contents
- Customized Blow Molded Plastic Case Sizes Come From the Cavity
- Wall Thickness Comes From the Parison
- Load Rating and Stack Test Conditions
- Mold Line and Pinch-Off Trim
- Sample Validation Before the Tool Is Cut
- FAQ
1. Customized Blow Molded Plastic Case Sizes Come From the Cavity
A customized blow molded plastic case is dimensioned from the cavity back: the drawing states cold dimensions, so shrinkage comes off first.
Polypropylene shrinks 1.6 to 2.0 percent in blow molding, 1.8 as a working value, more on thick walls. A 1,000 mm length loses 18 mm, so the cavity is cut at 1,018 mm and 420 mm width becomes 427.6 mm.
| Item | Example | Range | Method |
|---|---|---|---|
| Cavity L W H | 720 x 420 x 380 mm | plus or minus 1.5 mm | tape and gauge |
| Outside L W H | 742 x 442 x 402 mm | plus or minus 2.0 mm | surface plate |
| Wall | 4.0 mm | 3.5 to 4.5 mm | ultrasonic, six points |
Three allowances sit outside the cavity: 0.3 mm trim stock, a 5 mm rim flange, 12 mm feet.
2. Wall Thickness Comes From the Parison
Wall thickness is set by the parison, not by the mold. A 9 mm tube drops from the die, blows at a ratio of 2.5 and lands at 3.6 to 4.0 mm.
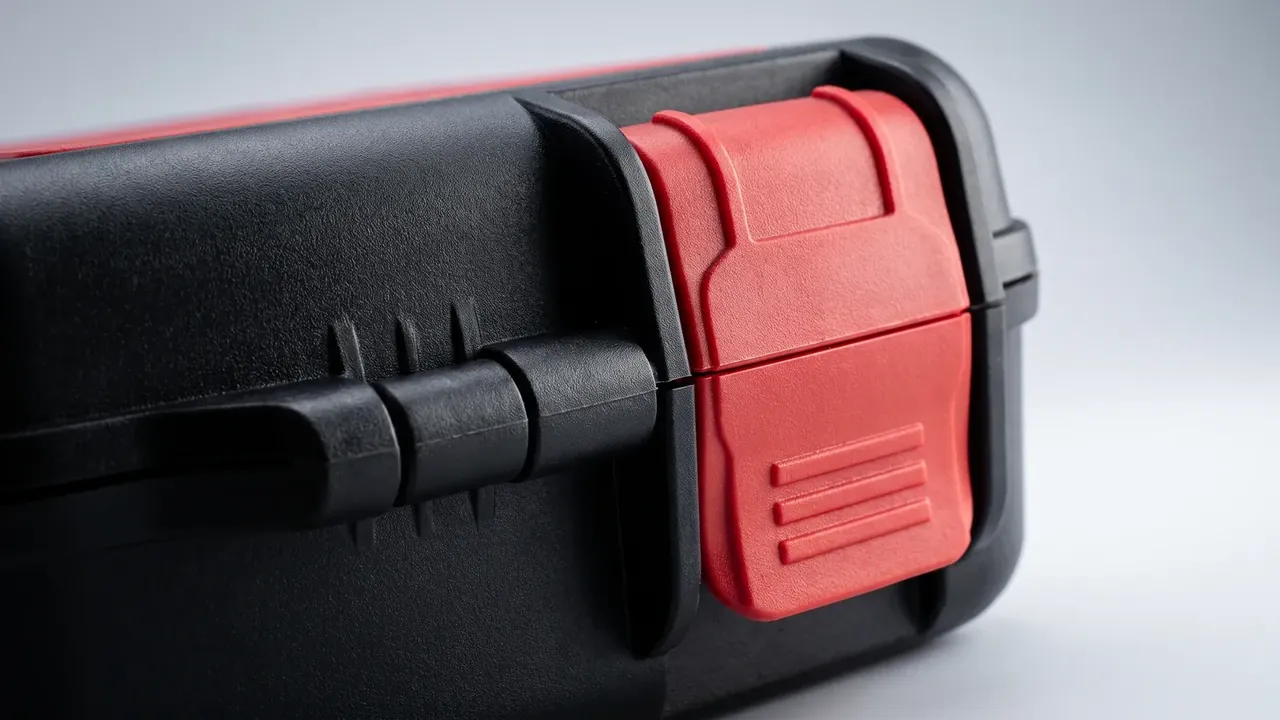
Distribution comes from 25 axial control points and 8 circumferential segments: 7 mm on thin sections, 11 mm on thick ones. Corners stretch hardest, so the parison is pre-thickened 30 percent there, or the corner lands at 2.5 mm.
Air enters at 0.5 MPa with the mold at 25 C; a 4 mm wall cools 90 seconds inside a 270 second cycle. Too little pressure leaves the corner short of the surface; too much thins the pinch-off.
3. Load Rating and Stack Test Conditions
For a customized blow molded plastic case, a rating is a test condition, not a lone number: at 30 kg and five layers the bottom carries 120 kg, so with a 1.25 factor the test load is 150 kg.
Hold it 24 hours at 23 C with base sag under 3 mm and residual set under 1 mm, then drop 0.9 m on six faces at minus 20 C.
Derating is milder than for injection molded parts, but above 50 C take 15 percent off: 128 kg, sag limit 4 mm.
| Case | Condition | Pass line |
|---|---|---|
| Stack, ambient | 150 kg, 23 C, 24 h | sag 3 mm or less |
| Stack, hot | 128 kg, 50 C, 24 h | sag 4 mm or less |
| Drop, cold | 0.9 m, six faces, minus 20 C | no crack, lid shut |
4. Mold Line and Pinch-Off Trim
The mold line is unavoidable, so it is specified rather than hidden: no more than 0.4 mm proud and 0.3 mm mismatch between halves.
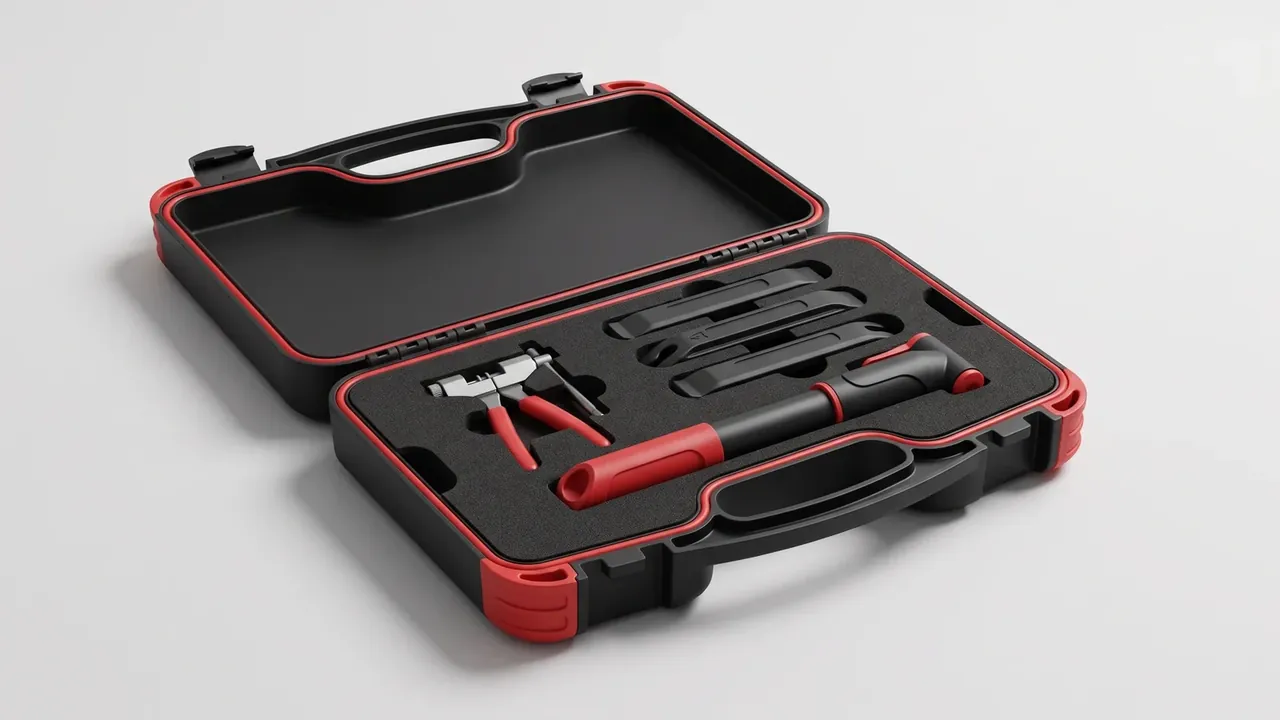
The pinch-off is 2 mm wide with 0.6 mm of flash, trimmed by a profiling knife run 0.5 mm from the edge: too far leaves a sharp lip, too close cuts the sealing plane.
Position matters more than finish: on the side centre the line escapes the stack load, and it is fixed before the tool is cut.
5. Sample Validation Before the Tool Is Cut
First samples are not for appearance but for three measurements: wall distribution, the thinnest corner and rim flatness.
Three cases, five checks: six wall readings each, 24 hours of water fill, a 150 kg stack, a 0.9 m drop, 8 Nm on the inserts. All five pass before volume; otherwise the parison program changes first, which costs far less.
| Feature | Allowance | Action |
|---|---|---|
| Mold line | 0.4 mm proud max | scrape flat, no sanding |
| Corner wall | 3.0 mm min | thicken the parison corner |
| Rim warp | 1.2 mm max | cooling fixture |
Conclusion
A customized blow molded plastic case is specified by three sets of numbers: a cavity scaled 1.8 percent, a wall held between 3.5 and 4.5 mm by 25 parison points, and a rating written as a 150 kg test with a temperature derating. Get those right and both sides sign the same customized blow molded plastic case.
This article discusses only the container (case body) side of specifications and design intent, and does not cover any handling, loading or use of the contents.
Related Reading
- Case mold maintenance rhythm
- Size and wall specifications for rotomolded cases
- Injection molded versus rotomolded cases
- Wall and load on heavy duty cases
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models