

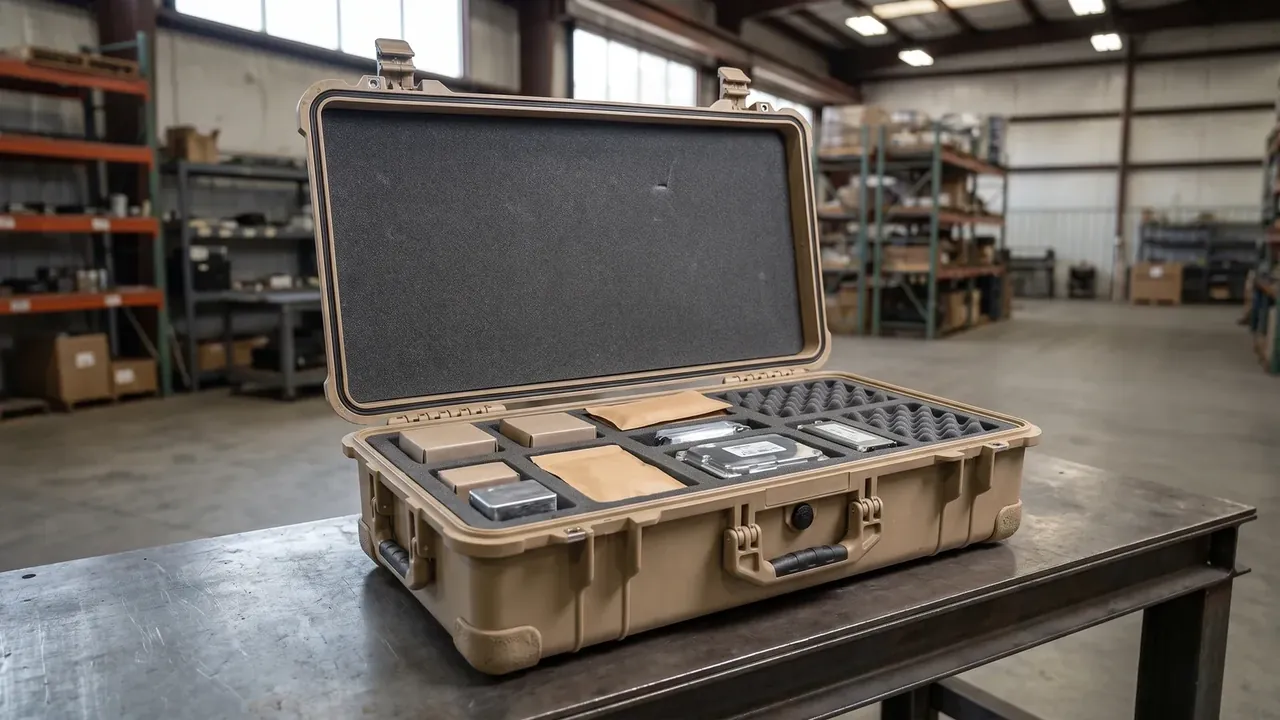
Quick answer: A Portable CNC cutting tool protective hard box pairs a 22 mm bottom rib with 7.0 mm slot walls, reading deflection under 20 kg held for 2 h.
Table of contents
- Bottom ribs of a Portable CNC cutting tool protective hard box
- Wall thickness of the cutter slots
- Base deflection under a point load
- Slot-wall indentation after unloading
- Rib-height setting for the cutter batch
- FAQ
1. Bottom ribs of a Portable CNC cutting tool protective hard box
A point load at the base centre bends the longitudinal rib first, while slot-wall thickness decides whether an indent survives unloading. This shell is 480 by 330 by 160 mm outside, 420 by 275 by 115 mm inside, with a 3.9 mm wall, one 22 mm floor rib and a 7.0 mm liner slot wall. Taller ribs stiffen the floor but drive more load into the slot walls, deepening the post-unload indent. Rib height leads the cutter-batch ledger for a Portable CNC cutting tool protective hard box.
Three heights of 18 mm, 22 mm and 26 mm run on one mould and one static rig, all cut to 7.0 mm slot walls. A rib outside forming tolerance biases deflection before the indent does; a shell with no batch number stays out of the ledger.
| Rib grade | Rib height | Slot-wall thickness |
|---|---|---|
| One lower | 18 mm | 7.0 mm |
| Nominal | 22 mm | 7.0 mm |
| One higher | 26 mm | 7.0 mm |
One lower grade pushes deflection to 1.4 mm past 1.1 mm; one higher pulls it to 0.6 mm but lifts the indent to 0.47 mm past 0.35 mm. Only 22 mm holds both, at 0.9 mm and 0.28 mm. On the lower grade a Portable CNC cutting tool protective hard box has no soft resin: a short rib spreads the moment poorly, while the higher grade hands the force to the slot wall.
2. Wall thickness of the cutter slots
A 7.0 mm slot wall is the second grading quantity, a continuous bearing face along the slot rather than a filled rim. Its thickness decides whether the wall springs back after 20 kg or dents.
Two latches close at 350 N each on one seal at 18% compression, logged on the same sheet. A thicker wall eats the floor's rebound, and latches not tightened together let the mouth slacken first, so a high indent is wrongly blamed on rib height. A Portable CNC cutting tool protective hard box files wall reading and latch force together and drops a shell missing either.
3. Base deflection under a point load
The static rig parks a 20 kg block at the floor centre for 2 h and reads deflection along the floor normal with a dial gauge to 0.1 mm. The verdict uses the full-load peak, not the unloaded residual, because the release line asks whether rib and wall carry the moment. Earlier readings are trend only.
| Load run | Single-run condition | Deflection reading |
|---|---|---|
| Run 1 | 20 kg / 2 h | 0.9 mm |
| Run 2 | 20 kg / 2 h | 1.0 mm |
| Run 3 | 20 kg / 2 h | 1.0 mm |
Run 1 reads 0.9 mm, Run 2 rises to 1.0 mm and Run 3 stays at 1.0 mm, so the rib stops relaxing. Deflection of 1.1 mm and indent of 0.35 mm fill two columns of one ledger, and one filled column is no pass; the stretch past 2 h is filed without a grade. The static ledger for a Portable CNC cutting tool protective hard box takes only the 2 h row.
4. Slot-wall indentation after unloading
Unloading does not close the verdict: the liner comes out of the same shell and a depth gauge reads the pit at the wall root to 0.01 mm. Deflection and indent are separate: a taller grade bends the floor less but presses the wall harder, so the pit deepens.
| Deflection value | Rib grade | Slot-wall indentation |
|---|---|---|
| 1.4 mm | One lower | 0.20 mm |
| 0.9 mm | Nominal | 0.28 mm |
| 0.6 mm | One higher | 0.47 mm |
Set the three side by side: 1.4 mm crosses on deflection, 0.6 mm looks best yet its 0.47 mm indent crosses 0.35 mm, and only 0.9 mm holds both. A shell never revisited after unloading earns no grade; the indent counts only after full load. A Portable CNC cutting tool protective hard box keeps the indent in its own column, apart from deflection.
5. Rib-height setting for the cutter batch
The cutter batch closes on one line: the shortest grade whose deflection after a 20 kg load stays below 1.1 mm becomes the setting, and any shorter rib stays off the cutter box drawing. Empty weight 3.8 kg, load 11 kg, 4400 cycles and two latches at 350 N freeze as boundary conditions; a new mould restarts the static trial and the unloading recheck.
No single sample stands for the batch. Rib grade, wall thickness, full-load deflection and post-unload indent are logged for every shell, and four matching cells admit it; one missing or crossed cell sends only that shell back. Moulding parameters and static readings sit in separate columns for a Portable CNC cutting tool protective hard box; drawing tolerances trace to the rig, and one seal at 18% is filed in the lid column.
Conclusion
Lining up rib height, slot wall and post-unload indent grades a Portable CNC cutting tool protective hard box for a cutter batch: a 22 mm rib holds full-load deflection to 0.9 mm, a 7.0 mm wall keeps the indent at 0.28 mm, and neither borrows margin from the other. One crossed cell sends that shell back. JUNZHIJIA files 4400 open-close retest records by batch; drawing tolerances come afterwards from Kexin New Materials (Guangdong) Co., Ltd.
Related Reading
- EPE Foam vs EVA Foam in a Tool Box: What Is the Difference?
- Rust on a Metal Toolbox: How to Remove It and How to Stop It Coming Back
- Woodworking Machine Cases: Cutter & Spindle Component Protection
- Four Core Parameters for Choosing a Toolbox: Durability, Portability, Function and Materials
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models