

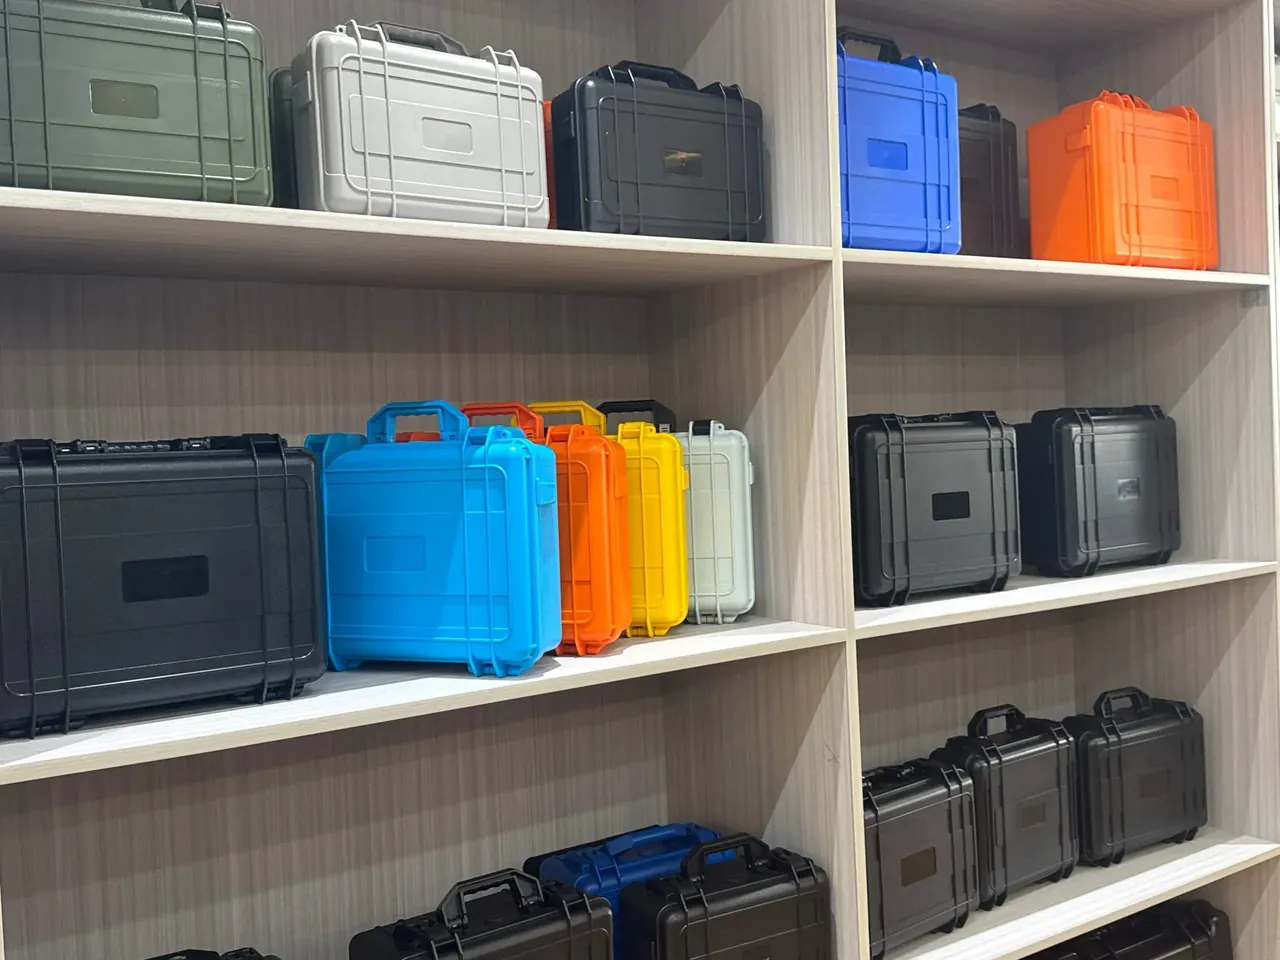
Quick answer: In small batch case customization the minimum order is a division problem, not a policy. A mould swap costs six to eight hours of press time however few parts you buy, and that block spreads across 200 or 2000 units at about 5 CNY.
Table of contents
- Small Batch Case Customization Starts at the Changeover
- What a Changeover Costs in Hours
- Colour and Foam Inserts Add a Floor
- The Cost Curve From 200 to 2000
- Four Ways to Shrink the Changeover
- FAQ
1. Small Batch Case Customization Starts at the Changeover
Small batch case customization is charged per tool, not per unit: aligning, clamping, plumbing and ejector travel take as long for 100 units as for 5000.
The quote is a division. Changeover hours times the machine rate, plus trial scrap, over margin. Six hours at 180 CNY is 1080 CNY, and at 4 CNY of margin 270 units recover it, hence the 200 to 300 floor.
| Order size | Amortisation (CNY) | Landed cost (CNY) | Slot |
|---|---|---|---|
| 200 | 5.4 | 58 | Inserted, waits |
| 500 | 2.2 | 55 | Shared colour run |
| 2000 | 0.5 | 53 | Priority |
| 5000 | 0.2 | 53 | Dedicated |
The curve flattens: 200 to 500 removes 3.2 CNY, 2000 to 5000 only 0.3.
2. What a Changeover Costs in Hours
Seven steps: 45 minutes stripping the old mould, 50 aligning to 0.05 mm, 20 for water and sensors, 60 to 90 for heat soak to 50 degrees Celsius, 40 purging, 40 for trials, 25 for the first article, totalling 4.7 to 5.2 hours.
Heat, not the crane, is the bottleneck. Preheating 40 minutes early is the only free compression, and five scrapped trials cost 2 kg.
| Step | Minutes | Constraint | Overlap |
|---|---|---|---|
| Old mould out | 45 | Sticking ejectors | No |
| Alignment | 50 | 0.05 mm parallelism | No |
| Heat soak | 60 to 90 | 2.5 to 3.5 mm wall | Preheat |
| Trials and first article | 65 | Shrink, flash | No |
3. Colour and Foam Inserts Add a Floor
Colour and mould changes stack. Charcoal to black is a 40 minute purge; to a light tone, three passes of 8 minutes plus hopper cleaning, so 70 minutes. Colour is judged on Delta E, where 1.5 is visible, so one masterbatch lot is required. For small batch case customization that means 25 kg, enough for 3000 units at 380 grams and 2% letdown.
Foam adds a floor. An EVA die costs 1800 CNY and three days, or 18 CNY per set across 100 sets; CNC cutting skips it at 12 minutes per set, holding radii to R3 or above.
4. The Cost Curve From 200 to 2000
Material and moulding scale linearly at about 26 CNY per unit; changeover is one 1080 CNY batch charge; finishing drops from 4 to 3.4 minutes after 500 units. The gap sits in the middle line: 5.4 CNY per case at 200 units against 0.5 at 2000, a share of 9% against 1%.
| Cost line | 200 units | 2000 units | Behaviour |
|---|---|---|---|
| Material and moulding | 26 | 26 | Linear |
| Changeover | 1080 | 1080 | Fixed |
| Landed unit cost | 58 | 53 | 5 CNY gap |
The break is near 800 units: below it, recolouring an existing mould beats a 28,000 CNY tool, and in small batch case customization that is the line worth arguing over.
5. Four Ways to Shrink the Changeover
A quick-change platen with hydraulic clamps locks four points at once, cutting alignment from 50 minutes to 12. It costs about 16,000 CNY and pays back in forty changeovers.
Preheat costs nothing: warm the next mould during the previous job and save 40 to 60 minutes.
Colour batching covers three jobs with one purge, at two to three days of slippage.
Standard body plus finishing sprays a stock mould at 6 CNY per case, or wraps it in 0.4 mm PVC at 3.5 CNY, pushing the floor to 50 units.
Stacked, they bring a changeover in small batch case customization to 3.5 hours and amortisation on 300 units from 5.4 to 3.2 CNY.
Conclusion
A minimum order looks commercial but behaves like a process calculation. The changeover does not shrink with quantity while the amortisation does, and the whole 5 CNY gap comes from that line. Move the floor by sharing a changeover or compressing it below 3.5 hours, and a quote for small batch case customization stops being a yes or no answer.
This article discusses only the container (case body) side of specifications and design intent, and does not cover any handling, loading or use of the contents.
Related Reading
- Seven stages of a case customization project
- EVA insert thickness and cavity specifications
- Selection parameters for injection moulded protective cases
- Pallet building for mixed specification orders
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models