

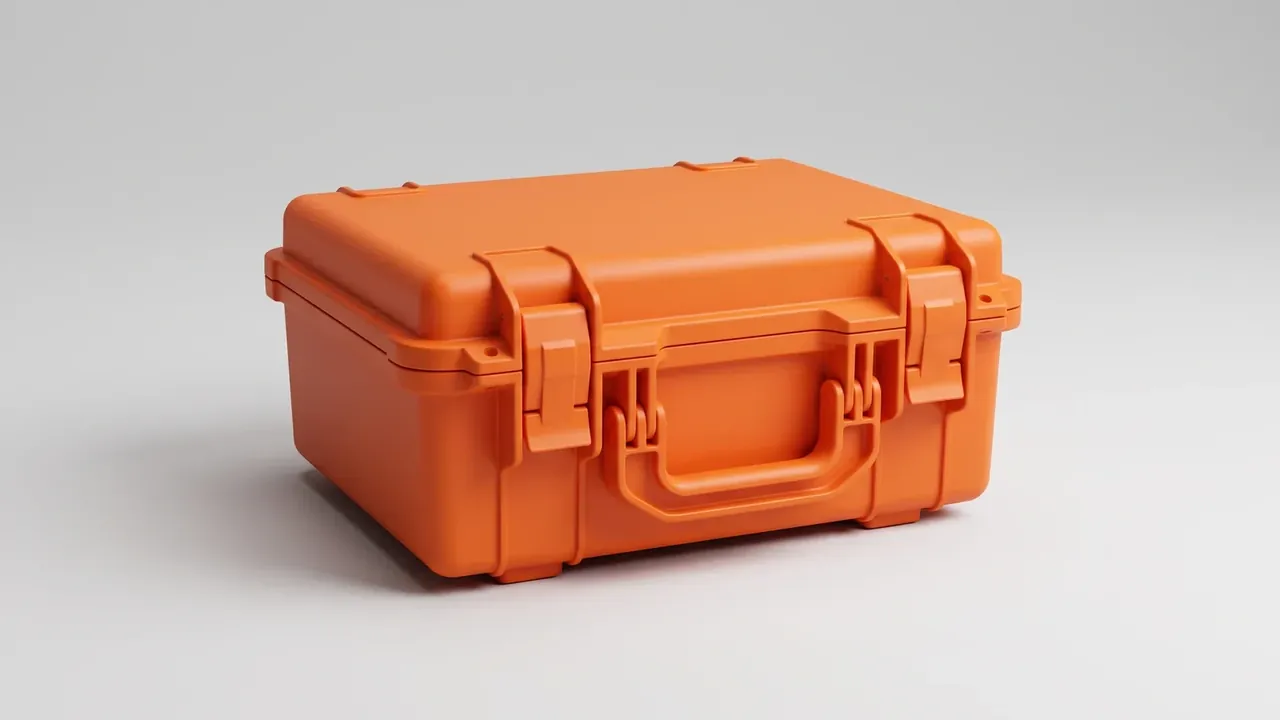
Quick answer: A Case Factory Tour is a timing exercise: 3 hours of drying at 90 degrees Celsius, 210 seconds per shot on a 1600 tonne press, a 4 mm wall, 90 seconds on the leak bench. Follow one cycle and capacity stops being a claim.
Table of contents
- Cycle Time Before Equipment
- Four Stages From Pellet to Lid
- Wall, Ribs and Parting Line Live in the Mold
- Three Fits at the Assembly Bench
- Leak, Drop, Packing: Where the Numbers Land
- FAQ
1. Cycle Time Before Equipment
Most visitors photograph nameplates first. A nameplate states a ceiling, never a habit, so a Case Factory Tour should start at the cycle: how long one body takes from hopper to carton.
A 1600 tonne press running a 620 by 420 mm body cycles at 210 seconds. Subtract changeovers and stops and an 8 hour shift yields about 130 units; a 45 minute changeover twice a day drops that to 110.
| Step | Time per unit | Pass mark | Warning |
|---|---|---|---|
| Drying | 90 C, continuous | Under 0.02% moisture | Caked resin |
| Moulding | 210 seconds | Drift under 5 seconds | Cycle cut to 180 |
| Extraction | 8 seconds | No sticking | Manual prying |
| Trimming | 30 seconds | Nail passes clean | Knife needed |
| Assembly | 95 seconds | Three fits seated | Hammer used |
| Leak test | 90 seconds | Drop under 0.02 bar | Visual check |
2. Four Stages From Pellet to Lid
On a Case Factory Tour, drying comes first. Polypropylene picks up water, and above 0.05% the wall shows silver streaks; three hours at 90 degrees Celsius is the setting, and a 5 degree gap between hopper and dryer display invites a question.
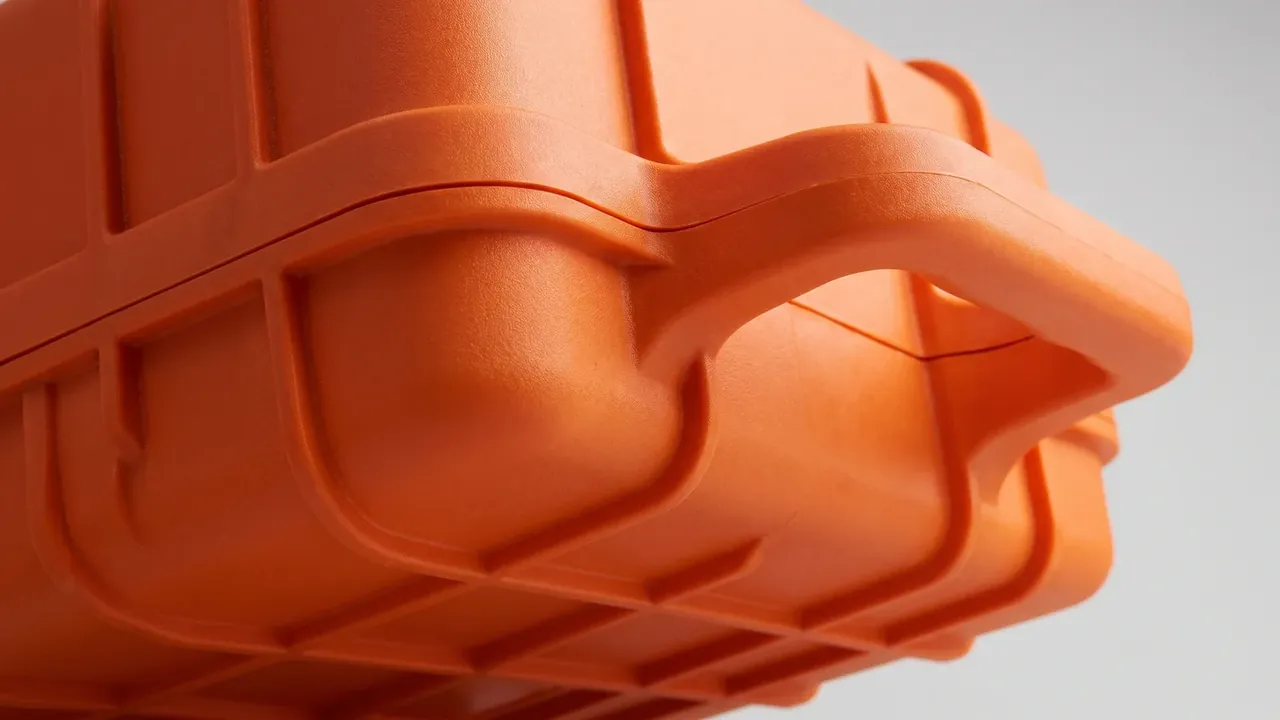
Injection follows at 210 to 230 degrees Celsius melt, 45 to 60 mold, 90 to 120 bar. Clamping force runs 400 kg per square centimetre of projected area, so a 620 by 420 mm body needs 850 to 1,200 tonnes.
Cooling takes 60% of the cycle, and a 3 degree spread bows the body; trimming closes the loop, where flash a fingernail passes means the faces still seat.
| Stage | Parameters | Normal band | Where to read it |
|---|---|---|---|
| Drying | 90 C, 3 hours, 0.02% | Caked resin | Hopper glass |
| Injection | 210 to 230 C, 90 to 120 bar | Short shots | Press screen |
| Cooling | Water delta | Under 3 C | Return line |
| Trimming | Flash | Nail passes clean | Parting line |
3. Wall, Ribs and Parting Line Live in the Mold
A Case Factory Tour will show 4 mm as the standard wall. At 3 mm the corner cracks first in a drop, at 6 mm sink marks follow, and variation should stay inside 0.2 mm.
Ribs are not a quantity contest: thickness at 0.6 of the wall, about 2.4 mm, height 18 mm, draft 1 degree. Too thick sinks the outer face; too dense traps air, so corners scorch through 0.03 mm vent grooves.
The parting line is fixed in steel, mid-wall trimming cleanly while a radius leaves a scar. The tool weighs 6.5 tonnes in 718H with a 300,000 shot life.
| Feature | Value | Why | Failure sign |
|---|---|---|---|
| Wall | 4 mm, 0.2 mm tolerance | Drop strength against cooling | Whiten at corners |
| Ribs | 2.4 mm by 18 mm | Stiffness without sinking | Dents outside |
| Draft | 1 degree | Clean release | Scuffing |
| Parting line | Mid-wall | Easy trimming | White scar |
4. Three Fits at the Assembly Bench
On a Case Factory Tour, assembly decides how the case feels. Get latch, hinge and gasket right and a body takes 95 seconds.
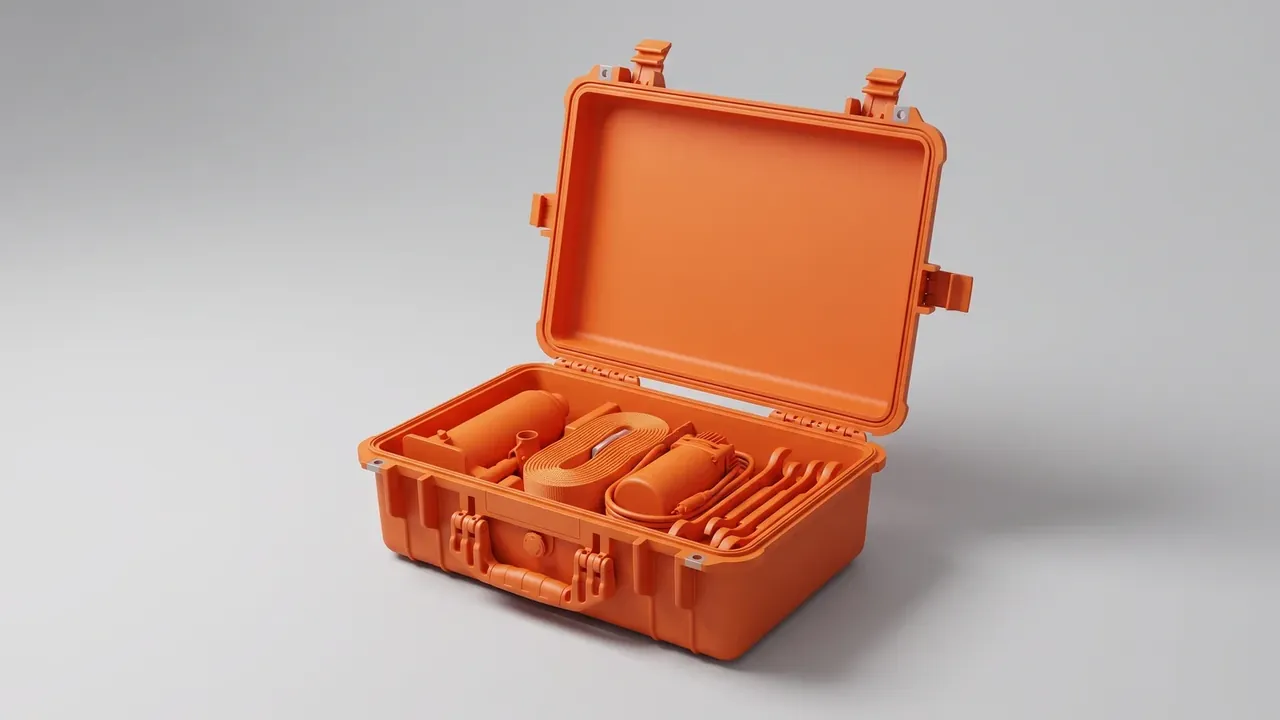
Latch force is a number: six M5 screws at 2.5 N·m, torqued diagonally, hold a lid shut above 40 N of pull. Hinge play comes next: 0.15 mm between pin and bore stops the lid rocking.
Gasket compression closes the list: 30% to 35% squeeze seals the joint, past that it lifts the lid, and a 65 Shore A compound holds its memory.
5. Leak, Drop, Packing: Where the Numbers Land
On a Case Factory Tour, leak, drop and salt spray are where every parameter lands. Leak testing means 0.3 bar held 90 seconds with a drop under 0.02 bar, and salt spray runs 72 hours.
Drop testing covers 1.5 m on six faces: no crack, no latch release, no liner shift, all three or the lot stops.
Packing is measured too: 25 units per 1200 by 1000 mm pallet to 1.3 m, where three tiers put 46 kg times three on the bottom body.
| Test | Condition | Pass mark | Shortcut |
|---|---|---|---|
| Leak | 0.3 bar, 90 seconds | Under 0.02 bar | Visual check |
| Drop | 1.5 m, six faces | No crack, no release | One face |
| Salt spray | 72 hours | No red rust | Cut to 24 hours |
| Stacking | 3 tiers at 46 kg | No permanent set | Single tier |
Conclusion
Time one cycle, trace it through the stages, watch the numbers land on the test bench: a Case Factory Tour then produces evidence, not photographs. Presses can be bought; a steady cycle cannot.
This article discusses only the container (case body) side of specifications and design intent, and does not cover any handling, loading or use of the contents.
Related Reading
- The sheet to prepare before you travel
- Twenty questions to ask at the gate
- How a gear case body and fittings work together
- Where a knife case gets its stiffness
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models