

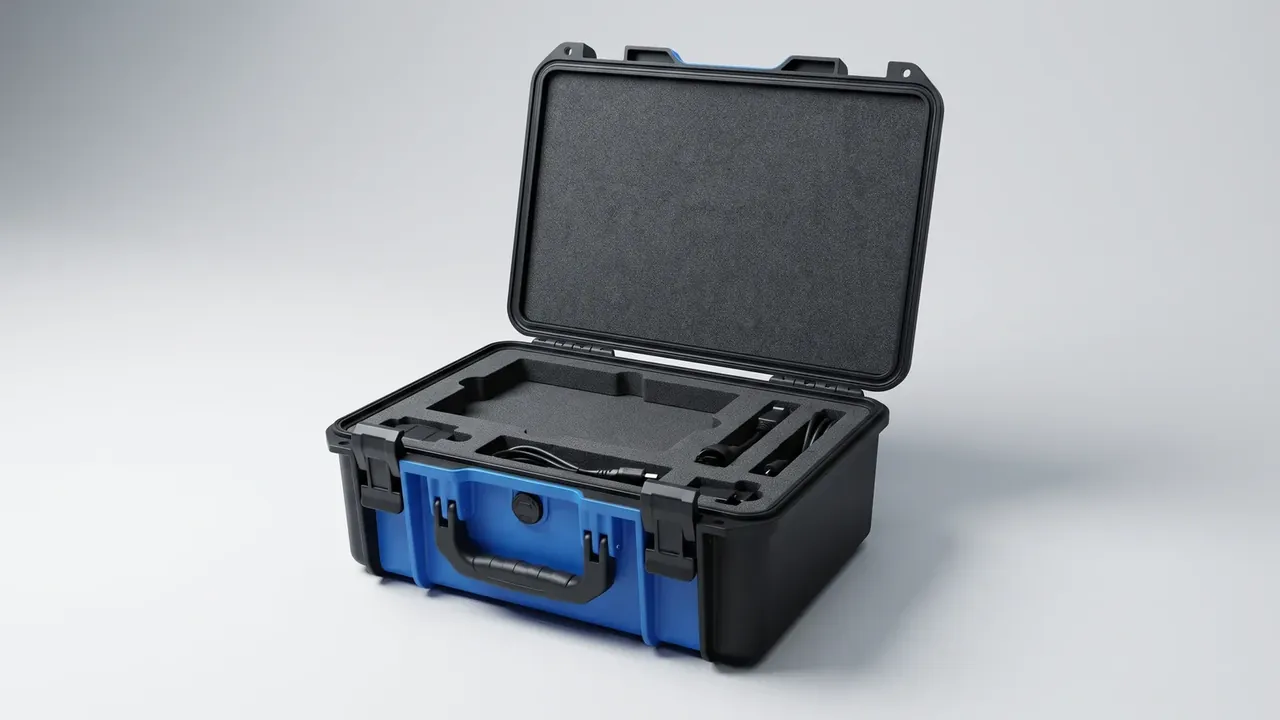
Quick answer: A Custom Traffic Equipment Case Factory pairs 210 mm ear pitch with a 40 mm exit bend radius and a 3.2 mm boot wall to hold roadside cracks under 1.8 mm.
Table of contents
- Roadside Vibration Load at a Custom Traffic Equipment Case Factory
- Mounting Ear Pitch and Mode Shape
- Bend Radius at the Cable Exit
- Fatigue Cracks in the Exit Boot
- Ear Pitch Values for Roadside Batches
- FAQ
1. Roadside Vibration Load at a Custom Traffic Equipment Case Factory
A two-hour sweep from ten to five hundred hertz shows whether the boot or the ear bolt fails first, and where. A Custom Traffic Equipment Case Factory hangs the shell on four ears clamped to a pole: input enters at the bolt holes, climbs the side wall and leaves through the thinnest ring, the boot. Where peak frequencies at ear root and exit boss disagree, a section between them amplifies displacement for the case.
Roadside input is never one frequency. Lorry traffic shakes ten to sixty hertz, wind sway sits in the middle, expansion joints knock transients past three hundred hertz. A sweep locates the shell's first two modes. Inside the ten to five hundred hertz band a two-hour dwell grows a small defect into a readable crack; outside it the trace stays flat.
2. Mounting Ear Pitch and Mode Shape
Pitch is 210 mm with φ9 mm holes, four ears paired along the long sides. Widen it and the wall between two ears becomes a long-span plate, so the first mode drops; narrow it and stress crowds into the root fillet. A Custom Traffic Equipment Case Factory sets 560 mm bodies at 210 mm, where those two directions meet.
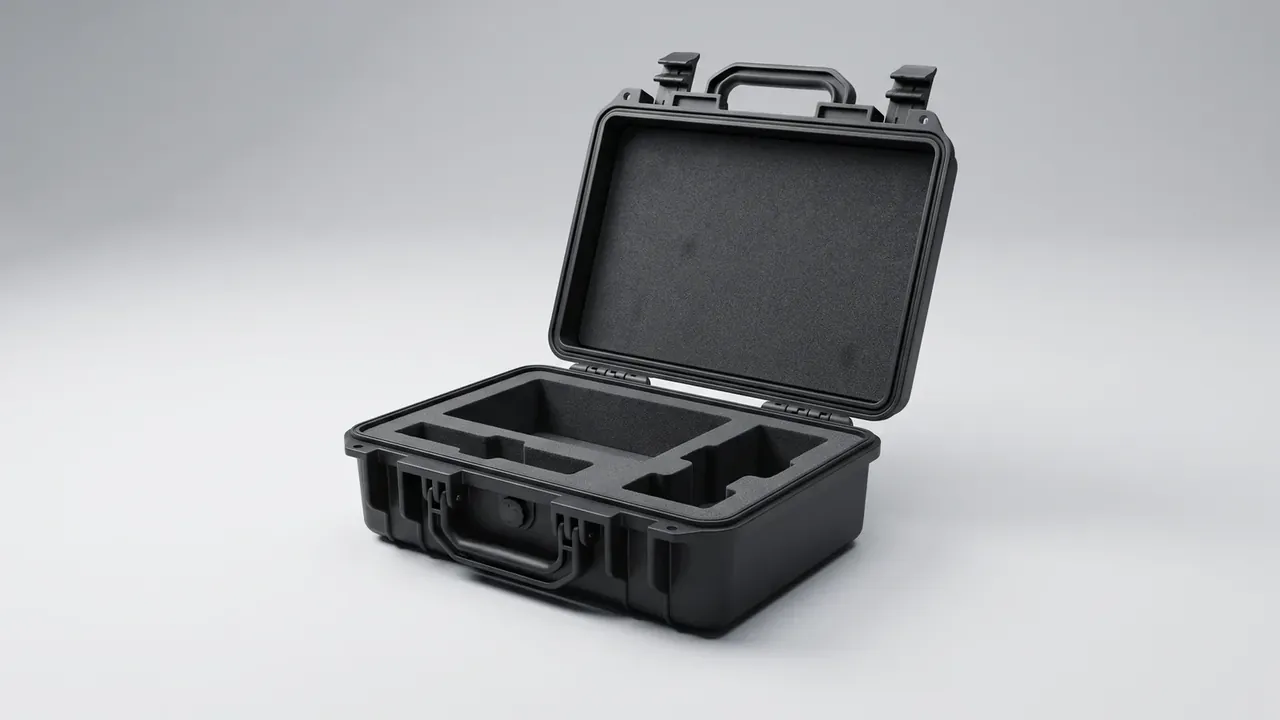
One tier wider is buildable, but the cost lands on the floor. Ears near the corners press preload onto the radius transition, and a floor slightly out of flat stands on three points. Assign a tier by body span before any transducer goes on.
| Ear bracket tier | Pitch and hole | Body span served | First check |
|---|---|---|---|
| Narrow | 150 mm / φ9 mm | Under 560 mm | Ear root fillet stress |
| Baseline | 210 mm / φ9 mm | 560 to 640 mm | First mode inside band |
| Wide | 270 mm / φ9 mm | Above 640 mm | Four-point floor contact |
Bolt fit follows pitch. A φ9 mm hole takes an M8 bolt, and all four holes are drilled in one jig in a single pass at a pitch tolerance of plus or minus 0.3 mm. Skip the jig and two diagonals run tight.
3. Bend Radius at the Cable Exit
The exit sits low on the side wall with a φ22 mm bore. Cable runs straight for at least 1.5 times the exposed boot length before any bend, and the radius on the inner jacket face is no less than 40 mm. At 25 mm outer strain doubles, enough for two hours of sweep to leave a pale ring.
Fixed wiring takes four to six times the outer diameter, moving runs about ten; glands quote six to eight at the entry. Here 40 mm is routing margin, not a target to scrape.
Pointing the exit down costs nothing. Rain drips off the jacket instead of pooling on the seal, and a cable tie fifty to one hundred millimetres below the entry takes the pull. A Custom Traffic Equipment Case Factory puts both notes on the assembly drawing.
| Sweep window | Rig state | What it records |
|---|---|---|
| Zero to thirty minutes | Low band, ten to sixty hertz | Ear bolt preload walks |
| Thirty to ninety minutes | Mid band, sixty to two hundred and fifty hertz | Boot root turns pale |
| 90 to 120 minutes | High band, 250 to 500 hertz | Crack passes 1.8 mm |
4. Fatigue Cracks in the Exit Boot
The boot wall is 3.2 mm with a fillet into the boss. Cracks start where that fillet lifts off and travel around the circumference, pale at first, later a gap that catches a fingernail. Read under a ten-times loupe and record the longest crack to 0.1 mm.
A Custom Traffic Equipment Case Factory has tried a 4 mm wall and found it worse, because a thicker wall raises outer strain at the same radius and sharpens the root concentration. At 3.2 mm with a 40 mm radius, cracks stay under 1.8 mm after the two-hour sweep. At 2.5 mm they cross the line just past the first hour.
Crack and leak do not arrive together. A 1.8 mm crack often passes a 100 L/m²·h rain run because the lip is still compressed. A thermal cycle then slows the rebound, and water tracks along the jacket. Write the criterion on crack length, not on dripping.
5. Ear Pitch Values for Roadside Batches
The ear tier is the widest one whose boot still shows a crack shorter than 1.8 mm after a two-hour sweep; any wider pitch returns to a new mounting-hole tool. That line ties pitch, bend radius and boot wall to a single ruling.
A Custom Traffic Equipment Case Factory also checks whether the latches close in one push after 3900 cycles, whether each of the four latches at 380 N pulls open, whether water film shows inside the boot after an IP66 jet, and whether the 50 mm reflective strip lifts after salt spray.
| Crack reading | Where it is read | Action |
|---|---|---|
| Under 0.6 mm | Fillet lift-off at the boot root | Record, run the next window |
| 0.6 to 1.8 mm | A quarter around the boot root | Re-check lip imprint, add rain |
| Over 1.8 mm | Boot root against the boss | Reject unit, change batch pitch |
The sheet that travels with the case carries three columns: pitch, radius, wall. The wall baseline is 4.3 mm: at 3.8 mm the bolt bearing area dishes, at 4.8 mm the extra mass raises root load. The 560×400×225 mm body and 495×340×165 mm cavity are dimensioned around that wall and the 210 mm pitch.
Conclusion
Three values settle roadside duty: ear pitch, exit bend radius and boot wall. A Custom Traffic Equipment Case Factory puts them in one rig plan, or a two-hour crack reading cannot be compared across batches.
Related Reading
- Corner Radius and Usable Volume
- Plastic Cases vs Wooden Crates in Transit
- CCTV Case Fixing and Lens Clearance
- Custom Construction Tool Case Factory
- Custom Communication Case Factory
Related Products
- 8 Series — Gun Cases; Military Equipment Cases; Camera Equipment Cases; Drone Cases; Watch Cases; Knife Cases; First Aid Cases; Electronics Equipment Cases
- WL8-2812 PP Gun Case — model WL8-2812
- All protective cases and toolboxes: 7 series, 158 models