

A meat processing hall is a wet, cold, saline and heavily washed environment. Equipment is hosed down daily with hot water or chlorinated sanitiser, so stainless steel sits under the combined attack of chloride ions and residual stress and pits easily. When a line is relocated, expanded or exported, the grinder blades and plates, the stuffer vacuum pumps and filling nozzles, and the sanitary clamp fittings that join the pipework are all too often packed into ordinary cartons or open totes. What arrives shows the cost: chipped blade edges, a blade-to-plate clearance opened from 0.08 mm to over 0.2 mm so the grinder heats and smears instead of cutting, vacuum pump vanes dented and oil pushed into the working chamber, and clamp seals crushed or missing so the pipework cannot be assembled on site.
JUNZHIJIA meat processing equipment cases treat food-contact safety as equal in importance to impact resistance. Liners are made from food-contact compliant materials and built as removable blocks that can be washed as a unit, stainless parts sit in separate compartments that keep edges away from polished faces, clamps and seals are indexed by size, and the shell includes drainage and drying routes. The result is a case that can go straight into a washdown cycle after road or cold-store transit without introducing a new contamination source.
Table of Contents
- Blade and Plate Edge Failure in Meat Grinders
- Auger Flights and Hopper Deformation Under Load
- Stuffer Vacuum Pump Rotors, Vanes and Oil Circuits
- Sanitary Clamp Fittings and Seals in Indexed Pockets
- Filling Nozzles and Portioning Mechanism Accuracy
- Passive Layers and Chloride Corrosion of Stainless Parts
- Food-Grade Liner Materials and Washdown Compliance
- Case Sealing and Drainage for Washdown Cycles
- Condensation Management Across Cold Chain and Humid Shifts
- Heavy-Part Support, Stacking and Post-Wash Drying
- Microbial Risk and Removable Washable Liners
- Unpacking Acceptance and Hygiene Check List
- Custom Liners, Tooling and Compliance Documentation
Blade and Plate Edge Failure in Meat Grinders
The working pair at the heart of a grinder is the blade and the perforated plate. They run with a very small clearance, usually between 0.05 and 0.15 mm, and that gap creates the shearing surface. Once an edge rolls, chips, or the plate loses flatness, shearing degrades into crushing: product is rubbed repeatedly inside the barrel, discharge temperature rises, colour darkens, fat begins to render, throughput falls and energy consumption climbs. The transit causes are narrow and predictable. Blades and plates are packed together, an edge rests directly on the case floor, or several blades are threaded onto the centre shaft and knock against each other.
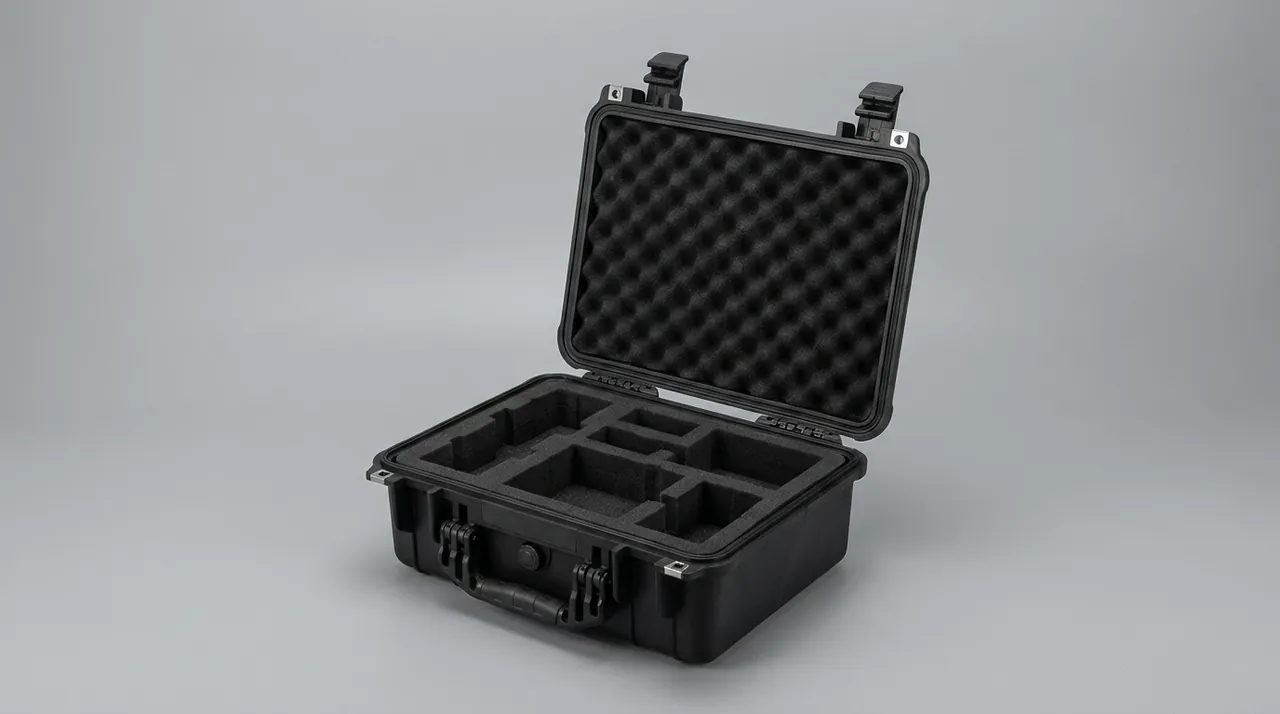
Pocket design therefore starts from one rule: no cutting edge ever touches a rigid surface. A blade sits with its edge angled upward, carried on the back face and the centre bore, with at least 3 mm of clearance beneath the edge. The plate lies face down in its own shallow pocket whose floor is faced with IXPE, so the working face cannot be marked by a trapped particle. Blades and plates must never be stacked, even with a foam sheet between them, because foam compresses under stacking load and the two surfaces eventually meet.
| Grinder component | Sensitive feature | Typical tolerance | Transit protection focus |
|---|---|---|---|
| --- | --- | --- | --- |
| Blade edge | Edge straightness and hardness | Clearance 0.05 to 0.15 mm | Edge suspended, load on blade back |
| Perforated plate | Flatness and hole burrs | Flatness within 0.05 mm | Own shallow pocket, face not loaded |
| Auger | Flight clearance and coaxiality | Barrel clearance 0.5 to 1 mm | Axial cradle, no side loading |
| Pre-cutter | Tooth profile integrity | Tooth pitch within 0.1 mm | Teeth inboard, bagged separately |
| Centre and square shaft | Keyway and straightness | Straightness within 0.1 mm | Long channel, located at both ends |
One detail is easily missed. Grinder blades are normally vacuum heat treated, which gives high hardness and limited toughness, so an impact chips the edge rather than bending it. A chipped edge cannot be dressed back with a stone the way a rolled edge can, and the part is usually scrapped, so blades need fragile-component protection rather than ordinary stainless handling.
Auger Flights and Hopper Deformation Under Load
An auger is a slender helical part, and the clearance between its flight outside diameter and the barrel bore sets both conveying efficiency and product retention. That clearance is typically in the 0.5 to 1 mm band. If the auger takes a lateral squeeze in transit and bows, one side of the flight runs against the barrel while the other leaves a wide gap, which shows up as unstable feed, product flowing back, and a barrel that is hard to clean. The more serious consequence is that a bowed auger rubs the barrel in service and generates metal particles, which in meat processing is a direct safety hazard and can force a product recall.
The protection method is an axial cradle with location at both ends. Cut a continuous semicircular channel parallel to the axis so the auger is supported along its whole length. Fit a stop at each end to limit axial movement, and let the centre shaft ends sit in separate blind holes so lateral force is taken by the bore wall rather than the flight. Never lean an auger diagonally into a case corner, because that concentrates load on a small area and reliably produces a permanent bow.
Hoppers are usually fabricated from thin stainless sheet and have low stiffness, so they dent permanently under pressure. Load a hopper mouth upward with a temporary internal support ring, or a cross brace, to hold circularity; fill between the outer wall and the case with EPE but without interference so no dent is pressed in. If the hopper carries an agitator shaft or a safety grid, remove the agitator and pocket it separately rather than shipping it attached.
On combined grinder and loader modules, lock the lift arm in its transport position and secure it with a dedicated bracket so hydraulic and pneumatic elements cannot swing against the case wall. Mark the locking point in yellow and put a reminder label on the lid so nobody starts the machine before releasing the lock.
Stuffer Vacuum Pump Rotors, Vanes and Oil Circuits
A vacuum stuffer draws air out of the hopper so the meat mass is compacted under negative pressure and fills the casing evenly. Rotor, vane and end-face fits in the pump determine ultimate vacuum and pumping speed. Once a vane is dented or a rotor face is scored, vacuum falls away and the symptoms appear at the filler: air inclusions in the casing, unstable density, and greater weight deviation between portions.
Rotary vane pumps have three transit problems: oil migrating into the working chamber, vanes crushed against the rotor, and side loading on the shaft. Oil migration is the most common: if the pump is tilted or inverted, lubricant passes the discharge valve into the chamber and on restart the machine spits oil and takes a long time to reach vacuum. Drain to the minimum level as the maker requires, fit a sealed plug at the oil port, print a bold upward arrow on the case, and include a tilt indicator inside so the receiving team can see whether the pump was inverted.
Vanes and rotor form a hard and brittle combination, so fix the pump in its own compartment, support the body at four points and keep the shaft ends unloaded. Where pump and motor are separate, pocket them separately and take the load on the coupling locating face rather than the exposed shaft. Water ring impellers are thin-walled, so fit a liner plate of matching material on each side and let stacking load pass through those plates.
| Pump element | Failure symptom | Cause | Protection |
|---|---|---|---|
| --- | --- | --- | --- |
| Vanes | Chipped edges, sticking | Rotor crushing vanes after tipping | Four-point support, keep level |
| Rotor face | Scoring, clearance growth | Face load or debris ingress | Face guard, plug the inlet |
| Oil circuit | Oil spit, low vacuum | Inversion driving oil into chamber | Lower oil level, plug, orientation label |
| Coupling | Coaxiality out of tolerance | Pump and motor shipped apart without location | Separate pockets, load on locating face |
| Seals | Hardening, set | Long compression or oil contact | Own pocket, away from oil and heat |
Sanitary Clamp Fittings and Seals in Indexed Pockets
Sanitary clamp fittings, in the tri-clamp pattern covered by DIN 32676, ISO 2852 and 3A practice, join pipework, pumps and valves into a complete system, and a single relocation can call for anywhere from dozens to hundreds of them. They are numerous, varied in size and small, which makes them a prime target for loss and mixing. The seal inside each clamp matters just as much: silicone or EPDM seals take a permanent set when compressed, and a deformed seal fitted to pipework leaks, which meat processing tolerates poorly.
Build the liner by size first, then by layer. Assign a large pocket to each pipe diameter, for example 1 inch, 1.5 inch, 2 inch and 3 inch, and split each pocket into three layers for clamp body, pin and bolt, and seal, separated by soft dividers. Label every pocket with size and quantity and fix a matching list inside the lid.
Seals must be kept away from oil, heat and long-term compression. Store them in a lidded box or their own pocket, never loose with metal parts and never bundled with a cable tie. Compression set is the main failure route, so cut the pocket slightly deeper than the free height of the seal and let it travel essentially unloaded. If a batch of seals has to be stored with the machine for a long period, add a label recording material, size and recommended replacement interval so the schedule is not left to memory.
Clamp pins and bolts work loose and disappear, so run each nut to the end of its pin in a half-locked position; it will neither separate in transit nor pre-compress the seal. Apply a thin film of food-grade grease to the threads to stop corrosion seizing them.
Filling Nozzles and Portioning Mechanism Accuracy
Filling nozzles, portioning gears and vane-type portioning units form the metering end of a stuffer, and they set the weight deviation between portions. Nozzle bore and bore surface roughness govern flow resistance, so a scratched bore or a distorted outlet changes the flow characteristic. Portioning gear and vane clearances are very tight, often only 0.02 to 0.05 mm, and any impact destabilises metering.
Nozzles are thin-walled tubes, so protect them from inside and outside. Internally, insert a soft mandrel matched to the bore, in polyoxymethylene or food-grade PE, to stop the wall ovalising under load. Externally, fit a PE or food-grade silicone cap over the outlet so the lip cannot be struck. Pocket nozzles by bore size and never mix sizes in one pocket, because nesting one inside another scores the bore.
Portioning gears and vane pump rotors are matched components. Treat them as a set with a single identification number and note the pairing on the packing list. Gear and housing are lapped together and are not interchangeable; once the pairing is lost, restoring the original accuracy requires lapping equipment that is rarely available on site.
Drive shafts, encoders and proximity switches belong in a dry compartment. A proximity switch face deforms under pressure, so sleeve it. Load cells are high-precision elastic elements and must stay locked with their transport bolts, released only before use; put that instruction on the card inside the lid.
Passive Layers and Chloride Corrosion of Stainless Parts
The threat to stainless steel in a meat plant comes from chloride. Sodium hypochlorite and chlorinated alkaline detergents destroy the passive film when they remain on a surface, and combined with residual stress they drive pitting and stress corrosion cracking. Transport is often where corrosion begins: a part comes off the line with blood water, salt and detergent on it, gets boxed in a closed humid space, and after a few weeks at sea shows rust at contact faces, threads and weld toes.
The order of operations is therefore non-negotiable: neutralise and wash first, dry completely, and only then pack. Rinse off residue, brush with a neutral or mildly alkaline detergent, rinse again with deionised or softened water to cut chloride carry-over, blow out recesses with compressed air, and where necessary dry at 60 to 80 degrees Celsius. Confirm the part has cooled to room temperature before it goes in. Never pack parts straight after a chlorinated sanitiser, and never pack with a water film still on the surface.
Contact corrosion is a second route, particularly when grades such as 304 and 316L travel together, so separate stainless parts with IXPE or food-grade EVA. Coat threads and keyways with a food-grade rust preventive or VCI film and state in the shipped documents that it must be washed off before use. Never apply tape to mirror-polished surfaces, because adhesive residue cures during hot washing and is very difficult to remove.
Salt spray testing to the GB/T 10125 or ISO 9227 method is a common way to assess corrosion-resistant packing, and the conditions and interpretation are set out in a guide to salt spray corrosion testing. Be careful with the result: salt spray hours do not map linearly onto service life, so treat the figure as a comparative measure and agree any conversion basis in writing rather than quoting hours as a service-life guarantee.
Food-Grade Liner Materials and Washdown Compliance
A liner has to cushion and to satisfy food-contact compliance at the same time, and those two demands do not pull in the same direction. The regulatory basis includes the GB 4806 series for plastic materials in food contact in China, EU 10/2011 in Europe and the relevant FDA 21 CFR sections in the United States; compliance turns on the base polymer grade, the additives used and migration limits. The supplier must provide a material declaration and migration test report rather than an assurance that the product is food grade.
| Material | Food-contact compliance | Washdown suitability | Cushioning behaviour | Typical position |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Food-grade EVA | Achievable with declaration | Warm water and neutral detergent | Moderate rebound, low creep | Precision part pockets |
| Food-grade PE (IXPE) | Achievable, closed cell, low water uptake | Tolerates alcohol wipe | Slow rebound, very low creep | Precision face facing |
| Polypropylene (PP) board | Achievable, good heat tolerance | High-pressure washdown | No cushioning, pairs with foam | Dividers and pallets |
| Silicone pad | Achievable, widest temperature band | High-temperature disinfection | Local cushioning | Blade contact faces |
| Ordinary recycled EPE | Not recommended | Absorbs water, slow to dry | Low cost | Non-contact outer layer only |
The recommended build is EPE on the outside for energy absorption, food-grade EVA routed in the middle for the pocket geometry, and food-grade IXPE or a silicone pad wherever a part touches the liner directly. Everything in direct contact should withstand washing above 80 degrees Celsius without distortion and should not absorb grease or protein. Where the temperature range is not documented, ask the supplier for dimensional stability data after two hours at 80 degrees Celsius.
Meat plant cleaning normally runs as foaming detergent, hot high-pressure rinse and then chlorinated sanitiser, and a liner that lets water into its core will support microbial growth. Build the liner as removable blocks with no blind holes and radius the edges so they can be wiped. Where parts enter a high-hygiene zone, the clean packing approach used in cleanroom equipment cases is a useful model.
Case Sealing and Drainage for Washdown Cycles
Meat processing parts usually get a wash before installation, so the case itself has to survive the cycle of open, take out, wash the case, put back. That rules out a design that considers only transport sealing and ignores drainage and drying.
The trade-off between sealing and drainage is the core decision. A fully closed case held shut for weeks traps moisture next to stainless parts and seals. A case with open drain holes loses its protection class. A workable compromise is a removable drain plug in the base: screwed in with a gasket for transport, then removed on arrival so the case drains naturally, with compressed air blown through the port for fast drying, and refitted once the case is dry. The design keeps the transport seal while solving drainage in service.
Where high-pressure hot water or steam disinfection is involved, assess the cleaning tolerance separately. IP69K is the common high-temperature, high-pressure jet rating, tested with hot water near 80 degrees Celsius sprayed at close range from several angles, which is a different logic from the short immersion behind IP67. The difference in scope between the two is explained in a comparison of IP69K and IP67 ratings. If the case travels into the wash bay with the machine, select towards IP69K and confirm the temperature range of the gasket and latches.
Avoid right-angle corners inside the case so it rinses clean, and make latches and hinges removable from outside the shell. Keep paper labels out and use polyester or metal nameplates that survive repeated washing, because a peeled paper label becomes a foreign body.
Condensation Management Across Cold Chain and Humid Shifts
Meat processing equipment moves between cold stores and ambient halls, and the temperature difference produces heavy condensation. A part stored at 4 degrees Celsius and opened in a 25 degree hall forms a water film within minutes, and that film sits on stainless parts and seals, creating both a corrosion and a microbiological risk. This route is harder to manage than plain humidity because it happens after packing.
Managing the rate of warming is the first lever. Park the case in a transition area for four to eight hours on arrival so the shell warms slowly, then open, and put that instruction on the case label. The second lever is free water inside: displace the air with dry air before closing, add enough food-grade desiccant and include a humidity indicator card so the receiving team can decide whether the contents may go straight into a wash cycle.
Size the desiccant by the net internal volume of the packed space rather than the external case dimensions. A starting point of three to five grams of indicating desiccant per ten litres of enclosed air is reasonable, adjusted for route duration and the temperature swing on the lane. Parts that are salty or still damp, such as a freshly rinsed filling nozzle, must be dried fully before packing, otherwise the desiccant saturates quickly and stops working.
For spare-part cases that sit in a cold store for months, a case with a pressure equalisation valve is the better choice. Low temperatures draw a partial vacuum inside a sealed case, which can make the lid hard to release and, over time, flattens the gasket. A valve with a hydrophobic membrane lets the differential bleed off while keeping the ingress protection class intact, and the temperature-control practice used in cold chain food cases is a useful companion reference.
Heavy-Part Support, Stacking and Post-Wash Drying
Component weights vary enormously. A blade set may weigh one or two kilograms, while a vacuum stuffer pump group with its hopper can exceed eighty. Structural design has to cover the heaviest configuration. For heavy builds, reinforce the base with ribs and put load-bearing feet at the four corners, keep wall thickness at 6 mm or more, and where necessary add a PP or aluminium pallet inside so weight passes directly into the base rather than through the liner.
| Configuration | Typical payload | Shell structure | Liner form | Stacking guidance |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Light (blades, clamps) | 2 to 10 kg | Wall 3 to 4 mm | Routed food-grade EVA | 3 to 4 layers |
| Medium (nozzles, portioning) | 10 to 30 kg | Wall 4 to 6 mm, ribbed sides | EVA and IXPE composite | 2 to 3 layers |
| Heavy (pump group, auger) | 40 to 80 kg | Wall 6 to 8 mm, reinforced corners | PP pallet with EVA location | 2 layers |
Stacking affects foam as much as the shell. Food-grade EVA creeps under sustained load, especially in a hot summer warehouse, and once the liner thins a heavy part shifts into contact with the case wall. Heavy builds should pass load through a rigid pallet and use foam only for location and cushioning.
Drying after washing belongs in the same design conversation. A stainless part that goes back into the case wet corrodes and loads the foam with water. Provide a removable drip rack so washed parts drain before packing, open the base drain plug and use compressed air to complete the dry; a case that cannot be dried quickly will be packed wet eventually.
Microbial Risk and Removable Washable Liners
Meat processing operates under explicit microbiological controls, and cross-contamination between raw and cooked zones or between product lines is a routine audit focus. A case with complex internal geometry and crevices that cannot be washed becomes a reservoir. After repeated open-and-remove cycles, blood water and meat particles left inside create a warm, damp substrate for microbial growth.
The answer is a liner that can be removed as a whole, has no dead corners and can be disinfected. Build the liner from several removable blocks that lift out and lie flat for washing. Avoid blind holes and radius the base of every pocket. Specify materials that tolerate washing above 80 degrees Celsius. Keep the shell interior smooth with no laminated layers. Dry the liner in air after washing and never reload stainless parts into a damp liner.
Parts of different hygiene status should travel in separate cases. Knives and plates from the raw zone should not share a case with filling nozzles and portioning units from the cooked zone. Use colour to distinguish them, for example blue for raw and white or green for cooked, and mark the zone in large characters on the lid, because colour coding survives a busy shift better than a written note. Where the site demands more, use different coloured liner blocks within one case, provided no open crevice connects the zones.
Bring case management into the hygiene procedure: clear debris after every opening, deep clean the liner weekly and inspect gaskets monthly. These actions cost far less than dealing with a contamination event after the fact.
Unpacking Acceptance and Hygiene Check List
Acceptance on arrival should run through four layers, exterior, dimensions, hygiene and function, and each layer needs a criterion that can be decided rather than sensed.
On the exterior, confirm no cracking or distortion, no compression mark or tear in the gasket, working latches and hinges, and clear pressure valve and drain plug. On dimensions, use a feeler gauge and surface plate to confirm blade-to-plate clearance has returned to the 0.05 to 0.15 mm band, a straight edge to confirm auger shaft straightness within 0.1 mm, and an internal micrometer to sample nozzle bores within 0.02 mm of drawing.
On hygiene, check the liner for mould, odour or residue, confirm there are no paper labels or debris acting as foreign bodies, and verify that seals carry a legible material marking with no hardening or cracking. On function, run the vacuum pump unloaded and listen for abnormal noise, confirm ultimate vacuum reaches the nameplate value, verify portioning deviation is inside the declared band, and check that all proximity switches and load cells output correctly once the transport locks are released.
If the liner has absorbed water or shows mould, take it out of service immediately and clean and dry the case thoroughly. If a seal has hardened or taken a permanent set, replace it even if it looks intact, because a deformed seal leaks readily under vacuum or high-pressure washdown. Keep the acceptance record with the packing list and material declaration.
Custom Liners, Tooling and Compliance Documentation
Meat processing equipment is highly fragmented by brand and model. Blade diameters, plate hole patterns, clamp pipe sizes and nozzle bores have no common standard, so a standard liner is almost never usable and custom work is the norm.
The usual sequence has five steps: supply the parts list with drawings or physical samples; agree the pocket layout, materials and cleaning method; produce the first-article liner and a sample case; trial-load and run drop, stacking and wash validation; and release to volume production with a material declaration. At the first-article stage, also validate the wash-and-reload loop, because how easily the liner comes out and goes back, and how completely the case drains and dries, affects daily use more than the cushioning figures do.
As the manufacturer, JUNZHIJIA supplies moulded shells, routed and vacuum-formed food-grade liners, removable block designs, zone colour coding, wash-resistant nameplates and compliance documentation, with OEM and ODM support and multilingual delivery. The shipped document set normally covers the packing list, pocket layout drawing, liner material declaration and migration test report index, a cleaning and drying work instruction, and a summary of compliance references for the destination market, so the equipment owner can cite them directly in a hygiene audit.
Where components come from poultry cutting equipment, the compartment and cleaning approach used for poultry processing transfers directly; for a complete prepared-food line, the shell and conveyor chapters apply.
Frequently Asked Questions FAQ
Q: Our grinder blade edges came back chipped. Is that a packaging problem?
A: In the great majority of cases it is a packaging design problem rather than a material problem. Grinder blades are normally vacuum heat treated, which leaves them hard and relatively low in toughness, so an impact chips the edge instead of rolling it, and a chipped edge is treated as a fragile failure rather than a dressing job. Three mistakes account for most damage: blades and plates packed together, so that foam compresses under stacking load and the two surfaces meet; several blades threaded onto the centre shaft so they strike each other; and blades lying flat on the case floor with the edge taking load from both above and below. The correct arrangement suspends the edge at an upward angle, carries the load on the blade back and centre bore, leaves at least 3 mm beneath the edge, and gives the plate its own shallow pocket with the working face down. Never stack blades and plates, even with a foam sheet between them.
Q: What does a bent auger cause, and how is it prevented in transit?
A: The clearance between the auger flight and the barrel bore is typically only 0.5 to 1 mm, and that gap sets conveying efficiency and product retention. Once the auger bows, one side of the flight runs against the barrel while the other side opens a wide gap, producing unstable feed, product flowing back and a barrel that is difficult to clean. The serious consequence is that the bowed section rubs the barrel in service and generates metal particles, a direct food safety hazard that can trigger a recall. Prevention uses a continuous axial cradle with location at both ends: cut a semicircular channel parallel to the axis so the auger is supported along its full length rather than at one point, fit stops at both ends to limit axial movement, and let the centre shaft ends sit in separate blind holes so lateral force is taken by the bore wall. Never lean an auger into a case corner, because that concentrates load on a small area and reliably produces a permanent bow.
Q: What must be done to a stuffer vacuum pump before shipping?
A: Three tasks come first. Deal with the lubricant by draining to the minimum level or emptying the sump as the maker specifies, and fit a sealed plug at the oil port, because a pump that is tilted or inverted in transit lets oil pass the discharge valve into the working chamber and will spit oil and take a long time to reach vacuum on restart. Second, fix and signal the orientation: print a bold upward arrow on the outside of the case and include a tilt indicator inside so the receiving team can see whether the pump was inverted before opening the chamber. Third, separate and locate: if pump and motor are separate units, pocket them separately and take the load on the coupling locating face rather than on the exposed shaft, and fit a liner plate of matching material on each side of a water ring impeller so stacking load passes through the plates. Support the pump at four points and keep it level so the rotor cannot crush the vanes.
Q: How should sanitary clamp fittings and their seals be stored in the case?
A: A single relocation can involve dozens to hundreds of clamps, and being numerous, varied and small they are a prime target for loss and mixing, so indexed pockets are essential. Assign a large pocket to each pipe diameter, for example 1 inch, 1.5 inch, 2 inch and 3 inch, then split each pocket into three layers for clamp body, pin and bolt, and seal, with soft dividers between them. Label every pocket with size and quantity and fix a matching list inside the lid. Store seals in a lidded box or their own pocket, away from oil and heat, and never compress them for long periods; the pocket should be slightly deeper than the free height of the seal so it travels essentially unloaded. Run each clamp nut to the end of its pin in a half-locked position before packing, so it neither separates in transit nor pre-loads the seal, and apply a thin film of food-grade grease to the threads to prevent corrosion seizing.
Q: Why do stainless steel components develop rust spots during shipping?
A: Chloride ions drive corrosion in a meat plant. Sodium hypochlorite and chlorinated alkaline detergents used in washdown destroy the passive film when residue remains, and together with residual stress they cause pitting and eventually stress corrosion cracking. Shipping is often where the process starts: a removed part still carries blood water, salt and detergent, and if it is boxed in a closed humid space, several weeks at sea are enough to produce rust at contact faces, threads and weld toes. The correct order is neutralise and wash, dry completely, then pack. Rinse off residue, brush with a neutral or mildly alkaline detergent, rinse with deionised or softened water to cut chloride carry-over, blow out recesses with compressed air, and dry at 60 to 80 degrees Celsius where necessary, allowing the part to cool before packing. Parts of different grades should also be separated, because contact corrosion occurs when 304 and 316L travel together, and any part that has been polished should be protected from abrasive contact that removes the passive layer.
Q: Which liner material satisfies both cushioning and food-contact requirements?
A: Cushioning and food-contact compliance pull in different directions, so a layered build works better than any single material. Use EPE on the outside for bulk energy absorption, food-grade EVA routed in the middle for pockets matched to the component outline, and a food-grade IXPE or silicone pad wherever a part touches the liner directly, giving soft contact together with wash resistance. Everything in direct contact should withstand cleaning above 80 degrees Celsius without distortion and should not absorb grease or protein. On compliance, obtain a material declaration and a migration test report referencing the GB 4806 series, EU 10/2011 or the relevant FDA sections, rather than relying on the words food grade; the declaration should name the polymer grade and the additives used, because two liners advertised as food grade can differ substantially in migration behaviour and heat tolerance. Build the liner as removable blocks with no blind holes and no crevices, so it can be lifted out and washed deeply, dried in air and refitted without trapping water in a core that would later support microbial growth.
Q: The case has to enter the wash bay. What protection class should be specified?
A: It depends on whether the case itself is sprayed with high-pressure hot water along with the machine, and a transport rating cannot simply be reused. If the case is used only for transport and storage, IP65 to IP67 is usually enough. If it enters the wash bay and takes hot high-pressure water from several angles at close range, it should be selected towards IP69K capability, because that test uses water near 80 degrees Celsius under high pressure, which is a different logic from the short immersion behind IP67, and the difference in scope between the two ratings is worth reviewing separately. Beyond the ingress class, confirm that gasket and latch materials tolerate the actual wash temperature, radius the internal corners so nothing can hide, make latches and hinges removable from outside for separate cleaning, and keep paper labels out; use polyester or metal nameplates that survive repeated washing, because a peeled paper label becomes a foreign body in a food area and can halt a production batch. Also confirm the case can drain, because a wash-rated shell with no base drain plug holds water under the liner.
Q: What information is needed to specify a custom meat processing parts case, and what documents ship with it?
A: Provide the parts list with names, quantities, materials and individual weights; key dimensions with drawings or physical samples; the position and tolerance of precision features such as cutting edges and polished faces; the cleaning and disinfection regime including detergent type, temperature and whether chlorine is used; the hygiene zone of use, raw or cooked; and the transport and storage temperature range. For export, state the destination market food-contact basis and the label language. The usual sequence is parts list review and pocket layout, first-article liner and sample case, trial loading with drop, stacking and wash validation, then volume production. The shipped documents normally include the packing list, pocket layout drawing, liner material declaration and migration test report index, a cleaning and drying work instruction, and and a compliance reference summary for the destination market.
Conclusion and Related Reading
Meat processing cases succeed when impact, corrosion and hygiene are solved together: edges suspended, augers supported along their length, pumps level with oil lowered, liners removable for washing. JUNZHIJIA builds food-grade liners, tooling and compliance documents to order, with OEM and ODM support.
Related Reading