

Start with the conclusion: evaluating a protective case supplier cannot rest on the impression left by one quotation or one factory tour. It needs a scoring system that is repeatable, cumulative and comparable. Use five weighted dimensions, namely quality capability at 35 percent, delivery performance at 25 percent, technical and engineering capability at 20 percent, cost and commercial terms at 15 percent, and systems and service at 5 percent. Break each dimension into three to five quantifiable score items, and score them against three evidence streams: factory audit records, pilot batch data and incoming inspection logs. Rank suppliers by total score for admission and exit, update the ranking on a fixed cycle, and supplier management shifts from relationship judgment to data judgment.
A protective case is the archetype of a functional enclosure. Its quality differences barely show on the surface; they live in sealing, strength, weather resistance and service life, all of which need time and the right conditions to reveal themselves. That means one factory visit, one sample and one quotation carry far too little information to judge a supplier. Many procurement failures begin with a beautiful sample and a favorable price in the first three months, and only surface in the second rainy season, when the gasket material has been downgraded and the latch wall has been thinned.
This guide is written for B2B buyers, supply chain managers and quality engineers. It sets out a supplier scoring system for protective cases that can be implemented directly: how to split the dimensions, how to set the weights, how to quantify the score items, where the data comes from, how to design the tiers and the exit mechanism, and how to develop a mid-tier supplier into a better one. The standards and figures used are common practice or typical values; the formal policy should be tuned to your own purchasing scale, product criticality and risk appetite.
Table of Contents
- Start With the Conclusion: Five Dimensions and Suggested Weights
- Why "Cheapest" Is Not an Evaluation Criterion
- Dimension One: Quality Capability (35%)
- Dimension Two: Delivery Performance (25%)
- Dimension Three: Technical and Engineering Capability (20%)
- Dimension Four: Cost and Commercial Terms (15%)
- Dimension Five: Systems and Service (5%)
- The Scoring Model: Weighting and the Scorecard
- Where the Data Comes From: Audits, Pilot Batches and Inspection Logs
- Supplier Tiers, Admission and Exit
- Supplier Development: Bringing a Mid-Tier Supplier Up
- Frequently Asked Questions
- Conclusion and Related Reading
Start With the Conclusion: Five Dimensions and Suggested Weights
Here is the structure first. A workable supplier scoring system for protective cases should consist of five dimensions, each carrying several score items, each item with a clear scoring rule and a defined data source.
| Dimension | Suggested weight | Core question | Main data source |
|---|---|---|---|
| --- | --- | --- | --- |
| Quality capability | 35% | Can delivered batches meet specification consistently | Incoming inspection log, pilot batch validation, test reports |
| Delivery performance | 25% | Can it deliver on time, in quantity, in the agreed packaging | Order fulfillment records, delay statistics |
| Technical and engineering | 20% | Can it solve customization and engineering problems | Prototyping response, structural advice, drawing capability |
| Cost and commercial terms | 15% | Is total cost reasonable and predictable | Quotation structure, payment terms, change costs |
| Systems and service | 5% | Do systems and management support a long partnership | ISO 9001 certificate, spare parts supply, responsiveness |
The weights are not fixed. For military-spec, energized-equipment or export projects, raise the quality weight. For schedule-critical projects such as engineering fit-out, raise the delivery weight. For heavily customized projects, raise the technical weight. The point of weighting is to convert the vague question of what we care about most into a set of rules fixed in advance and open to explanation.
Note that the weighted total is a ranking tool, not the decision itself. If any dimension reveals a disqualifying issue, such as an inflated protection rating, a falsified material grade or a refusal to provide test documents, the supplier should be removed from the approved list regardless of total score. The policy must state this explicitly.
Why "Cheapest" Is Not an Evaluation Criterion
This is the first thing worth making clear. A low price is not a virtue; the fit between price and specification is.
The reason is that the cost structure of a protective case is highly adjustable. Two cases that look identical can differ sharply in cost through four levers: replacing a weather-resistant resin grade with a commodity grade or recycled content; reducing the main wall thickness from 3.0 mm to 2.4 mm and deleting the bottom grid ribs; replacing a silicone gasket with a reclaimed rubber strip; and swapping a high-density foam insert for low-density sponge. None of these changes is visible on a finished case, yet together they cut the real service life and protective capability of the case dramatically. For a detailed breakdown of where cost sits, see breaking down the cost structure of a protective case.
The correct sequence is therefore to lock the specification first and compare prices second. Write the material grade, wall thickness range, gasket material and hardness, protection rating, insert density and inspection sampling method into the request for quotation, and require every supplier to quote against the same specification. Only then are the quotations comparable. Otherwise you are comparing the prices of different products, and the conclusion is meaningless.
This is also why a scoring system must include specification consistency as a score item. If a supplier cannot state a definite material grade and structural parameter at the quotation stage, that should cost points in the quality dimension, not earn points in the cost dimension.
Dimension One: Quality Capability (35%)
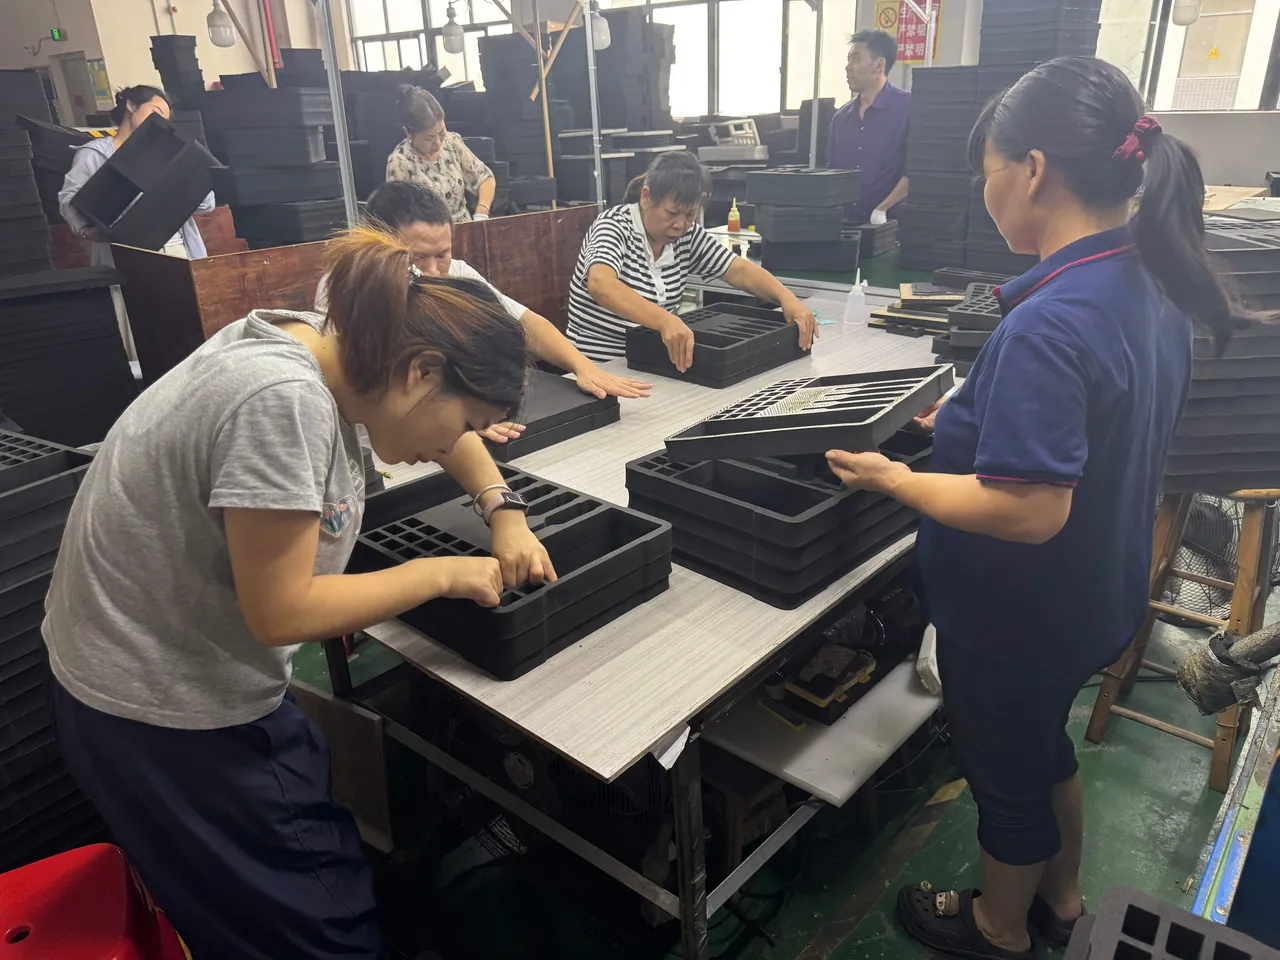
Quality carries the highest weight because the cost of failure is highest: one leaking case can destroy equipment worth several times its price. Split quality into five score items.
Item one: incoming and in-process control. Assess whether the supplier has defined incoming inspection rules, in-process patrol records and first-article confirmation on critical dimensions. The evidence is the inspection procedure plus sample records. A supplier with three consecutive months of traceable records is in a different class from one that can only produce a document describing an inspection system.
Item two: outgoing inspection and batch traceability. Assess whether batches are inspected against a sampling standard, how nonconforming batches are handled, and whether a batch can be traced back to its material lot and production crew. Sampling can follow the inspection level and AQL logic of GB/T 2828.1 or ISO 2859-1. For inbound inspection practice, see how to sample an incoming batch inspection for protective cases.
Item three: verification of critical performance. Assess whether the supplier can provide verification for protection rating, drop, stacking and sealing, and whether the report sample matches the model actually supplied. For how to verify a rating, see how to verify that an IP67 certificate is genuine.
Item four: first pass yield (FPY) at incoming inspection. This is the single most revealing quantitative indicator, and the data must come from the buyer's own inspection log rather than supplier self-reporting. Track batch pass rate and unit defect rate over the last six to twelve months.
Item five: quality incidents and corrective action. Assess the number and severity of historical incidents, plus the speed and effectiveness of corrective action. A supplier that has had an incident but corrected it thoroughly and passed re-validation is often more reliable than one that claims no incidents but refuses to share data.
| Score item | Suggested points | Scoring rule (example) | Data source |
|---|---|---|---|
| --- | --- | --- | --- |
| Incoming and in-process control | 20 | Full marks for procedure plus continuous records; half for documents only | Audit, record samples |
| Outgoing inspection and traceability | 20 | Sampling rule plus batch traceable to material | Inspection records, sealed samples |
| Critical performance verification | 25 | Full marks when reports map to models one-to-one | Test reports |
| First pass yield at incoming | 25 | Full at 99 percent or above; half at 95 to 99; low below 95 | Buyer inspection log |
| Quality incidents and corrective action | 10 | No major incident, or a closed corrective loop | Quality file |
Dimension Two: Delivery Performance (25%)
Delivery is the second most important dimension because it directly sets the buyer's schedule. Protective cases are often a fit-out item; if the cases do not arrive, the equipment cannot ship and the program slips.
Item one: on-time delivery (OTD). Define it as the share of order lines delivered by the agreed date or window. Track the last six to twelve months. A stable supplier should hold a high level; one that repeatedly falls short should lose points even if quality is good.
Item two: quantity accuracy. Look for short shipments, over shipments and mixed models. Short shipments break production plans, over shipments tie up inventory and cash, and mixed models impose extra manual sorting at receiving.
Item three: reliability of the committed lead time. This is not about the shortest lead time but about whether the committed date is met. A supplier that quotes 45 days and delivers in 45 usually beats one that quotes 20 and slips to 40. Compare committed against actual.
Item four: capacity and flexibility. Assess whether the supplier can scale up during a demand spike and whether a demand reduction will affect quality. This matters especially for seasonal programs.
Item five: packaging and marking compliance. Assess whether the actual packaging matches the agreed specification, including corner guards, cushioning, pallets, stack layer markings and packing documents. This item is often skipped even though it directly determines the arrival damage rate. For the underlying requirements, see how cross-border logistics works for protective cases.
Dimension Three: Technical and Engineering Capability (20%)
Technical capability decides whether a supplier can solve problems with you, and it matters most on customized projects.
Item one: prototyping response and accuracy. The time from requirement confirmation to sample delivery, and the share of samples that pass first time. Prototyping is the cheapest validation window and the clearest view of engineering capability.
Item two: structural and material advice. A supplier with real engineering depth will volunteer recommendations on sealing groove design, wall thickness, rib layout and latch selection rather than passively machining to a drawing. For the criteria behind structural design, see how the shell structure of a high-strength protective case is built.
Item three: drawings and documentation. Whether the supplier can provide proper product drawings, bills of material, material declarations and process descriptions. This directly affects later spare parts purchasing and second-source development.
Item four: mold and process understanding. Whether the supplier can hold a professional discussion about gate location, sink mark control, weld line position, draft angle and cooling of thick sections. This item separates a factory from a trading company.
Item five: track record on custom projects. Whether comparable projects have been delivered successfully and verifiable references can be provided, without disclosing customer confidentiality.
Dimension Four: Cost and Commercial Terms (15%)
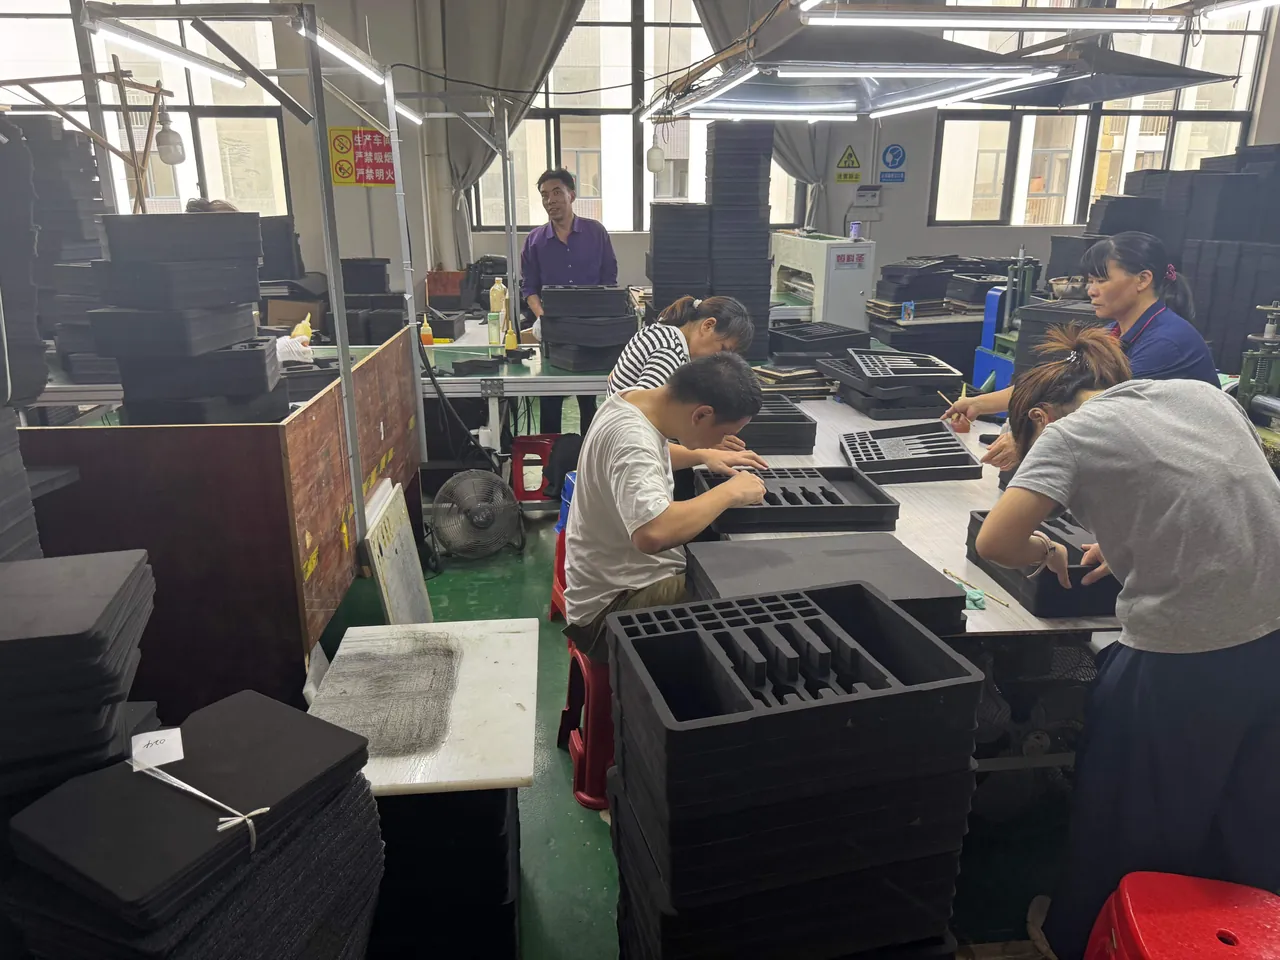
The cost dimension is not about who is cheapest but about whether total cost is reasonable and predictable.
Item one: transparency of the quotation structure. Whether the quote breaks down into material, processing, tooling amortization, insert, packaging and freight. Only a structured quotation makes later cost reduction discussions possible; a single lump sum leaves nothing to work with.
Item two: total cost of ownership (TCO). The hidden costs beyond unit price, including rework and returns from incoming defects, transport damage from inadequate packaging, and downtime risk from unstable spare parts supply. A cheap supplier with a high defect rate often has a higher TCO than a mid-priced one.
Item three: commercial terms. Payment terms, payment method, minimum order quantity, and tool ownership and amortization. Tool ownership especially must be settled in the contract, or changing suppliers later becomes very difficult. For contract essentials, see intellectual property and tooling clauses in custom protective case contracts.
Item four: price stability. When raw material prices move, does the supplier adjust unilaterally or negotiate in advance, and is the adjustment evidenced. A stable adjustment mechanism is itself part of predictability.
Item five: cost of change. Whether quotes for mold, material and packaging changes are reasonable and transparent.
| Dimension | Key score items | Suggested weight | Data source |
|---|---|---|---|
| --- | --- | --- | --- |
| Quality capability | Incoming and in-process control, outgoing inspection and traceability, critical performance verification, first pass yield, incident corrective action | 35% | Inspection logs, test reports, audit |
| Delivery performance | On-time delivery, quantity accuracy, lead time reliability, capacity flexibility, packaging compliance | 25% | Order fulfillment records, receiving records |
| Technical and engineering | Prototyping response, structural and material advice, drawings and documents, mold and process understanding, custom track record | 20% | Prototyping records, technical discussions, documents |
| Cost and commercial | Quotation transparency, TCO, commercial terms, price stability, change costs | 15% | Quotations, contracts, price history |
| Systems and service | ISO 9001 and similar, spare parts supply, responsiveness, cooperation | 5% | Certificates, spare parts records, service log |
Dimension Five: Systems and Service (5%)
The systems dimension carries a low weight but has threshold characteristics. It will not add many points, but its absence can cost points or become a disqualifier.
Item one: quality management system. Whether the supplier holds ISO 9001 or equivalent certification, and whether the scope covers the products supplied. Note that a certificate is a threshold, not a guarantee. What matters is whether the records behind it reconcile with the product, which is the same verification logic used in the quality dimension.
Item two: spare parts and after-sales. Whether consumables such as gaskets, latches, hinges and handles can be bought separately, how long supply is committed, and whether the part-to-model mapping is clear. For practical guidance, see how many years a protective case typically lasts.
Item three: responsiveness. Average response time for quotations, technical clarification and complaint handling. This item is the easiest to assess and the quickest to expose problems.
Item four: communication and cooperation. Whether there is a stable point of contact, whether changes and risks are communicated proactively, and whether the supplier accepts audits and improvement suggestions.
The Scoring Model: Weighting and the Scorecard
Combining the five dimensions yields a workable scorecard. Use a 100-point scale per dimension and weight the result. To avoid the trap of a supplier scoring mid-range everywhere and looking acceptable overall, set minimum thresholds on critical items, so that a dimension fails if any critical item falls below its threshold.
| Dimension | Weight | Score (0-100) | Weighted score | Critical item threshold |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Quality capability | 35% | To be filled | Score x 0.35 | First pass yield at incoming at least 95% |
| Delivery performance | 25% | To be filled | Score x 0.25 | On-time delivery at least 90% |
| Technical and engineering | 20% | To be filled | Score x 0.20 | First-time prototype pass rate at least 70% |
| Cost and commercial | 15% | To be filled | Score x 0.15 | Quotation structure can be itemized |
| Systems and service | 5% | To be filled | Score x 0.05 | Valid system certificate held |
| Total | 100% | Not applicable | Weighted total | Not applicable |
The value of the scorecard is that it is explainable. When procurement chooses supplier B over a cheaper supplier A, the card shows why: A leads by 8 points on price but trails by a combined 22 points on first pass yield and on-time delivery. That explainability is the precondition for the system surviving long term.
Two practical points. Define the review cycle and the unit of assessment. A quarterly light review covering delivery and incoming quality, and an annual full review covering technical and systems dimensions, works well. Assess the supplier plus product line combination, because the same supplier can perform very differently across different lines.
Where the Data Comes From: Audits, Pilot Batches and Inspection Logs
Whether the system holds up depends on whether the data is obtainable and verifiable. There are four main sources.
First, audit records. These cover incoming control, in-process control, equipment and personnel, and shop floor management. Audit by watching actions rather than reading documents: check whether the incoming quarantine area is actually in use, whether inspection records are filled in continuously, whether equipment is within its maintenance cycle, and whether nonconforming goods are segregated. An audit is there to exclude the clearly unacceptable, not to produce a precise score.
Second, pilot batch data. This assesses production consistency. A pilot batch is not a sample. It must be produced on the real mold, the real line and the real takt time, and delivered in the agreed quantity. Validate dimensions, sealing, structure, environment and life. For sampling methods, see how to use AQL sampling for custom protective case acceptance.
Third, incoming inspection logs. This is the most valuable source, because the data is generated by the buyer and cannot be polished by the supplier. The log should record batch, quantity, sample size, defect count and defect type, aggregated monthly into pass rate and defect distribution.
Fourth, order fulfillment and complaint records. These assess delivery and responsiveness, including committed date, actual date, reason for delay, complaint count and handling time.
Together the four sources form a supplier profile. That profile should be updated continuously and pulled fresh before every major purchasing decision, rather than being reconstructed from memory or relationship impressions.
Supplier Tiers, Admission and Exit
Scores need handling rules, or they are decorative. A four-tier classification works well.
| Tier | Weighted total (example) | Management approach | Share of purchases |
|---|---|---|---|
| --- | --- | --- | --- |
| A, preferred | 90 or above | Priority orders, joint development, reduced inspection frequency | Main share |
| B, qualified | 80 to 89 | Normal orders, standard inspection | Regular share |
| C, watch | 70 to 79 | Limited orders, tightened inspection, deadline for corrective action | Small trial share |
| D, exit | Below 70, or a disqualifying event | Stop new orders, phase out, start replacement | Phased withdrawal |
Admission should state three things: the minimum entry score, the mandatory qualifications and documents such as system certificates, test reports and material declarations, and the pass criteria for pilot batch validation. A supplier that has not passed pilot validation should not enter volume supply.
Exit must be written down as well. Three common triggers apply. First, the score falls into the D tier for two consecutive review cycles. Second, a disqualifying event occurs, such as an inflated protection rating, substituted materials or a refusal to provide test documents. Third, a systemic problem persists without improvement, such as the same critical defect appearing in three consecutive batches. The value of an exit mechanism is that it makes removal defensible, so that "inconvenient to change" does not become "never change."
A multi-source strategy is the natural partner of a scoring system. Keep at least two approved suppliers for critical materials, with clear primary and secondary roles. This reduces supply interruption risk and gives the scoring system a real comparison baseline. Only when a substitute exists does the assessment carry real weight.
Supplier Development: Bringing a Mid-Tier Supplier Up
The purpose of evaluation is improvement, not elimination. For a C-tier supplier, use a three-step method of issue list, deadline and re-validation.
Step one is to issue a specific list. The list must tie to score items and evidence, avoiding vague statements such as "quality is poor." Instead of "the gaskets are bad," write "two of the last three batches had gaskets whose compression set missed specification, with measured values deviating from the datasheet requirement."
Step two is to agree a corrective plan. Assign owners and deadlines to each measure, and define how effectiveness will be verified. Effective corrective actions commonly include switching to a specified resin grade with datasheets attached, adding an outgoing sealing test, improving packaging protection, and introducing batch traceability marking.
Step three is re-validation and restoration. After corrective action, validate through tightened inspection on three consecutive batches; restore normal share if effective, downgrade if not. The process is itself a test of supplier engineering capability. A supplier willing and able to complete the loop usually deserves a long-term relationship.
For A-tier suppliers, the management focus shifts from control to collaboration: joint development of new structures, shared cost optimization, earlier demand forecasts, and long-term agreements covering spare parts supply and technical support. A strong supplier relationship is not squeezed out by price pressure but grown through stable orders and transparent rules.
JUNZHJIA, manufactured by KeXin New Materials (Guangdong) Co., Ltd., serves wholesale, distribution, OEM/ODM and global supply. Within an ISO 9001 framework, JUNZHJIA provides product drawings, material declarations, inspection records and process documents where required, supports factory audits and pilot batch validation, and supplies consumable spares by case model, so that buyers can map the quality, delivery and after-sales items of their scoring system onto verifiable evidence.
Frequently Asked Questions
Q: How should the weights be allocated when evaluating a protective case supplier? A: There is no universal set of weights, but there are universal principles. For projects with demanding protection ratings and costly failure, such as military-spec, energized-equipment or long-term outdoor exposure, quality should take 35 to 40 percent. For engineering fit-out and schedule-critical projects, raise delivery to 25 to 30 percent. For heavily customized projects, raise technical and engineering capability to 20 to 25 percent. For standardized, repeat-purchase categories, cost can be raised. A workable starting point is quality 35 percent, delivery 25 percent, technical 20 percent, cost 15 percent and systems and service 5 percent. What really matters is fixing the weights in advance and making them public, so suppliers know what is expected and internal decisions are explainable. Weights should stay stable for a period, typically a year, before revision; changing them often destroys the constraint they provide.
Q: How do you score a new supplier that has no history? A: Use admission assessment instead of performance assessment for new suppliers. Look at three things. First, qualifications and documents, including system certificates, test reports, material declarations and drawing capability. Second, capability verification through a factory audit of incoming control, in-process control and equipment, focusing on what happens on the floor rather than what is written in the manual. Third, pilot batch validation on real molds and lines in the agreed quantity, with validation of dimensions, sealing, structure, environment and life. Once the pilot passes, admit the supplier with a small allocation, and bring it into regular performance scoring after three or more batches of incoming inspection data. Note that an initial score means only that the supplier passed admission; it should not earn a main share, because admission assessment carries much less information than sustained performance data.
Q: How should first pass yield at incoming inspection be measured to stay objective? A: Define three things. First, the counting basis: whether you count by batch or by unit. The two mean different things, so keep both, since batch pass rate reflects consistency between batches while unit defect rate reflects consistency within a batch. Second, the defect criteria: agree in advance the specific rules for critical, major and minor defects, for example insufficient wall thickness or seal failure as critical and sink marks or color variation as minor, so that inspector subjectivity does not drift the data. Third, the data source: use the buyer's own incoming inspection log rather than supplier self-reported figures, with sampling following the agreed inspection level. Track a rolling six to twelve months and retain the defect type distribution, because the distribution often explains more about the supplier's problem than the pass rate alone.
Q: How can you tell a real factory from a trading company? A: Cross-check five angles. First, process communication: a real factory will discuss mold structure, gate location, sink mark control, draft angle and sealing groove design, while a trading company usually relays messages. Second, willingness to accept a factory audit and provide production floor documentation. Third, material sourcing and property data, since a factory can usually engage material suppliers directly and provide grade data. Fourth, how prototyping problems are answered: a factory proposes structural improvements, while a trading company more often suggests making a new sample. Fifth, spare parts capability: a factory can keep supplying gaskets and parts for older models, which a trading company finds hard to do. Note that trading companies are not automatically excluded; their value lies in integration and small-batch responsiveness, but their margin and information gap amplify quality risk, so validation intensity and contractual constraints should be increased accordingly.
Q: Does multi-sourcing increase cost, and is it worth it? A: In the short term it adds some cost; in the long term it usually pays. The direct costs include two sets of admission validation, two sets of samples and pilot batches, and a slightly higher unit price from split volumes. The benefits are usually larger. First, it reduces supply interruption risk, since a single-source supplier that stops production, relocates or suffers a quality incident can halt an entire program. Second, it creates a real price and technical benchmark, because without a substitute the scoring system has little bite. Third, it encourages continuous improvement, since share can be switched. The practical structure is primary plus secondary: the primary supplier takes most of the volume while the secondary keeps a small ongoing allocation to stay capable and willing. Both are managed within the same scoring system.
Q: How long should the evaluation cycle be? A: Use a dual cycle of quarterly light review and annual full review. The quarterly review covers only the data dimensions that can be collected automatically, mainly incoming quality such as first pass yield and defect distribution, and delivery performance such as on-time delivery and quantity accuracy, because this data comes from the buyer's own logs at low cost and updates quickly, allowing early detection of anomalies. The annual full review covers all five dimensions, including the technical, engineering and systems items that require dedicated effort, plus a complete audit or re-assessment. Trigger an immediate review on three special events: a major quality incident or disqualifying event; a major supplier change such as relocation, a change of key material supplier or a change of ownership; and a major change on the buyer side, such as a new requirement for a higher protection rating. Immediate reviews prevent problems from lying dormant between scheduled assessments.
Q: When should you start replacing a supplier that will not improve? A: Set three explicit triggers. First, the data trigger: two consecutive review cycles below the qualified tier with a critical item such as first pass yield or on-time delivery falling below its threshold. Second, the event trigger: a disqualifying event such as an inflated protection rating, substituted materials, a refusal to provide test documents, or a safety or compliance problem. Third, the cooperation trigger: no substantive corrective action within the agreed period after an issue list was issued, or a failed re-validation after corrective action. Any one of the three justifies starting replacement sourcing. Be aware that changing suppliers carries costs of its own, including re-admission, pilot validation, tooling transfer and switchover risk, so confirm that the replacement supplier can take on the volume and allow enough switchover time before you begin, to avoid a supply vacuum.
Conclusion and Related Reading
Returning to the question in the title: how do you evaluate a protective case supplier? Replace relationship judgment with data judgment. Set weights across five dimensions, namely quality capability at 35 percent, delivery performance at 25 percent, technical and engineering capability at 20 percent, cost and commercial terms at 15 percent, and systems and service at 5 percent. Break each dimension into quantifiable items, score them against three evidence streams of audit records, pilot batch data and incoming inspection logs, and then use the total to drive admission, exit and improvement.
Three actions you can take immediately. First, lock the specification before comparing prices, so that every supplier quotes against the same document; otherwise the price comparison means nothing. Second, build an incoming inspection log and keep it running for at least six months, the one irreplaceable data foundation for any scoring system. Third, write the weights, thresholds, tiers and exit rules into your procurement policy and publish them, so suppliers know what is expected and internal decisions are explainable and traceable.
JUNZHJIA, manufactured by KeXin New Materials (Guangdong) Co., Ltd., covers protective cases, tool cases, military-spec storage cases and waterproof junction boxes, serving wholesale, distribution, OEM/ODM and global supply. Operating within an ISO 9001 framework, the company provides product drawings, material declarations, inspection records and process documents, supports factory audits and pilot batch validation, and supplies consumable spares by case model, so that buyers can fold quality, delivery and after-sales indicators into a single supplier evaluation system.
Related Reading