

The short answer: most protective case procurement failures do not happen because a supplier is dishonest. They happen because the buyer handed the basis of judgement to photographs and verbal promises. The only reliable way to avoid the pitfalls is to replace opinion with evidence — resin grade stated in writing, ingress protection tied to a named standard and a test report, sealing structure seen in a physical section, and latches and hinges backed by material data and life figures. Bring those ten pieces of evidence to the negotiation and most common quality problems surface before the goods ship. Skip them and a glossy render plus the words "absolutely waterproof" is enough to deliver a batch that leaks the first time it meets a rainy season.
This guide is written for B2B buyers, supply chain managers and quality engineers. It takes the ten quality problems that appear most often in protective case procurement and breaks each one down: what the pitfall looks like in practice, where the supplier saves money by cutting it, and what the buyer can do during sampling or the first production run to catch it. Every figure in the text is a typical or empirical value. The binding basis for acceptance is always the drawing, the signed golden sample, the stated standard revision and the test report agreed by both parties. If you are sourcing a case for an outdoor, military-specification or powered-equipment project, this checklist can be used directly as an on-site audit sheet.
Contents
- The short answer: turn opinion into evidence
- Pitfall one: judging from renders instead of sealing structure and sections
- Pitfall two: vague resin grades and mixed use of PP, ABS and PC
- Pitfall three: wall thickness and reinforcement ribs cut back
- Pitfall four: recycled or thin-wall latches and hinges
- Pitfall five: poor gasket material with high compression set
- Pitfall six: inflated IP ratings with no test report
- Pitfall seven: low-density foam that powders and crumbles
- Pitfall eight: no high or low temperature validation, brittle fracture in cold
- Pitfall nine: missing packaging and transport protection
- Pitfall ten: no after-sales support and no spare parts
- On-site audit sheet for all ten pitfalls
- Clauses that must appear in the purchase contract
- Frequently asked questions
- Conclusion and related reading
The short answer: turn opinion into evidence
Start with the logic. A protective case is a functional enclosure. It does not sell on appearance. It sells on four classes of performance: sealing, strength, weather resistance and service life. Those four share one property. When they are inadequate in the normal state, the eye cannot see it. A case whose gasket cross-section is 0.3 millimetres undersized looks identical on a bench to a fully compliant case. The difference only appears after immersion, after a cold chamber, or after two thousand open-and-close cycles.
So the method for avoiding procurement pitfalls is to convert every part that should not be economised into evidence that can be requested, checked and filed. Evidence comes in five forms: drawing and specification sheet covering resin grade, dimensional tolerance and wall thickness; a physical section or sectioned sample showing the gasket groove and wall thickness; test reports covering IP rating, drop, stacking and material properties; a golden sample fixing the boundary of appearance and feel; and field validation of a pilot batch.
| Evidence type | Pitfall it exposes | When to request | Note |
|---|---|---|---|
| --- | --- | --- | --- |
| Drawing and specification | Vague resin grade, unstated wall thickness, missing tolerances | Quotation stage | Demand a grade, not "engineering plastic" |
| Sectioned sample or section view | Thin walls, fake ribs, poor gasket groove design | Sampling stage | Cutting one case apart beats reading ten drawings |
| Test report | Inflated IP rating, weak material performance | Before first batch | Verify the standard number and sample identity |
| Golden sample | Colour, feel and dimensional disputes | Before first batch | One pass sample and one boundary sample, signed by both parties |
| Pilot batch validation | Life, low temperature and field condition problems | Before mass production | Run a full cycle under real conditions |
Keep one line in mind: the areas a supplier will not let you cut open are usually the areas where money was saved. Nearly all ten pitfalls below map back to a cell in this table.
Pitfall one: judging from renders instead of sealing structure and sections
This is the most common and the most damaging pitfall. A buyer sees a polished 3D render online, reads "waterproof, dustproof, crush resistant, drop resistant", and places an order without ever inspecting the sealing structure at the case rim. When the goods arrive, the rim turns out to be a flat sealing face that relies on the lid's own weight to press shut. There is no designed compression, and no groove to keep the gasket from migrating sideways.
A compliant sealing structure normally has three elements: a gasket groove, a gasket cross-section, and a design that limits and controls compression. The groove stops the gasket from moving laterally. The cross-section, usually a round O-ring or a square or custom profile strip, determines whether a continuous contact band forms under compression. The limiting structure determines how far the gasket is compressed when the lid closes. As an empirical value, solid rubber gaskets are typically designed with 20 to 30 percent compression. Too little and the seal is not continuous. Too much and permanent set accelerates and the case becomes hard to close.
The only reliable action is to request a section drawing or a physically sectioned sample. If a supplier will not even provide a section, the evaluation can be closed. For more on how a standard case rim is designed, see how waterproofing is designed into outdoor cases.
Pitfall two: vague resin grades and mixed use of PP, ABS and PC
The second common pitfall is vague material language. A quotation that says "high strength engineering plastic" sounds professional and says nothing. Engineering plastic is a broad family with performance that can differ by a factor of several. As "plastic cases", copolymer PP, ABS, PC, PC/ABS alloy and glass-filled grades are entirely different products in toughness, weather resistance, low temperature behaviour and cost.
The way to spot this is simple: require the specific grade, the resin maker's name and the property data for that grade. If the answer is only the two letters PP, the supplier is probably using the cheapest general-purpose material available. On appearance, watch for several signs: pronounced sink marks, weld lines near ribs and the gasket groove, uneven colour with a grey or mottled cast typical of regrind, and a dull sound when tapped, which can indicate over-filling or aged material.
For a systematic material comparison see the difference between PP, ABS and PC protective cases and how to choose plastic materials for protective cases. Keep one principle in mind: material is the performance ceiling of the case, and no downstream process can buy back what was saved in the resin.
Pitfall three: wall thickness and reinforcement ribs cut back
The third pitfall hides in walls you cannot see. A protective case gains its resistance to compression, torsion and drop mainly from wall thickness and reinforcement ribs, including the base grid, circumferential ribs and corner blocks. Reducing wall thickness directly saves material cost and cycle time, and is nearly invisible from the outside unless you cut the case open.
As an industry empirical value, the main wall of a mid-sized protective case is typically in the 2.5 to 4.0 millimetre range, depending on material modulus, case size and load requirement. Rib height and spacing matter just as much. Ribs packed too closely cause sink marks. Ribs spaced too far apart do not resist bending. There are three ways to judge. First, measure the section wall thickness with a calliper in front of you rather than trusting a spoken number. Second, do a press test on the wall and the base centre, feeling for clean spring-back rather than a bulging dent. Third, review the rib layout drawing, which a serious supplier will provide.
For more structural detail see how high strength case bodies are structured. If a supplier refuses to measure a section for wall thickness, that refusal is itself the strongest signal.
Pitfall four: recycled or thin-wall latches and hinges
Latches and hinges are the parts most easily cut and most easily broken. They carry the fatigue load of repeated opening and the impact load of a drop. Use recycled material or thin the walls, and the result is predictable: latches loosen after a few hundred cycles, catches crack, and hinge pins wobble or fall out.
There are four things to check. First, material. Latches are commonly PA or POM, and hinge pins are metal or high strength engineering plastic. Require the material to be stated. Second, structure. A good latch has an engagement feel and a secondary lock, avoiding a half-closed state. A hinge should have axial retention to stop the pin from walking out. Third, feel. A new part should have stable and consistent opening force, not an action that is stiff for a dozen cycles and then loose. Fourth, life validation. Require open-and-close life data or run a test. Typical engineering targets specify a life of several thousand cycles.
For latch selection logic see how to select case latches, and for how the three parts interact see how hinges, latches and seals work together. These three parts are one system, and economising on any one of them collapses the protection life of the whole case.
Pitfall five: poor gasket material with high compression set
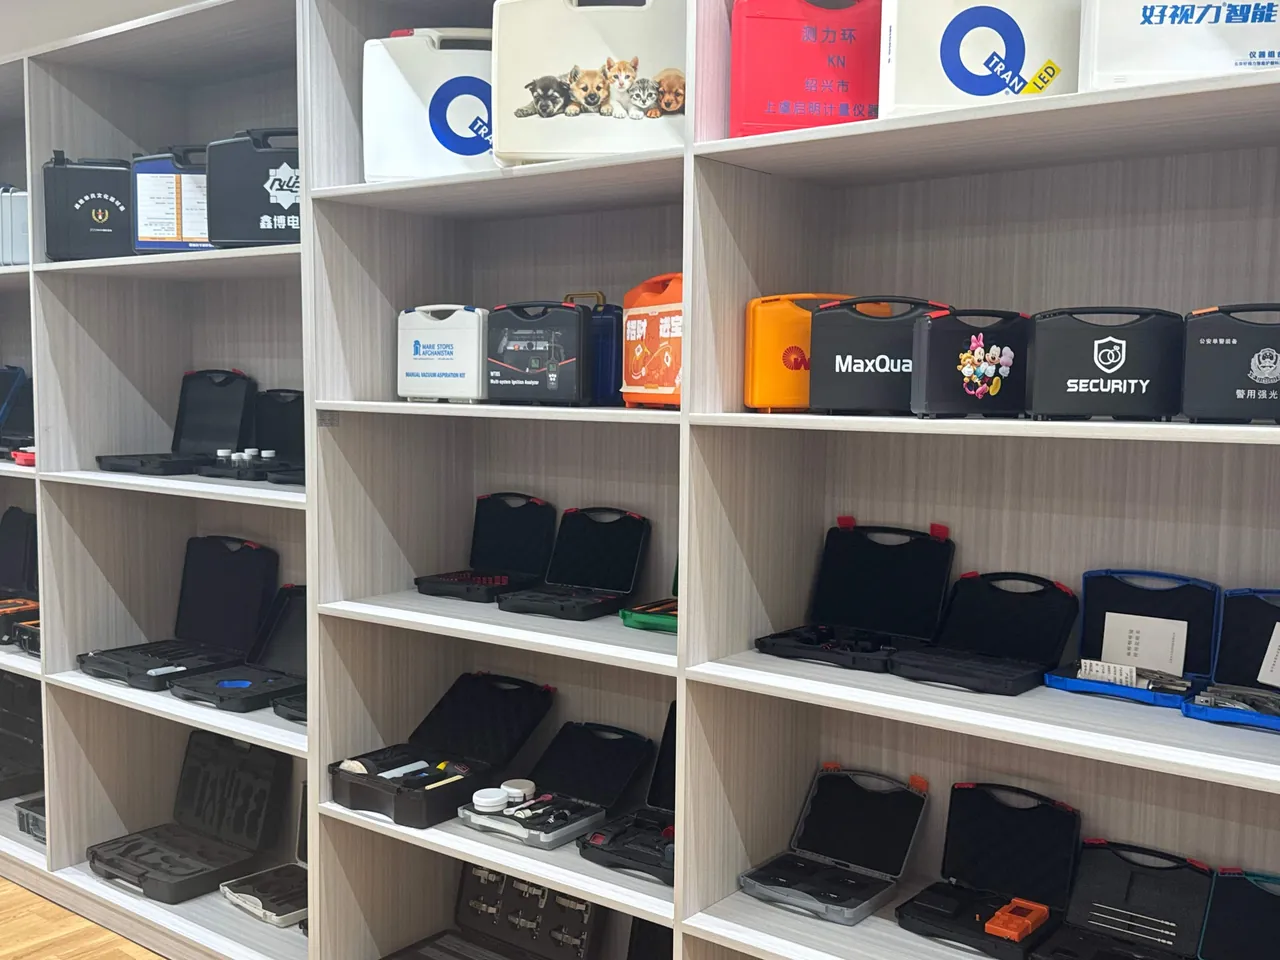
The gasket is the consumable heart of a protective case and the part most often downgraded in procurement. A compliant gasket must satisfy three things at once: weather resistance so it does not harden, low compression set so it recovers after long compression, and suitable hardness, typically in the Shore A 40 to 70 range depending on structure. Low cost suppliers often use reclaimed rubber or low grade compounds. Short term nothing shows. Over six months to a year the material hardens, cracks and loses recovery, and the seal fails.
There are three ways to judge. First, establish the material — common options include silicone VMQ, EPDM, nitrile NBR and neoprene CR, each with different temperature and media strengths. Second, request ageing and compression set data, which may be described against methods such as GB/T 5470 or ASTM D3574. Third, do a tear and rebound test. Poor compound tears with a white edge and recovers slowly.
For deeper material and ageing content see what material protective case gaskets use and how gaskets age and how to tell. Remember one thing: the gasket is the only part of the case that is guaranteed to reach the end of its life first. Saving money here sets a hidden shelf life on the whole case.
Pitfall six: inflated IP ratings with no test report
"IP67 waterproof" is the most repeated claim in protective case marketing and the most frequently inflated. An IP rating must be confirmed inside the framework of IEC 60529 or GB/T 4208 using the specified test methods and acceptance conditions. IP67 means dust protection level 6, fully dust tight, and water protection level 7, short term immersion. IP68 corresponds to more severe continuous immersion, with depth and duration agreed between buyer and supplier.
The action is clear: require a test report that corresponds to the model you are buying, and check the standard number, the sample description, the test conditions and the conclusion. Watch three things. First, does the report sample match your model rather than a "similar product". Second, are the immersion depth and duration stated. Third, are the issuing laboratory and the date traceable. If the only document is a picture of a "waterproof certificate" with no standard to check against, treat it as an inflated rating.
For the difference between rating definitions and acceptance conditions see understanding ratings from IP67 to IP68, and for the test method see how an IP67 immersion test is performed. To put the requirement into a contract, see how waterproofing is designed into outdoor cases.
Pitfall seven: low-density foam that powders and crumbles
The insert is a major part of a protective case's value, yet it is often downgraded as filler. Poor foam shows a characteristic pattern: low density, weak rebound, and after a year or two it begins to powder and shed debris that contaminates the equipment inside. Flocked surfaces may delaminate and peel after repeated loading.
To judge an insert, look at four things: density, rebound, cell structure and bonding process. Density is usually given in kilograms per cubic metre. Common PE, EVA, EPE and PU foams trade off density and rebound differently. A cut face on EVA or PE foam should be clean with no dust, and a flocked layer should be firmly bonded with no lifting edges. For precision instruments, check whether an ESD safe material is specified.
An insert is not better for being softer, nor for being harder. It should match the weight, fragility and handling frequency of the item being protected. During procurement, request the density and material description and ask for a small physical sample you can press, rub and smell. Powdering, shedding and a sharp chemical odour are all clear negative signals.
Pitfall eight: no high or low temperature validation, brittle fracture in cold
Protective cases are routinely used outdoors, in vehicles, in warehouses and in cold chain environments where temperature swings widely. Cold is a silent killer of plastic parts. Toughness falls and brittleness rises, so a drop can crack the case. Heat accelerates gasket ageing and material deformation. Many procurement incidents happen after the first batch has survived its first winter.
The method is to define the operating temperature range and require the supplier to provide low temperature drop or impact validation. On the material side, check whether a low temperature grade was selected; copolymer PP typically has better low temperature toughness than homopolymer PP. On the structure side, avoid sharp internal corners, which concentrate stress, and avoid abrupt wall thickness changes. For how materials trade off across environments see how to choose materials for outdoor cases.
This is the pitfall most worth validating at the sampling stage. Conditioning a specimen in a cold environment, for example in the minus 20 to minus 30 degree Celsius range as agreed to the real duty, and then dropping it, is more convincing than any verbal assurance.
Pitfall nine: missing packaging and transport protection
Many "quality problems" actually happen in transit rather than in production. A protective case protects other things but is often left unprotected itself. Stacking without corner protectors, no cushioning between cases, pallets without stretch wrap, and outer cartons with no stacking strength marking. The result on arrival is scratches, crushed corners, deformed latches and even chips in the sealing face.
There are three points to agree. First, the packaging specification, stating inner packaging, cushioning, stack layers and pallet method. Second, transport or stacking requirements, commonly by referencing an ISTA style transport test approach that validates the packaging by drop and vibration. Third, the arrival appearance criteria, with scratch length, area and location graded so that arguments about "that is a transport issue, not ours" do not arise.
For export projects, destination packaging and environmental requirements also apply. A practical move is to make the packaging scheme part of the technical agreement and approve it alongside the product drawing, rather than improvising shortly before shipment.
Pitfall ten: no after-sales support and no spare parts
The last pitfall usually appears after the purchase is complete. When a gasket ages, a latch breaks or a handle snaps, the buyer discovers that the factory does not sell parts separately, that the model is obsolete, or that a substitute supplier's parts simply do not fit. A protective case is a long service tool, so the availability of after-sales support and spare parts should be assessed as a criterion at the time of purchase.
Ask four questions. First, can consumables such as gaskets, latches, handles, feet and pressure relief valves be bought separately. Second, do the spares carry a stable part number that maps to a specific case model. Third, for how long after a model is discontinued or revised will spares be supplied. Fourth, is there an official or authorised channel, to avoid buying a substitute with the wrong dimensions. For the risk of substitutes see replacing a gasket: original versus aftermarket parts, and for building the spares list see the consumable spare parts stocking list for protective cases.
JUNZHJIA, manufactured by KeXin New Materials (Guangdong) Co., Ltd., supplies wholesale, distribution, OEM and ODM projects worldwide and can provide matched gaskets, latches, handles and other consumable parts by model, together with drawings, material declarations and test documents so that buyers can write spare parts supply into a long term agreement.
On-site audit sheet for all ten pitfalls
Compress the ten pitfalls into one sheet that can be printed and taken to a factory. Every action should be photographable and recordable.
| No. | Pitfall | Audit action | Acceptance basis (typical value) | Evidence |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| 1 | Sealing structure | Request a section drawing or cut sample | Groove present, compression 20 to 30 percent | Section photograph |
| 2 | Resin grade | Require grade and property data | Named grade plus maker | Specification sheet |
| 3 | Wall and ribs | Measure wall thickness, review rib layout | Main wall 2.5 to 4.0 mm range | Measurement record |
| 4 | Latch and hinge | Check material, run a cycle test | Engagement feel, several thousand cycles | Life statement |
| 5 | Gasket | Ask material, run a rebound test | Shore A 40 to 70, clean rebound | Material declaration |
| 6 | IP rating | Verify the test report | Standard, sample, conditions | Test report |
| 7 | Insert | Physical sample, press and rub | No powdering, no shedding, bonded | Physical sample |
| 8 | Temperature | Cold soak then drop | No brittle fracture, no cracking | Test record |
| 9 | Packaging | Check spec and stacking marks | Corner protectors, cushioning, layers | Packaging specification |
| 10 | After-sales | Ask about separate spares and supply term | Consumables available, part numbers map | Spares list |
The most useful column is the evidence column. If a supplier can produce the matching document for all ten rows, procurement risk is largely brought under control.
Clauses that must appear in the purchase contract
Beyond the checklist, the contract is the last gate that turns verbal promises into obligations. Write at least five categories clearly.
- Material clause: state the resin grade, colour standard and appearance criteria, and require written notification and buyer approval before any material change.
- Performance clause: state the ingress protection rating and its verification standard, such as IEC 60529 or GB/T 4208, together with drop, stacking and operating temperature requirements.
- Acceptance clause: state the sampling standard, for example the inspection level and AQL under GB/T 2828.1, the critical, major and minor defect classification, and the disposition of nonconforming lots.
- Change clause: notify and potentially retest on any change to tooling, material, gasket or supplier.
- After-sales clause: state consumable supply, the mapping between spares and models, and the supply period.
For the acceptance and sampling method in practice see how to sample an incoming batch of protective cases, and for contract wording see putting the ingress protection requirement into the purchase contract. Writing clauses in detail is not about going to court. It is about filtering out nonconforming suppliers in the first round.
Frequently asked questions
Q: When buying protective cases, which document should be requested first? A: Ask for the specification sheet plus a section view or sectioned sample as a pair, rather than looking first at price or a render. The reason is that nearly all of a protective case's performance sits in structures you cannot see: the gasket groove shape, the wall thickness, the rib layout, and the material and structure of the latch and hinge. A specification sheet answers the key questions in one pass, covering resin grade, dimensional tolerance, IP rating and operating temperature, while a sectioned sample verifies whether the sheet is truthful. Many procurement incidents trace back to a buyer ordering on a vague line such as "engineering plastic, waterproof and drop resistant". The correct order is to obtain the specification and section first and confirm the structure, then obtain the test report and golden sample to confirm performance and appearance, and only then negotiate price and payment terms. Reversing that order means making the highest risk decision with the least information.
Q: A supplier says every case is IP67. What is needed to believe it? A: Require a test report that corresponds to the specific model you are purchasing, not a picture of a "waterproof certificate" or a report for a "similar product". Check four things. First, the standard number and revision referenced, IEC 60529 or GB/T 4208. Second, whether the sample description in the report is your case specification. Third, whether the immersion depth and duration of the water test are stated, which is exactly where IP67 and IP68 differ. Fourth, whether the issuing body and the date are traceable. If the only material is marketing artwork, or the report covers a "same series product" that cannot be matched one to one, treat the claim as an inflation risk. As a fallback, agree in the contract on incoming immersion sampling, with clear return and liability terms if the batch fails.
Q: Where do low cost protective cases usually cut their costs? A: Empirically, in four places. First, material, where a general purpose resin or regrind replaces a weather resistant grade; the appearance is almost identical but toughness, weatherability and low temperature behaviour fall noticeably. Second, wall thickness and ribs, where the main wall is thinned and the base grid is reduced, directly saving material and cycle time with no visible difference. Third, the gasket, where a cheap rubber replaces silicone or EPDM; short term it is fine, but within six to twelve months it hardens and fails. Fourth, the insert, where low density foam replaces the specified density PE or EVA, and powders over time. All four save on performance you cannot see. Price in itself is not the problem. The problem is whether the low price comes with a downgraded specification. The right method is to take the low quote and require the supplier to confirm those four specifications in writing, comparing specification rather than price.
Q: Which items should be validated at the sampling stage to avoid a mass production failure? A: Sampling is the cheapest validation window. Cover at least five categories. First, dimensions and fit: measure key dimensions, lid closure gap and latch engagement. Second, sealing: run a negative pressure check or immersion test to confirm the gasket compression is right. Third, structure: cut one case open and measure wall thickness and inspect the ribs and gasket groove. Fourth, environment: condition in cold and then drop, checking for brittle fracture. Fifth, life: cycle the latch and hinge a defined number of times and look for rapid loosening. In addition, sign off a golden sample from the sampling run as the appearance and feel baseline for production. In practice, most mass production quality problems can be exposed early if these five are done at sampling, at the cost of a few samples and one round of time.
Q: For a small order of a few hundred pieces, will a supplier cut corners? A: Small orders deserve more caution for two reasons. First, the tooling and fixtures for a small order are usually a shared existing solution, so the supplier has little incentive to optimise material and structure for your run, and the probability of "use whatever is on hand" rises. Second, the buyer has weak bargaining power and is tempted to concede on specification to secure delivery. Small order buyers should therefore lock the specification down harder: resin grade, wall thickness range, gasket material, IP rating and insert density, each stated in writing. A small order also does not need elaborate customisation such as two colour moulding or complex flocking. Concentrate the budget on the three items that decide life: sealing, latch and material. If a supplier is clearly evasive when asked to confirm specifications, pay more and change supplier rather than risk a batch rework to save a little.
Q: How do you tell a real protective case factory from a trading company? A: Cross check five angles. First, look at process depth: a real factory can discuss mould structure, gate location, sink mark control and gasket groove design, while a trader can only relay. Second, look at willingness to accept a factory audit and to provide production floor photos or video. Third, look at material purchasing evidence and property data, since a factory usually deals with resin suppliers directly. Fourth, look at how sampling problems are answered: a factory offers structural improvement suggestions, while a trader tends to say it will make another one. Fifth, look at spare parts capability, since a factory can keep supplying gaskets and parts for older models and a trader usually cannot. A trading company is not automatically off limits, but its markup and information gap amplify quality risk, so raise the validation intensity and contract discipline accordingly.
Q: What should the first round of incoming inspection focus on? A: Work quickly through appearance, structure, function and marking. For appearance, check colour variation, scratches, sink marks, and the position and area of weld lines. For structure, check whether the lid closure gap is even, whether latches engage, whether hinges wobble, and whether feet are complete. For function, check opening force, whether the gasket is flat and untwisted, and whether a negative pressure or immersion check passes. For marking, check whether the model, batch number and IP marking match the contract. At the same time check the packaging for impact marks and, if present, separate production defects from transport damage and record them separately. Inspection should leave written and photographic records, classify defects and decide the lot disposition: accept, screen, concede or reject. For the detailed incoming inspection flow see how to sample an incoming batch of protective cases.
Q: If a batch has already arrived with quality problems, how should it be handled and claimed? A: Secure the evidence first, then discuss liability. The first step is to retain samples and records: photograph and video the nonconforming areas, keep batch and quantity information and, where necessary, seal part of the shipment. The second step is to define the nature of the problem, separating a design or structural defect such as an inadequate gasket groove, which is systemic, from an incoming material or process defect such as sink marks or poor assembly, which is lot related, and from transport damage, which belongs to delivery. The third step is to check the contract clauses and raise the claim on the agreed defect classification, sampling standard and disposition path, including return, screened resubmission, concession with price adjustment, or supplier corrective action followed by a new run. The fourth step is to assess rework feasibility, since a locally repairable defect such as a gasket change or a missing foot can be settled by the supplier shipping spares. Keep every step in writing and file it in the supplier quality record, both for this claim and for future negotiation and consolidation decisions.
Conclusion and related reading
Back to the original question: how do you avoid procurement pitfalls when buying protective cases? By targeting the ten things you cannot see and shining evidence on each of them. Sealing structure, resin grade, wall thickness and ribs, latches and hinges, gasket, IP rating, insert, high and low temperature behaviour, packaging and transport, and after-sales spares. Together these cover virtually every source of a protective case's real performance, and their shared property is that appearance rarely distinguishes a compliant unit from a noncompliant one.
Three actions you can take immediately. First, make "specification sheet plus sectioned sample" the entry threshold for a quotation, and dismiss any supplier who cannot provide them. Second, write the IP rating, resin grade, gasket material and acceptance sampling into the contract, turning verbal promises into written obligations. Third, complete the five validations at sampling — dimensions, sealing, structure, environment and life — to stop problems before mass production at the lowest possible cost.
JUNZHJIA, manufactured by KeXin New Materials (Guangdong) Co., Ltd., produces protective cases, toolboxes, military-specification storage cases and waterproof junction boxes for wholesale, distribution, OEM and ODM programmes and global supply. The company configures material, sealing, latches and inserts to the duty of each project, supplies drawings, material declarations, inspection records and test documents, and supports long term supply of consumable spare parts so that buyers can fold quality and after-sales clauses into the technical agreement.
Related Reading