

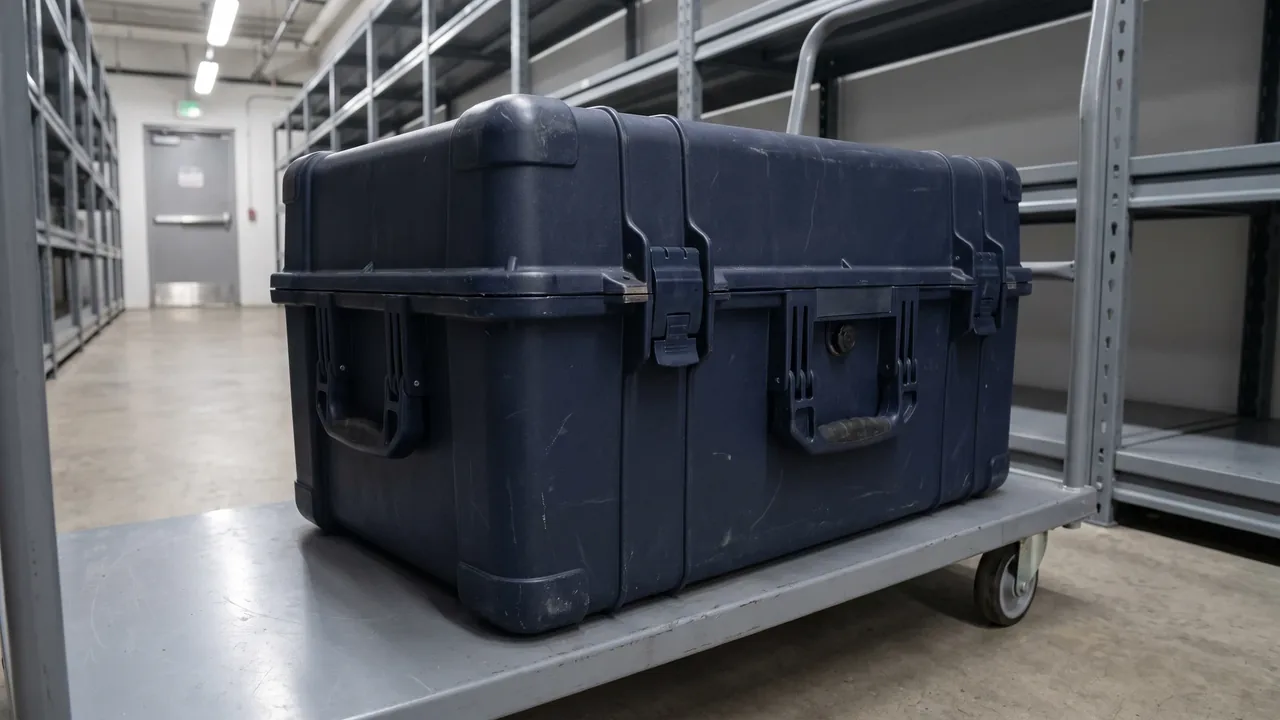
The logistics support box is a modular resupply container built for military rear services, emergency support, and defense-trade channels. Its task is not to hold one specific piece of equipment, but to turn "resupply" itself into a box capability that can be standardized, rapidly issued, and reconfigured on site. A support box cycles between base warehouse, transfer hub, and forward support point; it must survive forking and stacking, let an untrained handler find each item by its fixed position, and remain traceable after many open-and-reseal cycles. This article unpacks, from a protective-case manufacturer's point of view, the general requirements a logistics support box should meet in modular topology, material, quick open-close, zoned liner, palletization, seal traceability, and military acceptance, and gives procurement a checklist they can drop straight into a technical agreement. It must be stated plainly that this article discusses the packaging container only; the movement of materiel and any defense-trade export are governed by local regulations and export control requirements, and the container supplier's duty is to translate modularity, sealing, restraint, and traceability into a mass-producible box structure.
Written from the bench of a protective-case manufacturer, this guide deliberately stays within the boundary of the container. It does not describe what the box holds, how it is dispatched, or the controls that govern its movement; those sit with the logistics authority and the regulator. What it does offer is the engineering reasoning a buyer can use to turn a vague "support box" request into a numbered technical agreement, and to ask the right questions when two quotations look identical on paper but diverge sharply on the support capability they actually deliver. The rest of the article walks the support chain link by link, from the standard module to on-site acceptance.
The Mission: Turning Resupply into Modular Capability
The logistics support box faces a cycle of "store, transport, push forward, recover" rather than a single trip. At the base it must stack densely and align to pallet and rack modules; at the hub it must move in groups and re-load quickly; at the forward point it must let a handler open it and pick by diagram without a manual; at recovery it must let the seal be counted, the destination recorded, and the box return to service. This mission means the core of a support box is not "carry a lot" but "recognizable, quick to pick, easy to recover." Abstracting resupply into a standard box plus standard modules is the fundamental way to cut the complexity of the support chain, and the basis on which modern logistics moves from item-level management to box-level management.
Broken down, the mission has four capabilities: standardization, identifiability, reconfigurability, and traceability. Standardization means dimensions and interfaces align to unit-load equipment so boxes and pallets interchange and stack. Identifiability means the box identity and contents list are readable at a glance, cutting search time. Reconfigurability means liner and zoning can adjust quickly to the task, so one box can hold tools in one mission and consumables in another. Traceability means every opening and handover leaves a record, so the responsibility chain still closes at recovery. The manufacturer must reserve interfaces for these four in the structure: modular external dimensions, a readable identification panel, adjustable zoned liner, and a verifiable seal position, all of which are the engineering details that make support capability real.
Concretely, a support box earns its name only when three conditions hold together: the shell is generic enough to share pallets and stacks with other boxes, the interior is configurable enough to match the task, and the identity is readable enough that any handler can tell what is inside without opening it. Miss any one and the box reverts to a one-off crate managed item by item, which is exactly the complexity modular support was built to remove. The remainder of this article treats those three conditions as engineering requirements with measurable acceptance criteria, so a buyer can specify them in numbers rather than adjectives, and can reject a quotation that only describes them in adjectives.
Modular Topology: Standard Box and Combinable Modules
Modular resupply usually takes two topologies. One is "standard box plus fixed liner," where each box is typed to one class of materiel and identical across the batch, suited to long-fixed baseline kits. The other is "standard box plus adjustable module," where the shell is generic and the liner is assembled per task, suited to ad-hoc missions or changing requirements. The former has high protection consistency and easy reset; the latter has high flexibility and utilization. Selection should look at the support rhythm, not just flexibility: fixed-base support favors typed liners, while mobile or ad-hoc tasks favor adjustable modules, because the latter's real value is letting one box switch roles quickly between missions.
Combinable modules bring a frequently overlooked benefit: a shorter repair and spare radius. When a liner is damaged, an adjustable module can be replaced alone without scrapping the whole box; when a task changes, only the module changes, not the box. This matters especially at sea or overseas support points, where a whole-box swap is often impossible on site. The manufacturer should provide the module interface standard and interchange specification, so modules from different batches or suppliers work together inside the same shell, instead of making modules closed parts only the original factory can fit. Writing interface standardization into the technical agreement is more reliable than discovering "modules are not interchangeable" mid-mission and then coordinating a fix.
Material Routes: Why Rotomolded HDPE Leads Support Boxes
The most common material for logistics support boxes is rotomolded HDPE, because it is integrally molded with no weld seam, resists salt fog and weathering, and its cost amortizes across very large batches, fitting the long service of thousands of boxes. Aluminum shells are lighter and more rigid, suiting airfreight or weight-critical scenes, but welds and corners need extra corrosion treatment and cost rises fast with size; composite fiber wins on specific strength but repairability and batch consistency need separate assessment. Support boxes are numerous, widely circulated, and exposed to mixed environments, so the whole-shell corrosion consistency of rotomolded HDPE usually beats a metal box that must be leak-checked point by point, which is the root reason it leads the category.
Whichever material is chosen, the support box should place maintainability on a par with protectiveness. A rotomolded shell, while paint-free, still needs protection from long local compression by sharp objects that causes stress whitening; a metal shell's coating, once scratched, needs prompt touch-up or it pits from the scratch and grows inward. The manufacturer should state the maintenance boundary at delivery: which damage can be handled on site, which needs return to factory, and the inspection interval. Writing the maintenance boundary into the technical agreement saves both sides time over arguing "is this a defect" at acceptance, and avoids a support point using the wrong patch material for lack of guidance and thus accelerating aging. On the detail of weld and corner corrosion, the support box's demand for whole-shell consistency aligns with the "no natural weak point" logic of the metal ammunition container specification, only scaled to the consistency of thousands of boxes.
A second material consideration is whole-life cost, not just unit price. A rotomolded box that survives a decade of circulation with only latch and gasket service is cheaper across its life than a lighter metal box that needs periodic coating inspection and touch-up at every depot. Procurement should ask the manufacturer for a recommended inspection interval and a spare-parts list, then compare the two boxes on the cost of ownership over the expected service life rather than on the purchase line alone. This comparison usually flips the apparent winner, because the box that looks expensive at the dock often costs less by the tenth year of circulation.
Sealing and Quick Open-Close: IP and Life Under High Frequency
The biggest difference between a support box and an ordinary transport case is open-close frequency. An ordinary case may stay sealed three years before one opening; a support box may be opened dozens of times in a single mission, so its sealing system must solve two things at once: outside water and dust stay out, and the latch keeps its life under high-frequency cycling. External protection usually starts at IP65, rising to IP67 for wet-transfer scenarios; the key is uniform gasket compression around the full perimeter and continuity at corners. Latches and hinges must be specified by open-close life with a clear cycle count, not merely labeled "durable."
High frequency also brings a hidden enemy of sealing: human mis-latch. When a handler closes the box hastily under stress, the latch may catch only halfway, the gasket never fully compresses, and water enters unnoticed. Therefore the support box latch should be designed to give clear feedback when not fully engaged, such as a two-stage latch tongue or a visible closure indicator, turning "is it closed tight" into a readable state rather than a matter of personal habit. Such details look trivial but decide whether the box keeps its seal in real use, and are the most worthwhile investment within the manufacturer's responsibility boundary, far more than simply thickening the wall.
Liner and Zoning: Giving Every Item a Fixed Home
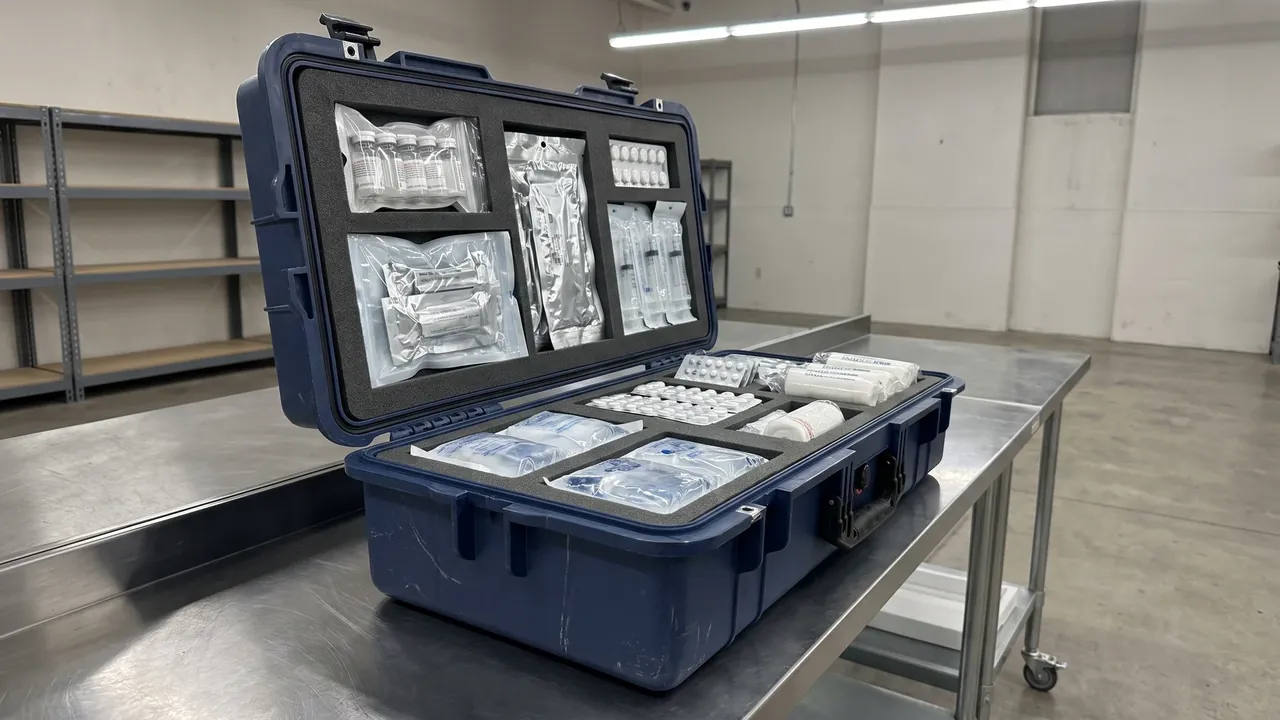
The liner system of a support box has one goal: every item inside has a fixed position, pickable on open and secured on reset. EVA and EPE foams fix single items through pre-cut cavities; divider panels and adjustable trays handle mixed loads; label slots and rest diagrams let any handler reset without training. The liner is not "stuff it with foam" but assigns force to the mass center and vulnerable points so transport shock is absorbed and dispersed rather than concentrated on one edge causing deformation or breakage.
The trade-off between fixed and universal liner depends on how the kit is organized. Fixed-baseline kits suit CNC-cut typed liners with high consistency; ad-hoc tasks suit adjustable dividers and modular trays using zoning logic rather than per-item cutting. Either way, the support box should guarantee "pick on open, secure on reset" without special tools, which directly decides reseal quality and next-mission accuracy. Writing the reset as a diagram on the inner lid is low-cost and high-return; if reset depends on one specific handler's memory, quality drifts when that person leaves, and that is exactly the human-factor risk large-batch support fears most.
A practical liner detail often missed is anti-static treatment for electronic support contents. Many support kits mix tools and sensitive electronics, and a static discharge during pick can damage the latter; specifying an anti-static liner grade and a grounded handling note turns an invisible risk into a controlled one. The manufacturer should state the liner's surface resistance and whether it is permanent or coating-based, because a coating that wears off after a few openings is worse than none, since it gives a false sense of protection. Writing the anti-static requirement into the technical agreement, with a verification method, is far cheaper than learning the hard way that a "static-safe" liner had lost its property months before.
Stacking and Palletization: Docking with Unit Loads
Support boxes rarely sit single in warehouses; more often they stack densely and dock with pallets, racks, and container modules. Stacking strength depends on bearing surface, ribs, and locator pins working together: top and bottom stacking bosses must align so load transfers vertically to the main structure, not onto thin walls or latches; locator pins prevent inter-layer sliding, avoiding collapse during a forklift hard brake or rough road. The manufacturer should give a clear maximum tier and single-tier load, marked visibly, not buried in a manual.
Palletization is the key interface that lets a support box join the logistics system. External dimensions should prioritize alignment to standard pallets and container inner widths, so multiple boxes tile a pallet without gaps or overhang; the base should have features that work with pallet straps or anti-slip mats, preventing the whole load from sliding in transit. This interface looks like a sizing issue but decides whether the box truly enters containerized logistics or gets re-stacked at every node. For defense trade and overseas support, palletization also directly affects sea and air loading efficiency, the last mile that turns "a box" into "a logistics unit," and it shares the load-path discipline discussed in stackable containers.
Locks and Seals: The Responsibility Chain in Mass Issue
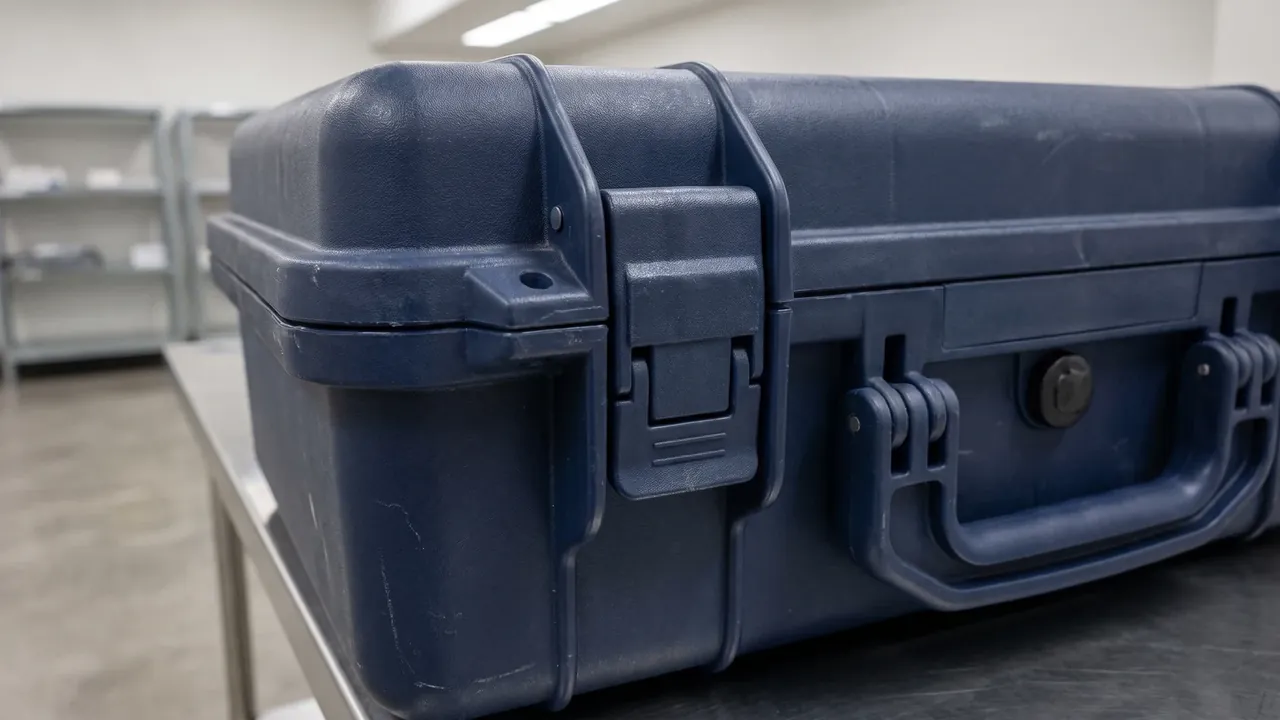
In mass issue, seal management matters more than for a single box. A support box usually has two lock layers: a quick-open latch for daily access, and a numbered seal added at handover. The seal number binds to the handover sheet, and every opening generates a record, ensuring a definite answer to "was it opened." High-value or sensitive batches can upgrade to RFID seals that automatically record time and location at each custody point, turning the responsibility chain from manual check to system trace, reducing human error and raising credibility across multi-unit handovers.
Traceability also lives in the identity system. The support box should provide both a QR code and an embossed serial on the identification panel, so manual verification survives a scanner outage; a hidden verification code inside the lid guards against malicious replacement of the external plate. This dual identity matters especially in mass support, because a batch may cross many units and years, and any single identity mismatch voids every later record. Front-loading traceability into the box structure, rather than pasting paper after the fact, is the key action within the manufacturer's responsibility boundary and the basis the buyer can rely on at inventory and audit. The logic is consistent with the sealed-to-opened traceability emphasized for the ordnance packing box, only the support box raises the frequency from "once in years" to "once in days."
Rapid Issue and On-Site Reconfiguration: A Warehouse at the Front
The highest value of a support box is reconstructing a "warehouse" at the forward point. When the shell is standardized, the liner modular, and the marking visual, a handler can assemble the needed kit from standard modules by task without relying on the rear, and quickly return and reconfigure them. This requires the box to reserve design for on-site reconfiguration: liner modules must be hand-removable, markings quickly swappable, and lists updatable with the task rather than welded onto the lid. Making "on-site reconfigurable" a product capability, not the handler's improvisation, is the divide between "a box" and "a support system."
On-site reconfiguration must also consider mis-fit protection. When many module types are mixed, the chance a handler grabs the wrong one rises with task complexity, so module interfaces should be mistake-proof: different shapes or slots prevent a wrong module from seating, stopping misconfiguration at the source. The box should also reserve a list card position so current contents match the task list one to one, and opening reveals "what this box holds now." These designs move support accuracy from personal responsibility to product design, markedly cutting mis-issue and omission in high-tempo, large-batch support, and are the core advantage of a modern support box over traditional wooden crates and assorted plastic cases.
Marking and Visibility: Making the Box Speak
A support box is handled and quickly identified by many people in transit, so its marking system matters more than for ordinary cases. A qualified support box should provide at a readable position: box type, contents class, weight and center-of-gravity mark, open indicator, stacking limit, and a scannable identity code. Marking should let warehouse, hub, and forward personnel complete identification and handling within seconds — see the class from afar, see the contents up close, scan the whereabouts — instead of everyone opening the box to search. Visibility is the cheapest way to cut communication cost across the support chain.
Marking materials and process must survive the environment. Outdoor and deck conditions quickly fade and peel paper labels, so identity and class markings should prefer silkscreen, engraving, or weatherproof plates over stickers; the updatable task list can use a clear window card that is both weatherproof and easy to change. The manufacturer should deliver marking maintenance guidance: which marks are fixed, which are field-updatable, and how to verify after update. Writing marking into the technical agreement is more reliable than discovering "can't tell what this box holds" mid-support and then fixing it, and avoids mis-identification causing wrong-issue accidents.
Beyond the marks themselves, the support box should make re-marking a controlled act. When a box is repurposed between tasks, the old class mark must be cleanly removable or permanently overprinted, not taped over, because a taped-over mark that peels at the wrong moment can send a box to the wrong destination. The manufacturer should design the marking surface so updates are deliberate: a recessed window for the swap card, an engraved class code replaced only with an authorized insert. Treating re-marking as a controlled change, like a configuration change on any managed asset, is what keeps a large box fleet honest across years of reuse.
Military Testing and Acceptance: Mapping MIL-STD-810H to GJB
A logistics support box cannot be accepted on "looks sturdy" alone; it must fall to repeatable tests. Vibration, drop, temperature-humidity cycling, and salt spray are the four basics: vibration verifies whether the liner truly keeps items still, drop verifies corner and latch behavior under accidental impact, temperature-humidity cycling verifies sealing and liner stability across seasons, and salt spray verifies the corrosion floor of long circulation. MIL-STD-810H and GJB provide the test framework, and the manufacturer should map the specific route to the corresponding profile rather than loosely claiming "tested to military standard," because climates and salt-fog grades differ widely by deployment. This route-mapping method follows the framework shared with the military standard case, the only difference being that the support box also brings open-close life into the profile input.
The test report's value goes beyond a pass mark. Drops leave recognizable corner deformation, vibration exposes insufficient liner restraint, and these findings feed directly back into mold and liner improvement, where the test budget truly earns its return. Support-box buyers usually hold real transit-damage data; aligning field-observed damage with lab-reproduced failure modes is the most effective improvement loop a manufacturer can run. Writing the test profile into the technical agreement, selected by real route rather than highest grade, neither under- nor over-validates; over-validation only raises cost without adding field reliability, while under-validation leaves a blind spot exactly where it is needed most.
A further point on test design is the environmental spectrum rather than a single point. In real deployment the box may sit in a hot humid port, transfer to a cold dry depot, then rest in salt fog; testing only one climate misses the others. Procurement should write "full environmental spectrum" into the agreement as a test input, requiring a combined sequence of temperature, humidity, salt spray, and vibration with the worst order as the acceptance threshold. This route-based design predicts field performance far better than chasing the words "military standard passed," and it is the same discipline the military standard case applies to its own test mapping.
Export and Compliance: Governed by Local Regulations
When logistics support boxes enter defense-trade export, the container adds a layer of compliance. Where dangerous-goods classification applies, UN packaging certification, packing lists, and material conformity documents must be complete, with the physical box, certificate, and test report corresponding one to one; wooden packaging must meet IPPC fumigation or exemption declaration, while metal and plastic focus on material declaration and recyclability marking. It must be emphasized that this article discusses the container only; whether materiel may be exported, which channel, and which controls apply are governed entirely by local regulations and export control requirements, and the container supplier's duty is to embody those traceability and compliance requirements in the box and document structure, not to judge or participate in the flow of the materiel itself.
The most typical export failure is "document inconsistency": the box type on the UN certificate, the state in the test report, and the actually shipped box do not match, and the batch is often detained at some port. The manufacturer's sound practice is to attach the document list as a technical-agreement annex stating version, validity, and issuing body, and to re-verify against the certificate before each new production. Starting the paperwork two weeks early usually halves clearance time; carriers and freight forwarders should receive the same annex, because most detention incidents begin with a document the shipper never saw. For defense-trade support materiel, compliance documents and box structure are equally important, and missing either end costs at the export stage.
On-Site Acceptance: What Procurement Should Verify
Acceptance is where paper meets the delivered box, and a few checks catch most failures before handover. First, verify identity: embossed serial matches the handover sheet, QR scans to the same record, hidden lid code corresponds. Second, verify sealing: press the lid at corners for even gasket contact, and confirm the pressure equalization valve (if fitted) is clear and moves freely. Third, verify liner: each item grips its cavity without force yet releases without tools, proving the reset logic truly works. Fourth, verify modules: external dimensions align to pallet, stacking bosses actually interlock rather than relying on friction. These checks take minutes on the first article and prevent a whole batch entering circulation with a tolerance the warehouse cannot use.
A second class of checks covers structural claims. Reconcile the stated stacking limit against actual boss alignment, dry-fit two boxes to see whether locator pins truly interlock; check fork-pocket spacing against base handling equipment; confirm lash points sit on reinforced zones, not thin shell. The technical agreement should name which checks are first-article mandatory and which are per-batch sampling, so acceptance is repeatable across deliveries and across the years the box will circulate. Writing "first-article failure stops the batch" as a mandatory clause turns acceptance from a signature into a control point, and is far cheaper than discovering a systematic flaw after thousands of boxes have entered years of circulation.
A Selection Checklist for Logistics Support Boxes
Finally, a parameter framework procurement can lift directly into a tender and technical agreement. Structure: whether external dimensions align to pallet and rack modules, empty-case weight, declared stacking tiers, fork-pocket and lashing-point positions, and open-close life rating. Protection: IP rating, gasket material, presence of a pressure equalization valve, liner zoning logic. Durability: hinge and latch open-close life, handle load test, salt-spray hours. Liner: fixed or adjustable, zoning method, rest diagram and label slots. Traceability: identification panel position and size, seal type and electronic-seal support, serial number format. Validation: an ISTA or equivalent report stating drop height and vibration spectrum, including open-close life and pallet compatibility. Putting this checklist into the tender upfront governs support quality better than arguing line by line at acceptance.
Buying a logistics support box is, in essence, paying for the support rhythm and the number of circulation cycles. Once those two numbers are estimated honestly, every line of the framework gains a budget anchor. It must be restated that this article discusses the packaging container only; the storage, transport, and export of materiel are governed by local regulations and export control requirements, and the container manufacturer's duty is to translate modularity, sealing, restraint, and traceability into a mass-producible box structure, not to participate in managing the materiel itself. Writing the checklist into the agreement is the first step that turns "modular resupply" from a slogan into an auditable engineering fact.
Frequently Asked Questions
Q: What is the core difference between a logistics support box and an ordinary transport case? A: The core difference is open-close frequency and responsibility-chain density. An ordinary transport case is built around a single shipment with three to five controlled handlings; a support box is built around the store-transport-push-recover cycle, and must keep its seal, liner order, and identity intact under high-frequency opening, many handlers, and cross-unit handovers. This forces it to clear quick open-close life, visual marking, adjustable liner, and seal traceability simultaneously, and a weakness on any line breaks the support chain at some node. The price gap is real, but putting an ordinary case into a support chain almost always returns as mis-issue, omission, and seal lapse several times over. The difference also shows in reset logic: the support box is designed so anyone can reset without training, while an ordinary case often relies on a specific person, raising long-term cost. In practice this means the support box is specified not by how much it holds but by how reliably it can be opened, picked, and reclosed by whoever happens to be standing there, which is a different engineering problem than shipping one sealed load across a quiet route.
Q: Should modular support use a fixed liner or adjustable modules? A: It depends on the support rhythm, not merely flexibility. Long-fixed baseline kits suit CNC-cut typed liners with high consistency and easy reset, and batch uniformity aids inventory; ad-hoc or mobile tasks suit adjustable dividers and modular trays using zoning logic, whose core value is letting one box switch roles quickly between missions. Selection must also weigh repair radius: an adjustable module can be replaced alone without scrapping the whole box, which matters when on-site whole-box swap is impossible. The manufacturer should provide the module interface standard so modules from different batches work together, rather than making them closed parts only the original factory can fit, because discovering modules are not interchangeable mid-mission directly slows support. A further consideration is configuration control: fixed liners make every box identical and thus easier to audit and reorder, while adjustable modules require the task list to travel with the box so the contents are always known; the buyer should decide which discipline fits their unit before specifying, because the two topologies manage change in opposite ways.
Q: How can a support box stay sealed under high-frequency open-close? A: Attack both the gasket and the latch life. External protection starts at IP65 and rises to IP67 for wet transfer, with the key being uniform perimeter compression and corner continuity; latches and hinges carry a stated open-close life count rather than a vague "durable" label. More important is preventing human mis-latch: under stress a handler may catch the latch only halfway, leaving the gasket uncompressed and water entering unnoticed, so the latch should give clear feedback when not fully engaged through a two-stage tongue or visible indicator. Such details look trivial but decide whether the box keeps its seal in real use, and are a more worthwhile investment than simply thickening the wall. The open-close life rating should also be verified by test, not asserted, because a latch that claims ten thousand cycles but fails at two thousand will surface exactly during a high-tempo mission when the box is opened most; asking the manufacturer for the test method behind the life number turns a marketing phrase into a checkable specification.
Q: How does a support box achieve "pick on open, secure on reset"? A: Through zoned liner and visual rest mapping. EVA and EPE foams fix single items in pre-cut cavities, dividers and trays handle mixed loads, and label slots with rest diagrams let any handler reset without training. The liner assigns force to mass centers and vulnerable points so shock is dispersed, not concentrated on an edge. Whether fixed or adjustable, the box should let the operator return items without special tools, which directly decides reseal quality. Writing the reset as a diagram on the inner lid is low-cost and high-return; if reset depends on one person's experience, quality drifts when that person leaves, and that is the human-factor risk large-batch support fears most. A subtle but important point is that the rest diagram must match the actual cavity layout, not a generic illustration, because a mismatch teaches the handler the wrong reset and silently defeats the design; the manufacturer should silk-screen or engrave the diagram from the same CAD used to cut the liner, so the picture and the pocket always agree.
Q: Which packaging documents are needed when support boxes are exported? A: Where dangerous-goods classification applies, UN packaging certification, packing lists, and material conformity documents must be complete, with the physical box, certificate, and test report corresponding one to one; wooden packaging must meet IPPC fumigation or exemption declaration, while metal and plastic focus on material declaration and recyclability marking. The typical failure is document inconsistency: certificate box type, report state, and actually shipped box do not match, often detained at a port. The sound practice is to attach the document list to the technical agreement with version, validity, and issuing body, re-verify against the certificate before each new production, and start paperwork two weeks early to typically halve clearance time. This article discusses the container only; export is governed by local regulations and export control requirements, and the box must carry the compliance structure rather than the authority to export. A practical tip is to give the freight forwarder the same document annex at the time of booking, not at the gate, because most detentions start with a paper the shipper never shared and the carrier cannot reconstruct under time pressure.
Q: How should the maximum stacking tier of a support box be determined? A: Not as an experience number, but by the synergy of bearing surface, ribs, and locator pins. Top and bottom stacking bosses must align so load transfers vertically to the main structure, not onto thin walls or latches; locator pins prevent inter-layer sliding during a forklift hard brake or rough road. The manufacturer should give a clear maximum tier and single-tier load marked visibly, and verification should calculate layer by layer under full load rather than testing only the bottom box, because the truly stressed part is the bottom-tier sidewall and corner. Writing both the limit and the allowed eccentricity into the technical agreement avoids warehouses arbitrarily adding tiers to save space, which is how most stack collapses actually begin in practice. The eccentricity note matters because real stacks are rarely centered and a jolt adds side load, so the stated tier should carry an allowed offset beyond which stability is lost; without that number the warehouse guesses, and guessing is what turns a rated stack into a collapsed one.
Q: Why does a support box need a dual-identity marking? A: Dual identity means the panel provides both a QR code and an embossed serial, with a hidden code inside the lid, so traceability holds even if any single point fails. When the scanner fails or the label wears, the embossed serial still allows manual verification; if the external plate is maliciously replaced, the internal code exposes it. Support boxes cross many units and years, and any single identity mismatch voids all later records, so the identity system must be front-loaded into the structure rather than pasted on afterward. High-value batches can upgrade to RFID seals that record time and location at each custody point, turning the responsibility chain from manual check to system trace, so "was it opened" has a definite answer and trust cost across multi-unit handovers drops sharply. The hidden code also defeats a subtler attack: an insider swapping the external plate while leaving the contents untouched, which a single-identifier system would never catch, and which in a high-value batch is exactly the scenario the dual system is built to survive.
Q: Why should the military test report not be read only for a pass mark? A: Because the report translates "this box is sturdy" into verifiable data. Drops record corner deformation, vibration records whether the liner truly kept items still, and salt spray records the corrosion floor, and these findings feed directly back into mold and liner improvement, where the test budget earns its return. A supplier without a report can only promise verbally, with nothing to compare in a damage dispute; a supplier with a report has committed to specific test conditions checkable line by line. The deeper value is the improvement loop: aligning field damage with lab failure modes forces mold or liner optimization. The report should bind to the real route rather than be requested generically, because only a profile matching the actual logistics scenario predicts field performance.
Closing
The reliability of a logistics support box is written into every detail of modularity and traceability: standardized interfaces, feedback-capable sealing, resettable liner, and closed-loop seals. Buy it as a support system, not as a thicker box. Related Reading: Rotomolded Transport Case, War Reserve Case, Transit Case and Shipping Case.