

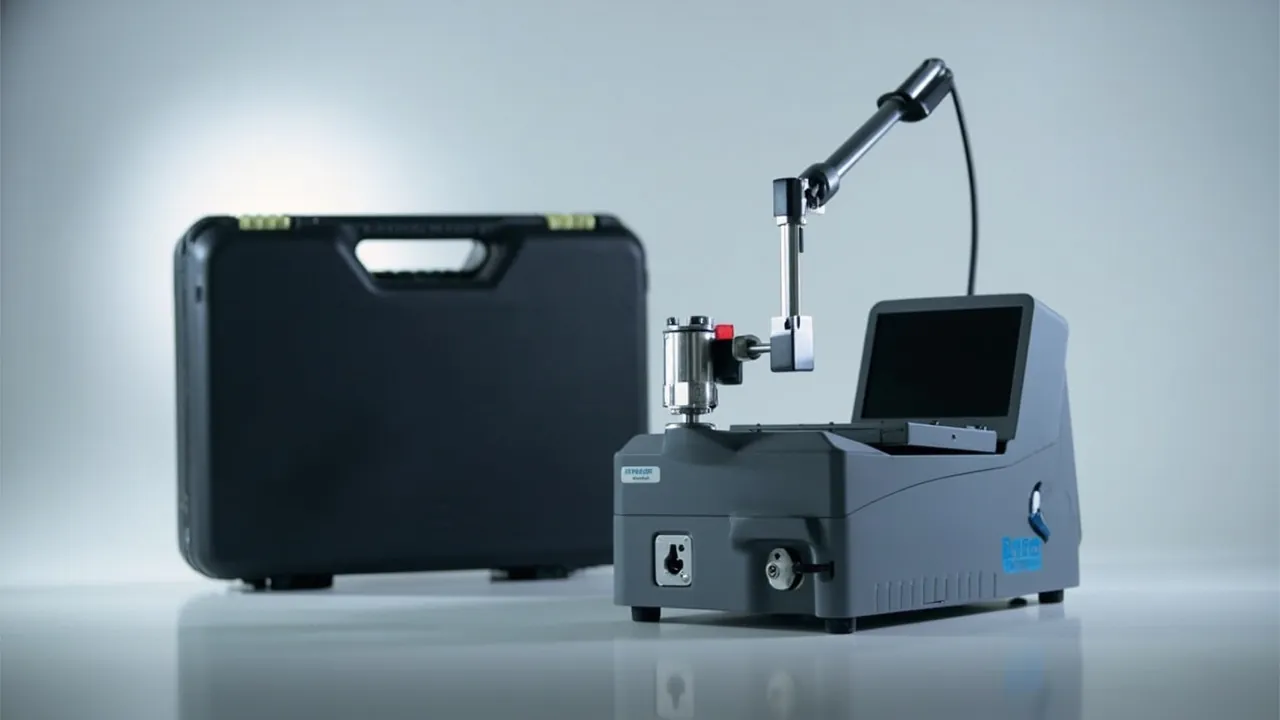
A counterintuitive fact governs test handler component maintenance: the parts most easily damaged in transit are often not the expensive ones, but consumable contact components such as test sockets and pick-and-place nozzles that carry a modest unit price and are replaced frequently. The reason is simple. Their acceptance criteria are contact force and coplanarity, not whether they can be bolted back on. A single badly packaged shipment can compress pogo pins a few microns permanently and change the contact-resistance distribution, or leave fine scoring on a nozzle face that shifts pick-and-place position. The central conclusion of this article is that handler component cases must be designed on a contact-component-first principle, giving test sockets, probes, and nozzles their own compartments and their own restraint, never mixing them into the same cushioning system as structural metal parts.
What makes these defects awkward is that they leave the machine's functional logic untouched. After installation the handler still loads, tests, and sorts, and no controller raises an alarm. What changes is the distribution of test data: contact failure rate rises on certain channels, temperature results shift on certain lots, or placement accuracy for a given package begins to jitter. Engineers typically suspect the test program, probe wear, or the temperature sensor first, and arrive at packaging and transport last.
This article follows the test flow sequence, working through protection requirements for test sockets, contact components, thermal heads, handling mechanisms, and alignment systems, and it sets out executable approaches for insert compartmentalization, cleanliness and static control, humidity transition management, and verification and offline re-measurement. It is written for equipment and process engineers at assembly and test houses, handler spare parts suppliers, and second-hand equipment dealers.
Table of Contents
- Three Difficulties That Define Handler Component Protection
- Module Inventory and Transport Fragility Ranking
- Test Sockets: Why Contact Force Retention Comes First
- Probes and Elastic Contacts: Deformation, Fatigue, and Coplanarity
- Thermal Heads and Temperature Chambers: Thermal Interfaces and Condensation
- Handling Mechanisms: Nozzles, Grippers, and Vacuum Circuits
- Precision Alignment Systems: Preserving Optical and Motion Datums
- Insert Compartmentalization: Flexible Layout for High-Mix Low-Volume Work
- Material Selection Under Combined Cleanliness and Static Constraints
- Humidity, Condensation, and Cross-Environment Transition
- Case Load Design From Bench Parts to Gantry Modules
- Packaging as a Storage Unit: The Spare Parts Inventory View
- Transport Verification and Offline Re-Measurement
- Frequently Asked Questions
- Conclusion and Related Reading
Three Difficulties That Define Handler Component Protection
Before defining packaging requirements, it helps to see how a test handler differs from general semiconductor equipment.
The first difficulty is the very small magnitude of contact force. A test socket establishes electrical connection to device leads, solder balls, or pads through pogo pins or elastic contacts, and contact force typically sits in the range of tens to hundreds of millinewtons. That force must be high enough for stable contact resistance yet low enough not to damage the device. A transport-induced displacement of a few tens of microns is enough to change the spring compression and therefore the contact resistance. For a structural part, the same displacement is irrelevant.
The second difficulty is that high-frequency behavior is sensitive to geometry. At high test speeds, the electrical behavior of a socket and its probes depends on geometric shape and dielectric distribution. Probe bending, dielectric displacement, and shield misalignment all change impedance and crosstalk. The consequence is not that testing becomes impossible but that it becomes inaccurate, often showing up only in specific frequency bands or on specific channels.
The third difficulty is coplanarity across many contacts. A BGA package may present hundreds to over a thousand contact points, and socket coplanarity determines whether all of them make contact at the same moment. Any deformation that shifts coplanarity shows up as partial contact failure, with failed positions varying by package lot, making diagnosis very difficult.
Stacked together, these three difficulties mean the design objective for a handler component case is not impact resistance. It is preserving contact force, coplanarity, and high-frequency geometry through transport.
Module Inventory and Transport Fragility Ranking
The pre-packing inventory should be built by module and sorted by fragility. Handler spares span a wide range, from nozzles weighing a few grams to thermal chambers weighing over a hundred kilograms, and one parameter set cannot serve all of them.
| Handler Assembly | Most Sensitive Feature | Transport Exposure | Retention Criterion | Handling Rule | ||
|---|---|---|---|---|---|---|
| --- | --- | --- | --- | --- | --- | --- |
| Test socket body | Contact array planarity | Sustained pressure, lateral shock | Contact force stays inside its band | Never compressed in the case | ||
| Pogo pins and elastic contacts | Spring preload | Long-term compression, side load | Force output unchanged | Free state only | ||
| Probe card and interposer | Needle tip geometry | Shock, vibration, particles | Tip coplanarity preserved | Own sealed inner box | ||
| Thermal head and heater block | Mating face flatness | Impact dents, moisture | Thermal resistance unchanged | Soft pad over the face | ||
| Temperature chamber parts | Seal condition, insulation | Condensation, compression | Seals recover completely | Dry, seals left unloaded | ||
| Pick nozzle and gripper | Face flatness, grip parallelism | Friction, blockage | Vacuum seal intact | Face up, never stacked | ||
| Vacuum generator and valve body | Internal passages | Crushing, internal debris | Flow and hold time unchanged | Every port plugged | ||
| Vision and alignment camera | Optical-axis datum | Vibration, particles | Imaging centre fixed | Lens and body packed together | ||
| XY alignment stage and drive | Raceway form, screw clearance | Shock, vibration | Repeatability retained | Travel blocked for transit | ||
| Sort tube and tray | Contact surfaces | Static charge, warping | No charge build-up | Dissipative material only |
The key to using this table is to isolate the hardest-to-protect components first. Test sockets, elastic contacts, and probe cards are highly sensitive on all four axes — shock, vibration, cleanliness, and static — so they should occupy dedicated, individually accessible cavities and should not depend on the rest of the case to provide their cushioning. Structural parts are then allocated cushioning by weight and stiffness.
One further practical rule: never put a test socket and a nozzle in the same cavity. The two have different allowable limits. A nozzle needs lower-stiffness cushioning, while a socket needs more stable face support. Mixed packing means one of them is always compromised.
Test Sockets: Why Contact Force Retention Comes First
A test socket is the mechanical and electrical interface between the handler and the device under test, and its key performance parameter is not outline dimension but the stability and uniformity of contact force.
A pogo-pin socket contains a set of independent elastic contacts, each with its own spring, barrel, and plunger. These elastic elements are screened and matched at the factory so that the contact force across the full array falls within a narrow band. Transport shock affects this system through three paths.
Path one: permanent spring compression. If pogo pins sit under load in the packaging, sustained compression produces permanent set and reduces force. The reduction may be only a few percent, which is already enough to matter for contact-resistance-sensitive high-frequency testing.
Path two: axial displacement of the plungers. Shock produces small displacement of plungers within barrels, and asymmetric displacement creates inconsistent tip heights that destroy coplanarity.
Path three: plating damage. Plunger plating is usually gold or a palladium alloy, and friction wears the plating, exposing base metal and raising contact resistance while destabilizing it.
Countermeasures follow.
- Keep contacts in a free state. A test socket must not be compressed or backed against a stop inside the packaging, and the cavity depth must leave adequate axial clearance.
- Restrain lateral motion, do not compress. Use cavity walls that conform to the socket outline to limit lateral movement rather than packing foam down on top.
- Fit a contact-area protective cover. The pin field should carry a protective cover whenever it is not in use, made from a low-shedding material that will not scratch. Remove the cover only at installation.
- Give it a dedicated cavity and dedicated cushioning. Socket cushioning must be independent of the rest of the case so heavy components cannot transmit vibration through the case structure.
- Label by channel group. When multiple sockets ship together, mark each cavity with its channel or product model, so that installation does not mix them and produce incomparable data.
On combined cleanliness and static requirements, test sockets sit in the strictest band. They contact device leads and solder balls directly, so surface particles become a direct source of contact failure, while accumulated static charge can discharge into the device at the moment of contact.
Probes and Elastic Contacts: Deformation, Fatigue, and Coplanarity
Probes and elastic contacts are the component class most likely to fail in a way that cannot be seen.
| Contact Type | Failure Mechanism | Transport-Sensitive Factor | Protection Priority | Inspection Method |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Pogo pin | Spring force decay, barrel sticking | Sustained compression, lateral shock | Free-state packing, lateral restraint | Force sampling, travel check |
| Cantilever probe | Plastic deformation of the beam | Free end compressed | Clearance at the free end, no wall contact | Tip height and coplanarity measurement |
| Elastic conductive elastomer | Permanent compression set, particle migration | Sustained pressure, elevated temperature | Pressure-free packing, avoid heat | Compression set sampling |
| Conductive spring finger | Plastic deformation, contact-face wear | Free end pinched by a stop | Keep in the naturally open position | Contact force and appearance |
| Precision spring | Stress relaxation | Long-term compression | No preload in packaging | Force sampling |
The rule that recurs throughout this table is: do not apply sustained load to an elastic element in the packed state. This runs against the instinct of many packing technicians, who compress parts with foam or hold-down bars so they will not move. For a rigid part that instinct is sound. For an elastic contact it is wrong, because a rigid part's performance does not change with clamping force while an elastic part's performance is defined by its force output, and sustained compression changes that output.
Coplanarity protection is the second theme. Coplanarity is usually destroyed not by single-point deformation but by inconsistent displacement across a group of contacts. Packaging should therefore subject the entire contact array to restraint in the same direction rather than loading some contacts first. In practice, the socket housing carries the support and restraint while the pin array is left suspended and unloaded.
The third theme is cleanliness. Probe tips are extremely small, and a particle only a few microns across can cause a single-point contact failure. Probes therefore should not share a cavity with metal structural parts, because debris generated by metal parts under vibration becomes a direct contamination source. Where they must ship in the same case, use an isolated sealed inner box. General guidance on sealing structures and materials is covered in how to select seal materials and sealing structures.
Thermal Heads and Temperature Chambers: Thermal Interfaces and Condensation
The temperature-control section of a handler includes thermal heads, heater blocks, high-low temperature chambers, and associated seals. These components present a different packaging problem, concentrated in thermal interfaces and condensation.
On thermal interfaces, heat transfer between the thermal head and the device under test depends on the flatness of the mating face and the state of the interface material. Handling impacts create dents or burrs on the mating face, raising local thermal resistance and degrading temperature uniformity. For tests that must hold within a few degrees, a uniformity degradation of a few degrees is already enough to cause misjudgment.
On condensation, parts of a temperature chamber that have been through low-temperature transport condense moisture when they enter a warm, humid environment. Condensation does not damage anything immediately, but it has two consequences. First, trapped moisture corrodes the gaps between seals and metal parts. Second, residual water freezes during subsequent low-temperature testing, affecting sealing and actuation. Worse, once the insulation inside a chamber absorbs moisture, its performance degrades long term and is difficult to restore.
Engineering measures include:
- Fit a protective pad over thermal mating faces. Use a low-shedding, non-scratching soft pad so the mating face never contacts the insert hard.
- Keep chamber interiors dry. Dry the chamber before dispatch, place desiccant inside where appropriate, and mark the exterior with a note that the chamber was dried and the date of treatment.
- Do not leave seals under sustained load. As with elastic contacts, rubber seals take a compression set under long-term load. Keep seals in their natural state during transport, or use removable transport blocks to carry load instead.
- Settle before opening. Components that have traveled cold should settle in the target environment until temperature equalizes before opening, reducing condensation risk. The same principle is central to packaging for extreme temperature environments.
One separate caution: thermal heads usually contain heating elements and temperature sensors, and both are sensitive to electrical connections. If a sensor's compensation leads are pulled during packaging, temperature readings shift, and that shift is often misdiagnosed as sensor failure.
Handling Mechanisms: Nozzles, Grippers, and Vacuum Circuits
The handling mechanism is the most frequently actuated assembly on a handler, and its components are mostly lightweight, high-precision parts with limited shock tolerance.
Nozzles are the classic wear item. The nozzle face must form a reliable seal against the device, so its flatness and roughness matter. Friction in transit scores the face, and scoring breaks the vacuum seal, raising pick failure rate. The second nozzle risk is bore blockage: a single particle or fiber is enough to drop vacuum flow below the critical threshold.
Grippers concentrate risk in the parallelism and surface condition of their gripping faces. Grippers usually hold devices with a parallel closing motion, and a burr or parallelism offset causes device skewing or scratching.
Vacuum circuits risk contamination and leakage. Valve bodies, filters, and tubing in the vacuum path can deform slightly under compression in transit or retain internal contamination, which appears as longer vacuum build time or reduced holding capability.
Packing points:
- Give nozzles their own small cavity, face up or against a protective pad. The nozzle face must not contact hard material, and nozzles must not be stacked against each other.
- Keep grippers in the naturally open position. As with elastic elements, a gripper should not sit closed under load in packaging.
- Plug vacuum ports with cleanroom plugs. Every pneumatic port should be closed during transport to keep particles out.
- Package vacuum filters and valve bodies separately. These contain precision internal structure and should not share a cavity with metal parts.
- Provide separate channels for cables and tubing. Flexible items should not be compressed by the insert, and they must be restrained against whipping.
Nozzles carry one further detail tied directly to cleanliness: a nozzle face that has contacted a device surface may retain flux or organic contamination. Clean it per the supplier's procedure before dispatch and protect it against recontamination during packaging, because residue will cure or attract particles during long storage.
Precision Alignment Systems: Preserving Optical and Motion Datums
Handler alignment accuracy determines whether a device can be placed accurately into the test socket. Alignment hardware includes vision cameras, illumination, XY stages, and screws or linear motors, and the packaging logic here differs from the previous categories: the focus is datum preservation.
The problem with vision cameras is the optical axis. A shift in the relative position of the lens and the camera body moves the imaging centre, and vision algorithms normally work from a calibrated centre, so the shift converts into systematic alignment error. Cameras are extremely vibration-sensitive, particularly the structure that joins lens to sensor.
The problem with motion stages is rails and screws. As with bonder stages, rail raceways indent under shock, and lead screws develop axial clearance change. These damages are nearly invisible at low speed and show up as positioning error once speed increases.
The problem with illumination is heat and fasteners. High-brightness sources usually carry heat dissipation hardware, and fasteners can loosen under vibration, changing illumination uniformity and therefore image-processing thresholds.
Engineering measures:
- Package camera and lens as one unit. If a camera is already assembled with its lens, pack them as a unit rather than separating and shipping them in separate cavities. If separation is unavoidable, cap the interface and secure each part individually.
- Three-point support with face contact for stages. Consistent with general precision motion practice, use statically determinate support so the insert itself does not become a distortion source.
- Add transport blocks to moving axes. For movable slides and Z-axis mechanisms, restrain travel with a block rather than relying on friction or spring pressure.
- Ship calibration data with the case. Include the factory calibration record covering imaging center, alignment offset, and stage repeatability, so it can be compared on arrival.
For general selection guidance on precision measurement and instrument components, see protective transport for laboratory equipment. Handler alignment hardware sits in the high-precision subset of that class.
Insert Compartmentalization: Flexible Layout for High-Mix Low-Volume Work
A distinctive feature of handler spares is high mix, low volume, and frequent changeover. A single machine may need a dozen socket types, several nozzle types, and various sensors and valve bodies. That structure rules out packaging customized for one component only.
The compromise is a modular insert: build the base structure from standard divider frames, then adapt to different components with dedicated locating blocks. Changeover then requires replacing only the locating blocks instead of remachining an entire insert.
| Layout Strategy | Suitable For | Advantage | Limitation | Recommendation |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Fully custom insert | Volume shipment of a single model | Highest locating precision, most stable structure | High changeover cost | Use for high-value single items |
| Modular insert | High mix, low volume | Low changeover cost, high reuse | Locating precision slightly below fully custom | Use for spare parts fleets |
| Divided tray plus outer case | Many small components | Easy individual access inside the clean zone | Not suitable for large items | Use for nozzles and contacts |
| Individual box in a cushioned outer case | Ultra-brittle high-value parts | Best isolation | Consumes volume, more handling steps | Use for probe cards and sockets |
One important rule in modular layouts is to zone by sensitivity, not by size. A common error is grouping components of similar size, which leaves high-sensitivity and low-sensitivity parts sharing one cushioning condition. Instead, group components of similar sensitivity into one zone and apply uniform cushioning parameters to that zone.
A second rule is that cavity labels must match drawing part numbers. In high-mix scenarios, mixing is the largest hidden cost: a socket of the wrong model can make an entire batch of test data unusable. Label each cavity with the part number, quantity, and machine model, and paste the packing list inside the case lid. The cost is low and the payoff is high.
Material Selection Under Combined Cleanliness and Static Constraints
Packaging materials for test sockets and contacts must satisfy cleanliness and static requirements simultaneously, and in material selection the two constraints pull against each other.
| Material Type | Cleanliness Behavior | Static Behavior | Cushioning Behavior | Suitable Layer |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Cross-linked polyethylene | Low shedding, low outgassing | Insulating, needs modification | Medium | Structural support |
| EVA | Low shedding, requires low-outgassing formulation | Insulating, accepts conductive filler | Good | Cushioning |
| Polyurethane | Moderate shedding, some formulations outgas | Available in dissipative grades | Excellent | Cushioning, cleanroom grade required |
| Conductive foam | Shedding depends on substrate | Conductive, good shielding | Good | Contact layer surface |
| Cleanroom-grade silicone | Extremely low shedding, low outgassing | Can be made dissipative | Soft | Contact layer |
| Anti-static bag film | Blocks particles | Static shielding | None | Inner barrier |
The common industrial structure has three layers: outer structural support, middle cushioning, and inner contact. The inner layer demands the most care because it touches sensitive device areas directly. Practical practice is to use a cleanroom-grade material with dissipative performance for the inner layer while avoiding formulations that can release plasticizers. Construction and selection of shielding layers is covered in picking a dissipative shielding case for handler parts.
One caution: dissipative material performance decays with use. Test socket packaging tends to follow a returnable model, and without periodic re-testing the static performance of an insert can fail after repeated cleaning without anyone noticing. Write the re-test interval into the packaging acceptance specification.
If packaging is handled inside a cleanroom, materials should also be wipeable. Wipeability affects not only cleaning effectiveness but whether the cleaning action itself generates particles: rough or open-celled surfaces release debris when wiped, so insert surfaces should be dense and smooth.
Humidity, Condensation, and Cross-Environment Transition
Handler components often travel across climates and cleanliness levels, which makes humidity management a subject in its own right.
Humidity acts through three paths. The first is corrosion of metal parts, including barrels, springs, and structural components. The second is moisture uptake by cleanroom-grade materials followed by release into the case, creating locally high humidity. The third is condensation, especially when a cold-transported part enters a warm environment.
| Scenario | Primary Risk | Management Measure | Note |
|---|---|---|---|
| --- | --- | --- | --- |
| Long sea freight | Moisture accumulation, salt fog | Sealing plus desiccant plus indicator card | Size desiccant for voyage length |
| Air freight | Low pressure, large temperature swing | Pressure equalization valve plus sealed bag | Membrane pore size must match cleanliness class |
| Cold transport then plant entry | Condensation | Settle to equilibrium before opening | Settling time from temperature delta and volume |
| Storage in hot humid regions | Mold, corrosion | Anti-mold packaging plus periodic inspection | Watch organic material formulations |
| Between cleanroom and uncontrolled area | Particle cross-talk | Strip in layers, wipe exterior | Inner barrier must not open in an uncontrolled area |
The standard combination is a sealed rigid case, an inner cleanroom bag, controlled desiccant, and a humidity indicator card. The pressure equalization valve balances differential pressure in transit so the gasket is not distorted. If component cleanliness requirements are high, the valve membrane pore size must match, or the design should switch to a cleanroom bag as the inner barrier with the rigid case managing pressure. For how equalization hardware works, see matching an equalization valve to a sealed case.
Two common desiccant errors deserve mention. One is scattering desiccant loose inside the case, where granules can roll into a cavity. The other is adding it by habit, which may be insufficient or excessive — over-drying is unfavorable for some elastomers. Correct practice is to enclose desiccant in a breathable cleanroom bag, secure it away from sensitive components, and size the quantity from the internal volume, the length of the journey, and the humidity target.
Case Load Design From Bench Parts to Gantry Modules
Handler spares span an enormous weight range, which imposes layered requirements on case structure.
| Weight Range | Typical Components | Case Form | Handling Method | Structural Priority |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Under 1 kg | Nozzles, contacts, small sensors | Carrying case, divided tray | Hand carry | Light, easy clean-zone access |
| 1 – 10 kg | Test sockets, camera modules, valve groups | Carrying case or wheeled case | Hand carry or cart | Insert strength first |
| 10 – 40 kg | Thermal heads, motion stages | Wheeled case, pallet case | Cart or two-person lift | Lifting points, reinforcement |
| 40 – 120 kg | Temperature chambers, gantry modules | Pallet case, frame case | Forklift or hoist | Load-bearing base, lift markings |
| Over 120 kg | Large handler structural parts | Frame case or timber crate | Hoisting | Structural calculation and testing |
Three structural points stand out. First, lifting points and load-bearing points must be clearly marked, so that no forklift tine can be shoved under an arbitrary spot on the base and drive the load into the contents. Second, heavy case inserts should prioritize structural support with cushioning as a secondary role, because a large mass carries high inertia and an overly soft cushion will bottom out. Third, heavy cases must be checked for stacking and tipping, particularly for the stack height and securing method used in sea freight containers.
The opposite applies to light components. The case can be simplified, but ease of access and wipeability matter more. A common error is giving nozzles a heavy case, which then becomes awkward to open and handle inside the clean zone and actually increases the chance of impact. For light items the packaging goal is light, clean, and fast — the opposite of heavy items.
Packaging as a Storage Unit: The Spare Parts Inventory View
Handler spares are usually held as plant inventory, which makes packaging a storage unit as well. This view introduces several additional requirements.
First, stacking stability. Spare cases may be stacked three or more high on shelving, so the case needs stackable geometry such as recessed tops and reinforced edges, and the insert must carry the weight above without passing it to contents. This is the same mechanics as transport stacking but sustained far longer, which puts compression set of the insert in focus.
Second, label legibility. Fast picking in a warehouse depends on identification. Labels should carry component name, part number, applicable machine model, quantity, cleanliness class requirement, and handling instructions after opening. They should be abrasion-resistant, non-detaching, and fiber-free.
Third, environmental control. Long storage in an uncontrolled warehouse cannot rely solely on desiccant inside the packaging. Sensitive items such as elastic contacts and probe cards are better held in a dry cabinet or a controlled area.
Fourth, managing partial use. When only part of a case is consumed, the remainder must be resealed. Packaging should therefore support resealing, for example through a reopenable sealing feature or supplied spare sealing bags. Otherwise the floor will close it with tape, destroying the original cleanliness and humidity barrier.
Fifth, shelf life management. Desiccant and some cleanroom-grade materials have storage limits. Provide a field on the case label for recording desiccant replacement and insert inspection dates, turning maintenance into an executable action rather than a verbal agreement.
Transport Verification and Offline Re-Measurement
Verification serves one purpose: to show that packaging leaves key component performance untouched under the transport conditions actually expected. For handler components, the plan should cover mechanical, environmental, and functional aspects.
| Checkpoint | Cited Method | What This Proves | Release Criterion | Re-Measure Target |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Drop, free-fall | ISTA procedures plus GB/T 4857 | Handling and transfer drops are survivable | Insert unbroken, no contact takes a set | Socket contact force |
| Random vibration | ISTA procedures plus ASTM D4169 | Road and air excitation is survivable | No creep, no fastener movement | Tip coplanarity |
| Static stacking | GB/T 4857 | Warehouse and transit stacks do not crush the insert | Case stays stable, insert set inside allowance | Insert thickness |
| Temperature and humidity cycles | MIL-STD-810H method clauses | Climate swings leave no residue or growth | No dew, no rust, no mould | Sealing faces |
| Low ambient pressure | MIL-STD-810H method clauses | Air freight does not distort the case | Gasket undistorted, equalizer open | Case seal |
| Post-test cleanliness | In-house work instruction | The packaging releases no debris at all | Wipe and particle counts inside limits | Interior surfaces |
| Post-test ESD | In-house work instruction | Dissipative behaviour has not drifted | Surface resistance inside band | Insert contact layer |
| Offline performance | In-house work instruction | The part is still within specification | Force, coplanarity and imaging centre pass | Socket, probe card, camera |
One boundary should be clear from the outset: MIL-STD-810H is quoted here purely as a source of environmental test procedures, and that reference does not amount to a military certification of a packaging product or design. For export programs, the distribution cycle simulation logic of ASTM D4169 is useful because it combines multiple transport stages into a continuous test sequence that better approximates real distribution. See how to use distribution cycle simulation testing and national transport packaging test practice.
The offline re-measurement row is the one most often skipped, and the most valuable. It means measuring key performance independently after transport or testing, before installation. For sockets and contacts, at minimum sample contact force, tip coplanarity, and contact-resistance distribution. For vision and stage components, measure imaging center and repeatability. Only when re-measurement passes does the packaging design meet its purpose.
When JUNZHJIA handles handler spare parts packaging programs, the usual route is to model and trial-fit inserts against the customer's component list, sensitivity classification, and cleanliness requirements, with contacts and structural parts zoned separately. For high-mix low-volume scenarios, a modular insert design with locating block drawings can be supplied so the customer can perform changeovers in house. Volume supply and OEM or ODM programs can be scheduled to the project's cadence, and insert material paperwork plus test records can be supplied on request.
Frequently Asked Questions
Q: Why are low-cost parts like test sockets and nozzles the design focus of a handler component case?
A: Because their acceptance criteria are stricter. A structural part's criterion is usually whether it has broken or visibly deformed, which is a loose criterion and easy to observe. A test socket or nozzle is judged by contact force, coplanarity, and face flatness, with allowable deviation in the micron range, and it can fail while appearing completely normal. If a socket's contact force drops by a few percent overall, no visual inspection will reveal it, but the test data will show rising contact resistance on some channels. If a nozzle face picks up fine scoring, pick failure rate creeps upward. The diagnostic cost of these hidden failures is high, because engineers suspect the test program, probe wear, and sensors before they suspect packaging. When designing a case, therefore, put the hardest-to-protect components first and give them dedicated cavities, dedicated restraint, and dedicated cushioning rather than sharing one cushioning system with heavy structural parts. The high replacement frequency of low-cost parts also means their cumulative purchase volume is substantial, and the total cost of hidden failures often exceeds the unit price by a wide margin.
Q: Why must a test socket never sit under compression inside its packaging?
A: Because socket performance is defined by the force output of its internal elastic contacts, and elastic elements undergo stress relaxation and permanent set under sustained compression. Inside a pogo pin is a spring, a barrel, and a plunger, and the factory screens and matches these so that contact force across the full array stays in a narrow band. If packaging presses down with foam or a hold-down bar, those springs remain compressed for the tens of hours of transport and the force output drops across the board. The drop may be only a few percent, but for contact-resistance-sensitive high-frequency testing or small solder ball devices that is already enough to skew measurements. Beyond force, sustained compression changes the consistency of plunger position within the barrels and destroys coplanarity. The correct approach leaves the socket in a free state and uses cavity walls conforming to its outline to limit lateral swing, with only the necessary axial clearance, substituting geometric restraint for pressure restraint. The pin field should also carry a low-shedding, non-scratching protective cover removed only at installation.
Q: Why does coplanarity become a focal point of transport damage for probes and pogo pins?
A: Because measuring a multi-contact device depends on all contacts engaging at the same moment. A ball-array package may present hundreds to over a thousand solder balls, and socket coplanarity determines whether all contacts establish electrical connection simultaneously. Coplanarity is usually destroyed not by single-point deformation but by inconsistent displacement across a group of contacts: as soon as one subset loads and displaces before the rest, overall consistency is lost. Transport shock is an ideal generator of exactly this condition, and lateral shock in particular loads the contacts on the leading side first. The failure shows up as partial contact failure, with failed positions varying by device lot and loading attitude, which makes localization difficult. The protective logic is therefore to subject the whole contact array to restraint in the same direction, assigning support and restraint to the socket housing while leaving the pin array suspended and unloaded. Also avoid sharing a cavity between metal structural parts and probes, because metal debris landing on a tip creates single-point contamination.
Q: Why does packaging for thermal heads and temperature chamber parts require special attention to condensation?
A: Condensation arises from the difference between a cold component and the dew point of a warm humid environment, and its consequences go beyond a damp surface. First, moisture trapped in the gaps between seals and metal parts causes corrosion, and those gaps are hard to inspect. Second, residual water freezes during subsequent low-temperature testing, affecting sealing performance and mechanical actuation. Third, once chamber insulation absorbs moisture its thermal performance degrades long term and is difficult to restore, effectively shortening service life. The key management measure is to make settling a mandatory step: after cold transport, let the case settle in a buffer zone at the target environment until the interior temperature approaches the installation environment, then open it. Settling time should be estimated from the temperature differential and the thermal mass of the case; a larger differential and thicker case require longer. The chamber should also be dried before dispatch, with desiccant placed inside where appropriate and the treatment date marked on the exterior. Thermal mating faces should carry a low-shedding, non-scratching soft pad so hard contact cannot create dents that raise thermal resistance.
Q: What details in nozzle packaging are most often overlooked?
A: Face protection and bore blockage. A nozzle face must form a reliable seal against the device, and its flatness and roughness directly affect vacuum sealing. Friction in transit scores the face, and once the seal is broken the pick failure rate rises. The nozzle face must therefore never contact hard material and nozzles must never be stacked against each other; the correct approach is a dedicated small cavity with the face up or against a dedicated protective pad. Bore blockage is equally common: a particle a few microns across or a single fiber can drop vacuum flow below the critical threshold. Every pneumatic port should therefore be closed with a cleanroom plug during transport, made of low-shedding elastomer rather than a fibrous cotton plug. One further cleanliness-related point: a nozzle face that has contacted a device may retain flux or organic contamination, so clean it per the supplier's procedure before dispatch and protect it against recontamination. Otherwise the residue will cure or attract particles during long storage and become a new contamination source.
Q: Why is a modular insert recommended over a fully custom insert for handler spare parts cases?
A: It depends on the batch structure. A fully custom insert offers the highest locating precision and the most stable structure, but it is optimized for a single model, and any changeover requires redesign and remachining at high cost and long lead time. The reality of handler spares is high mix, low volume, and frequent changeover: a single machine may need a dozen socket types, several nozzle types, and various sensors and valve bodies, and under that structure the changeover cost of custom inserts accumulates quickly. A modular insert builds the base structure from standard divider frames and adapts to different components with dedicated locating blocks, so a changeover costs only a new locating block, which cuts changeover cost and raises reuse. The trade-off is slightly lower locating precision than a fully custom insert, which is adequate for most spare parts transport. In practice the two can be combined: use fully custom inserts for high-value, ultra-precision single items and modular inserts for the many small items held in stock. Under either approach, zone by sensitivity rather than by size so that high- and low-sensitivity parts never share cushioning conditions.
Q: What additional requirements come from treating packaging as a storage unit?
A: At least five. First, stacking stability: spare cases may be stacked three or more high on shelving, so the case needs stackable geometry and the insert must carry the weight above without passing it to contents, sustained far longer than in transport, which puts insert compression set in focus. Second, label legibility: warehouse picking depends on fast identification, so labels should carry part number, applicable machine model, quantity, and cleanliness requirement while being abrasion-resistant, non-detaching, and fiber-free. Third, environmental control: long storage in an uncontrolled warehouse cannot rely on the desiccant inside the packaging alone, and sensitive items such as elastic contacts and probe cards are better held in a dry cabinet or controlled area. Fourth, managing partial use: packaging must support resealing, otherwise the floor will close it with tape and destroy the cleanliness and humidity barrier. Fifth, shelf life management: desiccant and some cleanroom-grade materials have storage limits, so a field for recording replacement and inspection dates on the case label turns maintenance into an executable action.
Q: Why is offline re-measurement needed after transport verification?
A: Because transport verification answers whether the packaging survived the test, while offline re-measurement answers whether the component is still acceptable, and these are different questions. The dominant failure mode for handler components is performance drift. A package may come through a test with an intact exterior and an unbroken insert while contact force has dropped across the board, or tip coplanarity has moved outside the allowable range. If verification judges only appearance and package condition, such problems are recorded as passes and only surface after installation when data turns abnormal. The correct practice measures key performance independently after transport or testing and before installation: sample contact force, tip coplanarity, and contact-resistance distribution for sockets and contacts; measure imaging center and repeatability for vision and stage components. Only when re-measurement passes has the packaging design met its purpose. For volume programs, write the re-measurement items and acceptance limits into the packaging acceptance specification so records are traceable and any deviation can be attributed either to a packaging design issue or to a single abnormal shipment.
Conclusion and Related Reading
The design difficulty of a semiconductor test handler component case is that it protects a class of components whose failure leaves no visible trace. Contact force, coplanarity, face flatness, and imaging center determine whether test data can be trusted, not whether the machine will run. Starting from that understanding produces several conclusions that differ from ordinary packaging practice: elastic elements must not be compressed, a test socket must not share a cavity with structural parts, probes must not ship in the same case as metal parts, and cold components must settle before opening. Individually none of these is complicated, but together they form a complete protection chain, and a single missing link leaves an untraceable deviation in the test data. For an assembly and test house, the worthwhile investment is not thicker case walls but more accurate sensitivity classification and stricter acceptance re-measurement. For spare parts suppliers and second-hand equipment dealers, packaging that withstands re-measurement is the most direct evidence of delivery quality.
Related Reading