

Spindles and drafting components combine three sensitive traits at once: high rotational speed, tight geometry, and aggressive corrosion behaviour. The job of a transport case here is not to survive a big drop, but to suppress micro-vibration, block moisture, and make sure no two steel parts ever touch. A cotton ring-spinning spindle shaft is normally held to a radial runout in the range of 0.01 to 0.02 mm, and that tolerance is created piece by piece through grinding and dynamic balancing. A drop from half a metre can destroy it in one instant. Rubber cots are attacked by ozone, ultraviolet light, mineral oil and long-term concentrated load. A chromium-plated fluted roller that picks up a scratch from a neighbouring steel part will keep snagging fibres and generating neps for the rest of its service life. A well-designed spinning frame case therefore has to deliver three outcomes at the same time: independent constraint of every rigid part in its own position, a controlled chemical environment inside the case using vapour-phase corrosion inhibitor and desiccant, and a vibration spectrum that is flattened by case wall stiffness plus an energy-absorbing liner.
Spinning mills face the same problem whenever they relocate equipment, move a used ring frame to another site, or take delivery of components from an OEM. Component counts are enormous, with a single ring frame carrying anywhere from 500 to 1200 spindles, while individual part value is high. Loose packing with generic fill means that receiving and re-inspection labour often costs more than the packing itself. Worse, a bent spindle, a dented cot, or a rust patch on a roller translates into a repair cycle measured in weeks, which directly disrupts the start-up plan. This article works from damage mechanisms outward: liner partitioning logic, material selection, corrosion and electrostatic control, case structure, and test verification, closing with a practical packing procedure and a list of information to supply when requesting a quotation. If you need the fundamentals of case and liner design first, see the custom foam insert design guide and the case foam material comparison.
Table of Contents
- 1. Why spindles and drafting parts are the most sensitive items on a spinning frame
- 2. Spindle damage chain: from bending deformation to fretting wear
- 3. Drafting components: rollers, cots, aprons and cradles each have a weak point
- 4. Liner partitioning: moving the machine layout into the case
- 5. Corrosion protection: how VCI film, desiccant and barrier bags work together
- 6. Static control and cleanliness: quantifying the soft risks
- 7. Case structure: ingress protection, wall stiffness and stacking strength
- 8. Test references: choosing between ISTA 3A, ASTM D4169 and GB/T 4857
- 9. Using MIL-STD-810H correctly: a test reference, not a military certification
- 10. Packing procedure and receiving inspection checklist
- 11. Common mistakes and the cost of rework
- 12. What to send us for a quotation and how customization runs
- Frequently Asked Questions
- Conclusion and Further Reading
1. Why spindles and drafting parts are the most sensitive items on a spinning frame
On ring spinning and compact spinning machines, spindle speeds typically run between 14000 and 19000 rpm, with some high-speed models running faster still. The spindle shaft is a slender cantilever whose thin end may be only a few millimetres in diameter, held stable by an elastic bearing and an oil film damper inside the bolster. That combination of elastic support and high rotational speed makes the shaft extremely sensitive to initial bending. Any lateral load that pushes it past the elastic limit leaves permanent deformation, and permanent deformation amplifies into spindle vibration and yarn tension fluctuation once the machine runs. The drafting zone is sensitive in a different way. Six to eight rollers form the drafting pair, rubber cots cover the top rollers, the nip gauge is set according to the staple length of the fibre being spun, and the cradle applies a stable pressure. The tolerance system in a drafting zone is cumulative: every individual part can be inside its own tolerance while the assembly still produces poor yarn because one cot has a circularity error or the cradle pressure deviates.
| Component | Key geometry or property (typical) | Primary transport failure mode | Packing constraint |
|---|---|---|---|
| --- | --- | --- | --- |
| Spindle shaft | Radial runout 0.01 to 0.02 mm, slender cantilever | Bending, surface nicks, cone-seat corrosion | One pocket per spindle, zero contact with steel |
| Spindle bolster with elastic bearing | Oil bath damping, precision mating faces | Fretting wear, oil seal extrusion, rust | Fixed in designed attitude, interface capped |
| Fluted drafting roller | Chromium plating a few to low tens of microns | Plating scratches, groove edge collapse | Semicircular cradle slot plus end caps |
| Rubber cot | Cover hardness roughly 63 to 70 Shore A | Cover indentation, ageing cracks, oil stains | Dark, cool, relaxed support, no point loads |
| Apron and tape | Thin-wall NBR or polyurethane | Creases, permanent set, static dust attraction | Flat suspension or large-radius roll, antistatic liner |
| Cradle and weighting assembly | Spring force spread usually held within plus or minus 5 percent | Loss of preload, lever arm distortion | Released before packing, individual pocket |
Treat this table as the basis for splitting a shipment into cases, and it answers the most practical question of all: how many cases a relocation project needs, which parts may share a case, and which parts must be separated completely.
2. Spindle damage chain: from bending deformation to fretting wear
Spindle damage during transport rarely shows up as a clean break. It is a progressive chain. An early impact creates a tiny scratch or a local plastic zone, transport vibration concentrates stress at that scratch and triggers fretting, moisture then reaches the mating face and starts corrosion, and the whole sequence finally appears at commissioning as excessive spindle vibration and rising yarn breakage. Every link in that chain can be cut at the packing stage.
The first link is bending. Acceptable bending is measured as radial runout, and once a shaft exceeds the factory criterion it cannot be recovered by straightening, because straightening itself introduces residual stress. The proven approach is to insert each spindle into its own liner pocket, with a pocket depth covering at least two thirds of shaft length and an axial stop formed at the whorl. Lateral load is then carried by the liner wall instead of by the shaft. The second link is fretting wear, concentrated at the mating faces between bolster and whorl. Sustained high-frequency, low-amplitude vibration during transport grinds the two faces against each other and destroys the original interference or clearance fit. The countermeasure is a layer of medium-resilience closed-cell foam between liner and bolster, so vibration energy dissipates in the foam rather than at the mating face.
The third link is corrosion. The ground outer surface of the shaft and the cone seat at the base are low-roughness, highly active surfaces. In a case whose internal relative humidity exceeds 60 percent, spot oxidation can appear within days. A spindle is therefore both a precision part and a corrosion-prone part, which aligns with the general approach described in our guide to protection concepts for textile machinery parts, except that the runout class of a spindle is stricter and the protection level must be raised accordingly.
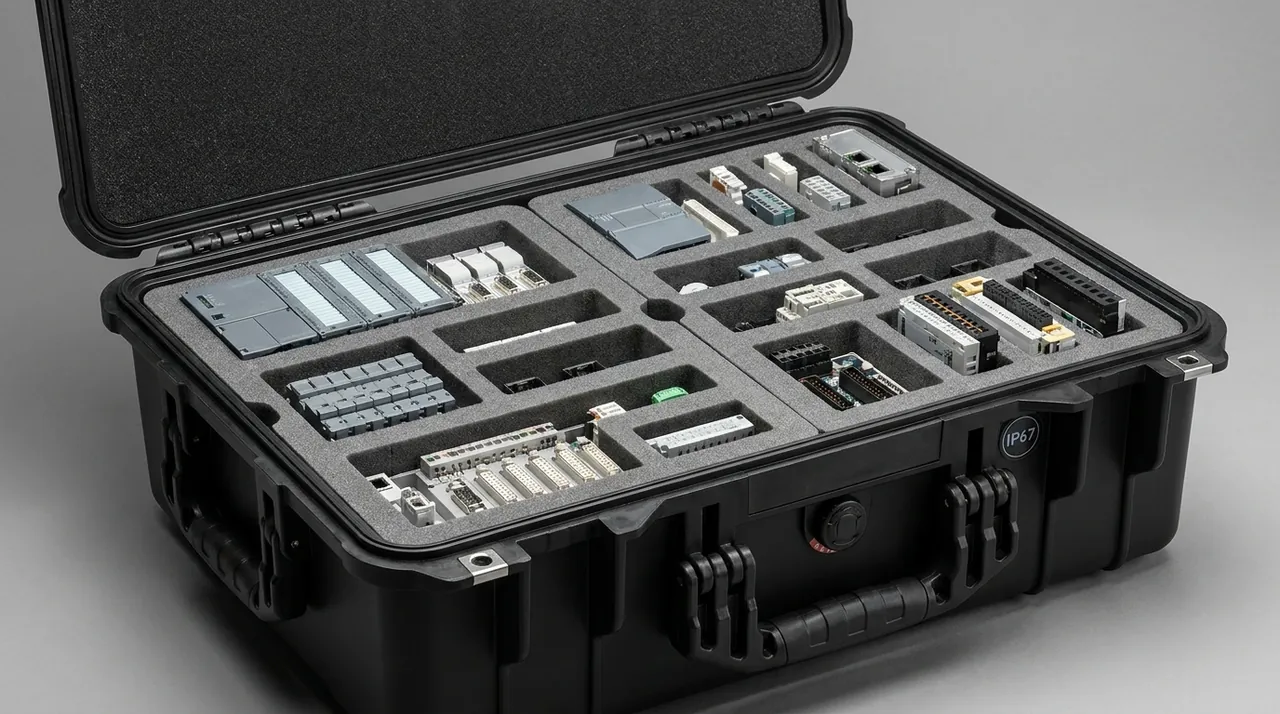
Practical criterion: after a spindle case completes one simulated transport test, re-measure radial runout on every spindle. If even one exceeds the factory criterion, the constraint scheme needs redesign rather than simply adding more foam.
3. Drafting components: rollers, cots, aprons and cradles each have a weak point
The difficulty with drafting parts is that one case holds items with completely different physical behaviour. A fluted roller is a rigid steel part that fears scratches. A rubber cot is an elastic covered part that fears deformation and ageing. An apron is a thin-wall elastic part that fears creases. A cradle is a spring mechanism that fears loss of preload. Forcing one liner concept onto all of them guarantees a compromise somewhere.
For fluted rollers the key idea is to replace line contact with surface contact. The chromium layer and the groove edges are thin, and any point load can leave a mark. The recommended approach is to machine a semicircular long slot in the liner at the roller diameter so the whole roller rests on the slot as a surface contact, then add soft end caps to protect the journals. When rollers are stacked in layers, place a divider board between layers with matching relief slots so that the weight of the upper layer never lands on the groove edges of the layer below. Roller storage attitude also matters: a slender part supported only at both ends with an unsupported middle will slowly take a bend.
Rubber cots are the most underestimated item. Cover failure is not a drop problem, it is a compression and ageing problem. Long-term concentrated load leaves an indentation in the cover that cannot be recovered, and once installed the machine shows a local change in nip gauge. Ultraviolet light and ozone break rubber molecular chains and cause cracking, while mineral oil, grease and some solvents cause swelling. A cot case therefore needs four properties: it blocks light through an opaque shell or a light-blocking inner bag, it avoids heat with a storage recommendation of 15 to 25 degrees Celsius, it avoids oil by using liner materials with no tendency to migrate plasticizer, and it never applies a point load, using instead a broad relaxed support or a suspended pocket. For extended storage, place desiccant inside and refresh it periodically, keeping relative humidity between about 50 and 65 percent.
Aprons and tapes are thin-wall parts whose main enemy is the crease. Winding them into a large-radius roll and fixing them flat is far better for dimensional stability than folding and laying flat. These parts carry a second, hidden risk: rubber surfaces become charged through friction and then attract airborne fly and dust. An antistatic liner, or one with a controlled surface resistivity, is therefore preferable. The material selection method behind this is described in our article on ESD shielding cases for static-sensitive parts.
Cradles and weighting assemblies must be depressurized before packing, otherwise the springs sit under preload for weeks and lose pressure consistency. The lever arm of a cradle is usually a thin-wall casting or sheet metal part that distorts in angle after an impact, so it needs an individual pocket and must not be mixed with rollers. Any part belonging to a kinematic pair is best delivered as a matched numbered set so that components from different spindle positions are never interchanged.
4. Liner partitioning: moving the machine layout into the case
The biggest difference between a spinning frame case and a general-purpose toolbox is that it is often a miniature of the whole machine being relocated. Shipping the spindles of a 1000-spindle ring frame at 20 spindles per case means 50 cases, and the numbering inside each case must be traceable back to the spindle position on the machine. Liner partitioning therefore has to satisfy three requirements at once: individual constraint, traceable numbering, and unobstructed removal.
There are two practical routes to individual constraint. The first is a locating pocket, suitable for spindle shafts and small-diameter shafts, with a bore clearance of 0.2 to 0.5 mm per side over the part diameter and a depth covering at least two thirds of part length. The second is a cradle slot plus stop blocks, suitable for rollers and levers, with slot width set to the local maximum diameter and stop blocks at both ends to limit axial travel. Both routes exclude the stacked-constraint idea in which one part presses on another, because the weight of an upper part must never become the retaining force for a lower part.
The usual way to achieve traceable numbering is to laser-mark or hot-stamp position ranges directly onto the liner surface, or to fit a nameplate inside the lid stating case number, part name, quantity, machine identity and position range. On relocation projects delivered in several batches, this alone compresses receiving time considerably. If your part mix is complex and several items must share one case, the logic for combining variable and fixed zones is explained in the guide to the removable divider system.
Unobstructed removal requires finger reliefs or lifting notches. The common design leaves a 20 to 30 mm wide relief beside each pocket so a gloved hand can extract the part, and the liner itself should be fitted with 1 to 3 mm of interference against the case wall so the whole block cannot shift during transport.
5. Corrosion protection: how VCI film, desiccant and barrier bags work together
Protecting spindles and rollers from rust cannot be closed with a single measure. A complete system has three layers: a vapour-phase corrosion inhibitor that creates a protective atmosphere close to the metal, a desiccant that holds internal relative humidity down, and a barrier bag that slows the rate of moisture exchange. Their roles are not interchangeable. Desiccant cannot replace VCI, and VCI cannot replace the barrier.
VCI material selection must account for the metals present. Spindle shafts, whorls and bolsters may involve different steel grades and different surface finishes, including ground surfaces, black oxide surfaces and plated surfaces, so a multi-metal VCI material effective on both carbon and alloy steel should be chosen. Before packing, confirm that no acidic cleaning residue remains on the surface. A VCI film does not need to be wrapped tightly against the part; close contact is unnecessary and can actually cause abrasion under vibration.
Desiccant quantity is estimated from free volume inside the case, the moisture vapour transmission rate of the packaging materials, the transport duration and the climate of the destination region. As a rule of thumb, for a 30-day transport cycle inside a barrier bag of moderate transmission rate, size the adsorbent type desiccant to the free volume per cubic metre and add a humidity indicator card next to the humidity-sensitive parts so that condition can be judged quickly at opening. Note that more desiccant is not better. In a case containing grease or rubber parts, excessive drying accelerates moisture loss and shrinkage in some rubber compounds, so the humidity target for cot cases should be set separately from that for all-steel cases.
| Protection layer | Function | Typical materials | Common misuse |
|---|---|---|---|
| --- | --- | --- | --- |
| Vapour phase inhibitor layer | Creates an inhibiting atmosphere at the metal surface | Multi-metal VCI film, VCI paper | Wrapping tightly against the part and causing abrasion |
| Humidity control layer | Holds internal relative humidity down | Adsorbent desiccant plus indicator card | Assuming desiccant replaces VCI |
| Barrier layer | Reduces moisture exchange rate | Aluminium composite bag, high-barrier PE bag | Poor sealing renders the barrier useless |
| Cushion layer | Dissipates vibration and impact energy | Closed-cell foam, moulded EVA liner | Open-cell sponge that absorbs moisture and becomes a rust source |
Seal quality on the barrier bag determines whether the whole system works. Heat-seal width, sealing temperature and whether to draw vacuum all depend on the part mix. Cases containing rubber parts should not be deeply evacuated, because the rubber can be compressed into a permanent set.
6. Static control and cleanliness: quantifying the soft risks
A spinning mill is inherently a static-sensitive environment, and airborne fly, short fibres and dust will cling to cots and aprons once a charge builds up, producing accumulation in the drafting zone. During transport there are two main static sources: contact electrification as the foam liner rubs repeatedly against part surfaces under vibration, and the fact that the case material itself is an insulator, so charge has nowhere to drain. For cots and aprons with cleanliness requirements, choose a liner with controlled surface resistivity and provide a simple drain path inside the case.
On cleanliness class, spindles and drafting parts are not semiconductor-grade items, but fibrous dust, paper debris and ink residue should still be excluded. What is easily overlooked is the particle generation of the packaging auxiliaries themselves: ordinary corrugated board, unfinished foam edges and printing inks can all become sources. For precision ground surfaces, use a non-shedding closed-cell material as the direct contact layer and wipe the part surface with a nonwoven cloth before packing.
When a part needs both antistatic behaviour and cushioning, material selection has to balance surface resistivity against energy absorption. High-resilience materials tend to have high surface resistance, and adding conductive filler such as carbon black changes the mechanical behaviour of the foam. The safer route is a layered design: a conductive or antistatic layer handles draining and clean contact, a high-resilience layer handles energy absorption, and a thin adhesive film bonds the two.
7. Case structure: ingress protection, wall stiffness and stacking strength
Case structure depends on three variables: unit weight, whether the shipment goes by sea, and whether cases will be stacked long term. In typical specifications, a spindle case weighs between 20 and 60 kg, while a drafting component case containing rollers may reach 60 to 120 kg. Weight determines whether you choose an injection-moulded hard case, a rotomoulded case, or a plywood crate with a moulded liner.
Where moisture resistance, rain protection and repeated reuse matter, injection-moulded or rotomoulded hard cases are stronger choices. Sealing performance can be defined against IEC 60529 or GB/T 4208, with common configurations in the IP65 to IP67 range, and a pressure equalization valve handles the differential created by temperature swings. For heavy, high-count, single-shipment projects, a plywood or steel-frame crate with a moulded liner is usually more economical, but wall deflection under stacking load must be solved. Insufficient wall stiffness first shows up as the liner block sinking, and then as part-to-part contact.
| Structure option | Typical weight range | Advantages | Risk points |
|---|---|---|---|
| --- | --- | --- | --- |
| Injection-moulded hard case plus moulded liner | 10 to 50 kg | Good sealing, reusable, uniform appearance | Size limited by tooling, oversize parts need joining |
| Rotomoulded case with internal frame | 40 to 120 kg | High impact resistance, large sizes possible | Higher tare weight, feet must carry stacking load |
| Plywood crate with liner | 60 to 300 kg | Flexible dimensions, controllable cost | Moisture protection depends on liner and barrier bag |
| Steel frame timber crate | Above 200 kg | High load capacity, suitable for lifting | Requires anti-corrosion treatment to avoid contact rust |
Stacking strength should be calculated against the most severe condition in the transport chain, including number of tiers, stacking duration, and whether high temperature and high humidity are involved. Heat inside a sea container softens case materials and increases the compression set of liners, which must be assessed in advance on long-cycle projects.
8. Test references: choosing between ISTA 3A, ASTM D4169 and GB/T 4857
Packing schemes cannot be validated by how sturdy they look. Three commonly used routes have different scopes. ISTA 3A addresses single parcels shipped through parcel networks and covers drop, vibration, compression and random vibration in combination. ASTM D4169 is a performance test practice for distribution cycles that lets you tailor the test sequence and assurance level to actual hazards. The GB/T 4857 series provides basic test methods for transport packages in China, covering vibration, impact and stacking as separate tests. For export projects, ASTM D4169 or ISTA 3A is usually the primary reference, while domestic projects may combine the sub-tests of GB/T 4857.
| Test reference | Application | Main test items | Pass and fail logic |
|---|---|---|---|
| --- | --- | --- | --- |
| ISTA 3A | Single parcel shipment | Conditioning, drop, random vibration, compression | No functional damage to package or contents |
| ASTM D4169 | Customized distribution cycle | Sequence selected from shock, vibration, compression | Damage allowance set by assurance level |
| GB/T 4857 series | Domestic transport packages | Vibration, impact, stacking as separate tests | Sub-test judgement plus functional re-check |
Judgement must return to whether the part still works, not whether the case broke. For spindles and drafting parts, functional re-check includes re-measuring spindle radial runout, inspecting roller surfaces and groove edges, checking cot covers for indentations, verifying cradle spring preload, and confirming no fastener has loosened. Post-test data is best compared against the batch's outgoing data and filed as input for the next packaging revision.
For reusable returnable cases, establish a periodic inspection regime covering seal ageing, hinge and latch wear, and liner compression set. The method behind case life assessment and replacement criteria is described in our article on protective case service life.
9. Using MIL-STD-810H correctly: a test reference, not a military certification
In documentation for spinning accessories and textile machinery components, MIL-STD-810H is frequently presented as a military certification, which is inaccurate. MIL-STD-810H is a collection of environmental test methods and engineering guidance. It specifies how to perform tests for temperature, humidity, vibration, shock, fungus and salt fog, rather than certifying a product itself. The correct way to cite it in civil industrial packaging is as a library of environmental test methods: use its vibration methods to shape sine and random vibration profiles, its temperature and humidity methods to define hot and humid storage conditions, and its shock methods to define drop attitude and magnitude.
A rigorous validation report should therefore state that vibration and temperature-humidity testing was carried out with reference to the relevant MIL-STD-810H methods, and that this reference does not constitute any military certification. Conversely, if a buyer sees a supplier claiming "military standard certification" on the basis of MIL-STD-810H, the supplier should be asked to separate a test method reference from a qualification certificate.
In the spinning context, MIL-STD-810H adds value in two ways. First, it supplies mature high-temperature and high-humidity cycling and random vibration profiles that help define combined sea and road transport conditions. Second, it offers fungus and salt fog test concepts for assessing corrosion risk in steel parts stored long term in humid coastal areas. The sealing protection level of the case itself should still be expressed against IEC 60529 or GB/T 4208 and never mixed up with MIL-STD-810H.
10. Packing procedure and receiving inspection checklist
Turning the design into shop-floor practice requires an executable procedure. The following is a packing procedure for spindles and drafting parts that can be trimmed to the actual part mix.
Before packing. Confirm the parts have been cleaned, dried and de-rusted. Apply a thin anti-rust oil film or VCI material to ground surfaces. Verify part numbers, spindle position numbers and quantities against the shipment list. Check that liner pockets and slot widths match the parts, and never accept a fit simply because the part goes in.
During packing. Place parts one by one into liner pockets, never stacked. Lay rollers into long semicircular slots, fit end caps, and tighten stop blocks. Support cots in a relaxed or suspended pocket with no concentrated load. Add desiccant and a humidity indicator card, seal the barrier bag, and inspect the heat seal line. Check the lid gasket and pressure equalization valve, then close the case and confirm latches share the load evenly.
After packing. Weigh and label every case, and apply pictorial markings such as this way up, keep dry, and do not roll in line with GB/T 191. Build a case-to-part cross-reference table. Carry out sampling or full inspection as planned.
Receiving inspection. Start with the outer case for damage, water ingress, deformation and any tilt indicator that has triggered. Then inspect the interior for humidity indicator status, VCI film integrity and liner displacement. Finally re-check each part functionally: radial runout for every spindle, plating and groove condition for rollers, cover condition for cots, spring and lever geometry for cradles. Acceptance criteria and sampling plans should be agreed in the contract; the method for setting sampling level and decision rules is described in our article on custom case acceptance and AQL sampling.
11. Common mistakes and the cost of rework
The following mistakes recur in spinning equipment relocation projects, and all of them are expensive.
Mistake one: mixed loading. Putting spindles in the same case as wrenches, bolts and bearings. The loose steel parts become hammers under vibration, and shaft outer surfaces and whorl edges take the hit. Separate hardware into its own case.
Mistake two: open-cell sponge as cushioning. Open-cell sponge absorbs moisture and becomes a corrosion source, and its resilience decays quickly. Spinning components call for closed-cell foam or moulded EVA.
Mistake three: vacuum packing cots. Deep vacuum compresses the cover into a permanent set, and in some rubber compounds vacuum combined with elevated temperature accelerates plasticizer migration. Cases with rubber components should stay at ambient or slight negative pressure.
Mistake four: accepting a shipment because the count matches. A correct count does not prove functional condition. Spindle runout must be re-measured, roller plating must be inspected, cot covers must be examined. Otherwise the defect surfaces after installation as rising yarn breakage, and troubleshooting then costs far more than opening a case at goods-in.
Mistake five: ignoring long-term compression set of the liner. After one long sea shipment a foam liner may lose 10 to 20 percent of its thickness as a typical experience value, so the constraint fails on the second trip. Returnable cases should treat liners as consumables with a scheduled replacement interval.
On rework cost: a bent spindle is rarely economic to repair and is normally replaced. A scratched roller must be re-ground and re-plated, which changes diameter tolerance. A cot indentation usually requires re-grinding and may fall below the minimum permissible diameter, effectively scrapping the part. A distorted cradle lever needs dedicated tooling to correct. Taken together, a single shipment with defects typically costs several times more than upgrading the entire packaging scheme.
12. What to send us for a quotation and how customization runs
To get an executable proposal rather than a generic price, include the following when requesting a quotation: part list with material, net weight, envelope dimensions and drawings; description of critical surfaces such as ground, plated, rubber-covered or mating faces; planned load per case and target case weight; transport mode and route covering road, sea or air, number of transfers and whether long-term stacking applies; climate characteristics of the destination; whether reusable construction and a sealing class are required; whether traceability by part number and spindle position is needed; and delivery schedule together with acceptance criteria.
JUNZHJIA, manufactured by Kexin New Materials (Guangdong) Co., Ltd., builds purpose-made protective cases for spinning accessories. Partitioned liners are designed around your spindle gauge, shaft length and bolster diameter, and gaskets plus anti-rust auxiliaries are matched to the part mix. The company works through OEM and ODM commissions as well as wholesale, agency and worldwide supply, and can provide test and material documents under contract terms. A typical customization flow runs from requirement confirmation and part assessment, through liner concept and case structure approval, to prototype and trial fit, then simulated transport testing where required, batch production with incoming and outgoing inspection, and finally delivery with packaging documentation. For a new part type, build one trial case and run an internal handling and short-haul verification before scaling up.
If the project also covers other textile process equipment, such as knitting or nonwoven line components, compare the differences described in our guides to knitting machine component cases and nonwoven line component cases so that the packaging system and numbering convention can be unified for plant-wide relocation.
Frequently Asked Questions
Q: How many cases does a 1000-spindle ring frame need, and how many spindles per case is sensible?
A: At 20 spindles per case the count is roughly 50 cases, though the real number depends on shaft length, pocket layout and the upper weight limit you accept. Keep total case weight in the 20 to 40 kg band so two people can handle it and the liner is not overloaded by its own contents. A 20-spindle layout normally uses a four by five array with a pitch no smaller than the whorl diameter plus 8 to 10 mm, so adjacent whorls never touch. If shafts are longer, say beyond 350 mm, drop to 12 to 16 spindles per case with a staggered two-layer arrangement and a divider board. Note that a bigger case is not automatically more efficient: as case size grows, inertial load on the parts during handling grows too, and the risk of local liner failure rises. Relocation projects usually also ship rollers, cots and cradles, and these should not share a case with spindles but receive their own liner geometry and their own case numbering tied to the machine they belong to, so the site can open cases in installation order.
Q: Should spindles be packed vertically or horizontally?
A: Both attitudes are used, under different conditions. Vertical packing aligns the load with the working direction so the shaft weight is carried axially and bending risk is lowest, which makes an individually pocketed vertical layout the most conservative choice; the drawback is case height and therefore reduced payload per case. Horizontal packing requires true surface-contact support with multiple support points, ideally spaced no more than one third of shaft length apart, plus positive location at both the whorl and the bolster. If a horizontal part rests on two ends with an unsupported middle, it will slowly bend under long-haul vibration. Handling also matters: vertical layouts put the centre of gravity high, so stacking and lifting need extra stability provisions. If you choose horizontal, machine a semicircular through slot in the liner for surface contact rather than padding with a few square blocks of foam. Whichever attitude is used, the ground shaft surface must never touch a hard material directly.
Q: How long can drafting cots be stored in a case, and which conditions must be controlled?
A: Under warehouse conditions the usable storage period for cots is typically in the 6 to 12 month range as an experience value that varies widely with compound and storage conditions. Beyond that, re-test cover hardness and surface condition before installing them. Four conditions matter, in order. First, block light, because ultraviolet radiation accelerates rubber ageing, so use an opaque shell or a light-blocking inner bag. Second, control temperature, with 15 to 25 degrees Celsius recommended and prolonged exposure above 30 degrees avoided. Third, control humidity, keeping relative humidity around 50 to 65 percent, since too dry causes shrinkage in some compounds while too humid promotes corrosion of the metal core. Fourth, keep oil and ozone away, meaning distance from motors, drives and welding equipment that generate ozone, and no shared cases with mineral oil, grease or plasticizer-bearing materials. Also remember that cots must never sit under a sustained concentrated load, because point or small-area support leaves permanent indentations in the cover that show up after installation as a local change in nip gauge.
Q: If spindles and rollers are already rusty, can they still be used?
A: Judgement depends on location and depth, and it falls into three bands. The first band is light surface discolouration on a non-mating face with no pitting. After cleaning and re-application of anti-rust treatment these parts can generally be used, but the condition should be recorded and monitored. The second band is pitting, or rust on a mating face such as a spindle cone seat or a roller journal. Even a very small dimensional deviation there destroys assembly accuracy and running smoothness, so the part is normally classed as requiring repair or replacement. The third band is a continuous rust band on a ground spindle surface or on roller plating, which is not economically repairable because removing the rust necessarily alters surface geometry and plating integrity. Use magnification to judge pit depth, and a micrometer to measure critical diameters against outgoing values. More importantly, write these criteria into the acceptance document so that the question of whether a part can be used is never argued on site. From a prevention standpoint, the three-layer system of VCI film plus desiccant plus barrier bag is the most direct control available.
Q: Is an antistatic liner really necessary when spinning parts are not electronic components?
A: Yes, but the purpose differs from the electronics industry. In electronics, static control protects devices from discharge damage. In spinning, the problem is contamination attraction and operator discomfort: charged cot and apron surfaces attract airborne fibre and dust, which accumulates in the drafting zone and directly affects yarn quality, while charged cases and liners can give operators a shock during opening and create dust re-deposition onto freshly cleaned surfaces. An antistatic liner therefore provides a drainable contact surface so that friction charging does not accumulate over a long journey. Note that antistatic does not mean conductive: surface resistivity should be held in a sensible band, neither fully insulating nor metallic, because a fully conductive liner can discharge abruptly enough to damage a delicate contact surface. Also, when the case body is an insulator, a liner alone has limited effect, so the practical scheme pairs an antistatic liner layer with a metal drain plate and a grounding label inside the case to complete the path. In practice, a layered liner is easiest to specify. The outer layer carries the antistatic behaviour and presents a clean, low-shedding face to the part, while the underlying layer carries resilience and absorbs vibration energy. Specify both in the drawing so that the two functions are never traded off against each other during procurement.
Q: Should the packaging be transport tested, and which tests and costs are involved?
A: Testing is recommended, particularly for a new part type, a new liner concept, or a first export project. At minimum cover random vibration, which simulates sustained long-haul vibration and is the single most important test for spindles and cots; drop or shock to simulate handling impact, with drop height set according to case weight; stacking compression converted from the actual number of tiers and duration; and temperature-humidity conditioning for sea freight projects in particular. Reference standards may be ISTA 3A, ASTM D4169, or a combination of sub-tests from the GB/T 4857 series. On cost, a full test programme normally costs far less than one defective shipment, so for high-value parts the sensible rhythm is to freeze the design and test immediately. After testing, always re-check function rather than only inspecting the case, re-measuring radial runout on every spindle, inspecting cot covers, and verifying cradle preload. File the data, because it becomes the direct basis for the next similar project and removes the need to repeat the programme each time.
Q: Should we specify IP65 or IP67, and does it make a real difference to spindle rust?
A: For sea freight, open-air transfer and rainy regions, both IP65 and IP67 significantly reduce water ingress risk; the difference lies mainly in resistance to temporary immersion. However, the real corrosion risk is usually not water getting in but moisture being unable to get out. A sealed case develops internal condensation as day and night temperatures cycle, which leaves steel parts in a humid micro-environment for weeks. Any sealed case must therefore be paired with a pressure equalization valve and desiccant so internal humidity is controllable. The logic should be: first define the case barrier against external water and dust using IEC 60529 or GB/T 4208, then manage the internal micro-environment with desiccant, an indicator card and a barrier bag. Doing only the sealing and skipping internal humidity management can produce more corrosion than an unsealed case. Reusable sealed cases also need periodic checks of gasket ageing and valve function, because a gasket that has taken a compression set no longer seals and a blocked valve reintroduces the pressure differential problem. A simple rule for spinning components is to specify the sealing class for the route and the climate, then specify a desiccant quantity and indicator card for the internal micro-environment, and finally write both into the acceptance document so the receiving team can verify them on the first shipment rather than discovering the gap a season later.
Q: Can you add traceability markings that match our spindle position numbering?
A: Yes, and this is exactly what separates a spinning accessory case from a general toolbox. There are three common methods. First, laser-mark or hot-stamp position ranges directly on the liner surface, for example A1 to A20. Second, fit a durable nameplate inside the lid or on the case side stating case number, part name, quantity, machine identity and position range. Third, mark each pocket individually so that a single spindle can be traced. These methods can be combined depending on part mix and project scale. For plant-wide relocations, build a three-level cross-reference of case number, part number and installation position, and deliver it with the shipment so the site opens cases in installation order and cuts counting labour substantially. JUNZHJIA, manufactured by Kexin New Materials (Guangdong) Co., Ltd., supplies traceability-marked packaging for spinning components with marking content and format configured to your list, and operates through OEM and ODM as well as wholesale, agency and worldwide supply, with test and material documents available under contract.
Conclusion and Further Reading
Packaging spindles and drafting parts is really about moving an entire precision system into a box intact. Three ideas cover most of it. Precision parts are threatened less by a single large impact than by sustained micro-vibration and metal-to-metal contact. Rubber parts are threatened by light, heat, oil and concentrated load rather than by dropping. Corrosion risk can only be closed with the three-layer system of vapour phase inhibitor, desiccant and barrier bag, because no single layer is sufficient. Apply those three ideas to liner partitioning, case structure and test verification, and a spindle or drafting component case will carry out its relocation and shipping duty instead of becoming a new source of quality problems.
Further Reading