

The accuracy of a weighing and dosing system is not decided by the instrument resolution but by a mechanical chain from the load-cell spring element to the hopper support, from the feeder gap to the valve seal. Every link on this chain shares one feature: a precision state "calibrated at assembly, maintained at run", and transport is exactly the window where that state loses monitoring. A 500 kg rated load cell often has a safe overload of only 1.5 times rated; a drop or impact in the case can delaminate the strain gauge or yield the spring element locally, bringing irreversible zero drift. A screw feeder's blade-to-tube gap is often at millimetre scale; after a knock the gap changes and dosing turns from steady conveyance to pulsed drop. A rotary discharge valve's rotor-to-shell gap is even fractions of a millimetre; a jam means line stop. Therefore the criterion for a weighing and dosing case is not "is the part damaged" but whether the sensor zero and span calibration still hold, whether feeder and valve gaps stay in the as-built range, and whether the load module mounting datum and level can be reproduced. This article gives protection criteria, transport locking, liner and support design, moisture-dust measures and arrival acceptance part by part.
The most common site practice is to put the removed load module with the hopper on a wooden pallet, wrap with film and no transport lock; lay the screw feeder across the case bottom with the body pressing on the blade; pack pneumatic parts and solenoids in a carton with the junction box face up open. This rarely fails at once in short hauls, but after long road vibration or multiple transfers the problems appear as "no identifiable cause": the scale zero drifts slowly after start, the same recipe shows systematic deviation between shifts; the feeder pulses at low speed and the controller keeps adjusting lead; the rotary valve noises after days and jams; the junction box floods and the signal jumps, and the first reaction is to suspect the instrument or software. The real trouble is the evidence chain: these state changes leave no record in transport, and by the time they show, the factory calibration is overwritten by site re-calibration, so liability cannot be judged. The following proceeds along this chain: first how accuracy is broken, then sensor, feeder, bin, valve and instrument protection, finally marks, documents, transport test and arrival acceptance.
Table of Contents
- Dosing Accuracy Is a Chain Transport Can Break
- Part List and Failure Paths
- Load Cell: No Overload, No Shock, No Eccentric Load
- Load Module Datum, Level and Calibration Weights
- Screw Feeder and Vibrating Feeder
- Hopper, Bin and Discharge Mechanism
- Dosing Valve and Pneumatic Components
- Weighing Instrument, Junction Box and Signal Cable
- Moisture, Dust and Hygiene Requirements
- Liner, Support and Compartment Design
- Frequently Asked Questions FAQ
- Conclusion and Related Reading
Dosing Accuracy Is a Chain Transport Can Break
Continuous and batch dosing differ in process but share the accuracy path. Take a four-station loss-in-weight scale: material goes from bin through feeder into the weigh hopper, hung on the frame by three to four load modules, whose strain-gauge sensors turn weight into millivolt signal, summed by the junction box into the terminal, which filters, calibrates and computes flow, then sends feed-speed command to the inverter or vibration controller. Any change on this chain is a dosing deviation.
The deviation sources are three transport-breakable quantities. First, the sensor mechanical zero. The strain-gauge output strictly follows spring-element strain, the zero compensated at factory with a precision resistor network. When the sensor takes over-limit shock, side force or bending moment, the spring element yields locally and the gauge adhesive shears, shifting zero observable even at no load, yet often hidden by "tare" on site. Second, the geometry gap of feeding and shut-off. The blade-to-tube gap of a screw feeder, the rotor-to-shell gap of a rotary valve, the plate-to-seat gap of a butterfly valve are designed small gaps deciding conveyance and shut-off stability, changed by any knock. Third, the structural mounting datum. The load module mounting-face level, the effective support polygon among modules, and whether hopper and pipe form a bypass force are assembly geometry; if fixing in the case deforms the module top or bottom plate, the datum is rewritten.
Explaining these three quantities shows why the weighing-dosing case cost structure differs: it needs not a thicker cushion but the "calibration state" frozen intact. General criteria are in instrument case selection guide.
Part List and Failure Paths
A dosing system transport unit often has ten to fourteen pieces, but truly needing separate design are the load module, feeder and calibration weights. Grading decides which parts keep original factory pack, which need dedicated fixtures, which are ordinary electromechanical. The table gives the common list and failure paths.
| Part | Main Failure Path | Grade | Key Measure |
|---|---|---|---|
| --- | --- | --- | --- |
| Strain-gauge load cell | Shock or side force yields element, gauge delaminates, zero drift | A | Transport lock, axial load only, independent support, no lift point |
| Load module (top/bottom plate, anti-tilt) | Mounting datum deform, anti-tilt pressed, lock bolt missing | A | Factory lock posture, bottom flat, top/bottom not pressed |
| Calibration weight (E2/F1/F2) | Impact changes mass, rust and scratch cause error | A | Separate cell each, soft pad, never stack |
| Screw feeder | Blade gap change, shaft bend, hanger bearing damage | A | Axial support, blade suspended, no tube or flange load |
| Vibrating feeder and leaf-spring set | Leaf angle change, excite misalign, trough deform | A | Leaf fixed or whole shipped, trough no side squeeze |
| Vibration motor and exciter | Eccentric phase wrong, bearing axial shock | B | Lock eccentric per maker, axial limit, upright |
| Hopper and bin | Thin-wall dent, liner scratch, outlet deform | B | Inner temp support, liner guard, no invert pressure |
| Rotary valve, butterfly, ball valve | Rotor-shell gap change, jam, seal face bruise | A/B | Locator at gap, port plug, seal zero contact |
| Pneumatic actuator and cylinder | Rod bend, limit switch damage, seal dry | B | Rod retracted, sleeve, switch separate pack |
| Weighing instrument, transmitter, box | Moisture zero drift, joint oxidise, board vibrate | A/B | Seal bag with desiccant, port plug, battery off |
| Signal cable and shield | Shield break, joint flood, radius too small | B | Large-radius coil, end cap, separate reel |
| Air prep and solenoid group | Regulator spring drift, spool jam | C | Port plug, whole fixed, no metal contact |
Beyond the list, multi-point systems calibrate sensors as a set; they must be "managed as a set" in transport. A common error is packing several sensors of one scale in different cases and re-assigning on arrival; though same spec, the factory compensation pairs by group and serial, and mixing directly causes eccentric error. So the packing drawing marks one scale's sensors and junction box as one group with colour or label. Grade and liner cooperation is in case foam material comparison.
Load Cell: No Overload, No Shock, No Eccentric Load
The load cell is the most "silent" part: no moving part, looks solid, needs no care after mounting, so it is most easily treated as ordinary metal. Actually its usability rests on the strain rosette and adhesive integrity on the spring element, both serving "precise strain" not "bearing load". Three numbers to remember: rated capacity, safe overload usually 1.5 times rated, limit overload usually 3 times rated, the latter two typical values per maker data. The danger zone is exactly between them: above safe but below limit, the sensor may have permanent zero shift with no appearance damage.
Shock and eccentric load are two different mechanisms. Shock is instant high-amplitude load: case drop, module lifted by fork then dropped, hopper hitting frame when lifted. Shock energy absorbed by the spring element shows as gauge adhesive micro-slip and local yield. Eccentric load is sustained non-axial load: using the sensor body as lift point, jacking the module top plate, tying the module to the frame side: these make the sensor take side force or bending moment, for which strain cells have almost no design margin. Some single-point cells allow some eccentric in duty, but that is for material eccentricity, not random lift and tie load.
Four transport practices. First, fit transport locks. Most modules ship with transport lock bolts or blocks rigidly linking top and bottom plates so dynamic load bypasses the sensor into structure; many sites throw the lock into the toolbox after install and lose it at next move, so keep it in a dedicated box near the module and ship with the case. Second, axial load only. The sensor and module lie horizontally with full-bottom support, no single-end hang; never use sensor body, cable or top plate as lift point. Third, limit displacement not clamp. Use surround limit allowing tiny assembly gap, never strap or plate clamping the sensor, which is itself sustained eccentric. Fourth, protect the cable. The cable exits the spring element; the joint is weakest, coiled and fixed alone, not pressed by other heavy parts, coil radius at least six times cable outside diameter (experience).
Pre-arrival cell check should precede energising: visual spring-element plastic-deformation mark, seal-weld crack, cable jacket press mark; then ohmmeter on input and output impedance versus factory record; then observe instrument zero at no load within factory range. These four screen most severe damage without weights; acceptance criterion is in section eleven. The protection logic of cell periphery matches precision mechanical parts in shaft coupling case.
Load Module Datum, Level and Calibration Weights
A load module is an assembly: sensor between top and bottom plates, plus anti-tilt, anti-rotation, ground and limit bolts. In transport the assembly value is not the sensor but the assembled relative position between top and bottom plates. Once the top is pressed, bottom pried or limit bolt bent, even with intact sensor the mounting datum changes, forcing shim rework or full re-calibration, cost far above two lock bolts.
Level is the most underestimated datum. A four-support scale with top-face height difference beyond a range makes each point's load not proportional to geometry, amplifying eccentric error from material offset; level deviation also forms a bypass force between hopper and rigid pipe, diverting part of the weight from the sensor, showing as "normal with weights, deviant with material". Experience guideline: top-face height difference within 0.5 mm, mounting-face level within 0.2 degree (about 3.5 mm per metre), final tolerance per maker. So transport keeps the module horizontal with full-bottom support, no single-end hang, never upright to save space.
Calibration weights are the most special content. Dosing-scale weights are graded E1, E2, F1, F2 by OIML R111, each with a maximum permissible error; in trade or metrology confirmation the weight itself is a measuring instrument, verified per JJG 99 "Weights". This means weights need logistics unlike ordinary metal: impact or drop changes mass (especially cast-iron and low-grade adjustment cavity), scratch and rust cause surface adsorption and mass drift, hand sweat on polished face causes pitting. So weights are packed one per cell with soft pad, never stacked, never used as filler by the outlet, and re-checked against standard on arrival. The level, signal source, simulator and feeler gauge shipped with weights are also fixed, because their accuracy also rests on mechanical integrity.
| Control Item | Experience Band (per maker) | Arrival Re-check |
|---|---|---|
| --- | --- | --- |
| Top-face height diff of one scale modules | Within 0.5 mm | Straightedge and feeler, or depth gauge per point |
| Module mounting-face level | Within 0.2 degree | Electronic or frame level segmented |
| Locator gap after lock removed | Consistent with as-built | Feeler compare, visual top-plate press mark |
| No-load zero return | Near zero after three load cycles | Instrument reading vs factory zero |
| Weight mass | Within grade error | Compare with upper standard |
| Cell input/output impedance | Consistent with factory | Ohmmeter, suspend if over |
Screw Feeder and Vibrating Feeder
A screw feeder looks like "a tube plus a screw" but its accuracy concentrates on three geometry values. First, the blade-outside to tube-inside gap, typically 0.5 to 1.5 mm, deciding shear and backflow in conveyance; once the blade deforms or tube flattens, the gap is uneven and conveyance turns from continuous to pulsed. Second, the screw-shaft coaxiality; a slender shaft can exceed 20:1 length-to-diameter, and if only ends supported with middle hanging, self-weight bends it permanently, showing as bearing heat and higher crush rate. Third, the drive-end flange register, a locating datum; a knock changes coaxiality and adds bending moment between reducer and screw.
Protection: add one to two mid supports beyond the two ends, the block holding only the shaft smooth section, not the blade; tube and flange take no lift load, lift points on dedicated lugs or timber; quick-disconnect feeders ship assembled, disassembly only adds register knock chance. If the feeder is long and shipped in sections, fit alignment-pin protectors and temp locating plates at the cut, and record section numbers to avoid mismatch.
The vibrating feeder vulnerability is different. Its conveyance comes from leaf-spring install angle, preload and excite frequency; leaf springs are stacked laminates, and an angle deviation of fractions of a degree changes material direction and speed, hard to compensate by amplitude on site. More critically, vibrating equipment must be mechanically locked in transport: an unlocked trough at resonance swings large, leaf springs fatigue, rubber shear springs overheat, exciter alignment changes. So fit transport lock bolts per maker, rigidly linking trough and base; for dual-motor drives, lock eccentric phase per mark or reverse per maker, and verify phase on arrival before energising. Electromagnetic feeders' armature-core gap is also micron-to-mm critical, kept as-built, never disassembled to save weight.
Vibration equipment general protection is in vibrating screen case, whose leaf-spring, rubber-spring and exciter handling matches feeders.
Hopper, Bin and Discharge Mechanism
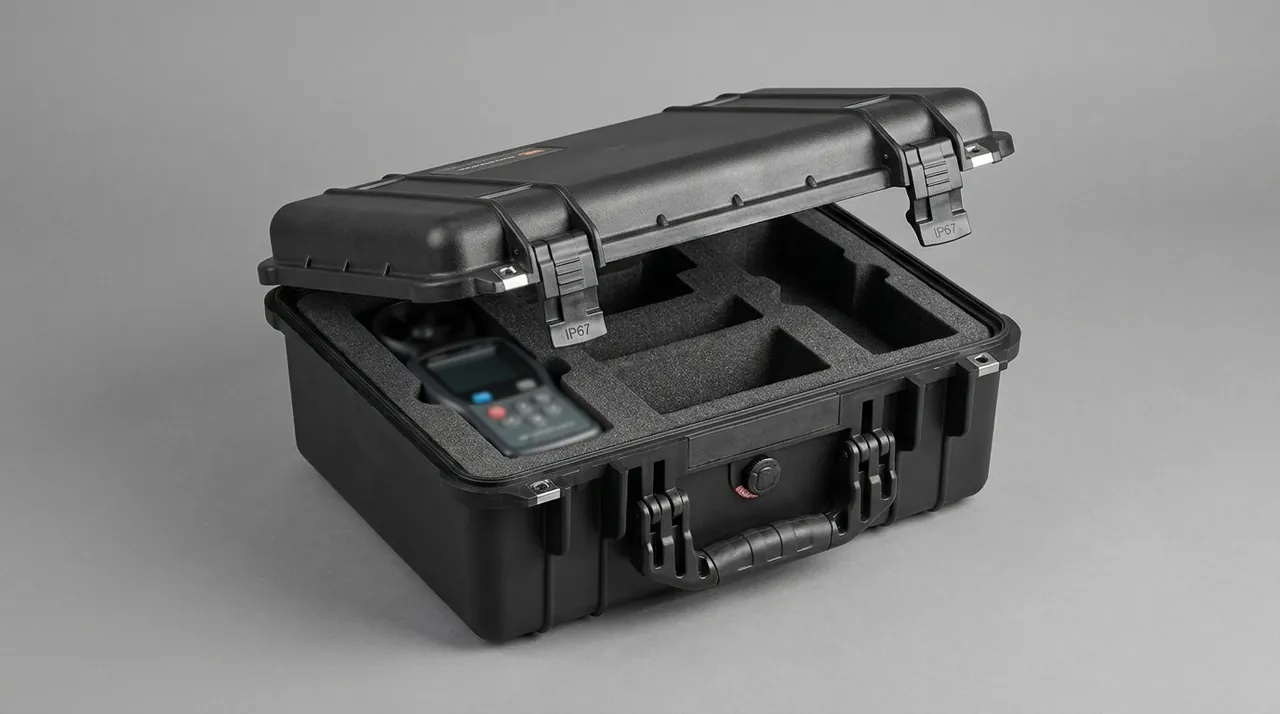
Hoppers and bins are the largest, least protection-sensitive yet most "long-term hidden" parts. Wall thickness is only 1.5 to 3 mm; large bin outer wall without stiffener dents directly under point load, and the dent is not appearance but flow change: a low-velocity zone forms, powder bridges, a rat hole forms by the outlet, dosing accuracy drops, the operator taps the bin to keep running, and tapping accelerates liner drop.
Inner-surface treatment is the second concern. Food and pharma hopper walls are often mirror-polished to 0.4 to 0.8 micrometre, some lined with PTFE or UHMW-PE for flow. These surfaces must have zero contact in transport; liner edges curl most easily, then hang material and breed hygiene dead zones. Practice: inner temp support, but the support point only on stiffener or outer structure, never on polished face or liner; or use an external embrace frame limiting deformation without entering the cavity.
Discharge mechanism includes slide, butterfly, rotary and pneumatic gate and level switch; rotary valve and seat butterfly have the smallest gap, covered in section seven. Level switches (paddle, capacitance, RF admittance) have thin long sensing rods easy to bend, removed and packed alone with the restore step noted in the document. Flexible connectors (cloth, silicone, expansion) avoid long compressed storage in cool dry transport, because rubber ages faster under ozone and UV and should recover shape soon after transport.
Dosing Valve and Pneumatic Components
The rotary valve (star valve) is high in both accuracy and failure rate. Its conveyance comes from impeller speed and cell volume, and the impeller-blade to shell radial gap is often only 0.1 to 0.3 mm (typical), the end to end-cover axial gap also small. This gap prevents leakage and shear but tolerates zero foreign object or deformation: one foam grain, one wood chip, or a burr from a pressed impeller end is enough to jam. So in transport do three things: fit a transport locator or pad between impeller and shell so the impeller does not shift axially; blind or plug all ports (inlet, outlet, shaft end, cleanout) to stop particles; remove the drive coupling or loosen per maker to avoid impact damage to motor-impeller assembly.
Butterfly and ball valve protection focuses on the seal face. The butterfly plate seal is mostly EPDM or PTFE, sealing by micro interference with the metal seat; any dent leaks. The ball is mirror-lapped; a scratch leaks and cannot be fixed on site. So keep these valves "closed but not fully pressed" per maker, seal face touching no hard object, never load-bearing on the body. Pneumatic actuator and cylinder piston rods are chrome or nickel mirror; rod bend is the typical transport damage, so retract the rod to end and add a sleeve; limit, proximity and magnetic switches are fragile electronics, removed and packed alone with valve number.
Pneumatic parts and solenoid groups share the foreign-object risk. The solenoid spool and sleeve gap is micron-scale; foam dust, carton fibre and metal chips cause jam, so all air ports are plugged and checked one by one. The filter-regulator has a regulating spring and diaphragm, the gauge glass fragile, so fix the whole group in an independent case cell, not with heavy parts. Correct arrival order is air-tightness and manual action test first, confirm no jam and no leak, then energise interlock, avoiding "forcing" a jammed spool live by experience.
Weighing Instrument, Junction Box and Signal Cable
The weighing instrument and junction box turn millivolt signal into digital, and that decides their transport logic. A strain-gauge cell typically outputs 2 mV per volt excitation, full-scale often only tens of mV, at the same order as site interference. So any factor raising contact resistance or breaking shield directly becomes zero drift: terminal oxidation, cable joint flood, shield broken in transport, shield wrongly grounded at both ends forming ground loop, are common field faults. So transport protects not against shock but against keeping the electrical state at arrival identical to factory.
Three measures. First, end seal and moisture. The junction-box cover seal and cable-entry seal are waterproof keys; confirm seal in place, entry plugged, desiccant inside, box placed face up to avoid long cover press. Second, cable management. Signal cable is never cut or spliced in transport, because shield continuity once broken is hard to restore on site; coil at large radius fixed alone, radius at least six times cable outside diameter, end cap on. Third, board protection. The terminal has analog front-end, A/D and switcher, vibration- and static-sensitive, so pack in anti-static bag, disconnect backup battery, avoid direct metal contact. Related practice is in ESD shield case and IP67 protective case.
One overlooked environment boundary: the LCD slows at low temperature and may permanently fail by liquid-crystal phase change in extreme cold, so in winter cold regions the instrument travels with the case and avoids long outdoor exposure. If the project has an outdoor exposed terminal, the case fits the corresponding IP grade per IEC 60529 and GB/T 4208, and the breather or vent film is confirmed unblocked before transport.
Moisture, Dust and Hygiene Requirements
Weighing-dosing systems serve food, feed, pharma and chemical scenes, so transport packing meets two constraints: equipment anti-corrosion and moisture, and industry hygiene. Food general hygiene follows GB 14881, pharma follows GMP; both care about cleanability, material compatibility and residue risk of material-contact surfaces, so inner packing should not shed, not release odour, not react with stainless, and be fully cleanable after opening.
Chloride is the invisible enemy of stainless. Dosing equipment is mostly 304 or 316L stainless, passivated, and the passive film is chloride-sensitive: chloride-bearing foam, PVC debris, some flame-retardant pack and chloride cleaner residue can pit in humidity, showing as brown pits hard to root out and becoming residue and microbe sites. So liner and cushion use halogen-free systems, e.g. halogen-free polyethylene or expanded polypropylene; if polyurethane moulded liner is used, add an isolation film between stainless and liner to avoid long bonding and moisture absorption. Wooden pack should be fumigation-free plywood, meeting quarantine and avoiding solid-wood debris and pest.
Another dust-environment requirement relates to equipment safety. If the dosing equipment serves a combustible-dust site, its electrical part is assessed per the current standard series for electrical equipment in combustible dust atmospheres; transport corresponds to "no residual dust inside": blow clean hopper, feeder and valve cavities before factory, because residual powder enters bearing, gap and solenoid in vibration, causing both mechanical jam and hygiene-safety risk at first run. For dust grade, agree IP6X per IEC 60529 and GB/T 4208 and check seals after opening. Higher cleanliness projects complete inner pack in ISO 14644 Class 8 or better, stainless cleaned then in clean bag, avoiding long open-shop exposure.
Liner, Support and Compartment Design
Weighing-dosing liner has three rules different from X-ray or electronic cases. First, creep control under long static load. The cell and module may store months in the case; any static load long carried by elastic material relaxes slowly and fails the limit, so load parts sit on wood or rigid bracket, foam only surrounds and isolates; for long storage prefer fatigue-better expanded polypropylene or cross-linked polyethylene over low-density polyethylene. Second, "surround not clamp". Cells, instruments and valves fear sustained eccentric and dent, so liner contact is multi-point constraint allowing tiny gap, forbidding any clamp or tie. Third, load layering and isolation. Hopper and frame heavy parts sit at the bottom near lift point and fork pocket; sensor module and instrument at upper independent cells; weights occupy one cell alone with soft pad around, no heavy part above weights, instrument or valve.
Compartments follow environment not volume: sensor and instrument need a low-humidity dust-free cell; feeder and hopper need scratch-proof but not humidity-controlled; valve and pneumatic need dust-proof with plugged ports; weights need knock-, moisture- and rust-proof alone. Each humidity-controlled cell gets its own desiccant and humidity card read separately on opening, because humidity can differ clearly among cells in one case. Case structure decides whether these cavities stay isolated; hinge, latch and seal selection and failure are in toolbox hinge latch and seal; long transport or air needs a pressure equalisation valve to avoid pressure difference deforming the seal, in case pressure equalisation valve; flexible compartment projects can use removable divider system.
Specially handle "set calibration" compartments. One scale's sensors, junction box and calibrated weights sit in adjacent traceable cells with colour labels inside and a list outside, avoiding mix on arrival. For frequent-turn projects like leasing or show tours, use a renewable-liner case because moulded liner loses surround precision after repeated opens and then passes shock to the sensor.
Frequently Asked Questions FAQ
Q: Why are load cell transport locks so important?
A: The transport lock bolt or block rigidly links the module top and bottom plates so dynamic load in handling bypasses the sensor into the structure instead of stressing the spring element. Without it, a drop or fork lift can send over-limit shock that yields the element locally or shears the gauge adhesive, shifting the zero even with no appearance damage, and that shift is then hidden by site "tare". Many sites throw the lock into a toolbox after install and lose it at the next move, so keep it in a dedicated box near the module and ship it with the case. The lock is the cheapest insurance that the as-built calibration state arrives intact, far cheaper than shim rework or full re-calibration after a deformed datum, and it also prevents the limit bolt from being bent during transit. JUNZHIJIA keeps the lock bolts in a dedicated box fixed near the module and ships them with the case, so the next relocation can re-secure the sensor instead of leaving it unprotected.
Q: Why does a screw feeder blade gap matter so much in transport?
A: The blade-outside to tube-inside gap, typically 0.5 to 1.5 mm, decides how evenly the feeder conveys and how much material shears back; once the blade is pressed or the tube flattened, the gap becomes uneven and conveyance turns from continuous to pulsed, forcing the controller to keep adjusting lead. The slender shaft also bends permanently if only ends are supported with the middle hanging, showing as bearing heat and higher crush rate. Transport adds one to two mid supports holding only the shaft smooth section, keeps tube and flange off the lift path, and ships quick-disconnect feeders assembled to avoid register knock. Long feeders in sections get alignment-pin protectors and numbered cuts to prevent mismatch on arrival, and the drive flange register is protected from impact that would add bending moment. JUNZHIJIA adds one or two mid supports beyond the two ends so the screw shaft is fully cradled, and never lets the tube or flange carry lifting load, keeping the gap uniform through transit.
Q: How is a rotary discharge valve protected against jamming in transport?
A: The impeller-blade to shell radial gap is often only 0.1 to 0.3 mm, so it tolerates zero foreign object or deformation; one foam grain or a burr from a pressed impeller end jams it. Transport fits a locator or pad between impeller and shell so the impeller does not shift axially, blinds or plugs all ports (inlet, outlet, shaft end, cleanout) to stop particles, and removes or loosens the drive coupling per maker to avoid impact damage to the motor-impeller assembly. The valve is kept "closed but not fully pressed" with the seal face touching no hard object and never load-bearing on the body, because a dent on the seat leaks and cannot be fixed on site, forcing a full valve replacement that stops the dosing line. JUNZHIJIA blinds every port with a dedicated plug and labels the drive-end disassembly position, so the rotor is found in the same state at arrival and no metal enters the tight clearance.
Q: Why must load module level be controlled in transport?
A: Level decides whether each support point's load matches its geometry. A four-support scale with top-face height difference beyond about 0.5 mm makes load not proportional to position and amplifies eccentric error from material offset; level deviation also forms a bypass force between hopper and rigid pipe that diverts part of the weight from the sensor, showing as "normal with weights, deviant with material". Transport keeps the module horizontal with full-bottom support, no single-end hang, never upright to save space, and the limit bolt must not be bent. After arrival, check top-face height with straightedge and feeler and mounting-face level with an electronic or frame level per maker tolerance, then compare against the factory record before the scale is commissioned. JUNZHIJIA stores modules flat with full-bottom support and marks the install-face level on the case drawing, so the original reference is reproducible rather than re-derived on site. JUNZHIJIA records the measured top-face height difference on the acceptance form so any change during transit is visible at receiving inspection, and treats a shifted level as a stop-ship item rather than a field adjustment.
Q: What special care do calibration weights need in transport?
A: Weights are measuring instruments graded E1, E2, F1, F2 by OIML R111 and verified per JJG 99, so logistics differ from ordinary metal. Impact or drop changes mass, especially cast-iron and low-grade adjustment cavities; scratch and rust cause surface adsorption and mass drift; hand sweat on polished face causes pitting. So each weight is packed in its own cell with soft pad, never stacked and never used as filler by the outlet, and re-checked against an upper standard on arrival. The level, signal source, simulator and feeler shipped with the weights are fixed too, because their accuracy also rests on mechanical integrity, and a bent feeler or shifted level gives a wrong datum that defeats the weight calibration. JUNZHIJIA packs each weight in its own cell with soft lining and never stacks weights over other parts, and attaches the calibration certificate so grade compliance is provable at receiving. On arrival, JUNZHIJIA advises comparing each weight against the next higher standard before use, so any mass drift from transit is caught before it reaches the scale and corrupts the calibration chain.
Q: Why protect the junction box and signal cable from moisture?
A: The cell output is only tens of mV, at the same order as site interference, so any rise in contact resistance or break in shield becomes zero drift: terminal oxidation, cable joint flood, shield broken or wrongly grounded at both ends all cause it. Transport confirms the box cover seal and cable-entry seal are in place, plugs the entry, puts desiccant inside and keeps the box face up; the signal cable is never cut or spliced, coiled at large radius fixed alone with end caps. The terminal board is vibration- and static-sensitive, packed in an anti-static bag with backup battery disconnected. Keeping the electrical state at arrival identical to factory is the real goal, so a humidity card inside the box gives the receiver evidence of the storage condition. JUNZHIJIA seals the junction box upward with desiccant inside and ships the terminal in an anti-static bag with the backup battery disconnected, so the electrical state at arrival matches the factory record.
Q: Why avoid chloride in stainless dosing equipment packing?
A: 304 and 316L stainless rely on a passive film that is chloride-sensitive; chloride-bearing foam, PVC debris, some flame-retardant pack and chloride cleaner residue can pit the surface in humidity, leaving brown pits that are hard to clean and become residue and microbe sites. So liner and cushion use halogen-free polyethylene or expanded polypropylene, and if polyurethane moulded liner is used, an isolation film separates stainless from liner to avoid long bonding and moisture absorption. Wooden pack should be fumigation-free plywood to avoid solid-wood debris and pest. These choices protect both corrosion resistance and hygiene compliance of the contact surface, which matters for food and pharma dosing lines. JUNZHIJIA selects halogen-free polyethylene or expanded polypropylene for liner and cushion, and adds an isolation film between stainless and any polyurethane insert, avoiding chloride contact during the whole transit. JUNZHIJIA also prefers fumigation-free plywood for any wooden pack, avoiding both solid-wood debris and pest risk, and keeps the stainless surface clean and dry through the whole route so no chloride film forms.
Q: How to verify weighing-dosing case transport protection?
A: Combine physical and test verification rather than appearance only. Physical: pack real modules, feeders, valves and instruments by the plan, run one real route, then open and check sensor impedance and no-load zero, feeder blade gap and shaft straightness, valve locator and seal, instrument self-test and cable continuity; this finds structure defects directly. Test can reference ISTA whole-case performance or ASTM D4169 distribution cycle; domestic uses GB/T 4857 vibration, shock, stack and drop; air also cares about low-pressure effect on sealed cavity. For rust concern, sample by GB/T 10125 neutral salt spray, and if MIL-STD-810H is specified as environmental basis, state in the report that this is a method reference only and constitutes no military certification.
Conclusion and Related Reading
Weighing-dosing protection is less about case strength than freezing the calibration state: lock the sensor, keep the module level, hold feeder and valve gaps, and separate weights, instruments and hygroscopic cells. JUNZHIJIA provides custom cases, liners and documents by system model so dosing accuracy stays verifiable from factory to installation.
Related Reading