

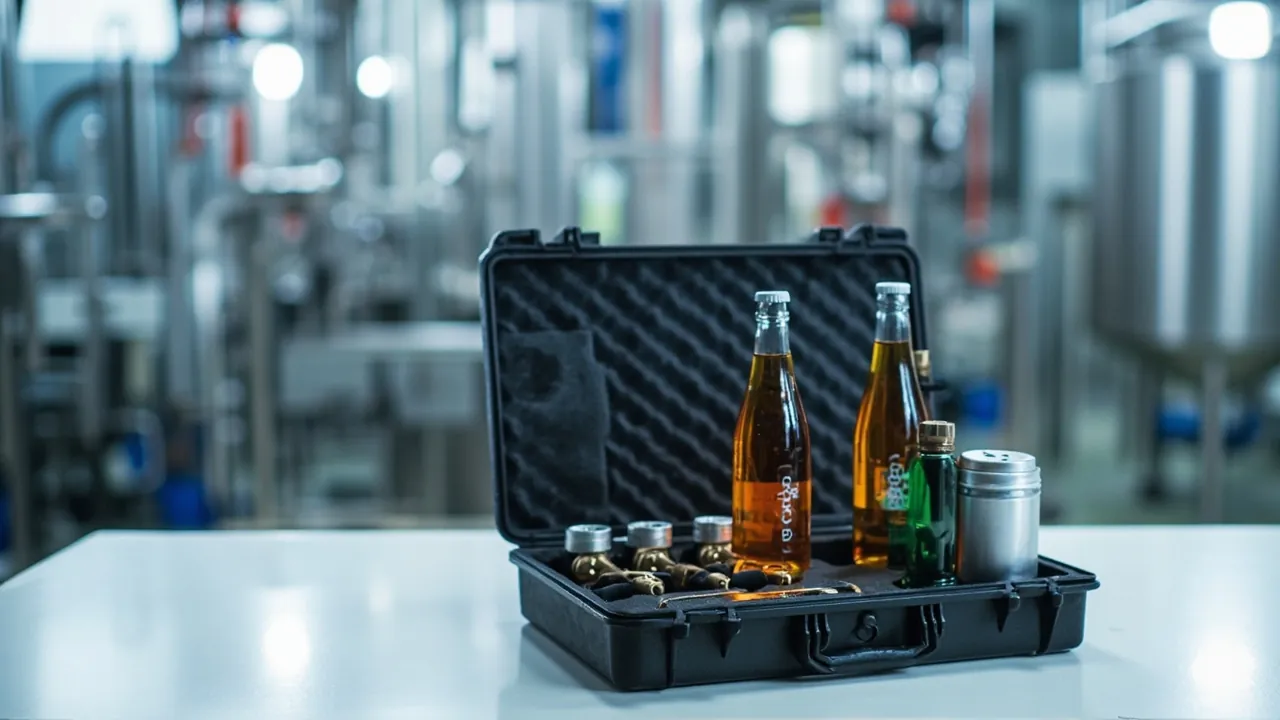
A beverage bottling line is one of the most highly continuous food production assets in existence. When a line running thirty thousand bottles an hour stops for ten minutes, it loses a full segment of output, and sterile or hot-fill lines often need additional cleaning and sterilization time before they return to a stable state. Getting filler valves, filling heads, seals, and drive components to the workstation safely, cleanly, and quickly is therefore the central spare-parts management problem in a bottling hall. A beverage bottling parts case must satisfy three conditions at once: valve sealing cones and O-ring grooves must not be deformed by impact or compression, the case itself must be washable, sanitizable, and dryable to meet basic hygienic design requirements, and the enclosure should reach IP65 or better per IEC 60529 / GB/T 4208 to cope with wash-down and wet-cold conditions. JUNZHJIA can provide round-bore locating inserts sized to specific filler models, gasket options resistant to CIP chemicals, and matching structure drawings and material certificates.
Three problems dominate real-world practice. Filler valves knock against each other in a tote, leaving pressure marks on sealing cones that are almost invisible to the eye, and after reinstallation the result is dripping or unstable fill volume. O-rings are loose in a plastic bag, mixing specifications and deforming under long-term compression, so sealing fails on installation. Water remains in the case after washing, leaving water marks and pitting on stainless parts. None of these is hard to solve, but the solution has to start at the selection stage, considering valve characteristics, hygiene requirements, and transport conditions together. This article follows the sequence of spare grading, valve protection, hygienic design, material compliance, insert architecture, sealing, transport validation, inventory, and acceptance.
Table of Contents
- 1. Protection Challenges for Beverage Bottling Line Spares
- 2. Grading the Bottling Line Component and Spare Inventory
- 3. Precision Protection for Filler Valves and Valve Assemblies
- 4. Hygienic Design: CIP/SIP and Aseptic Filling Requirements
- 5. Material Compliance: GB 4806, Stainless Parts, and Seals
- 6. Shell Material Comparison
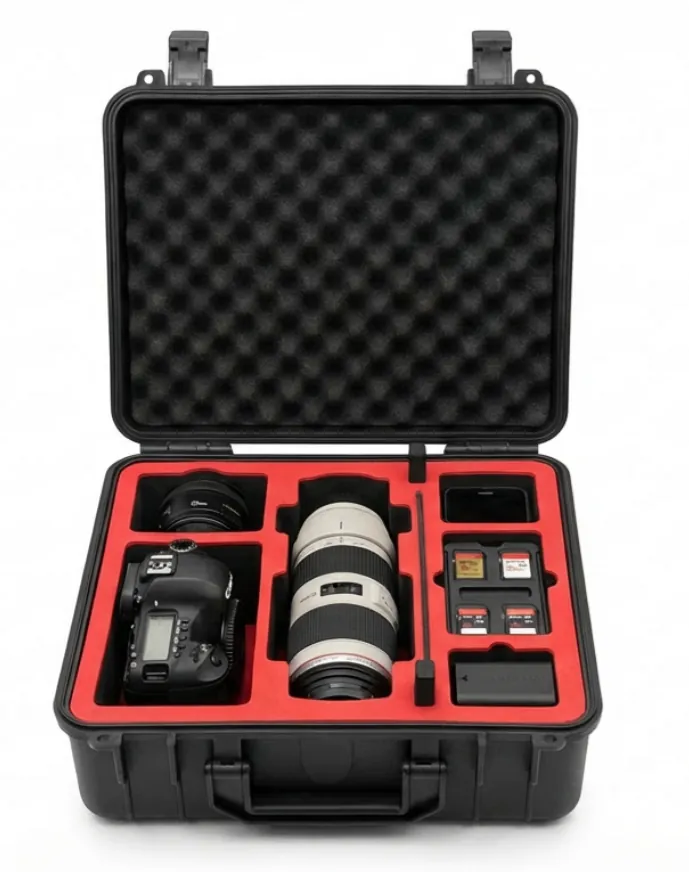
- 7. Insert Design: Round-Bore Retention and Removable Dividers
- 8. Sealing, Dust, and Wash-Down: IEC 60529 and GB/T 4208
- 9. Carbonated Beverage Pressure Components and Pressure Protection
- 10. Corrosion and Chemical Resistance: CIP Chemicals, Sugar, and Acid
- 11. Vibration and Impact Validation: ISTA and GB/T 4857
- 12. Latch, Hinge, and Gasket Selection
- 13. Spare Inventory, Marking, and Traceability Management
- 14. Acceptance, Cleaning Maintenance, and Life-Cycle Cost
- Frequently Asked Questions
- Conclusion and Further Reading
1. Protection Challenges for Beverage Bottling Line Spares
Spare-part protection on a bottling line differs from general mechanical spares in four significant ways.
First, sealing surfaces are held to very high precision. A filler valve usually seals through contact between a metal cone and an elastic seal, with fit tolerances measured in microns. Any scratch, pressure mark, or out-of-round deformation translates directly into dripping, fill-volume variation, or oxidation risk. This type of failure is usually invisible before assembly and only appears once the part is on the line, which means another line stop.
Second, hygiene requirements are severe. Aseptic and ultra-clean filling impose strict control over anything entering the filling zone. If a spare-parts case is to enter a clean zone, it must be washable, sanitizable, free of dead corners, and must not become a carrier of microorganisms or particles.
Third, wet-cold and chemical exposure coexist. A bottling hall continuously presents rinse water, CIP chemical residue, sugar syrup, and acidic beverage splash, with low-temperature areas in cold filling and chilled staging. The shell and gaskets must resist both corrosion and low temperature.
Fourth, there are many specifications and high unit value. A single bottling line may involve dozens of valve, seal, guide, and drive variants. Unit value is high but quantity is low, which makes the convenient-looking practice of mixing everything in one tote the highest-risk option.
In one sentence: the core conflict for a bottling spare case is how high-precision seals and a high-frequency washing environment can coexist.
2. Grading the Bottling Line Component and Spare Inventory
Grading is the precondition for controlling both budget and risk. The table below maps common categories to protection strategy.
| Category | Typical components | Primary failure mode | Suggested IP class | Suggested insert |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Filler valves | Filler valves, filling heads, valve cores, valve seats | Sealing-cone scoring, out-of-round deformation | IP65 | Round-bore retention plus face protection cap |
| Seals | O-rings, lip seals, gaskets | Compression set, low-temperature hardening | IP65 | Compartmented bins stored flat and unloaded |
| Drive | Star wheels, transfer wheels, guides, bearing housings | Tooth-face impact, bore deformation | IP65 | Tooth contour fitting plus axial retention |
| Electrical control | Servo drives, photoelectric sensors, encoders | Moisture short circuits, vibration-induced error | IP65/IP67 | Anti-static foam plus desiccant |
| Piping and fittings | Sanitary fittings, clamps, hoses | Thread damage, bore scoring | IP54 | Round-bore fixing plus face protection |
| Consumables | Springs, retaining rings, strainers, labels | Spillage and mixing, deformation | IP54 | Compartmented bins plus transparent lid |
The key rule is that anything whose function depends on surface-to-surface contact must occupy its own compartment and must not be compressed. O-rings and filler valve cores are the classic examples. Mixing them in the same compartment as wrenches and bolts is the most common and most expensive error in bottling spare-part management.
In practice, JUNZHJIA advises completing this graded inventory first and then deriving case dimensions and insert format from it, concentrating spending on the three categories that are genuinely sensitive: valve assemblies, seals, and electrical components.
3. Precision Protection for Filler Valves and Valve Assemblies
The filler valve is the most typical high-precision component on a bottling line and the part that demands the most careful protection design.
Filler valve failure modes are mainly three:
- Sealing-cone scoring, caused by contact with hard objects or mutual impact, showing up as micro-dripping;
- Valve body out-of-round deformation, caused by compression or impact, showing up as fill-volume variation;
- Valve core guide wear, caused by repeated relative movement under vibration, showing up as sluggish actuation.
Corresponding insert design points:
- Round-bore locating. Size the bore to the valve body outside diameter with 0.5 to 1.5 mm interference per side so EVA elasticity holds it and prevents movement.
- Face isolation. The end carrying the sealing cone must have a 3 to 5 mm cavity and must never touch the insert base or other components directly.
- Axial retention. Provide a stepped shoulder to stop movement along the axis.
- One part per compartment. Give each valve its own cavity with at least 8 mm of EVA wall between cavities.
- Protection caps. For valves with exposed sealing faces, supply a dedicated cap that is removed immediately before assembly.
Valve core and seat pairing is a commonly overlooked detail. If ground-matched cores and seats are mixed up, sealing performance drops after assembly. Provide adjacent positions on the insert keyed to the pairing number, and note the pairing on the checklist so the two are always retrieved together.
Seal protection follows three rules: unloaded, unmixed, and shielded from light. O-rings held under compression develop permanent set, so they should lie flat in compartmented bins rather than being stacked or crushed; different specifications must be separated, which colour-coded bins make easy; and rubber items should be stored away from light and heat with receipt date and recommended shelf life recorded.
4. Hygienic Design: CIP/SIP and Aseptic Filling Requirements
CIP and SIP are standardized processes in the beverage industry. A spare-part case is not part of the piping system, but once it enters a clean zone it faces the same cleanability scrutiny.
The core logic of cleanable design matches that of food processing: let the cleaning medium reach every surface and let residue leave.
Specific points:
- Rounded transitions and no dead corners. Avoid right angles and deep textures inside and out to prevent syrup and organic matter retention.
- Liner removable as a whole. Once out, the liner can be washed, air-dried, and UV-sanitized while the shell is rinsed separately, so no closed layer accumulates moisture.
- Drainage. Provide a closable drain port and flow channels at the base so water can be removed on the return leg.
- CIP chemical resistance. Confirm tolerance to sodium hydroxide, nitric acid, peracetic acid, and other common CIP chemicals.
- Dryable and verifiable. Check crevices for residual water with blotting paper after washing rather than judging by feel.
Additional aseptic zone requirements deserve specific mention. Items entering an aseptic area normally pass through a transfer hatch or a sanitizing procedure, so case dimensions must fit the transfer hatch, the shell must tolerate disinfectant wiping, and the materials must not shed particles, which rules out unsealed foam and fragile paper labels. This should be confirmed at project kickoff, otherwise a case may be built that cannot physically enter the aseptic zone.
5. Material Compliance: GB 4806, Stainless Parts, and Seals
Bottling involves many components in direct contact with the beverage, so material compliance receives more attention here than in general food settings.
Where GB 4806 applies:
- The GB 4806 series comprises mandatory national standards for food-contact materials and articles and governs materials that contact food directly.
- Filler valves, valve cores, seals, and pipe fittings that contact the beverage directly must themselves satisfy the applicable food-contact requirements, normally evidenced by compliance documentation from the original equipment manufacturer.
- A spare-part case shell is an indirect-contact or non-contact component and is not normally managed as a food-contact material. If the case is used to hold beverage or concentrate directly, it must then be specified as food-contact compliant.
Practical advice:
- Keep OEM documents with the part. Case design should work alongside the OEM compliance documents for the part so that a complete part, case, and record chain exists.
- The insert does not replace original packaging. Newly purchased valves and seals should retain their original packaging, usually a clean bag, with the insert providing only physical location rather than acting as a cleanliness barrier.
- Avoid sheet from unidentified recycled sources, which can cause odour migration.
- Watch chlorides with stainless parts. Chlorinated sanitizers cause pitting in stainless steel under certain conditions, leaving rust spots after prolonged contact, so chlorinated chemicals should not remain in a case long term.
Wording advice: when explaining the design to an auditor, distinguish clearly between direct-contact parts covered by OEM compliance documents and the transport case, which is an indirect-contact item. Do not claim the entire case is a food-contact material.
6. Shell Material Comparison
Shell material governs impact resistance, chemical resistance, temperature tolerance, and dead weight. The wet-cold and chemical environment of a bottling hall calls for corrosion resistance combined with cleanability.
| Material | Impact resistance | Chemical / cleaner resistance | Temperature range (typical) | Dead weight | Typical use |
|---|---|---|---|---|---|
| --- | --- | --- | --- | --- | --- |
| HDPE | Excellent | Good | -20 C to 70 C | Medium | General spare cases, chilled staging |
| Copolymer PP | Excellent | Excellent | -20 C to 100 C | Medium | High-frequency circulation, near wash-down |
| Glass-fibre reinforced PP | Excellent | Excellent | -20 C to 100 C | Medium to heavy | Heavy valve stacks, drive components |
| Stainless steel (316L) | Medium (dents easily) | Excellent | Wide | Heavy | Fixed station cases in clean zones |
| ABS | Medium | Medium | -20 C to 70 C | Light | Indoor ambient, light loads |
| Aluminium alloy | Medium | Medium | Wide | Medium | Electrical enclosures needing low weight |
Engineering guidance:
- Long-term wet-cold exposure: prefer HDPE or copolymer PP and avoid standard ABS, which embrittles and cracks at low temperature.
- Close to CIP areas: confirm tolerance to alkaline and acidic chemicals, running immersion tests where necessary.
- High opening frequency: reinforcing ribs at hinge bosses and latch points are essential to prevent stress-crack initiation.
- Flame retardance: if the case contains chargers or lithium battery equipment, confirm the material's flame rating, commonly targeting UL94 V-0 or V-2, and obtain the material report.
Where heavy valve stacks must travel between shop floor and warehouse, a case with wheels and a telescopic handle may be worth considering; the structural choices are covered in this guide to protective case wheels and trolley handle configuration. Note, however, that a wheeled case has a different vibration signature from a carried case on steps and ramps, so insert retention should be reinforced accordingly.
7. Insert Design: Round-Bore Retention and Removable Dividers
The insert cushions, locates, and separates. Filler line spares have distinctive insert requirements.
Round-bore inserts are the best format for valves and cylindrical parts:
- Bore diameter is sized to the component outside diameter with 0.5 to 1.5 mm interference per side;
- Bore depth covers 60 to 80 percent of component length, balancing retention against ease of retrieval;
- Leave cushioning margin at the bore base so the end face does not bear load directly;
- Maintain at least 8 mm of wall between adjacent bores so components cannot press on each other in transit.
Removable divider systems suit situations where specifications change frequently. Their locating accuracy is lower than a custom milled insert and the slots trap debris that needs extra attention during cleaning. To combine adaptability with accuracy, use removable dividers together with replaceable milled blocks; the relevant structural choices are covered in this guide to removable divider systems for protective cases.
Insert material. EVA is the first choice, in the 45 to 90 kg/m3 density range with the upper range for valve assemblies to increase grip. Insert materials differ noticeably in compression behaviour and moisture uptake, so it is worth reviewing a comparison of protective case foam materials before fixing a grade. Unsealed EPE or PU foam should be avoided as a clean-zone insert material because its pores absorb moisture and shed particles.
Cleanability. The insert should be removable for washing and drying, and milled bores should not form closed cavities that create uncleaned dead zones. Where bores are deep, provide a through hole at the base to drain water and vent air.
8. Sealing, Dust, and Wash-Down: IEC 60529 and GB/T 4208
The first digit of an IP code indicates solid particle protection from 0 to 6 including dust, and the second indicates water protection from 0 to 9. Common bottling hall needs are:
- IP54: dust protected with limited ingress plus splash resistance, suitable for short indoor transfers;
- IP65: dust tight plus water-jet protection, suitable near wash-down areas where spray may reach the case;
- IP67: dust tight plus temporary immersion, typically 1 metre for 30 minutes, suitable where the case may fall into a wash tank or faces prolonged high humidity.
Three points must be emphasized:
- An IP rating is a conclusion under type-test conditions, not a permanent capability. Gasket ageing, latch deformation, or shell gouging all reduce practical protection.
- IP65 and IP67 differ mainly in water, since both reach dust class 6.
- Distinguish empty-case protection from loaded-case protection. Most tests use a closed empty case; a sharp component pressing on the sealing face defeats actual sealing.
Selection logic for protection class is discussed in this analysis of IP67 protective case design and this guide to choosing a waterproof case IP rating.
The pressure equalization valve is a frequently overlooked detail in bottling halls. If a case moves between high and low temperature, for example from a cold store into an ambient shop floor, the differential pressure deforms gaskets, makes the lid hard to open, and can draw in moisture. Fitting a pressure equalization valve maintains the IP class while equalizing internal and external pressure; the principle and selection points are described in this guide to pressure equalization valves for protective cases.
9. Carbonated Beverage Pressure Components and Pressure Protection
Carbonated bottling involves pressure components including counter-pressure filler structures, pressure gauges, regulating valves, and pipe fittings. Beyond ordinary impact protection, these have three special requirements.
First, pressure components are more sensitive to deformation. A counter-pressure filler valve balances internal pressure to fill, and the roundness of the valve chamber and the flatness of the sealing face directly determine fill accuracy. These parts need one part per compartment, thicker cushioning, and no compression of any kind.
Second, pressure components carry residue risk. Used pressure parts may retain liquid and gas internally, so before transport confirm they have been depressurized, drained, and dried. Transporting under pressure is not only hazardous but creates additional stress as temperature changes.
Third, calibration records matter. Pressure gauges and safety valves require periodic verification, so the checklist should record the calibration expiry date and prevent out-of-date parts from being used. A case can be divided into "awaiting calibration" and "calibrated" compartments distinguished by colour coding.
Where instrument-type components such as pressure gauges travel in the case, provide a dedicated instrument compartment with anti-vibration support so the pointer mechanism does not lose accuracy under vibration.
10. Corrosion and Chemical Resistance: CIP Chemicals, Sugar, and Acid
The chemical environment in a bottling hall includes four main categories:
- Alkaline CIP chemicals, mainly sodium hydroxide, which attack aluminium aggressively, so aluminium parts need caution;
- Acidic CIP chemicals based on nitric or phosphoric acid, which corrode many metals and some plastics;
- Chlorinated sanitizers such as sodium hypochlorite, which cause pitting in stainless steel and accelerate ageing of ordinary rubber gaskets;
- Sugar syrup and acidic beverages, which support microbiological growth on prolonged contact and swell some foam materials.
Handling guidance:
| Exposure type | Preferred materials | Materials requiring caution |
|---|---|---|
| --- | --- | --- |
| Alkaline CIP chemicals | PP, HDPE, EVA | Aluminium, some coated parts |
| Acidic CIP chemicals | HDPE, PP | Carbon steel, some metal inserts |
| Chlorinated sanitizers | PP, HDPE | 316L stainless under long contact, standard nitrile gaskets |
| Sugar or acidic beverage | Sealed EVA, PP | Unsealed EPE, PU foam |
Gasket material should be selected against both chemical and temperature duty. For ambient service, EPDM or FKM works well, with FKM offering better chemical resistance at higher cost. For low-temperature cold-chain service, use low-temperature silicone or a dedicated low-temperature compound so the gasket does not harden and lose resilience.
11. Vibration and Impact Validation: ISTA and GB/T 4857
The typical bottling spare route is spare-parts store to in-plant vehicle to shop-floor workstation, or supplier to long-haul trunking to factory warehouse to shop floor, with a shock signature dominated by low-to-medium frequency vibration and manual handling drops.
Citable test frameworks:
- ISTA series: transport performance validation for packages, covering drop, vibration, and stacking;
- GB/T 4857 series: China's basic test methods for transport packages, covering drop, vibration, and stacking, convenient for domestic acceptance and contract citation. See the key points of GB/T 4857 transport packaging testing;
- ISTA 7D: suited to temperature-controlled transport routes, covering cold-chain distribution temperature simulation.
A recommended validation sequence:
- Define the representative load state, meaning the heaviest combination and least favourable centre of gravity, with components secured as in service.
- Choose drop height from real handling height; manual handling commonly corresponds to 600 to 900 mm.
- Run fixed-frequency or random vibration testing and inspect insert displacement, latch loosening, and witness marks on components.
- Re-test sealing after the sequence to confirm the IP class has not failed.
- For valves and seals, run a post-test sealing or fit check rather than judging appearance alone.
One clarification: MIL-STD-810H and similar standards are often cited as method references, but they are methodology standards and do not constitute military certification. External communication should say "test methods referenced," never "military standard certified."
12. Latch, Hinge, and Gasket Selection
These components set the lower bound of case life and are the concentrated source of complaints about cases failing within six months.
Selection guidance follows the engineering logic in this toolbox hinge, latch, and gasket selection guide. Core conclusions:
- Hinges need a metal core. All-plastic hinges fatigue-crack under frequent opening.
- Latches need secondary security. After an in-plant impact, a single-point latch can pop open; prefer two-point or self-locking designs.
- Gaskets must be replaceable. A gasket is a wear part and should be field-replaceable so the whole case need not be scrapped.
- Match gasket material to temperature and chemicals. EPDM or FKM for ambient service, low-temperature silicone or a dedicated compound for cold-chain duty.
Gasket groove compression ratio is typically held between 20 and 30 percent. Too little compression leaks, too much accelerates permanent set. Where a client wants the ratio optimized for actual duty, JUNZHJIA can supply sample gaskets in several hardness grades for comparative testing and support a sealing re-test on the case.
13. Spare Inventory, Marking, and Traceability Management
Bottling spare parts are characterized by many specifications, small quantities, and high value, so inventory accuracy matters more than inventory volume.
A "one case, one code, one list" system is recommended:
- Numbering. Laser-mark or hot-stamp a serial number on every case and bind it to the asset register.
- Checklist. Include a rewritable checklist card listing component name, model, material, quantity, and compatible machine types.
- Pairing identification. For parts used as a matched set, such as valve cores and seats, record the pairing number on both the checklist and the insert.
- Colour coding. Green for cleaned and available, yellow for awaiting wash, red for awaiting calibration or repair.
- Stocktaking. Sample-count weekly and full-count monthly, with discrepancies entering a traceability process.
For ageing seal items, record the receipt date and recommended replacement interval so that a part stored for three years does not leak the moment it is installed. Rubber items should be stored away from light and heat and free from crushing deformation, ideally in original packaging with periodic hardness spot checks.
14. Acceptance, Cleaning Maintenance, and Life-Cycle Cost
The most common procurement mistake is comparing unit price alone. The true cost of a spare case should be assessed over its full life cycle:
Cost per trip = (purchase price + insert tooling amortization + annual maintenance) / (annual trips x service life in years)
Acceptance should follow a sampling plan, focusing on:
| Acceptance item | Method | Pass criteria |
|---|---|---|
| --- | --- | --- |
| Appearance and burrs | Visual plus hand check of interior | No sharp edges, no flash, no unsealed foam |
| Round-bore fit | Trial-fit the actual valve | 0.5 to 1.5 mm interference per side, no forced compression |
| Sealing class | Test per GB/T 4208 at the specified class | No significant water ingress after test |
| Latch life | Open-close cycling | Function normal after the agreed cycle count |
| Insert retention | Re-inspect after vibration | No displacement, no tearing, no component witness marks |
| Material evidence | Document review | Resin grade and flame test reports complete |
Cleaning maintenance should run on a fixed cycle: empty, wipe, and air-dry after every use; deep clean weekly; inspect gaskets and hinges monthly. Routine methods are described in this guide to cleaning and maintaining protective cases.
For service-life management, the logic in this assessment of protective case service life evaluation is useful: track the three wear parts, the gasket, hinges, and latches, rather than waiting for the whole case to fail.
Frequently Asked Questions
Q: A filler valve drips after being circulated. How can the packaging be investigated?
A: Dripping points to a damaged sealing cone or a deformed valve body, and both usually originate in impact and compression inside the case. Three checks help. First, confirm that each valve occupies its own compartment with sufficient wall thickness between them, recommended at no less than 8 mm. Second, confirm that the end carrying the sealing cone has a 3 to 5 mm cavity and never touches the insert base. Third, confirm that round-bore interference is between 0.5 and 1.5 mm per side, since too loose allows movement and too tight scores the part during insertion and removal. Improvements include switching to a round-bore EVA insert, adding face protection caps, and writing a post-vibration sealing re-test into the acceptance clause. Where parts are ground-matched, provide positions keyed to the pairing number so the matched set is never separated.
Q: Does a beverage bottling parts case need to be IP67?
A: Not necessarily; decide from the actual exposure environment. The second digit of an IP code indicates water protection, increasing from splash resistance to immersion. If the case is only carried short distances indoors, IP54 is usually enough. If it operates near a CIP area where spray may reach it, specify at least IP65, combining dust tightness with water-jet protection. Only where there is genuine risk of falling into a wash tank or short immersion is IP67 justified. Two further points deserve attention: clarify whether the rating applies to an empty or a loaded case, since most tests use a closed empty case, and if the case moves between high and low temperatures, consider fitting a pressure equalization valve so differential pressure does not deform the gasket or draw in moisture.
Q: How should O-rings and seals be stored?
A: The core rules are unloaded, unmixed, and shielded from light. O-rings held under compression develop permanent set, so they should lie flat in compartmented bins rather than being stacked or coiled. Different specifications must be kept in separate compartments, and colour-coded bins make this easy, preventing the mixing that leads to installation failure. Rubber items should be kept away from light, heat, and ozone sources such as electric motors and variable frequency drives, ideally in original packaging. Record the receipt date and recommended shelf life on the checklist, since rubber seals stored for several years should be re-evaluated. Use a blunt tool rather than a sharp pick when removing them so the sealing face is not scored. If the case also serves a clean zone, the bins themselves should be washable.
Q: What additional requirements apply to a case entering an aseptic filling zone?
A: Aseptic areas impose more than ordinary clean zones. Dimensional compatibility comes first: the case must pass through a transfer hatch or sanitizing tunnel, so confirm the clear opening dimensions at project kickoff. Surface sanitizability comes second, meaning the shell must tolerate wiping with the disinfectants in use, and a sealed-edge EVA liner is preferable so no particles are shed. Third, avoid materials that release particles, which rules out unsealed foam, fragile paper labels, and coatings that flake. Fourth, cleaning and drying must be verifiable, with the case and liner fully washable and dry within a defined time. Fifth, records should be traceable, retaining wash, sanitizing, and transfer records for system audits. Write all of this into the technical agreement to avoid building a case that cannot enter the aseptic zone.
Q: Does MIL-STD-810H mean the case holds military certification?
A: No. MIL-STD-810H is an environmental test methodology standard describing how to simulate and evaluate environmental effects. It can serve as a method reference for vibration, shock, and temperature-humidity testing, but it must be described as "test methods referenced" and must never be presented as "military standard certified" or as evidence of military qualification. For beverage bottling parts cases, a more realistic validation path is to cite the ISTA series or the GB/T 4857 series for transport package testing, combined with actual in-plant handling drop heights and transport vibration spectra, and then to run a post-test sealing re-test on the valves, which yields conclusions closer to real service duty.
Q: The lid becomes hard to open after the case moves between hot and cold areas. What is the solution?
A: This is the classic result of differential pressure. When a case leaves a cold store for an ambient shop floor, the air inside warms and expands; moving in the other direction creates internal negative pressure. With good sealing and no equalization path, the pressure difference deforms the gasket, makes the lid hard to open, and under negative pressure can draw in external moisture. The solution is a pressure equalization valve, which allows gas to move slowly in and out while maintaining the IP class and equalizing internal and external pressure. When specifying, confirm the valve's protection class, cracking pressure, and airflow rate, and ensure it is not located where water pools. For bottling spare cases that frequently travel between hot and cold areas, a pressure equalization valve is usually a high-value addition.
Q: Should the insert be milled EVA or a removable divider system?
A: It depends on how stable the spare-part specifications are. For filler valves and seals with fixed specifications, a custom milled EVA insert is recommended: locating accuracy is high, dimensions are stable and unaffected by humidity, the sealed surface is dense and wipeable, and contour support holds the component precisely. If one case must serve many specification combinations, a removable divider system offers more flexibility, though its locating accuracy is lower and the slots gather debris that needs extra attention during cleaning. A middle path is removable dividers combined with replaceable milled blocks, which keeps adaptability while achieving high-precision location at critical positions. Whichever is chosen, unsealed foam should never enter a clean zone.
Q: The case never dries fully after washing. What is the cause?
A: In most cases there is a closed layer or a deep cavity that admits water easily and drains poorly. Three causes are common: a gap between liner and shell with no drainage path; a flat case base with no flow channel so water pools and dries naturally; and milled bores with closed internal cavities from which moisture cannot escape. The remedy is a closable bottom drain with flow channels, through holes at the base of deep bores to drain and vent, and an insert design that avoids closed cavities. After washing, verify crevices and bore bases for residual water with blotting paper and make drying verification a documented step rather than a judgement by feel. For cases entering a clean zone, this step is mandatory.
Q: Should a spare-parts case be fitted with wheels and a telescopic handle?
A: It depends on loaded weight and carrying distance. A case filled with valve stacks or drive components may exceed 25 kg, and wheels with a handle reduce handling injuries and drop risk over longer distances. Three cautions apply. First, a wheeled case has a different vibration signature from a carried case on steps, ramps, and floor joints, so insert retention should be reinforced. Second, wheels and handles are wear parts and should be individually replaceable. Third, if the case must enter a clean zone, wheels and wheel housings are harder to clean and need dedicated attention in the cleaning procedure. For light loads carried short distances, carrying by hand or by two people remains the simpler and more reliable choice.
Conclusion and Further Reading
Selecting a beverage bottling parts case is essentially about achieving high-precision seal protection, hygiene compliance, and fast retrieval at the same time. The implementation path compresses into five steps: build a graded spare inventory, define the material compliance boundary from contact relationships, set the protection class and decide whether a pressure equalization valve is needed based on the exposure environment, solve locating and cushioning with a round-bore insert, and verify through transport testing and acceptance sampling. What determines cost is not unit price but the replaceability of the three wear parts, the gasket, hinges, and latches, along with whether the liner can be removed as a whole for cleaning.
For buyers and maintenance managers, the three most practical rules are: write "one part per compartment and no load on sealing faces" into the technical agreement, write the protection class test basis and post-test sealing re-test into the acceptance clause, and write paired-part numbering into the inventory procedure. With those three in place, a bottling spare case fleet will hold stable performance across wash-down areas, chilled zones, and clean zones.
When a project requires round-bore inserts sized to a specific filler model, gasket selection resistant to CIP chemicals, or OEM/ODM volume supply, JUNZHJIA can provide matching structure drawings, material certificates, and test-basis documents, and can schedule first-article trial fitting to the project timeline.
Further Reading