

The specialized shipping and storage container is a protective enclosure custom-built for non-standard, high-value, or special-environment cargo. Its task is not to "slip on a standard box" but to turn a cargo that no off-the-shelf general case can solve into a standard unit that can be designed on a custom route, verified, mass-produced, and managed long term. A specialized container faces unique envelope, load, environment, or compliance constraints that a general case either cannot fit, cannot protect, or cannot certify. This article unpacks, from a protective-case manufacturer's point of view, the custom route a specialized container should follow in requirement breakdown, boundary definition, material route, internal restraint, marking traceability, stack load, protection grade, interface standardization, prototype verification, military acceptance, and export compliance, and gives procurement a checklist they can drop straight into a technical agreement. It must be stated plainly that this article discusses the packaging container only; the nature, handling, and any defense-trade export of whatever is loaded inside are governed by local regulations and export control requirements, and the container supplier's duty is to translate the customer's special constraints into a mass-producible box structure. JUNZHIJIA manufactures rotomolded and aluminum protective cases over the long term, and the experience below references this kind of volume production process.
Written from the bench of a protective-case manufacturer, this guide deliberately stays within the boundary of the container. It does not describe which special cargo the box holds, how it is handled, or the controls that govern its movement; those sit with the cargo authority and the regulator. What it does offer is the engineering reasoning a buyer can use to turn a vague "make me a custom case" request into a numbered technical agreement, and to ask the right questions when two quotations look identical on paper but diverge sharply on the custom capability they actually deliver. The rest of the article walks the custom route link by link, from requirement breakdown to production acceptance.
The Mission: Turning Non-Standard Cargo into a Manageable Unit
The specialized container faces a specificity problem that "general cases cannot solve" rather than a single trip. On the demand side it must translate the customer's vague "this thing must move" into measurable envelope, load, environment profile, and compliance list; on the design side it must turn those constraints into shell, liner, and interfaces; on the production side it must keep prototype and batch consistent so every box reproduces the verified conclusion; on the management side it must be traceable, sparable, and long-serving. This mission means the core of a specialized container is not "built" but "clearly defined, verifiably tested, stably produced, manageably maintained." Abstracting non-standard cargo into a custom standard unit is the fundamental way to cut special-support complexity, and the basis on which modern custom support moves from item-by-item patch to unit-level management.
Broken down, the mission has four capabilities: definable requirement, verifiable structure, consistent production, manageable life. Definable requirement means the customer's special constraints become numbers not adjectives; verifiable structure means the box passes tests under the real environment profile not verbal promise; consistent production means mold and process make every box reproduce the prototype; manageable life means consumables are traceable and replaceable. The manufacturer must reserve interfaces for these four on the custom route: acceptance clauses mapped to requirements, reports bound to tests, molds mapped to volume, spare numbers mapped to life, all of which are the engineering details that make custom capability real.
Concretely, a specialized container earns its name only when three conditions hold together: the requirement boundary is jointly signed by customer and manufacturer, avoiding "change while building"; the verification report binds to the real batch, avoiding "prototype passed, volume drifted"; the interface is standardized, avoiding "custom means closed" and later no spares. Miss any one and the custom box reverts to a one-off workshop piece, which is exactly the risk custom management was built to remove. The remainder of this article treats those three conditions as engineering requirements with measurable acceptance criteria, so a buyer can specify them in agreement rather than feel, and can reject a quotation that only promises capability in a render.
The Core of the Custom Route: Requirement Breakdown and Boundary
The biggest difference between a specialized container and a general case is that it must break down requirements first, not draw structure first. The customer often gives "this equipment must ship," but what really decides the box is envelope, center of gravity, unit weight, vulnerable points, environment profile, stacking method, and compliance list. The manufacturer should first turn all of these into numbers with a requirement-breakdown sheet: envelope tolerance, load, vibration bandwidth, temperature-humidity range, IP grade, and which certifications. Writing requirements into the technical agreement is more reliable than finding "it also needs salt spray" after prototyping, and aligns with the "define internal module before molding" idea of the tactical hard case.
Requirement breakdown should also define the boundary, that is "what this box does NOT solve." A specialized container often gets endless added requirements because the boundary is unclear, eventually blowing cost and schedule. Therefore the agreement should state: what the container owns (structure, restraint, sealing, marking, compliance) and what the cargo party owns (content handling, declaration, load-fixing details); which environment profiles are in verification and which are explicitly excluded. Writing the boundary clearly is more reliable than arguing "who owns this" at the production stage, and avoids mistakenly pushing cargo responsibility onto the container manufacturer. This is the most front-loaded step of the custom route, and the extension of the "sealed-duty boundary" idea of the ordnance packing box into the custom scene.
A frequently overlooked detail of requirement breakdown is the "change window." Custom projects fear mid-course requirement changes most, so the agreement should set freeze nodes and change costs before prototyping, before pre-production, and before volume, so the customer knows when a change is still cheap and when it reopens the mold. The manufacturer should write the change window into the delivery spec so custom does not become "endless rework." Front-loading the change window into the contract is the core difference of a specialized container over a general case on the management dimension, and the key for the buyer to control budget and schedule, avoiding one verbal "just tweak it" dragging down a whole batch of delivery.
Material Routes: By Load and Environment, Not by Habit
Material choice for a specialized container depends more on specific constraints than a general case. Heavy load with high rigidity picks aluminum or steel-aluminum composite; wet and high-volume picks rotomolded HDPE; high-value low-volume chasing specific strength picks composite fiber; food or medical contact surface adds a compliance layer on top of the material declaration. Material is not "whatever the factory usually uses" but reverse-derived from load, environment profile, and compliance list. Writing the material reason as verifiable force and compliance notes is the core by which a buyer distinguishes a "select-by-experience" quotation, and aligns with the "material serves the military spec" idea of the military rotomolded case.
Whichever material is chosen, the specialized container should place "production consistency" on a par with "single-unit performance." A good block for prototyping is easy; a thousand units all qualified is hard, so the material declaration should bind the process: wall-thickness distribution and cooling curve for rotomold, weld and anodize parameters for aluminum, layup and cure for composite. The manufacturer should state at delivery which parameters decide consistency and provide first-article and periodic sample retention. Writing consistency into the technical agreement is more reliable than finding "this one differs from that one" after volume and then remedying, and avoids a whole batch of non-standard cargo being reworked collectively because of box scatter.
A second material consideration is repair and whole-life cost. Specialized containers are often few in number and high in unit price, so they are more often required to "repair when broken" than "scrap when broken." Aluminum can be field-straightened and patched, rotomold heat-repaired and panel-swapped, composite returned to factory; the manufacturer should advise which material fits the customer's site condition and write replaceable-part numbers into the delivery spec. Front-loading "damaged but recoverable" into material selection is the key that keeps a specialized container at low ownership cost over long service, and avoids a key custom box being damaged with nowhere to repair.
Marking and Visibility: Making the Non-Standard Box Speak
Because a specialized container has a non-standard shape, it is more easily mis-handled and mis-placed in transit, so its marking system matters more than a general case. A qualified specialized container should provide at a readable position: box type and purpose, contents class, weight and center-of-gravity mark, open indicator, stacking limit, compliance mark, and a scannable identity code. Marking should let warehouse, hub, and front personnel complete identification and handling within seconds — see the class from afar, see the contents up close, scan the whereabouts — instead of everyone guessing by shape. Visibility is the cheapest way to cut communication cost across the non-standard support chain, and aligns with the "marking is a management interface" idea of the logistics support box.
Marking materials and process must survive the environment. Specialized containers often go to harsher sites where paper labels fade and peel faster, so identity and class markings should prefer silkscreen, engraving, or weatherproof plates over stickers; the updatable task list can use a clear window card that is both weatherproof and easy to change. The manufacturer should deliver marking maintenance guidance: which marks are fixed, which are field-updatable, and how to verify after update. Writing marking into the technical agreement is more reliable than discovering "can't tell what this box holds" mid-support and then fixing it, and avoids mis-identification causing wrong-load accidents. A specialized container's marking should also highlight center-of-gravity and compliance hints so any handler sees "how to carry, can it stack" before "custom shape."
Beyond the marks themselves, the specialized container should make re-marking a controlled act. When a box is repurposed between tasks, the old class mark must be cleanly removable or permanently overprinted, not taped over. The manufacturer should design the marking surface so updates are deliberate: a recessed window for the swap card, an engraved class code replaced only with an authorized insert. Treating re-marking as a controlled change, like a configuration change on any managed asset, is what keeps a non-standard box honest across years of reuse, and is the "pre-pack, rapid deploy" idea of the deployable hard case landing in the custom scene.
Internal Restraint and Custom Liner
The liner system of a specialized container has one goal: keep the non-standard cargo in its place under vibration and bump, no shift and no collision. Because the cargo shape is unique, the liner is almost always custom: formed brackets of aluminum or engineering plastic slotted to the cargo envelope, EVA/EPE foam for local cushion, straps and restraint blocks for irregular overhangs. The liner is not "stuff it with foam" but assigns force to the cargo's mass center and vulnerable point so transport shock is dispersed and absorbed. Writing restraint as an acceptable displacement is the core difference of a specialized container over a general storage box on the stability dimension, and the link custom work should most invest in.
The trade-off between custom and universal liner depends on whether the cargo is fixed-kitted. Fixed cargo suits CNC-cut or formed brackets with high consistency; if the cargo shape varies slightly between batches, the liner should keep adjustable margin, using zoning logic rather than per-item cutting. Either way, the specialized container should guarantee "pick on open, secure on reset" without special tools, which directly decides restraint quality on the next transit. Writing the reset as a diagram on the inner lid is low-cost and high-return; if reset depends on one specific person, quality drifts when that person leaves, and that is the human-factor risk small-batch custom fears most.
A detail often missed is liner-to-shell coordination. Under vibration a liner that detaches from the shell lets the cargo bounce a second time inside the cavity, so the liner should clamp the shell or form its own shell so restraint does not depend on the shell shape. The manufacturer should give the liner-shell fit tolerance and clamp method, writing "liner stays put" into acceptance rather than discovering "bracket loosened" after transit. Front-loading liner-shell coordination into the structure is the essential action that keeps cargo intact under long-route and bad-road sustained vibration, and the basis the buyer can rely on at inventory, far more than simply filling the box.
Locks and Seals: The Responsibility Chain for Custom Parts
In batch or high-value transit, seal management matters more than for a single box. A specialized container usually has two lock layers: a quick-open latch for daily access, and a numbered seal added at handover. The seal number binds to the handover sheet, and every opening generates a record, ensuring a definite answer to "was it opened." High-value or sensitive batches can upgrade to RFID seals that automatically record time and location at each custody point, turning the responsibility chain from manual check to system trace, reducing human error and raising credibility across multi-unit handovers. This is consistent with the sealed-to-opened traceability of the war reserve case, only the specialized container extends the concern from storage environment to non-standard cargo completeness and responsibility boundary.
Traceability also lives in the identity system. The specialized container should provide both a QR code and an embossed serial on the identification panel, so manual verification survives a scanner outage; a hidden verification code inside the lid guards against malicious replacement of the external plate. This dual identity matters especially in non-standard scenes, because a custom box often crosses many units and years, and any single identity mismatch voids every later record. Front-loading traceability into the box structure, rather than pasting paper after the fact, is the key action within the manufacturer's responsibility boundary and the basis the buyer can rely on at inventory and audit.
The seal should also link to the cargo list. The specialized container seal or list should record pack date and contents class so every handover can check "is this box complete, any missing part." When a batch circulates across years, any mismatch of identity or date voids cargo management, so the identity and list system must be front-loaded into the structure rather than pasted on afterward. High-value batches can upgrade to time-stamped seals that record time at each custody point, turning the cargo responsibility chain from manual ledger to system trace, so "any missing part" has a definite answer and mis-issue risk across multi-unit handovers drops sharply.
Stack and Load Design: Load Path for Non-Standard Shape
Because a specialized container has a non-standard shape, stack and load design relies more on structural analysis than a general case. The load path must be clear: top and bottom stacking bosses must align so load transfers vertically to the main structure, not onto thin walls, latches, or custom bosses; cargo with off-center center of gravity should pull the resultant back to the axis via in-box ballast or restraint, avoidingeccentric load collapse. The manufacturer should give a clear maximum tier and single-tier load, marked visibly, not buried in a manual, especially important for irregular containers because irregular faces often mislead placement.
Load design should also consider the transport interface. The specialized container base should have features that work with pallet straps or rails so a non-standard shape can also be fixed stably; if vehicle-carried, it should reserve forklift slots and lift points so a single heavy box moves safely. This interface looks like a sizing issue but decides whether the non-standard box truly enters containerized logistics. For special support, the transport interface also directly affects rapid loading efficiency, the last mile turning "custom part" into "logistics unit," and it shares the stack-to-pallet discipline of the stackable container, only the specialized container re-designs the load path per irregular cargo.
Load design should also consider the special requirement of long compression. A specialized container stacked in a warehouse may have local compression at the bottom due to irregular contact, so the base should have off-ground support or load-spreading structure to reduce pooled water and rising damp attacking the seal. The manufacturer should state the minimum off-ground clearance and stack-bottom ventilation in the technical agreement. Writing this into acceptance is more reliable than finding the bottom box deformed under compression at the warehouse and then remedying, and avoids a whole stack of non-standard cargo being scrapped in a chain because the bottom box failed.
Protection Grade and Sealing: Grade by Environment Profile
The protection grade of a specialized container should be written as an acceptable IP grade and environment profile, not a vague "splash-proof." Wet transit needs at least IP67, dusty site at least IP65, salt-spray environment needs metal corrosion treatment; the key is uniform gasket compression around the full perimeter and continuity at corners. The gasket material must be a weatherproof elastomer that does not leach or stick to the shell over long use, a point barely asked on general storage boxes but a dust-water floor on specialized containers, consistent with the "grade sealing by environment profile" idea of the temperature-controlled case.
Sealing should also consider opening frequency and maintenance. If a specialized container holds high-value equipment, opening may be frequent, so the latch should give clear feedback when not fully engaged, turning "is it closed tight" into a readable state. Such details look trivial but decide whether the box keeps protection in real use, and are the most worthwhile investment within the manufacturer's responsibility boundary, solving more field failures than simply thickening the wall.
A further key of protection grade is special gas or humidity control. Some specialized containers need humidity control or inert-gas protection, so the seal should carry a balance valve and indicator port so the handler sees the state at a glance. The manufacturer should give desiccant capacity advice and replacement interval, writing "special environment is maintainable" into the technical agreement. Front-loading special-environment control into the structure is the key that decides whether a specialized container keeps cargo intact across climate-spanning transit, and a dimension ordinary cases often ignore.
Interface Standardization: Custom Does Not Mean Closed
The most common way to make a specialized container a "one-off closed part" is to block later spares and upgrades. The discipline of the custom route is: what is custom is the structure and liner; what is standard is the interface and consumables. Divider clips, tray rails, liner clamps, latch and gasket specs should be unified so modules from different batches or suppliers cooperate rather than only the original factory fitting them. Writing interface standardization into the technical agreement is more reliable than discovering "modules not interchangeable" mid-mission, and aligns with the "common unit at hub nodes" idea of the transit case and shipping case.
Interface standardization also brings the benefit of fewer spares. When a module of a specialized container is damaged, the standard part can be replaced alone without scrapping the whole box; when a task changes, only the module changes, not the box. The manufacturer should provide the module interface standard and interchange specification so the site can replace on the spot. Writing module replaceable into the delivery spec is the key that keeps a specialized container at low ownership cost over years of reuse, and avoids one module's failure dragging down a whole high-value box.
A second layer of interface standardization is documentation. Custom projects fear most "the person left and the know-how went with them," so the manufacturer should deliver an interface manual with part numbers and a spare list so the customer can procure by drawing years later rather than depending on one engineer's memory. Front-loading documentation into delivery is what keeps a non-standard box maintainable over long service, and the dimension most easily overlooked yet most affecting whole-life cost at selection.
Verification and Prototype: Prototype Before Volume
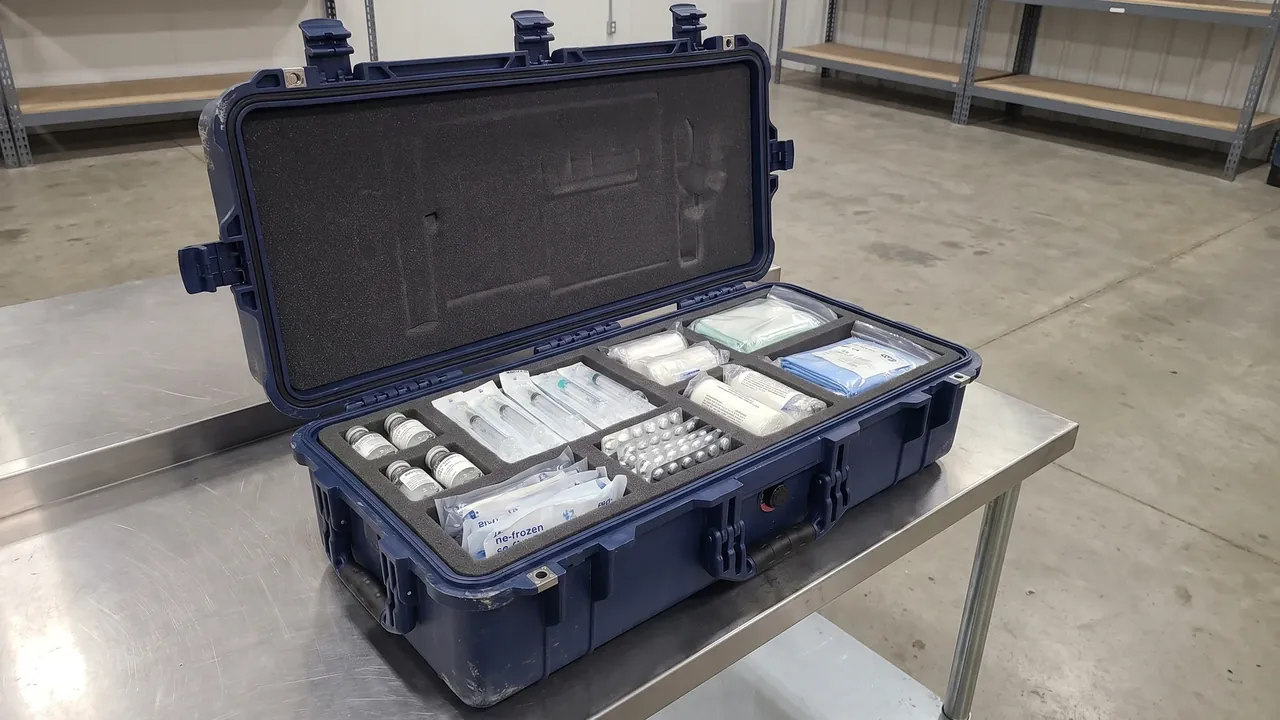
The reliability of a specialized container is written in the discipline of "prototype first, volume second." The prototype stage should do structural verification: load path, stacking, seal compression, and liner displacement should all have measured data, not just a render. The prototype should also do environment-profile pre-test so design flaws surface before volume rather than batch rework after. The manufacturer should make the prototype verification report a precondition for volume, more reliable than stopping the line after "structure wrong" on the production line, and aligns with the "verify load before typing" idea of the heavy-duty protective case.
Prototype verification should also bind to the real cargo. The most common mistake of a specialized container is using ballast instead of the real cargo for prototyping, so the cargo's center of gravity or irregular point is not covered. Therefore the prototype should verify restraint and center of gravity with the real cargo or a high-precision model as much as possible, so volume does not reproduce "prototype stable, real cargo wobbles." The manufacturer should write "real-cargo verification" into the agreement so custom does not become "close enough." Front-loading real-cargo verification into the prototype is the core difference of a specialized container over a general case on the credibility dimension, and the link small-batch high-value cargo should most insist on.
A second layer of prototype is first-article qualification. Before volume, a full first-article qualification should be done, and the first article retained as the baseline for later sampling, so batch consistency has a reference. The manufacturer should provide the first-article report and periodic sample retention, writing consistency into acceptance. Front-loading first-article qualification into volume is the key that keeps a specialized container "every box like the prototype" over a long cycle, and avoids a batch of non-standard cargo failing collectively because of scatter.
Military Acceptance: Mapping MIL-STD-810H to GJB Custom
Military acceptance of a specialized container usually maps to MIL-STD-810H and the corresponding GJB methods, but the profile must be customized to the cargo's real environment, not copied from a general case. Beyond generic drop, vibration, and salt spray, the specialized container should add cargo-related verification such as whether the liner truly kept cargo still under vibration, whether the load path under irregular stacking stayed stable, and the durability floor of latch and marking under salt spray. Turning "custom adaptation" from a claim into a set of acceptable tests is the core by which a buyer distinguishes a custom quote from a general one. The test profile should bind to the real route, because only a profile matching the actual scenario predicts field performance.
Military testing should not be read only for a pass mark, but for whether the report maps to the specific box. The specialized container acceptance report should record: corner deformation at drop, whether the liner truly kept cargo still under vibration, the durability floor of latch and marking under salt spray, and the load transfer under irregular stacking. These findings feed directly back into mold and liner improvement, where the test budget earns its return. A supplier without a report can only promise verbally, with nothing to compare in a dispute; a supplier with a report has committed to specific test conditions checkable line by line. The bound object should be the real batch, not a generic sample, because the consistency of batch specialized containers shows exactly in every box reproducing the report's conclusion.
The deeper value is the improvement loop: aligning field damage with lab failure modes forces mold or liner optimization. For example if a bracket breaks at a corner in transit, the lab should reproduce it with vibration at the same corner, then use the bracket section and clamp as the mold-change basis. Writing this loop into the technical agreement makes the specialized container not "accepted once, then unchanged" but continuously converging with field feedback. This is consistent with the "drive mold iteration by test profile" idea of the military rotomolded case, only the specialized container extends the test goal from general protection to non-standard cargo stability.
Export and Compliance Documents: Trade Requirements for Custom Containers
When a specialized container is exported or moved cross-border with special cargo, its compliance documents are more complex than a general case. Beyond the general UN packaging certification (where applicable), packing list, and material conformity, a custom container also needs a module declaration, a third-party test report number, and traceable batch records so the physical box, certificate, and report correspond one to one. Wooden packaging must meet IPPC fumigation or exemption; metal and plastic focus on material declaration and recyclability marking. The typical failure is document inconsistency: certificate box type, report status, and actually shipped box do not match, often detained at the port. Writing the boundary of "container compliance" versus "cargo compliance" clearly is the premise that defense-trade export avoids responsibility disputes.
Export should also separate the boundary of "container compliance" from "cargo compliance." The specialized container manufacturer is responsible only for the container's structure and sealing; the cargo compliance is the cargo party's, and the two must not be confused. Therefore the technical agreement should state which module declarations the container provides, who issues them, and for how long, while the cargo compliance is separately the buyer's or cargo party's responsibility. Writing the boundary clearly is more reliable than arguing "who owns this box" at the port, and avoids mistakenly pushing cargo responsibility onto the container manufacturer. It must be restated that this article discusses the container only; export is governed by local regulations and export control requirements, and the manufacturer's duty is to build compliance into the box, not to replace the cargo or regulatory body.
In practice, the specialized container export documents should attach a list-style annex stating version, validity, and issuing body, re-verified against the certificate before each production, starting paperwork two weeks early typically halving clearance time. The specialized container's multi-batch, long-cycle nature makes document version management more critical than single-batch export: the same box type in different years may correspond to different test standards, and if documents are not updated per batch, an old report with a new box fails at the port. Binding the document version to the production batch is the most overlooked yet most fatal link in specialized container export compliance.
Life Cycle and Spares: Long-Term Management of Small-Batch High-Value
Specialized containers are mostly small-batch high-value, so life-cycle and spare management matter more than a general case. A custom box may serve ten years, during which latch, gasket, and liner modules all age; without replaceable-part numbers, a whole high-value box is scrapped over one small part. The manufacturer should deliver a complete spare list with part numbers at delivery so the customer procures by drawing rather than verbal inquiry. Front-loading spares into delivery is the key that keeps a specialized container at low ownership cost over the whole cycle, and avoids a key custom box being out of service for a missing part, exactly the management action small-batch scenes should most use.
Life-cycle management should also include aging visibility. The specialized container should turn easily aged parts into visible maintenance nodes: gasket press-back, latch feel, marking clarity should all have on-site criteria. The manufacturer should provide a recommended inspection interval and spare list so the customer can do a minimal check before the task. Writing aging visibility into the technical agreement is more reliable than finding "the box should have been replaced long ago" at the task site, and avoids a whole batch becoming unusable in a chain because one consumable failed.
A further key of life cycle is document retention. Custom projects fear most "the person left and the art died," so the manufacturer should deliver an interface manual with part numbers, a spare list, and acceptance reports that stay retrievable with the box or contract long term. Front-loading document retention into delivery is what keeps a non-standard box maintainable years later, and the dimension most easily overlooked yet most affecting whole-life cost at selection, avoiding one personnel change making a whole batch of custom unmaintainable.
Procurement Checklist: Writing "Custom Case" into a Technical Agreement
Buying a specialized container should not stop at "make me a box" but turn every line above into an acceptable clause. The checklist should at least include: requirement-breakdown sheet and boundary definition, material reason and consistency process, liner typing and reset method, stacking tier and load path, transport interface and center-of-gravity control, seal and dual-identity traceability, readable marking positions and weatherproof process, IP grade and environment profile, interface standardization and spare part numbers, prototype verification and first-article qualification, military test profile with bound batch, and export document list with version management. Writing this list into the technical agreement gives the buyer the right to question quotations rather than picking boxes by feel at acceptance.
Procurement should also write "change window" and "whole-life cost" into the requirement. The real cost of a specialized container is not the prototype unit price but whether it can clearly define requirements, stably produce, long sparable, and control change cost. Once those numbers are estimated honestly, every line of the checklist gains a budget anchor. It must be restated that this article discusses the packaging container; cargo storage, transport, and export are governed by local regulations and export control requirements, and the container manufacturer's duty is to translate the customer's special constraints into a mass-producible box structure, not to replace the cargo or regulatory body. Writing the checklist into the agreement is the first step that turns "custom support" from a slogan into an auditable engineering fact.
Frequently Asked Questions
Q: Why must a specialized container break down requirements first; can it not just draw structure? A: Because what a specialized box must solve is not "fits" but "all non-standard constraints met," and drawing structure directly inevitably misses items — envelope tolerance, center of gravity, unit weight, vulnerable points, environment profile, stacking, and compliance, any un-quantified one causes rework after prototyping. Requirement breakdown turns these into numbers in the agreement so the buyer can distinguish "real custom" from "guess by experience" with acceptable clauses. The typical field failure is the customer saying "this equipment must ship," the factory building by habit, then finding at salt spray or vibration that it was never verified, doubling the rework cycle, with the responsibility boundary already blurred because "requirements were never written." Front-loading requirement breakdown is more reliable than finding "it also needs salt spray" after prototyping, and avoids budget being endlessly added. A practical tip is to require the breakdown sheet as a signed appendix before any deposit, because a vague mandate almost always hides a profile that surfaces only at the test chamber, where fixing it costs ten times the prototype.
Q: Why does a specialized container liner stress shell coordination rather than stuffed foam? A: Because non-standard cargo has a unique shape, and under vibration a liner detached from the shell lets the cargo bounce a second time inside the cavity, losing all restraint. A coordinated liner clamps the shell or forms its own shell so restraint does not depend on the shell shape, keeping cargo in place under vibration. The manufacturer should give liner-shell fit tolerance and clamp method, writing "liner stays put" into acceptance rather than discovering "bracket loosened" after transit. At acceptance the buyer should remove and refit the liner once without tools and confirm no looseness, not only checking restraint, because a well-restrained but loose liner will expose shift risk on the long route. A general storage box only wants filling; the specialized container wants zero second bounce of non-standard cargo under vibration, which is the core stability difference and the link custom work should most invest in yet quotations most often omit, so it must be written into the technical agreement without fail.
Q: How does a specialized container avoid "custom means closed" blocking later spares? A: The discipline is: what is custom is structure and liner; what is standard is interface and consumables. Divider clips, tray rails, liner clamps, latch and gasket specs should be unified so modules from different batches or suppliers cooperate rather than only the original factory fitting them. The manufacturer should provide interface standard and interchange specification so the site can replace on the spot, and write spare part numbers into the delivery manual. Field experience is that a closed-custom box with one broken module must return to factory in months, while a standard-interface box swaps on site in hours and can still be procured by drawing years later. Writing interface standardization into the agreement is more reliable than discovering "modules not interchangeable" mid-mission, and avoids a small-batch high-value box being out of service over one consumable, exactly the discipline custom management should most insist on, paid by the support unit rather than the factory.
Q: What documents differ from a general case when a specialized container is exported? A: Beyond the general packing list and material conformity, a custom container also needs a module declaration, a third-party test report number, and traceable batch records so the physical box, certificate, and report correspond one to one; wooden packaging needs IPPC fumigation or exemption, metal and plastic focus on material declaration and recyclability. The biggest failure is document inconsistency: certificate box type, report status, and shipped box mismatch often get detained. Also separate "container compliance" from "cargo compliance" — the manufacturer only owns the container structure, the cargo compliance is the cargo party's, and the agreement must state who issues which and for how long. The specialized container's multi-batch long cycle means the document version must bind to the production batch; an old report with a new box fails at the port, and starting paperwork two weeks early typically halves clearance time. A sound practice is to attach the document annex with version, validity, and issuing body, and re-verify against the certificate before each new production.
Q: Why should a specialized container stack also consider the load path? A: Because a non-standard shape often misleads placement; if load presses on thin walls, latches, or custom bosses rather than the main structure, the stack collapses under eccentric load. The specialized container should clarify the load path: stacking bosses aligned, off-center cargo pulled back to axis via restraint or ballast. The manufacturer should give stacking tier limit and single-tier load marked visibly, not only in the manual. A further point is that the load path must be checked against the real center of gravity, not the geometric center, because an irregular box often looks balanced while the mass sits to one side. The field lesson is an irregular box stacked by shape, bottom locally compressed and deformed, a whole stack of non-standard cargo scrapped in a chain; writing load path and off-ground clearance into the agreement is more reliable than opening boxes afterward, and avoids the bottom box failing from local contact, exactly the extra design a specialized container should do over a general case on the load dimension, which quotations routinely skip.
Q: Why should a specialized container seal preferably carry a time stamp? A: Because a specialized container circulates across many units and years, a seal numbered but not timed breaks the responsibility chain — you do not know when this box was sealed, opened how many times, or any missing part. A time-stamped seal records time and location at each handover, giving a definite answer to "is it missing parts, was it opened midway," turning the duty from manual ledger to system trace and markedly cutting mis-issue and missing-part risk across multi-unit handovers. High-value or sensitive batches should upgrade to RFID seals so turnover records are one-click. Dual identity (QR plus embossed serial plus hidden lid code) defends against external plate replacement, verifiable even if any single point fails. Linking the seal to the cargo list and writing it into the structure is the essential difference of a specialized container over a general storage box on the traceability dimension, and the one that survives the multi-year, multi-unit reality of custom support.
Q: Can a specialized container be civil-military common to cut total cost? A: Yes, and it should be. Field transit of power, communication, and medical equipment equally needs custom restraint, protection grade, and traceability, differing only in marking class and dispatching body, so the specialized container's modularity and standard interfaces can migrate directly to the industrial system, letting the two share production and spares and cut total cost of ownership. The manufacturer should reserve interfaces for "civil-military common structure" rather than making two incompatible molds. The civilian scene should also stress reachability: marking highlights how to carry and reset, with multilingual or pictogram card positions so cross-region support needs no repaint. Writing "readable by civilians" into the design is the last mile taking the specialized container from military to industrial public service, and the key to its real scaled-reuse value, avoiding dual-tooling that wastes the most money over a decade of service, exactly where civil-military common structure pays back fastest across both systems rather than duplicated tooling.
Q: Why should a specialized container's military test not copy a general-case profile? A: Because a specialized box's environment profile is decided by the cargo's real route, and copying a general-case profile inevitably misses irregular stacking, non-standard center of gravity, or special sealing, so the test passes yet the field still fails. The specialized container report should record whether the liner truly kept cargo still under vibration, whether the load path stayed stable under irregular stacking, and latch and marking durability under salt spray; these findings feed directly back into mold and liner improvement, where the test budget earns its return. A supplier without a report can only promise verbally, with nothing to compare in a dispute; a supplier with a report has committed to specific test conditions checkable line by line. The report should also bind to the real batch rather than a generic sample, because the consistency of batch specialized containers shows exactly in every box reproducing the conclusion. The deeper value is the improvement loop: aligning field damage with lab failure modes forces mold change, so the specialized container converges continuously with feedback rather than staying unchanged after one acceptance, which is the only way bulk custom enclosures stay trustworthy across years of circulation.
Closing
The reliability of a specialized container is written into every detail of requirement definition and interface standard: clear boundary, verified test, stable volume, managed life. Buy it as a custom-management system, not as a sturdier hand-made box. Related Reading: Military Rotomolded Case, Stackable Container, Equipment Case and Gear Case.