

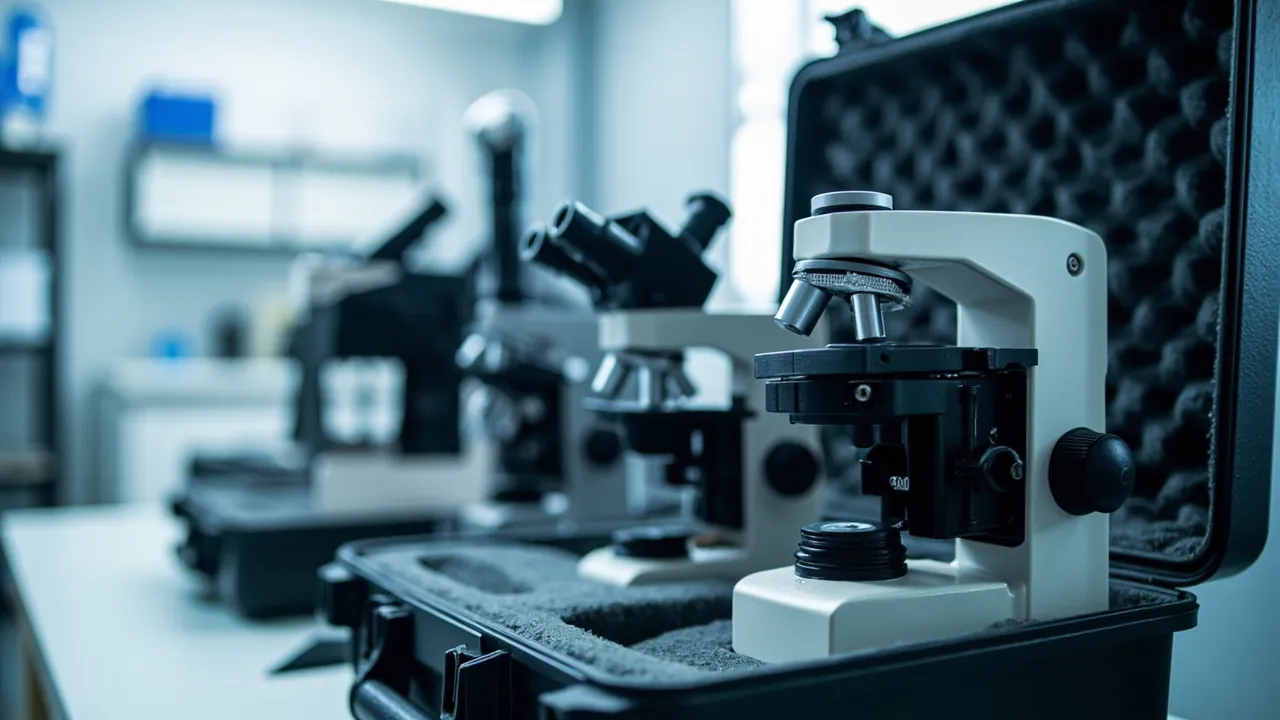
A microscope is the archetypal high-precision mechanical and optical instrument in a laboratory, and its transport protection problem is this: within one instrument, optical accuracy and mechanical accuracy are carried by the same set of fragile mechanisms. The objective lens embodies optical performance, and once its lens surface, thread fit or parfocal relationship is damaged, image quality cannot be restored. The stage and focusing mechanism embody mechanical accuracy, and once their guideway clearance, rack and pinion pair or fine-focus reduction gearing loses position, the original resolution and repeatable positioning accuracy can never be recovered. The correct selection logic for a microscope case is therefore four parallel threads: integral rigid support, dedicated objective lens cavities, motion mechanism restraint, and humidity control with mould prevention, rather than treating a microscope as a fragile instrument to be simply cushioned.
The practical pain points cluster in five areas. The first is objective lens contamination and damage. Objectives are the most frequently mishandled part of a microscope, with on-site staff commonly wiping them with ordinary lens paper or clothing and scratching the front element coating; in transit, if objectives are not individually protected, settled particles and mutual impact cause the same coating damage. The second is loss of the parfocal relationship. Parfocality, meaning an image that stays essentially in focus when objectives are changed at the same focal setting, depends on precise matching between thread face and objective length. Once an objective takes a shock that deforms the barrel or damages the thread, parfocality drifts and the user must refocus after every change. The third is loss of position in the stage and focusing mechanism. Long-term static load and vibration change guideway preload, wear the rack and pinion unevenly and increase fine-focus backlash, while handling impacts deform the stage or permanently change the distance between stage and objective. The fourth is mould growth on optical elements. Lens groups kept in high humidity develop mould, and mould spots corrode coatings and create permanent scattering; this is the most common microscope failure mode in the humid south of China and in Southeast and South Asia. The fifth is damage to illumination and power accessories. Light housings, condensers, filters, power adapters and cabling are all high-impact-probability items in transit.
This article works through the protection logic in the order of objective lens, stage and focusing, illumination and accessories, vibration, dust and mould prevention, sealing and humidity control, and testing and acceptance. It provides a microscope type comparison table, an objective and mechanism protection table, cleanliness and mould prevention points, sealing class recommendations, a transport test plan and a specification selection table. JUNZHJIA serves microscope manufacturers, laboratory instrument distributors, third-party testing laboratories, universities and research institutes and instrument rental services with case and insert design, dedicated clean objective cavities, motion mechanism restraint schemes, model-matched isolation and humidity configurations, and OEM/ODM volume delivery, manufactured and shipped worldwide by Kexin New Materials (Guangdong) Co., Ltd.
Table of Contents
- 1. Why Microscopes Need Purpose-Built Cases
- 2. Risk Profile: Failure Modes of Objective Lens, Stage and Focusing Mechanism
- 3. Microscope Types and Their Differing Protection Needs
- 4. Objective Lens Protection: Optical Surface, Thread and Parfocality
- 5. Stage and Focusing Mechanism: Accuracy and Loss of Position
- 6. Illumination, Condenser and Power Accessories
- 7. Vibration Isolation and Cushioning: Graded Design
- 8. Cleanliness, Dust Prevention and Mould Prevention
- 9. Humidity Control and Long-Term Storage
- 10. Sealing Class: How IEC 60529 and GB/T 4208 Apply
- 11. Custom Inserts and Cavity Schemes
- 12. Transport Testing: ISTA, GB/T 4857, ASTM D4169 and the MIL-STD-810H Note
- 13. Marking, Documentation and Accessory Management
- 14. Procurement Acceptance, AQL, Selection Table and Export Reassembly
- Frequently Asked Questions
- Conclusion & Related Reading
1. Why Microscopes Need Purpose-Built Cases
The starting point for understanding microscope transport protection is the fact that optical accuracy and mechanical accuracy share the same set of fragile mechanisms.
The objective lens carries optical accuracy and is the most easily damaged part. A microscope usually carries three to six objectives with magnifications from a few times to one hundred times. Objectives have these characteristics: the front element is exposed and small, so any contact can damage the coating; the barrel is slender with a precision thread, so shock deforms the barrel or damages the thread; parfocality depends on length accuracy, so a length change causes drift; and internal lens groups are cemented assemblies, so rapid temperature change and prolonged high humidity degrade the cement and promote mould. Once damaged, an objective is usually replaced whole rather than repaired, and a high-power objective can account for a significant share of the instrument cost.
The stage and focusing mechanism carry mechanical accuracy. The resolution and usability of a microscope depend largely on two mechanisms: stage movement quality, covering smooth travel, repeatable positioning and freedom from sticking, and focusing quality, covering coarse and fine adjustment interaction, the smallest resolvable fine-focus displacement and freedom from backlash. These mechanisms comprise guideways, ball or sliding fits, rack and pinion pairs and worm, harmonic or planetary reduction. Their accuracy depends on the original state of the mating surfaces and the stability of preload. Vibration in transit changes preload, shock brinells guideways or damages gear flanks, and sustained static load causes local wear. The loss of accuracy is gradual: the instrument still works, but its usability and measurement capability have declined.
Both are carried by the same body structure, so the whole instrument must be considered. The microscope body, comprising pillar, arm and base, is the common datum for objectives and stage. If the body deforms, the relationship between them changes. Protecting only the objectives or only the stage is therefore insufficient; integral rigid support is the foundation.
The use scenario sets the practical standard. Microscope use varies widely. University and research institute microscopes often stay fixed in a laboratory, moving rarely but over long distances when they do. Third-party testing laboratories and instrument rental companies need frequent turnover, so the case must support repeated opening and fast reassembly. Teaching institutions buy in bulk, distribute centrally and store long term, where the mould prevention requirement for storage often exceeds that for transport itself. Industrial sites such as metallography and semiconductor inspection move microscopes between site and laboratory, needing clear on-site unpacking and rapid calibration requirements. The case design must match these different usage patterns rather than offering one generic solution.
Arrival calibration cost must be counted. A microscope normally needs objective parfocality, stage movement, focusing feel and illumination uniformity checked on arrival, sometimes with a manufacturer engineer on site. Counting calibration and downtime cost into the packaging decision is the most frequently overlooked judgement in procurement.
In summary, the core requirements for a microscope case are integral rigid support, dedicated clean objective cavities, motion mechanism restraint and fixation, and comprehensive vibration, moisture and mould protection. A general selection framework is in the Instrument case selection guide.
2. Risk Profile: Failure Modes of Objective Lens, Stage and Focusing Mechanism
The microscope logistics chain is typically: manufacturer, distributor or agent, then end user in a university laboratory, testing body, hospital or industrial site, with some scenarios also involving rental turnover and exhibition shipping.
| Chain stage | Dominant stress | Typical consequence | Protection focus |
|---|---|---|---|
| --- | --- | --- | --- |
| Factory dispatch | Shock, vibration, temperature swing | Objective impact damage, body deformation, focusing looseness | Integral rigid support, dedicated objective cavities, mechanism restraint |
| Distributor warehousing | Long-term static load, humidity, temperature swing | Optical mould, cement degradation, local guideway wear | Humidity and mould control, avoid static load, correct attitude |
| Long-haul road and rail | Low-frequency vibration, random shock | Objective thread damage, parfocal drift, increased fine-focus backlash | Multi-axis location, graded cushioning, mechanism fixation |
| Sea and air freight | High humidity, heat, condensation, repeated handling | Mould, condensation, coating hydrolysis, housing corrosion | IP67 plus pressure equalisation plus desiccant |
| User installation on arrival | Handling, unpacking, abrupt environment change | Objective contamination, condensation, illumination damage | Clean unpacking, temperature equalisation, staged unwrapping |
Objective failure runs along two lines, optical and mechanical. On the optical side: front element coating scratches from contact with hard objects or improper wiping, coating hydrolysis in high humidity, degradation of the cemented layer under prolonged heat and humidity, and mould whose organic acids corrode the coating. On the mechanical side: barrel deformation from shock, which displaces internal lenses and shifts the optical axis; thread damage, which prevents proper threading or produces eccentricity once threaded; parfocal length change; and damage to the housing and knurling that affects handling. Both lines share one feature: the damage is irreversible. On site only cleaning is possible; repair means returning the objective to the factory or replacing it outright.
Stage failure takes the form of reduced accuracy. Common failures are changed guideway preload, felt as looser or stiffer travel with play; brinelling of guideway races, felt as periodic hesitation during travel; damage to screw or rack and pinion flanks, felt as uneven travel with noise; stage deformation, which appears as focal plane drift over a large travel range, meaning the stage is no longer flat; and deformation of travel stops or locking devices. Focal plane drift is particularly insidious in use: users notice they must keep adjusting focus when viewing a large specimen, but can rarely tell whether the cause is the stage or an uneven sample.
Focusing failure takes the form of backlash and changed feel. A focusing mechanism normally has coarse adjustment through rack and pinion or friction drive and fine adjustment through worm, harmonic or planetary reduction. Common failures are increased fine-focus backlash, felt as obvious lost motion when reversing direction; coarse focus creep, where the head slowly descends after the knob is released, which is among the most disruptive faults in use; noise or sticking in the fine focus; and damage to the focusing knob bearings. Coarse focus creep is mostly caused by gear pair wear or insufficient preload, and the original preload state is precisely what transport most easily disrupts.
Illumination and condenser systems are a high-impact-probability zone. Light housings with halogen, LED or mercury sources, condensers, filters, field and aperture diaphragm adjustment mechanisms are all easily struck in transit. Once the centring mechanism of an adjustable condenser deforms, field illumination uniformity falls. Filters are thin glass and break very easily. Gas discharge lamps such as mercury sources are shock-sensitive and contain high pressure, and transport must follow the manufacturer requirements.
Accessory and cable risk is often underestimated. Eyepieces, camera adapters, cameras, stage drive handles, power adapters and cables easily collide with the body in transit. Repeated cable flexing breaks conductors internally, and camera adapters are precision optical items vulnerable to contamination and impact.
3. Microscope Types and Their Differing Protection Needs
Microscope types differ significantly in protection requirements and must be designed separately.
Upright biological microscopes are the most common type, comprising base, pillar, arm, stage, objective nosepiece, tube and eyepieces. Their characteristics are a tall body with a high centre of gravity and limited resistance to tipping, a cantilevered nosepiece that takes load under shock, and a large flat stage vulnerable to compression in the stage plane. Protection focus: low centre of gravity fixation, local reinforcement around the nosepiece, no compression on the stage, and overall tilt restraint.
Inverted microscopes have objectives facing up and the stage above, so the structure's centre of gravity and load paths differ. Their characteristics are an open space between stage and objectives that admits foreign objects, a large stage with a large load-bearing area, and a fragile long working distance condenser in some models. Protection focus: temporary covers over open areas, stage restraint and independent condenser protection.
Stereo microscopes are usually compact with fixed or zoom objectives and a long-travel elevation mechanism plus long working distance. Their characteristics are a long-travel elevation column and focusing mechanism that can slide in transit, and a complex internal lens group in continuous zoom models that is shock-sensitive. Protection focus: elevation mechanism locking or restraint and local protection of the zoom lens group.
Metallurgical microscopes used for metal analysis usually carry reflected illumination, long working distance objectives and a large stage. Their characteristics are many internal lenses in the reflected light path, vulnerable to contamination, a large, heavy precision stage, and polarising and darkfield accessories that are precision optical modules. Protection focus: clean protection of the light path, load-bearing support for the large stage, and dedicated accessory cavities.
Confocal and fluorescence microscopes are high-end instruments containing a laser, a scanning head, filter wheels, detectors and a precision motion stage. Their characteristics are a shock-sensitive laser, protected by the same logic as laser equipment; a scanning head containing galvanometer mirrors or a spinning disk, vulnerable to vibration; filter wheels and detectors that are precision modules vulnerable to contamination and static; and high overall value, making them most sensitive to transport risk. Protection focus: high-grade isolation, attitude fixation, dedicated module cavities, ESD protection and clean humidity control.
Digital and all-in-one microscopes, including digital microscopes and teaching units, are usually integrated assemblies with display, camera module and light source. Their characteristics are a display vulnerable to compression and cracking, a camera sensor vulnerable to static and contamination, and an integrated lens vulnerable to impact. Protection focus: independent display protection with no shared cavity with hard objects, ESD protection for the sensor, and lens window protection.
| Microscope type | Most fragile parts | Main failure modes | Protection strategy | Key prohibitions |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Upright biological | Nosepiece, objectives, stage | Nosepiece deformation, objective damage, stage deformation | Low centre of gravity fixation, nosepiece reinforcement, no load on stage | No inversion, no load on the stage |
| Inverted | Long working distance condenser, stage | Foreign objects in the open area, stage load, condenser damage | Covers over open areas, stage restraint, condenser protection | No foreign objects in the open area |
| Stereo | Elevation column, zoom lens group | Mechanism sliding, lens group shock damage | Elevation locking, local cushioning of the lens group | No free sliding of the elevation mechanism |
| Metallurgical | Reflected path lenses, large stage, accessories | Light path contamination, stage load, accessory damage | Clean light path protection, stage load bearing, separate accessories | No polarising or darkfield accessories sharing a cavity with heavy items |
| Confocal and fluorescence | Laser, scanning head, filter wheel, detectors | Laser misalignment, scanning head vibration, module contamination and ESD | High-grade isolation, attitude fixation, dedicated module cavities, ESD protection | No inversion, no shared module cavities |
| Digital and all-in-one | Display, sensor, lens window | Screen cracking, sensor ESD damage, lens scratching | Independent display protection, ESD protection, window protection | No display sharing a cavity with hard objects |
4. Objective Lens Protection: Optical Surface, Thread and Parfocality
Objective protection means protecting three mutually independent performance lines.
Line one: the optical surface of the front element. The front element is closest to the sample and is typically only a few millimetres across, exposed at the front of the barrel. Its risks are coating scratches from contact with hard objects, improper wiping or collisions between objectives; coating hydrolysis under prolonged high humidity; organic contamination from fingerprints, oil and deposited packaging outgassing; and mould, which grows on the lens surface and secretes organic acids that corrode the coating. Protection points: objectives must each go into a dedicated objective box or cavity, with the front element never contacting packaging material directly; the cavity should use low-outgassing, low-shedding insert material so nothing deposits on the front element; and the cavity should contain desiccant and remain sealed.
Line two: mechanical integrity of barrel and thread. An objective threads into the nosepiece, and thread fit accuracy determines optical axis concentricity. Risks are radial shock deformation of the barrel, which displaces internal lens groups and shifts the optical axis; thread impact damage, which prevents proper threading or produces eccentricity; and damage to knurling and housing affecting handling. Protection points: objective cavities should form surface contact rather than point contact; objectives must be isolated from one another to prevent collision; never place several objectives loose in one cavity; and never share a cavity with tools or metal accessories.
Line three: parfocal length accuracy. Parfocality means the image stays essentially in focus when objectives are changed at the same focal setting, and it depends on each objective having a consistent distance from mounting datum to front focal point. That accuracy depends on barrel length and thread face machining precision. The transport risk is axial compression of the barrel changing length, or impact damage to the thread face datum. Protection points: no axial compression of any kind may be applied to an objective, including packing with soft material; objectives should be supported at the mounting datum or the middle of the barrel, never loaded at the end face; and the objective box itself must be fixed and must not move freely inside the case, since a free box develops a much higher relative velocity under shock and its end faces take far greater impact than in a fixed state.
On the boundary of objective cleaning and use. The correct on-site response to contamination is to remove particles first with a blower or soft brush, then wipe gently in a single direction with dedicated lens paper and solvent. Never wipe while particles are present, since that grinds the coating with the particles, and it is wise to handle low-power objectives, which are cheaper and easier to replace, first and to treat high-power objectives with caution. The case design should support that habit by providing a dedicated clean consumables cavity holding a blower, soft brush, lens paper and solvent bottle, so staff do not improvise with clothing or ordinary tissue.
5. Stage and Focusing Mechanism: Accuracy and Loss of Position
The stage and focusing mechanism embody mechanical accuracy, and protection means limiting load paths and fixing moving parts.
Stage protection points. First, no compression on the stage surface. A stage is a plate on a cantilever or slide and has limited bending strength. If other components press on it, or the case takes a stacking load, the surface bends slightly and focal plane drift appears. No storage cavity or load-bearing structure may therefore be placed above the stage. Second, restrain the degrees of movement. Before shipping, move the stage to a mechanically safe position, typically the middle of travel or the position the manufacturer specifies, and fix it with a lock or travel restraint, so that it does not slide freely on the guideways and repeatedly strike the stops, which accelerates guideway wear. Third, protect drive handles and stops. Handles are protruding structures easily deformed or bent by lateral impact and need a dedicated cavity or a guard. Fourth, avoid uneven guideway loading. Support points should be distributed under the load-bearing region of the stage rather than supporting one end and creating a cantilever.
Focusing mechanism protection points. First, restrain vertical movement of the tube or head. With the mechanism released, the head can normally move freely vertically, which is exactly the function that produces coarse focus creep. Without fixation in transit, the head moves up and down repeatedly with vibration, accelerating wear of the gear pair and guideways and potentially causing permanent clearance change. The focusing mechanism should therefore be fixed with the locking device or a travel stop as the manufacturer instructs; where no factory lock exists, the top restraint of the insert can limit head movement. Second, avoid load on the focusing knobs. Knobs are protruding structures vulnerable to lateral impact and need a dedicated cavity or guard. Third, avoid body deformation. The body, comprising pillar and arm, is the common datum for objectives and stage, and if it takes load in transit through an unsuitable attitude such as lying on its side or inverted, the overall geometry changes. The microscope should therefore travel upright with tipping restrained.
Two easily overlooked details. The first is the objective nosepiece. It is a cantilever carrying the heaviest high-power objective, making it more shock-sensitive than the body. The practice is to increase support density under the nosepiece region and to rotate the objectives to the position where the centre of gravity sits closest to the body, usually with the shortest objective facing forward or as the manufacturer specifies, reducing cantilever moment. The second is the eyepiece and tube. Eyepieces are usually push-fit and will work loose and collide unless restrained, and a tilting tube also needs fixation. Either remove detachable parts and pack them separately, or lock them as the manufacturer instructs and record the state.
| Mechanism | Key accuracy parameter | Transport risk | Protection point | Key prohibitions |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Stage | Travel smoothness, repeatable positioning, flatness | Surface bending, guideway brinelling, handle deformation | No load on the surface, move to safe position and lock, handle guard, support under load-bearing region | No storage cavity above, no free sliding |
| Coarse focus | Creep, consistent feel | Gear wear, preload change | Lock as instructed, top restraint limiting head travel | No shipping unfixed |
| Fine focus | Smallest resolvable displacement, backlash | Increased backlash, sticking, noise | Mechanism fixation, local reinforcement, no load on the knob | No load on the knob |
| Objective nosepiece | Positioning repeatability, concentricity | Cantilever deformation, datum damage | Local reinforcement, objectives rotated to a low-moment position | No long objective left cantilevered outward |
| Body and pillar | Geometric datum stability | Deformation changing overall geometry | Travel upright, tipping restrained | No side-lying, no inversion |
| Detachable parts | Assembly accuracy | Working loose, collision, loss | Remove and pack separately, or lock as instructed and record | No loose packing inside the case |
6. Illumination, Condenser and Power Accessories
Illumination and accessories are a high-impact-probability zone that whole-instrument thinking easily overlooks.
Light housings and lamps. Risks to halogen and LED housings are housing impact damage and lamp breakage. Gas discharge lamps such as mercury sources contain high pressure and are shock-sensitive, so transport and storage must follow the manufacturer requirements and accompanying compliance documentation must travel with the goods. Protection points: a dedicated cushioned cavity for the light housing, lamps packed separately or carried in original packaging, and no shared cavity with heavy items.
Condensers and diaphragm mechanisms. A condenser is usually an adjustable centring assembly with lenses, adjustment screws and sliding fits. Deformation of the centring mechanism causes uneven field illumination, and this deformation is hard to detect on arrival. Protection points: a dedicated cushioned cavity for the condenser, no lateral force on adjustment screws, and adjustable structures fixed or set to the mid position as the manufacturer instructs.
Filters and optical accessories. Filters are thin glass and crack very easily under compression, and polarisers, darkfield stops and phase rings are equally fragile. Protection points: a dedicated thin-plate cavity with isolating soft pads and no stacking, no shared cavity with heavy items, and easy counting.
Power adapters and cabling. Adapters are separate items that easily collide with the body, and repeated cable flexing breaks conductors internally. Protection points: a dedicated fixed cavity for the adapter, controlled cable coil radius with protected connectors, and no direct chafing against the body, which can be prevented with a soft barrier layer.
Camera adapters and cameras. Camera module sensors are static-sensitive and the adapter is a precision optical item. Protection points: ESD-safe packaging, for which the design thinking in ESD shielded protective case design is relevant; protective caps on adapter faces; separate cavities or an isolating barrier from the body; and independent protection for display parts with no shared cavity with hard objects.
7. Vibration Isolation and Cushioning: Graded Design
Isolation must be graded by component sensitivity rather than applied uniformly.
Distinguish shock from vibration. Shock is a short, high-amplitude event such as a drop, impact or emergency stop, needing sufficient cushion stroke and a suitable energy-absorbing material. Vibration is sustained, low-amplitude oscillation from road excitation and engine running, needing an appropriate natural frequency and damping to avoid resonance. The two require different countermeasures and must be designed separately.
Grading by sensitivity. Level one: objectives, especially high-power ones, confocal scanning heads, lasers and detectors, the most sensitive, needing the highest grade of isolation and dedicated cavities. Level two: stage, focusing mechanism, condenser and camera module, moderately sensitive, needing cushioned fixation and mechanism restraint. Level three: base, pillar, power adapter, cables and tools, relatively insensitive, needing impact and abrasion protection. Different levels must not share a cavity or cushion layer, because a cushion layer is designed around a specific weight and sensitivity and mixing defeats that design.
Avoid the padding-more-is-better trap. Cushion material must be matched to component weight: a material that is too soft compresses fully under a heavy load and loses its stroke, while too hard a material cannot absorb energy and transmits shock unchanged. Correct practice is to select material hardness and bearing area from cushion curves using component weight, the allowable acceleration limit given by the manufacturer and the expected drop height, then verify by test. An objective is the classic light but sensitive component: it may weigh only a few hundred grams yet have a very low allowable acceleration limit, so it needs softer cushioning over a larger bearing area and must never share a cushion layer with the whole instrument.
Low-frequency vibration and overall attitude. Road transport energy concentrates at low frequency, and if the system natural frequency falls inside the excitation band, resonance amplifies. A microscope has a high centre of gravity, particularly with a camera module fitted, so it readily rocks under low-frequency excitation. This needs low centre of gravity fixation, with the base and lower structure as the primary load-bearing and fixing face; lateral stops limiting horizontal rocking; top restraint limiting vertical bounce; and moderate damping to suppress the resonance peak. Related structural design is in Cushion liner case design and Shock-sealed case design.
| Component level | Representative parts | Allowable condition (typical practice) | Insert scheme | Verification |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Level one | Objectives, confocal scanning head, laser, detectors | Per manufacturer acceleration limit | Dedicated cavity, soft cushioning, large bearing area, clean packaging | Vibration test plus arrival function check |
| Level two | Stage, focusing mechanism, condenser, camera module | Conventional precision instrument level | Cushioned fixation, mechanism restraint, local reinforcement | Vibration and drop test plus mechanism feel check |
| Level three | Base, pillar, adapter, cables, tools | Impact and abrasion protection | Separated fixation, surface protection, controlled radius | Visual and appearance inspection |
8. Cleanliness, Dust Prevention and Mould Prevention
Cleanliness and mould prevention are the most region-specific requirements in microscope protection, and matter especially in the humid south of China and in Southeast and South Asia.
Sources of contamination and their consequences. The contaminants that reach a microscope in transport and storage are mainly particles such as dust, fibre and packaging debris; organic vapour from packaging outgassing and lubricant volatilisation; water vapour and condensate; fingerprints and skin oils; and mould spores. Their consequences are respectively: particles produce stray light and visible dark spots in the field of view; organic vapour forms a haze on lens surfaces; water vapour hydrolyses coatings and degrades cement layers; fingerprints cause localised contamination; and mould spores germinate in high humidity, and the organic acids the mould secretes corrode the coating and create permanent scattering, which is irreversible damage.
Three levels of mould prevention. Level one is humidity control: the key condition for mould growth is relative humidity, and keeping storage humidity low is the most effective measure. Recommended storage humidity for a microscope should be clearly below 60 percent RH, and the specific limit should come from the manufacturer, since different coating and cementing structures tolerate humidity differently. Level two is cleanliness: mould spores need a surface to attach to, so reducing particles and organic contamination inside the case lowers the germination probability, as does avoiding prolonged open exposure in humid conditions. Level three is periodic inspection: a microscope in long-term storage should be opened periodically to check for misty spots or thread-like mould on lens surfaces and to check desiccant condition. The plum rain season in southern China and the monsoon season in Southeast Asia are the periods when inspection matters most.
Hard constraints on insert materials. Insert materials that contact optical components or share a sealed volume must deliver low outgassing, releasing no siloxanes, plasticisers or condensable volatiles; low particle shedding; no hard fillers, to avoid coating scratches; and chemical inertness. This must be established by material evaluation rather than appearance, since materials that look alike can differ greatly in outgassing. A comparison method is given in the Case foam material comparison.
Unpacking and installation cleanliness. Delivery documentation should state: open in a clean area, clean the bench and tools beforehand, wear clean gloves, fit objectives immediately after removal or transfer them to a clean box, and avoid dust-generating work while the case is open. No packaging can compensate for contamination caused by leaving equipment open in a dusty area for a long time.
9. Humidity Control and Long-Term Storage
Humidity control serves three purposes for a microscope: mould prevention, coating hydrolysis prevention and corrosion prevention.
How condensation forms and how to prevent it. Condensation occurs when a surface temperature drops below the dew point of the surrounding air. Two situations are typical: container rain in a sea freight container crossing climate zones, where falling night-time outside temperatures cool the container walls and internal water vapour condenses on walls and cargo; and moving directly from cold storage into hot humid air, where the cargo surface is below the new dew point and condenses immediately. Prevention means reducing the absolute water content inside the case through sealing, desiccant and packing in a low-humidity environment; slowing the rate of temperature change using thermal inertia; and avoiding abrupt transfers by equalising temperature before opening.
Desiccant selection and quantity. Selection points: capacity matched to the target humidity, rate matched to the transport duration with fast-acting types for short journeys and high-capacity long-lasting types for sea freight, no dust or corrosive by-products, and an indicating type for visual checking. Quantity should be calculated from free internal volume, packaging material moisture vapour transmission rate, transport duration and target humidity, with an allowance, never estimated roughly. Where storage is long term, as with teaching institutions, backup instruments and rental stock, desiccant replacement should be a scheduled routine.
Four points for long-term storage. First, attitude: store upright, avoiding prolonged side-lying or inversion, since sustained static load causes local mechanism deformation. Second, environment: store in a temperature-stable, humidity-controlled position away from external walls, windows, floors and heat sources, and avoid storing a microscope under a laboratory bench or beside a reagent cabinet, where humidity swings are large and chemical vapour may be present. Third, dust covers and case: for long-term storage keep the instrument in the case or under a dedicated dust cover to reduce particle settlement and insect ingress. Fourth, periodic inspection: check lens condition, desiccant and gasket quarterly, adding one check before and after the plum rain season. Related care methods are in How to clean a protective case and service life assessment in Protective case service life evaluation.
On extreme temperature scenarios. Where a microscope must be stored or moved in cold or hot conditions, such as cold-region field work or tropical on-site inspection, additional thermal buffering is needed: materials become brittle at low temperature, so cushion and gasket material selection must be adjusted, while high temperature accelerates cement ageing and raises mould risk. Related schemes are in Extreme temperature protective cases.
10. Sealing Class: How IEC 60529 and GB/T 4208 Apply
Sealing class is a basic specification for microscope cases, but its scope must be understood precisely.
Definition and recommendation. The dust and water ingress rating follows IEC 60529 internationally and GB/T 4208 in China, expressed as IP plus two digits. For microscope cases:
- IP54: only for short transfers in a controlled environment, such as moving between rooms in the same building, and not recommended for long-distance transport or storage.
- IP65: suitable for domestic transport and normal storage, dust-tight and protected against water jets, and a common choice for teaching and routine laboratory use.
- IP66: for transfer and site environments where hosing or heavy spray may occur.
- IP67: for sea freight export, long-term storage and cases holding high-value optics, and the recommended class for export and long-term storage.
- IP68: only where there is a genuine immersion risk.
Three boundaries that must be stated. First, the IP class does not indicate internal humidity; sealed with humid internal air, the case will hold that humidity, so lowering it requires desiccant and low-humidity packing. Second, the IP class says nothing about vibration isolation; the two are independent parameters and must be designed and verified separately. Third, the IP class is not mould prevention; mould prevention depends on humidity control, cleanliness and periodic inspection, and a sealed case only supports the humidity control path. If humidity is high at the moment of sealing, sealing in fact locks the moisture inside.
Key structures for achieving the seal. Common practice for IP67 includes a continuous closed-loop perimeter gasket with no joint in a critical position; controlled sealing face rigidity and flatness with groove tolerances matched to the gasket cross-section; multi-point latch preload design; a pressure equalisation valve; and sealed cable and interface penetrations. Related structural points are in Toolbox hinge, latch and seal structure and Case seal material selection.
Why pressure equalisation is necessary. A high sealing class brings a pressure problem: sealed at low altitude and shipped at high altitude or by air, the differential loads the case structurally and makes it hard to open. Cases at IP67 and above used for microscopes should therefore be fitted with a pressure equalisation valve, which breathes slowly at a threshold differential while a hydrophobic and oleophobic membrane blocks liquid water and particles. Related structure and selection points are in Case pressure equalisation valve and IP67 protective case structure.
Gasket replaceability and service life. The gasket is a wear part and loses sealing performance through compression set, ageing and contamination. The structure should allow replacement without special tools, no re-adjustment of the overall structure afterwards, and standardised specifications for customer sourcing. Where material flammability matters, selection and verification can follow UL94 classification with testing of the actual part.
11. Custom Inserts and Cavity Schemes
The insert is the executing layer of protection and its design quality determines the outcome.
Body and base cavity design points: the base is the primary load-bearing face, using large-area surface support to create low centre of gravity fixation; lateral stops limiting horizontal movement and rocking; top restraint limiting vertical bounce, which must not bear on the nosepiece, tube or stage; upright attitude fixation restraining tipping; and clearly marked lifting points and centre of gravity.
Objective cavity design points: one cavity per objective, never shared; support at the mounting datum or the middle of the barrel so the end face takes no load; low-outgassing, low-shedding insert material; desiccant inside the cavity that does not touch the objective; objective boxes or cavity covers fixed so they cannot move freely; and position numbering showing magnification and identity for counting and assembly.
Stage and focusing area design points: no storage cavity or load-bearing structure above the stage; a dedicated cavity or guard for drive handles; a dedicated cavity or guard for focusing knobs; increased support density in the nosepiece region; and operating space and a sight window for the locking device so its state can be confirmed.
Accessory cavity design points: a dedicated cushioned cavity for the condenser; a dedicated thin-plate cavity with isolating soft pads and no stacking for filters and optical accessories; independent fixation for the power adapter; controlled cable coil radius with protective caps; independent protection for camera adapters and displays with no shared cavity with hard objects; and a separate dry document cavity. Custom machining processes are described in EVA foam insert custom process and Custom foam inserts guide.
| Cavity type | Contents | Key design parameters | Prohibitions |
|---|---|---|---|
| --- | --- | --- | --- |
| Body and base cavity | Microscope body, base | Large-area surface support, low centre of gravity fixation, lateral and top restraint | No top restraint bearing on nosepiece or stage |
| Objective cavity | Objectives of each magnification | One cavity each, datum support, low-outgassing material, desiccant, numbering | No several objectives loose in one cavity, no load on end faces |
| Nosepiece area | Objective nosepiece | Denser local support, objectives rotated to a low-moment position | No long objective left cantilevered outward |
| Stage area | Stage, drive handles | No load on the surface, handle guard, safe position lock | No storage above, no free sliding |
| Focusing area | Focusing knobs, coarse and fine mechanism | Knob guard, head travel restraint, locking access | No shipping with the mechanism unfixed |
| Accessory cavity | Condenser, filters, adapter, cables | Dedicated cavities, isolating soft pads, controlled radius | No stacking thin optical plates |
| Document cavity | Manuals, calibration and test documents | Independently sealed, moisture protected, fixed position | No mixing with consumables |
12. Transport Testing: ISTA, GB/T 4857, ASTM D4169 and the MIL-STD-810H Note
Packaging effectiveness must be verified by citable standard testing.
The ISTA series is graded by transport form and weight: Series 1 non-simulation performance tests, Series 2 partial simulation, Series 3 general simulation including temperature and humidity conditioning, and Series 6 carrier-specific and e-commerce programmes. For a single microscope case, ISTA 2A suits partial simulation; for palletised bulk dispatch, common in central purchasing by teaching institutions, ISTA 3E is closer to reality; and for export cargo with humidity requirements the conditioning of ISTA Series 3 is more complete. The process is described in ISTA transport testing procedure.
The GB/T 4857 series is the Chinese family of basic test methods for transport packages, covering vibration, shock, stacking and drop. For microscope cases the most important are vibration testing, after which objective condition, nosepiece positioning repeatability, stage travel feel and focusing backlash must all be checked; stacking testing, which evaluates structural stability under warehouse and container stacking and must specifically confirm that the stage takes no load from above; and drop testing, which evaluates the integrity of case and contents in an accidental drop, where a microscope high centre of gravity makes corner and edge drops more destructive than face drops. The method is analysed in GB/T 4857 transport packaging testing.
ASTM D4169 combines distribution cycles with assurance levels and suits sea freight and intermodal transport. It is described in ASTM D4169 distribution cycle testing.
| System | Emphasis | Typical microscope scenario | Common procedures |
|---|---|---|---|
| --- | --- | --- | --- |
| ISTA | General simulation and carrier specific | Export complete cases, palletised bulk dispatch | 3E, 3A, 2A |
| GB/T 4857 | Domestic road and rail | Domestic distributor and institutional delivery | Vibration, stacking, drop series |
| ASTM D4169 | Intermodal distribution cycle | Overseas projects, sea and land combined | DC12, DC13 and similar |
Additional verification items:
- Mechanism feel and accuracy check. This is the most direct verification for a microscope. Check stage travel smoothness and repeatable positioning, coarse focus creep, fine focus backlash and nosepiece positioning repeatability before and after vibration and drop testing, and use the difference to judge the effectiveness of the protection scheme.
- Objective-specific check. After testing, inspect the front element for scratches and contamination, check the thread for damage, and verify whether parfocality has changed using a parfocality test slide or a dedicated gauge.
- Shock recording. Place impact indicator labels and a transport data logger inside the case and collect data on real shipments to iterate the insert design.
- Cleanliness verification. Place cleanliness witness plates in the cavity and count settled particles after shipping under real conditions.
- Humidity verification. Place a temperature and humidity logger inside, record the humidity profile of the journey, and for export and long-term storage check specifically that the manufacturer limit was not exceeded.
- Reassembly verification. Simulate the on-site workflow, record time and problems from unpacking through completed assembly, and use the results to optimise cavity order and labelling.
Where a customer asks to reference MIL-STD-810H, it may be used as an environmental test method basis for designing test conditions such as high-temperature storage, low-temperature storage, damp heat cycling, vibration endurance and transport drop. It must be made clear that the standard is a test method standard and not equivalent to military certification, and no military certification claim may be made. Related notes are in MIL-STD-810H as an environmental test basis.
13. Marking, Documentation and Accessory Management
Marking and documentation are part of delivery completeness and matter particularly in bulk delivery and rental turnover.
Recommended external markings:
- Equipment information: equipment name and model, serial number, configuration list including the objective magnification set, net and gross weight, external dimensions.
- Handling pictograms: this way up, keep dry, do not stack, do not roll, fragile, centre of gravity, lifting points, following general practice in the GB/T 191 package handling pictogram and GB/T 6388 transport package marking systems.
- Impact indicator labels: fixed conspicuously on the outside so an over-limit shock can be judged visually on arrival.
- Traceability code: a QR or barcode linking equipment number, inspection records, packing list and arrival record.
- Unpacking notice position: stating the environment requirements, such as clean, dust-free and free of corrosive gas.
Recommended accompanying documentation:
- Packing list: item by item with part name, model, quantity and cavity number; objectives listed separately with magnification, identity and corresponding cavity.
- Operating and maintenance documents: manual, care handbook, and mould prevention and cleaning notes.
- Quality and test documents: factory inspection report, certificate of conformity and any agreed test report.
- Transport locking record: where the focusing mechanism, stage or detachable parts were locked as the manufacturer requires, record the locking state and position so it can be released as instructed on arrival.
- Document storage: must be protected from moisture, contamination and compression, ideally in a sealed pouch on the outside of the case or in a dry document cavity inside, isolated from the optical cavity.
Accessory and consumable management. Microscopes commonly ship with eyepieces, camera adapters, filters, spare lamps, lens paper and tools. Management points are dedicated cavities so nothing mixes with the body or objectives; isolating soft pads and no stacking for thin optical accessories; easy counting, with cavity labels showing name and quantity; and strict separation from tools, since the metal particles tools generate are a contaminant source for optics.
14. Procurement Acceptance, AQL, Selection Table and Export Reassembly
When buying microscope cases in volume, acceptance criteria must be written into the contract.
Recommended incoming inspection items:
- Appearance and dimensions: external and cavity dimensions match the drawing; no cracks, sink marks or flash; sealing face flat.
- Sealing performance: sample check to the agreed class, continuous perimeter seal fit check, gasket replaceability confirmed.
- Structural strength: sample static load test at the rated multiple held for the specified time, confirming no permanent deformation or cracking; sample corner drop or simulated drop.
- Insert fit: trial assembly with the actual item or a gauge confirming no interference, no point contact and smooth removal; confirm there is no load-bearing structure above the stage; confirm objectives are supported at the datum with no load on the end face.
- Cleanliness check: visual inspection of the optical cavity for particles, fibre and odour; obtain outgassing or cleanliness documentation for the insert material.
- Humidity control measures: desiccant type, quantity and placement; humidity indicator card; pressure equalisation valve function.
- Mechanism restraint scheme: trial assembly confirming the stage, focusing mechanism and detachable part restraints and locks, with locking state visually confirmable.
- Marking and documentation: content, position and durability of markings; completeness of documents; document cavity sealing effective.
AQL sampling method. Sample size and acceptance criteria follow batch size, inspection level and AQL value. For microscope cases the recommendation is a tighter AQL for critical defects such as seal failure, an insert that loads an objective end face or puts it in contact with hard material, a load-bearing structure above the stage, structural cracking, or a cavity dimension error preventing assembly, and a looser AQL for minor defects such as colour variation, light flow marks or font differences. The method and tables are in Custom case acceptance and AQL.
Specification selection table:
| Cargo category | Recommended case type | Insert and protection scheme | Sealing class recommendation | Suggested transport testing |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Upright biological microscope | Upright fixation case | Base surface support, lateral stops, denser nosepiece support, no load on stage | IP65 | ISTA 2A plus vibration plus mechanism check |
| Inverted microscope | Upright fixation case | Covers over open areas, stage restraint, dedicated condenser cavity | IP65/IP67 | ISTA 2A plus drop plus mechanism check |
| Stereo microscope | Compact fixation case | Elevation locking, local cushioning of the zoom group | IP65 | ISTA 2A plus drop |
| Metallurgical microscope | Heavy-duty fixation case | Clean light path protection, large stage load bearing, dedicated accessory cavities | IP65/IP67 | ISTA 3E plus vibration plus mechanism check |
| Confocal and fluorescence | High-grade isolating case | High-grade isolation, attitude fixation, dedicated module cavities, ESD protection | IP67 | ISTA 3E plus vibration plus function verification |
| Digital and all-in-one | Display protection case | Independent display protection, sensor ESD protection, window protection | IP67 | ISTA 2A plus drop |
| Objectives and spare optics | Clean box plus dedicated cavity | One cavity per objective, datum support, desiccant, low-outgassing material | IP67 | ISTA 2A plus cleanliness witness plates |
| Institutional bulk purchase | Palletised case sets | Uniform cavities, pallet load bearing, independent humidity control | IP65/IP67 | ISTA 3E plus stacking plus humidity verification |
Export and reassembly points:
- Mould and moisture are the primary risk. Sea freight containers crossing climate zones condense, and heat and humidity accelerate mould and cement ageing. An export case sealing class of IP67 or above is recommended with a pressure equalisation valve and calculated desiccant, plus a temperature and humidity logger inside for arrival verification. Where required, the test plan can follow an ASTM D4169 distribution cycle.
- Structural strength for repeated handling. Export cargo passes through factory loading, port storage, vessel loading, discharge and inland transport, so case corners, lifting points and the base need reinforcement.
- Regulations and documentation. Some microscopes, for example those with mercury lamps or lithium battery components, may attract additional cross-border requirements, so country requirements should be checked at quotation stage.
- Reassembly on arrival. The recommended sequence is: open in a clean area, check the packing list and record impact indicator status, release the transport locks as the manufacturer instructs, fit objectives and accessories, then check parfocality, stage travel and focusing feel. If the instrument has been in a cold environment, let it stand in the new environment before opening and powering up to avoid condensation.
- Post-delivery long-term management. Provide mould prevention and care notes with the goods, covering humidity control, periodic inspection and avoidance of direct sunlight and vapour-producing environments, and state the recommended inspection interval in the delivery documentation.
JUNZHJIA provides complete custom delivery capability in laboratory and industrial microscopy: developing cases and inserts around microscope model and configuration, designing dedicated clean objective cavities supported at the mounting datum, providing restraint and locking schemes for stage and focusing mechanisms, matching desiccant and pressure equalisation valves to humidity and mould prevention requirements, and supplying OEM/ODM manufacturing with stable volume delivery. Kexin New Materials (Guangdong) Co., Ltd. operates a complete chain from structural design, tooling development and rotomoulding or injection moulding through insert machining and case assembly, serving microscope manufacturers, laboratory instrument distributors, third-party testing laboratories, universities and research institutes and instrument rental services. For a first engagement we recommend a small trial batch and physical trial assembly including mechanism restraint and cleanliness verification, moving to volume supply once verified. Partner evaluation points are in How to choose a case OEM factory.
Frequently Asked Questions
Q: What is the biggest difference between a microscope case and an ordinary instrument case? A: The biggest difference is that a microscope's optical accuracy and mechanical accuracy are carried by the same set of fragile mechanisms, so both must be protected at once. Objectives carry optical accuracy: the front element is exposed, the barrel slender and the thread precise, so any impact can scratch the coating, deform the barrel or change the parfocal length, and these damages are usually unrepairable and end in whole-unit replacement. The stage and focusing mechanism carry mechanical accuracy: once guideway preload, gear pairing or fine-focus backlash change under vibration and shock, the instrument still works but its resolution and repeatable positioning have already declined. The body, comprising pillar and arm, is the common datum for both, so body deformation changes the overall geometry and protecting only one part achieves nothing. A microscope also has a high centre of gravity and limited resistance to tipping, so it must travel upright with low centre of gravity fixation plus lateral and top restraint. Finally, mould prevention for long-term storage often matters more than transport itself, so humidity design and periodic inspection cannot be omitted. Q: Why must each objective be fixed in its own cavity? A: Because an objective has three mutually independent performance lines that can all be broken, and individual fixation is the precondition for protecting all three. Line one is the optical surface of the front element, small and exposed at the barrel front, so contact with any hard object scratches it and friction against packaging material contaminates it. Line two is the mechanical integrity of barrel and thread: radial shock deforms the barrel and shifts the optical axis, while a damaged thread prevents proper threading or produces eccentricity once threaded. Line three is parfocal length accuracy, which depends on barrel length and thread face machining precision; once the end face takes axial compression or impact, parfocality drifts and the user must refocus after every objective change. If several objectives sit loose in one cavity they collide in transit, and a free objective box develops a much higher relative velocity under shock, so its end faces take far greater impact than in a fixed state. The right approach is one cavity per objective, support at the mounting datum or the middle of the barrel, no load on the end face, desiccant in the cavity and low-outgassing insert material. Q: What is most easily damaged in a stage and focusing mechanism during transport? A: What is most easily damaged is accuracy rather than appearance, in three forms. The first is focal plane drift from stage surface bending. A stage is a plate on a cantilever or slide with limited bending strength, so if other components press on it or the case takes a stacking load, the surface bends slightly and users find themselves constantly adjusting focus when viewing a large specimen, without being able to tell whether the cause is the stage or an uneven sample. The second is loss of accuracy in guideways and drive pairs. If the stage is not moved to a mechanically safe position and locked before shipping, it slides freely on the guideways and repeatedly strikes the stops, accelerating wear, while shock brinells races and produces periodic hesitation in travel, and an unfixed gear pair meshes back and forth under vibration, wearing flanks and changing preload. The third is coarse focus creep, among the most disruptive faults in use, where the head slowly descends after the knob is released; it is mostly caused by gear pair wear or insufficient preload, and the original preload state is exactly what transport most easily disrupts. Protection therefore means moving the stage to a safe position and locking it, keeping all load off the surface above, fitting guards on drive handles and focusing knobs, and fixing the focusing mechanism as the manufacturer instructs. Q: How should mould be prevented in humid southern China or on export to Southeast Asia? A: Mould prevention rests on humidity control first, cleanliness second and periodic inspection third, and all three are needed. Humidity control is the most effective measure, since the key condition for mould growth is relative humidity; keep storage humidity clearly below 60 percent RH, and take the specific limit from the manufacturer, because different coating and cementing structures tolerate humidity differently. Cleanliness is the second layer: mould spores need a surface to attach to, so reducing particles and organic contamination inside the case lowers germination probability, which means low-outgassing, low-shedding insert materials free of hard fillers, and avoiding prolonged open exposure in humid conditions. Periodic inspection is the third layer: for long-term storage, open the case periodically to check for misty spots or thread-like mould on lens surfaces and check desiccant condition, with an extra check before and after the plum rain season and the monsoon season. One common misconception is worth stressing: a sealed case is not by itself mould prevention. If internal humidity is high at the moment of sealing, a high sealing class simply locks the moisture in and holds the interior at high humidity. The correct approach combines packing in a low-humidity environment, sufficient desiccant, an indicating desiccant type and a pressure equalisation valve at high sealing classes. Q: What attitude should a microscope be transported and stored in? A: Upright at all times, with tipping restrained. There are three reasons. First, the body is the common datum for objectives and stage, so load applied through side-lying or inversion changes the overall geometry in a way that is hard to detect visually on arrival. Second, a microscope has a high centre of gravity, especially with a camera module or binocular tube fitted, so when lying on its side or inverted the centre of gravity is far from the support face, resistance to tipping falls sharply and drop and roll-over risk rises markedly. Third, some models contain lubricant or moving parts, and a prolonged non-upright attitude lets lubricant migrate to places it should not reach, affecting mechanism feel and potentially contaminating optics. In practice: use the base as the primary load-bearing face with large-area surface support to create low centre of gravity fixation; fit lateral stops to limit horizontal movement and rocking; fit top restraint to limit vertical bounce, while ensuring the top restraint never bears on the nosepiece, tube or stage; and mark this-way-up and do-not-roll pictograms clearly on the case and in the documentation. Long-term storage should also be upright, avoiding local mechanism deformation from prolonged side-lying. Q: What should be done when an objective is dirty, and how can the case help? A: The correct sequence for objective contamination is first remove surface particles with a blower or soft brush, then wipe gently in a single direction with dedicated lens paper and solvent. The essential point is never to wipe while particles are present, because that grinds the coating with the particles and creates unrepairable scratches. It is also wise to handle low-power objectives, which are cheaper and easier to replace, first, and to treat high-power objectives with caution, since they can account for a significant share of instrument cost. Once internal lens groups are mouldy or the cement layer has degraded, nothing can be done on site and the objective must be returned or replaced. The case can support this working habit in three ways: first, by providing a dedicated clean consumables cavity holding a blower, soft brush, lens paper and solvent bottle so staff do not improvise with clothing or ordinary tissue; second, by using low-outgassing, low-shedding insert materials to reduce contamination sources in transport and storage; and third, by giving objectives dedicated clean cavities with desiccant, which lowers both particle settlement and mould probability at source. Q: What sealing class does a microscope case need? A: The recommendation is IP65 for domestic transport and routine laboratory use, and IP67 for export and long-term storage, under IEC 60529 and its Chinese counterpart GB/T 4208. The reason is that a microscope faces three humidity risks at once: optical coatings hydrolyse in prolonged high humidity, cemented lens layers degrade, and metal parts corrode, while mould germinates more readily under hot humid conditions and the organic acids it secretes corrode coatings irreversibly. Three boundaries must be stated clearly. First, the IP class describes the case resistance to water and particles and does not indicate internal humidity, so lowering humidity requires desiccant and low-humidity packing. Second, the IP class says nothing about vibration isolation; the two are independent parameters that must be designed and verified separately. Third, the IP class is not mould prevention; if internal humidity is high at sealing, a high class locks the moisture in. In addition, at IP67 it is advisable to fit a pressure equalisation valve, otherwise a pressure differential across altitude changes or air freight loads the case structurally and makes it hard to open. Gaskets should be replaceable, with spare supply agreed in the contract. Q: What should be watched in bulk procurement or rental turnover scenarios? A: The core in bulk and turnover scenarios is consistency and reusability. On acceptance, check eight items: consistency of appearance and dimensions; sealing performance, sampled and confirmed by continuous perimeter fit; structural strength by sampled static load and drop; insert fit, confirming no load-bearing structure above the stage and that objectives are datum-supported with no end face load; cleanliness, with the optical cavity free of particles, fibre and odour and with outgassing documentation obtained for the insert material; humidity measures, covering desiccant type and quantity plus the humidity indicator card; the mechanism restraint scheme, trial-assembled with the locking state visually confirmable; and complete marking and documentation. Critical defects such as seal failure, objective end face loading, a load-bearing structure above the stage, structural cracking and out-of-tolerance cavities should take a tighter AQL. On usage management: institutions storing instruments long term should set up a quarterly inspection routine with extra attention around the plum rain season, while rental turnover needs gasket, insert, cavity residue and desiccant condition checked after every return, with a case service life assessment and replacement plan. Acceptance and AQL methods and service life evaluation are covered in the related articles. Q: What checks should be made after a microscope arrives? A: Five steps are recommended. Step one, review transport records: check impact indicator labels and data logger output to see whether a threshold event occurred. Step two, prepare the unpacking environment: open in a clean, dust-free area free of corrosive gas, wear clean gloves, and avoid dust-generating work while the case is open. Step three, release the transport locks: release the locking on the focusing mechanism, stage and detachable parts as the manufacturer instructs; this step is mandatory and omitting it will prevent the mechanisms moving normally and may cause damage. Step four, inspect appearance and mechanisms: check the objective front elements for scratches and contamination, the threads for damage and the nosepiece positioning, then stage travel for smoothness without hesitation, coarse focus for creep, fine focus for abnormal backlash, and the condenser, illumination, filters and accessories for function and breakage. Step five, verify performance: confirm objective parfocality, stage repeatable positioning and illumination uniformity, and carry out an actual observation. If the microscope has been in a cold environment, let it stand in the new environment before opening and powering up to avoid condensation. Fixing these checks into the delivery process both detects problems promptly and accumulates the data needed to improve the packaging scheme.
Conclusion & Related Reading
The design core of a microscope case is protecting at once the two performance lines, optical and mechanical, carried by one instrument. For objectives, three mutually independent lines must be protected: the optical surface of the front element, through dedicated cavities, low-outgassing insert material and desiccant; the mechanical integrity of barrel and thread, through surface contact support and isolation between objectives; and parfocal length accuracy, through prohibiting axial compression, supporting at the datum and keeping load off end faces. For the stage and focusing mechanism, protect accuracy rather than appearance: no load-bearing structure above the stage, move to a mechanically safe position and lock it, guards on handles and knobs, the focusing mechanism fixed as instructed to restrain head travel, denser support in the nosepiece region and long objectives rotated to a low-moment position. The thread connecting the two is integral rigid support and an upright attitude, since the body is the common datum and must be fixed at low centre of gravity with tipping restrained. Running through everything is the humidity and mould prevention thread: pack in a low-humidity environment, use sufficient desiccant, choose an indicating type, fit a pressure equalisation valve at high sealing classes, and set up a periodic inspection routine for long-term storage.
For microscope manufacturers, laboratory instrument distributors, third-party testing laboratories, universities and research institutes and instrument rental services, the sensible sequence is: first set protection levels by model and configuration, since upright and inverted, stereo and metallurgical, and confocal and digital types differ markedly; then determine insert cavities, mechanism restraint and locking, sealing class and humidity configuration for each level; then develop inserts for the main models and carry out physical trial assembly confirming no load-bearing structure above the stage and no end face loading on objectives; then verify vibration, stacking and drop to ISTA, GB/T 4857 or ASTM D4169, using the difference in mechanism feel and accuracy before and after testing as the core evidence of effectiveness; and finally write acceptance criteria, marking systems, document lists and arrival check procedures into the delivery documentation. JUNZHJIA supports the whole path from structural design, clean insert development and objective cavity and mechanism restraint design through trial samples to volume supply, with Kexin New Materials (Guangdong) Co., Ltd. manufacturing and delivering to customer model and configuration requirements, so that a microscope retains usable image quality and mechanical accuracy from factory dispatch, storage and transport through to laboratory installation.
Related Reading