

Most transit damage to machine-tool holders is not a case that cracks. It is three hidden damage types that are hard to see on arrival: taper scoring, pull-stud bending and balance upset. These defects are invisible to the eye yet cause chatter, degraded bore quality, shortened tool life and even spindle damage once installed. A tool holder, whether HSK, BT, CAT or SK, is the precision interface between machine and spindle. Taper fit accuracy is measured in micrometres, and any fine scratch or dent on the taper or face changes the contact state and amplifies radial runout. The pull-stud is the load-carrying element that clamps the holder into the spindle; a bend means eccentric clamping. A tool-setter's probe and air-bearing spindle are precision instruments that fear vibration and dust. Specifying a case for these items is therefore not about impact resistance. The core objectives are protect the taper, align the pull-stud, preserve balance and isolate the measuring instrument from vibration. Any scheme that lets tapers collide, puts side load on the stud or compresses the setter probe is simply wrong.
This article is written for procurement, process and warehouse staff at tooling manufacturers, holder distributors, precision machining companies and CNC training institutes. It provides a selection and acceptance method that can be applied directly: damage-mode analysis, lining design for holders, studs and setters, precision retention, sealing and ingress protection, transport-test standards, a packing SOP and supplier evaluation criteria. All figures quoted are typical industry values or empirical ranges; the governing inputs are always the holder specification, interface standard and the customer's acceptance specification. JUNZHJIA supplies custom-moulded inserts, OEM and ODM programmes, and supporting test documentation for machine-tool holder cases.
Table of Contents
- 1. Why Tool Holders Demand Zero Taper Damage
- 2. Five Typical Transit Damage Modes
- 3. HSK Holder Cases: Hollow Taper and Face Protection
- 4. BT/CAT Holder Cases: 7:24 Taper and Drive Key
- 5. Pull-Stud and Fastener Cases
- 6. Tool-Setter Cases: Precision Probe and Air-Bearing Spindle
- 7. Equipment-to-Case Selection Matrix
- 8. Lining Materials Compared: EVA, PE Foam, XPE and Structural Foam
- 9. Sealing and Ingress Protection: IEC 60529 and GB/T 4208
- 10. Precision Retention: Runout, Balance and Magnetic/Dust Protection
- 11. Transport Test Basis: ISTA, GB/T 4857, ASTM D4169 and MIL-STD-810H
- 12. OEM/ODM Customisation and Supplier Evaluation
- Frequently Asked Questions
- Conclusion and Further Reading
1. Why Tool Holders Demand Zero Taper Damage
A tool holder is the extension of the machine spindle. The requirement for holder interfaces has moved from "it fits" to "low runout, high rigidity, stable repeatability". Take the most common 7:24 taper, BT or CAT, and the 1:10 hollow taper, HSK. The taper and face are the dual transfer surfaces of force and accuracy: the spindle generates centring and clamping force through the taper and transmits torque through the face, which for HSK is a double-face contact. Once the taper is scratched or dented, the fit clearance changes, radial runout amplifies, the machined surface shows chatter marks and dimensional error, and in severe cases the holder can eject at high speed and cause injury.
From an engineering standpoint, the risks for these items split into four chains.
- Taper chain: taper, face, drive keyway. Once scratched or contaminated, the contact state changes on installation, runout amplifies and rigidity drops.
- Pull-stud chain: stud thread, flange step, load neck. The stud is the core load element clamping the holder to the spindle; a bend or thread defect means eccentric clamping, even stud fracture.
- Balance chain: overall holder dynamic balance. Hard impacts in transit can shift balance weights or loosen accessories, destroying the as-shipped balance and intensifying vibration at high speed.
- Instrument chain: setter probe, air-bearing spindle, grating or encoder. These parts fear vibration, dust and magnetism; transit vibration and contamination directly lower measurement accuracy and life.
A core understanding: the acceptance criterion for a holder case is first whether the taper is as-new after unpacking, the stud intact, and runout re-measurable to specification, not whether the case itself is dented. Shell strength is only the baseline. Precision retention is where the value lies.
A competent case must therefore answer four questions at once. Is the taper in zero contact and zero scratch throughout? Is the stud free of side load and bending? Is the case balance undisturbed? Is the precision instrument isolated from vibration and dust? The sections below work through these four questions.
2. Five Typical Transit Damage Modes
In after-sales and installation feedback, transit damage to holders and accessories clusters tightly into five modes. Understanding them is the first step in selection because each dictates where the lining must apply force and where the shell must be reinforced.
| Damage mode | Typical equipment | Trigger | Priority countermeasure |
|---|---|---|---|
| --- | --- | --- | --- |
| Taper scoring or denting | Holder taper, face | Metal-to-metal impact after displacement | Independent taper clearance plus soft facing |
| Pull-stud bend or thread damage | Stud, fastening screw | Side compression, crushed load point | Independent stud sleeve plus axial fixation |
| Balance upset | Weighted holder, integral holder | Hard impact, loose accessory | Full floating plus zero-displacement fixation |
| Instrument accuracy loss | Setter probe, air-bearing spindle | Cumulative vibration, dust contamination | Vibration-isolated lining plus sealed cavity |
| Loose accessory loss | Wrench, circlip, documents | No compartments, no checklist | Compartmented box plus packing-list label |
All five share a property: the damage occurs in transit but is usually discovered only at installation or tool setting. A taper scratch or a slight stud bend shows up as chatter and out-of-tolerance only on the machine, making responsibility hard to assign and rework long. Leading tooling manufacturers therefore adopt a zero-taper-contact and independent-stud-fixation strategy, blocking risk at the factory exit.
It is worth noting that the ranking of damage modes depends strongly on the transport mode. Domestic short-haul road transport is dominated by handling shock and stacking. Export sea freight is dominated by cumulative vibration, humidity and salt fog. The same batch of holders should use a different case and lining specification for domestic distribution than for export by sea, which is why hot, humid and cold-weather case design deserves its own treatment.
3. HSK Holder Cases: Hollow Taper and Face Protection
HSK, the hollow short taper, is the dominant high-speed interface. Its features are 1:10 hollow taper fit, torque transfer through double-face taper-and-face contact, and clamping by disc spring. HSK is extremely sensitive to cleanliness and mating-surface integrity: any taper or face scratch amplifies runout at high speed and can even affect clamping reliability. HSK holder case design must solve three things: zero taper contact, zero face compression, zero overall displacement.
Taper protection. The HSK taper is the core zone. The common engineering approach is a conical lining cavity: route the EVA or structural-foam lining with a conical recess matching the HSK taper so the holder taper hangs suspended in a buffer cavity touching no hard object. For the face, form a relief pocket at the face position with a soft felt facing, avoiding pressure marks. Either way, the principle is zero point contact along the taper; even a 0.01 mm scratch amplifies into visible chatter above 20,000 r/min.
Overall location. An HSK holder's centre of gravity sits toward the clamping end, so a reinforced support belongs there with axial limitation to prevent sliding. When multiple holders sit side by side, separate them with partitions and never let tapers collide. Following cushion lining and case floor interaction, the load path should be holder to rigid block to case floor to pallet, not weight pressed onto soft foam that sinks and shifts.
Independent cells. High-precision HSK holders should be placed one per cell, isolated by partitions, which both prevents mutual contact and eases numbered management. The zoning thinking is developed in removable divider systems.
For rental or service holder cases that survive many cycles, print specification, quantity and centre of gravity on the inside of the lid. JUNZHJIA typically builds these precision-interface cases with a moulded EVA insert and felt facing, issuing an insert drawing by HSK specification for approval before tooling.
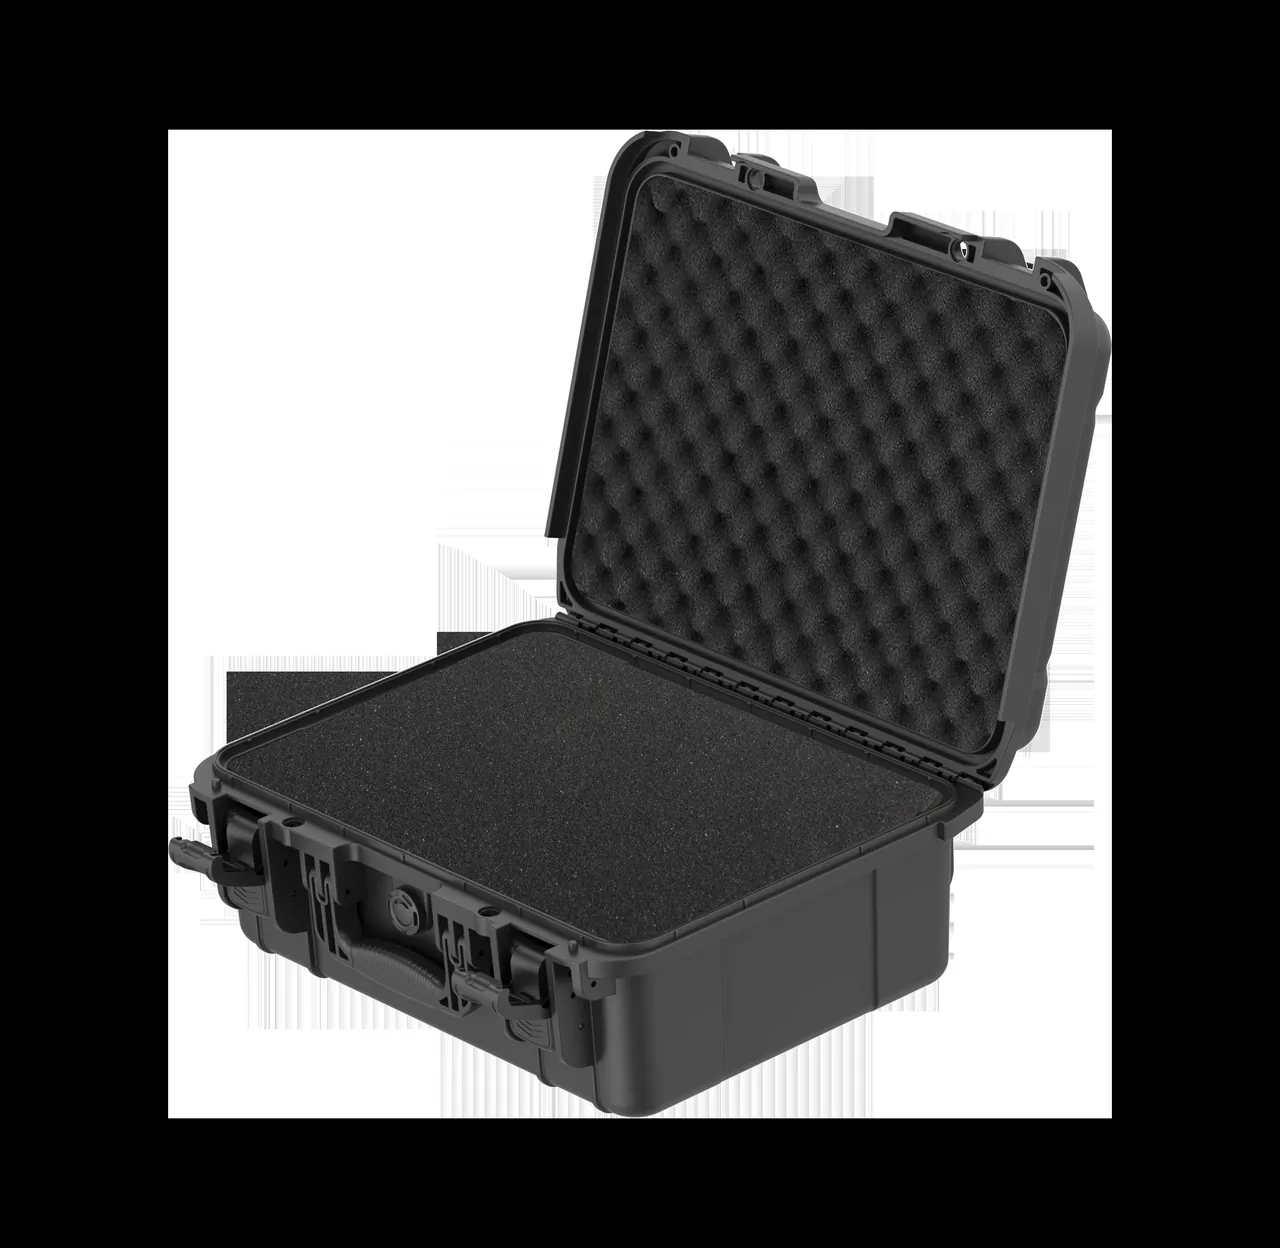
4. BT/CAT Holder Cases: 7:24 Taper and Drive Key
BT, the Japanese 7:24, and CAT, the American 7:24 or ANSI CAT40/CAT50, are the dominant interfaces for conventional machining centres. They centre on the 7:24 taper and transmit torque through a face key. Unlike HSK's hollow double-face contact, BT/CAT centre on the taper alone, so they are equally sensitive to taper scratches and add one more protection point, the drive keyway.
Taper and keyway protection. The 7:24 taper protection logic matches HSK: use a conical lining cavity matching the taper so the taper hangs free. The drive keyway is a protruding feature; the lining should form a relief slot at the keyway position to avoid side compression that deforms or chips it. A deformed keyway causes uneven torque transfer after the holder enters the spindle, producing tool release faults or abnormal noise.
Stud orientation. The BT/CAT pull-stud sits at the tail. When packing, orient the stud toward the case interior or upward, and fit an independent sleeve at the stud position to avoid tail-end bending under load. Thread damage on the stud directly causes poor engagement with the spindle gripper.
Face protection. The 7:24 face is the torque-transfer and axial-location surface and should be relieved with a soft facing, never marked. For holders with a central coolant passage, cap the passage against dust.
Magnetic and corrosion protection. Some precision holders carry magnetic inspection features or need long-term storage; keep the case away from strong magnetic fields. In high-humidity regions, add desiccant against taper rust, referencing IP67 protection solutions.
5. Pull-Stud and Fastener Cases
The pull-stud is small but is the vital point clamping the holder to the spindle. It carries the full disc-spring clamping force, its neck is the stress-concentration zone, and a slight bend causes eccentric clamping, excessive runout, even high-speed stud fracture. Stud-case design focuses on bend prevention, thread protection and specification separation.
Independent sleeve and axial fixation. Each stud should sit in a sleeve matched to its thread specification, plastic or felt, fixed to a partition. Studs should be placed axially, never side-stacked under load, and the neck load point must not be suspended under compression. Multiple stud specifications, such as BT30/BT40/BT50 with different threads, must be separated and labelled; mixing is a high-frequency cause of on-site "won't fit or won't clamp tight".
Thread protection. Cap the stud thread end with a thread protector to avoid mutual scoring in transit or metal debris adhesion. Clean threads with a clean cloth before packing to remove swarf.
Small-part management. Wrenches, circlips and seals go into a compartmented box with a packing list. The compartment thinking is detailed in removable divider systems.
6. Tool-Setter Cases: Precision Probe and Air-Bearing Spindle
A tool presetter measures tool length, radius and runout with high accuracy. Its core components include a high-resolution probe, an air-bearing or bearing spindle, a grating or encoder, and a granite or cast-iron base. Its transport difficulty is entirely different from a holder: holders fear impact, but a setter fears vibration, dust, magnetism and overturning. Setter-case design focuses on vibration isolation, dust control, overturning prevention and datum preservation.
Vibration-isolated lining. The setter body should be made to float inside the case: wrapped on all sides by low-rebound, low-resonance-frequency padding to avoid rigid contact with the shell. Compared with structural foam, low-rebound EVA or PU dissipates energy better under repeated excitation, a difference examined in more detail in protective case foam material comparison.
Probe and spindle protection. The probe is the sensing core and should be encapsulated independently with a soft sleeve, avoiding compression and contamination. The air-bearing spindle should be locked or mechanically supported during unpowered transit to prevent drift. Cover the grating or encoder face with a dust shield.
Dust and magnetic control. A setter is extremely dust-sensitive; the case should reach a high sealing grade, IP65 or better, with critical cavities independently sealed. Strong site magnetic fields disturb measurement, so keep transit and storage away from strong magnetic sources.
Overturning prevention and marking. A setter has a high centre of gravity and a heavy base; the case should constrain the centre of gravity and mark this-way-up, forbidding inverted transport. Case castors and trolley handles are covered in case castors and trolley handle options.
7. Equipment-to-Case Selection Matrix
The matrix below gives selection guidance for common holders and accessories so procurement and process staff can locate an answer quickly. The values are typical recommendations; the equipment specification, interface standard and actual route always govern.
| Equipment category | Typical spec | Insert scheme | Case format | Sealing guidance | Critical constraints |
|---|---|---|---|---|---|
| --- | --- | --- | --- | --- | --- |
| HSK holder | HSK32/40/63/100 | Conical lining cavity with felt facing | Carry or small case | IP65 | Zero taper contact, face relief |
| BT/CAT holder | BT30/40/50 | Conical cavity with keyway relief | Carry or small case | IP65 | Taper, keyway, stud orientation |
| Heavy or tooled holder | Various | Reinforced support, full floating | Medium case | IP65 | Balance, zero displacement |
| Pull-stud or fastener | Multi-spec | Compartmented sleeve, axial fix | Internal divider box | IP65 | Bend prevention, no mix |
| Tool-setter | Bench or portable | Full floating, sealed cavity | Upright case with castors | IP65 plus desiccant | Vibration isolation, dust, no overturn |
| Accessories (wrench, circlip) | Small parts | Compartmented box | Internal | IP65 | List label, loss prevention |
One empirical rule governs selection: any equipment with a precision mating surface or measurement datum must be assumed to require the same as-shipped accuracy and runout after unpacking, so the lining must provide zero taper contact, no side load on the stud, and vibration-isolated dust-free protection for instruments. This single rule eliminates most installation chatter and setting-error incidents.
8. Lining Materials Compared: EVA, PE Foam, XPE and Structural Foam
The lining is the soul of a holder case. The same shell with a different lining can differ by an order of magnitude in protection. Four material families are commonly used.
| Material | Typical density | Rebound behaviour | Processing | Best-fit equipment | Cautions |
|---|---|---|---|---|---|
| --- | --- | --- | --- | --- | --- |
| EVA | 40-120 kg/m3 | Low rebound, good damping | CNC cutting, lamination | Holders, setters, general | Softens when hot; verify temperature rating |
| PE foam | 20-50 kg/m3 | Medium-low rebound | Die cutting, cutting | Light accessories, studs | Limited load; use in composite |
| XPE/IXPE | 30-80 kg/m3 | Medium rebound, good weatherability | Lamination, cutting | Holder facing, spacers | Limited load capacity |
| Structural foam (cross-linked PVC/PE) | 60-300 kg/m3 | High rigidity, low deformation | CNC milling | Heavy holders, setter base | Requires CNC machining; higher cost |
The selection logic reduces to three steps. Define the load first, meaning pressure per unit area on the pad. Then define the vibration environment, meaning road, sea or air excitation. Finally define handling frequency, since one-way shipment can favour rigidity while repeated cycles favour toughness. For holders and setters there is an extra dimension, cleanliness and non-magnetism: the lining should be low-dust, non-shedding, and free of strongly magnetic fillers that could disturb the measurement datum.
The full route from 3D data to finished insert is covered in EVA insert customisation process and custom foam insert design guide. JUNZHJIA normally issues an insert proposal drawing for approval against the holder specification before tooling. Flammability requirements for lining materials can be clarified at enquiry stage following UL94 flame-rating thinking.
9. Sealing and Ingress Protection: IEC 60529 and GB/T 4208
Holder and accessory transport environments vary widely. Domestic distribution is mostly dry overland freight, while export sea freight faces high humidity, salt fog and temperature swing; a setter demands dust control. The goal of sealing design is a match to the environment, not maximum tightness.
What the IP code means. IEC 60529 uses two digits: the first for solids (0-6) and the second for water (0-9K). The equivalent Chinese standard is GB/T 4208. Typical configurations are as follows.
- IP54: limited dust protection, splash resistant. Suitable for short domestic routes with covered transport.
- IP65: dust tight, water-jet resistant. Suitable for the large majority of holders and accessories on domestic and near-sea routes.
- IP67: dust tight, short-term immersion, typically 1 m for 30 minutes. Suitable for sea freight, open-air storage and high-humidity regions.
- IP68: continuous immersion. Needed only for vessel decks or long-term outdoor storage.
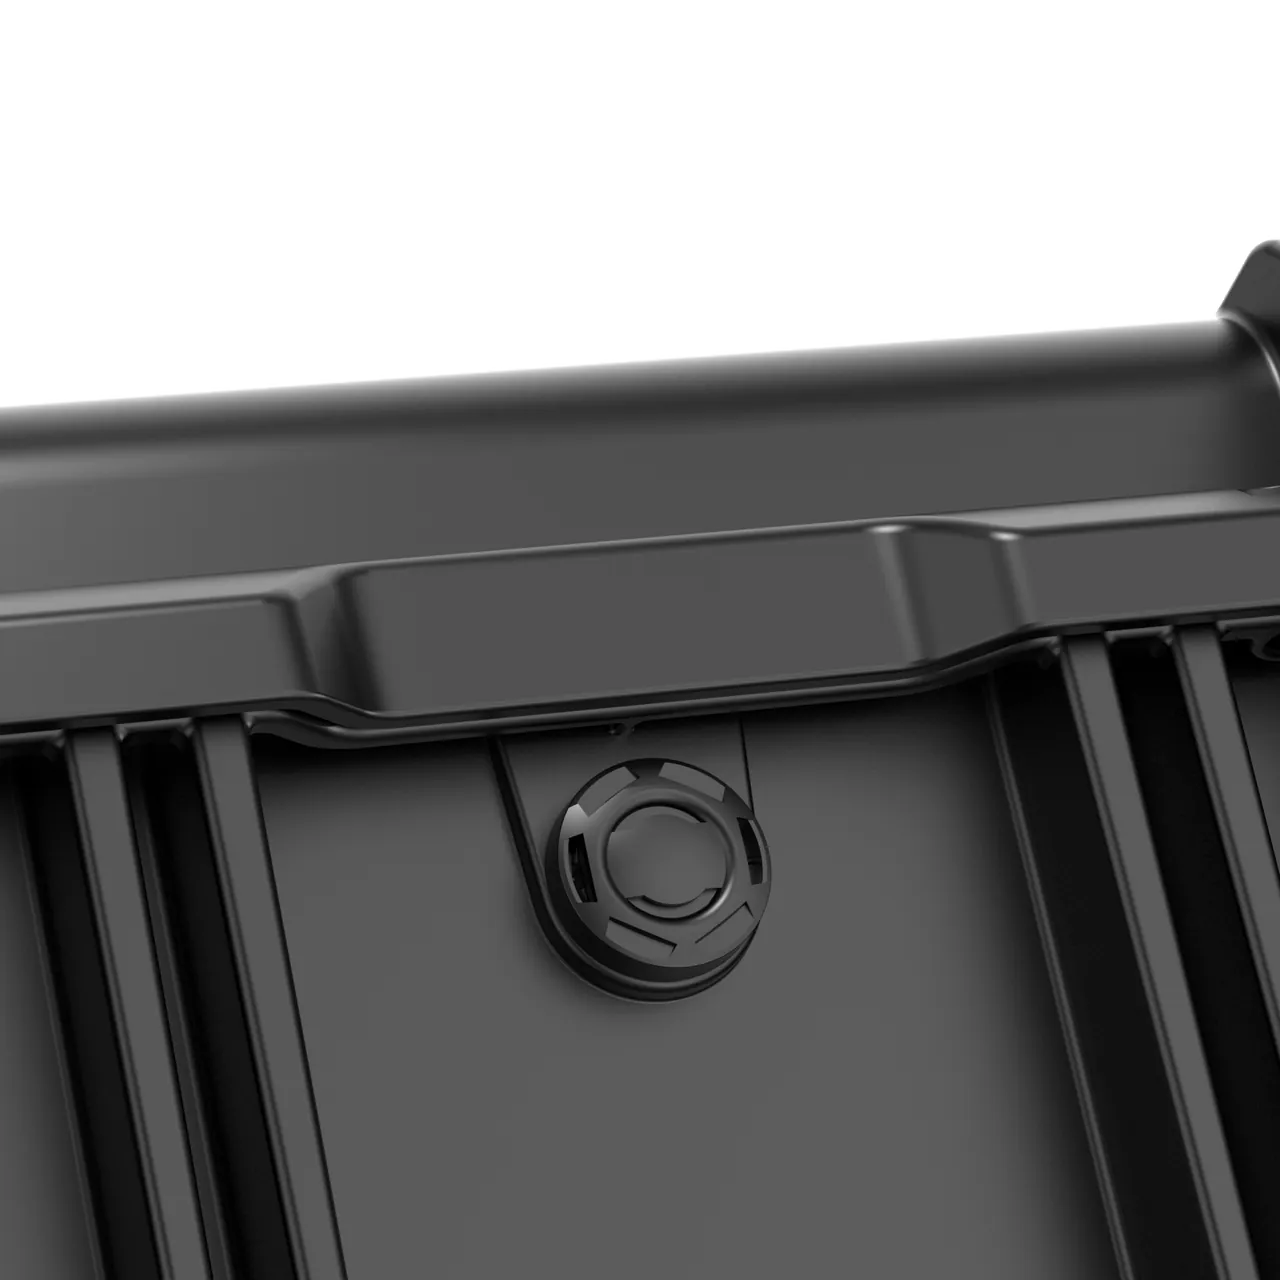
Important note: an IP rating verifies that external water does not enter. It says nothing about internal condensation. A sealed case can still condense internally across a day-night temperature cycle, so setters and high-value holders should also carry desiccant and a humidity indicator, with a pressure equalisation valve where the differential is large.
Seal selection. Case sealing relies on gasket profiles, commonly silicone, EPDM or foamed TPE. Silicone offers the best temperature and weathering resistance but costs more. EPDM balances ageing and weatherability for outdoor duty. Foamed TPE has low compression set and suits cases that open frequently. The cross-section must match the case groove, as set out in hinge, latch and seal selection. Seals are wear items and belong on the spare-parts list; replacement interval follows open-close count and storage environment, which is one of the drivers of overall protective case service life.
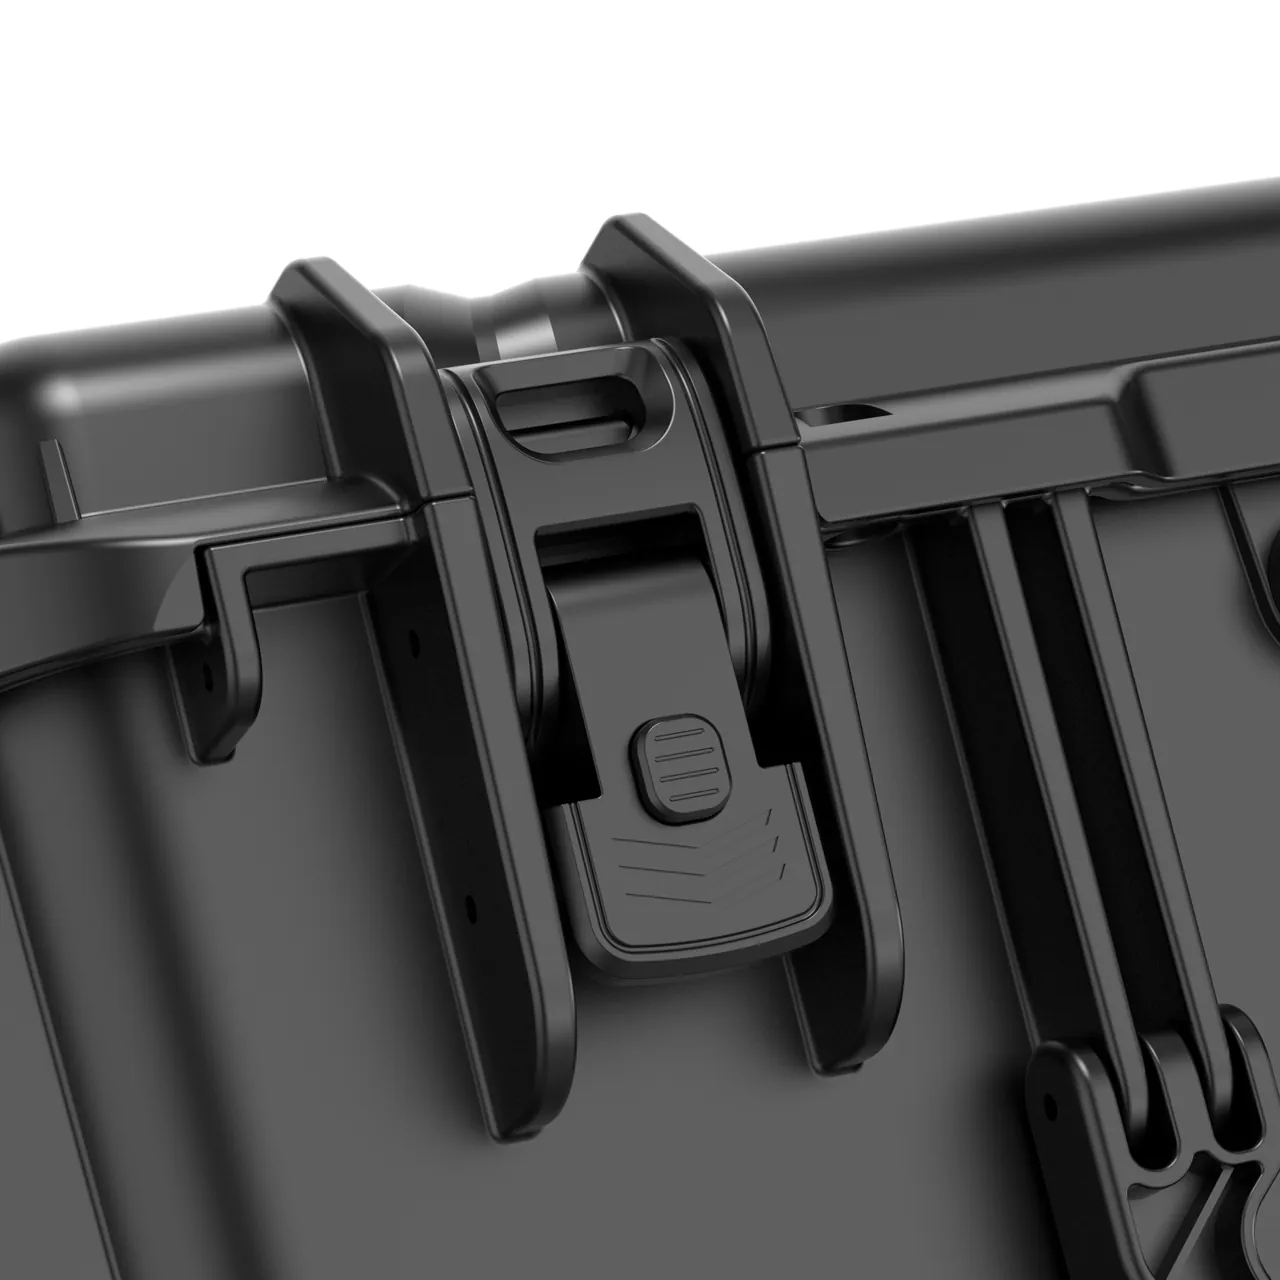
Latches and hinges. Holder cases often open frequently for access, so latches should be convenient and reliable. Setter cases have heavy lids, so latch count must match lid stiffness; when lid length exceeds 800 mm, three or more latches are advisable to prevent mid-lid lift and seal failure.
10. Precision Retention: Runout, Balance and Magnetic/Dust Protection
The ultimate goal of a holder case is that unpacking accuracy equals as-shipped accuracy. Beyond zero taper contact, three precision-retention elements deserve attention.
Radial runout. Holders are runout-tested before shipment, commonly with face runout at or below 0.003 mm and radial runout at or below 0.005 mm grades. Taper scratches or stud bends in transit directly amplify runout. Therefore sample runout re-measurement after packing is advised as one acceptance basis. Out-of-tolerance runout usually stems from lining interference or displacement and should be investigated at the first-article stage.
Dynamic balance. High-speed holders, especially high-speed HSK types, ship balanced to G2.5 or better. Hard transit impacts can loosen accessories or shift weights, destroying balance. The lining should fix the holder with zero displacement, forbidding in-case sliding. Related cushioning ideas appear in seal and shock case studies.
Magnetic and corrosion protection. Setters and some magnetically sensitive holders should stay away from strong magnetism. In humid regions holder tapers develop "rust freckles"; place desiccant inside and consider a pressure equalisation valve to reduce condensation.
11. Transport Test Basis: ISTA, GB/T 4857, ASTM D4169 and MIL-STD-810H
"Our cases are strong" is not an acceptable statement. An acceptable statement is that the case passed a specific test sequence under a named standard. Four families of standards are commonly used.
The ISTA series. The International Safe Transit Association grades procedures by package format and weight. Holders shipped as carry or small cases typically reference ISTA 2A or 2B; palletised batches reference ISTA 3E. The value of ISTA lies in sequencing: conditioning, then shock or drop, then vibration, then inspection, as explained in ISTA transport testing procedures.
The GB/T 4857 series. These Chinese standards cover vibration, shock, stacking and drop for transport packages. Domestic acceptance documents reference them heavily; practical application is set out in GB/T 4857 transport packaging.
ASTM D4169. This ASTM standard assigns test intensity by distribution cycle and is widely used for North American market validation, covered in ASTM D4169 distribution cycle testing.
MIL-STD-810H. Its environmental test methods, covering vibration, shock, temperature, humidity and salt fog, are frequently cited. This must be stated clearly: MIL-STD-810H is used here as a source of environmental test methodology and does not imply that any product has obtained military certification. See MIL-STD-810H environmental test compliance.
| Test type | Common standard | Example parameters | Relevance to holders and accessories |
|---|---|---|---|
| --- | --- | --- | --- |
| Random vibration | ISTA 2A/3E, ASTM D4169 | Power spectral density, duration | Verifies damping and displacement control |
| Shock and drop | GB/T 4857, ISTA | Drop height, peak acceleration | Verifies taper and stud protection |
| Stacking | GB/T 4857.3 | Load, duration, temperature and humidity | Verifies long-term compressive strength |
| Temperature and humidity cycling | MIL-STD-810H Method 507 | Temperature range, cycle count | Verifies sealing and condensation risk |
| Salt fog | ISO 9227, ASTM B117 | Concentration, duration | Verifies metal parts and coating protection |
Where UL94 applies. UL94 is a flammability classification for plastics, used to rate case plastic parts, insert materials and gaskets. Some customers specify flame-retardant packaging, so clarify at enquiry. On test documentation: write test items, standard numbers, sample quantities, acceptance criteria and report issuer into the contract annex so responsibility boundaries stay clear if a dispute arises.
12. Standard Packing Workflow (SOP)
The same materials produce different outcomes depending on who packs them. Writing the packing process as an SOP and confirming a first article is the most economical investment for reducing transit loss. The workflow below applies to holders, studs and setters.
- Verify and clean. Confirm specification, quantity and accessory list. Remove swarf and chips from holder tapers and stud threads with a clean cloth and compressed air. Swarf inside a lining becomes an abrasive that scores the taper.
- Taper and thread protection. Apply a temporary protection film or soft sleeve to holder taper and face. Cap the stud thread end; never suspend the neck under compression.
- Pre-fit the lining. Place conical cavities, partitions and sleeves per position markings; confirm nothing is loose or misplaced. Trial-fit and record the first article; re-measure runout and file it.
- Position the equipment. Drop the holder taper into the conical cavity with the face suspended. Place studs axially into fixed sleeves. Lower the setter into the floating lining and lock the spindle. No dragging, no forcing.
- Restrain and locate. Install the top locating block. Straps are auxiliary only, tightened just short of marking the surface. Confirm no perceptible movement when pushed by hand; an empirical criterion is displacement under 1 to 2 mm.
- Accessories and documents. Put wrenches, circlips and seals into the compartmented box. Put specification table, certificate and runout report into a pouch fixed inside the lid.
- Seal and record. Add desiccant and a humidity indicator card. Check the gasket for damage or debris. Close latches with uniform perimeter load. Apply this-way-up and moisture-protection labels. Photograph the packed case and archive.
Field experience: packing photographs and the first-article runout re-measurement report are the most effective evidence for arrival out-of-tolerance disputes. Take four fixed-angle images: empty lined case, equipment in position, restraint completed, closed case exterior, and attach the runout re-measurement values.
People and tools. Setter handling requires lifting equipment; never tilt or roll it. During trial fitting, keep a rubber mallet, marker and feeler gauges to confirm fit.
13. OEM/ODM Customisation and Supplier Evaluation
Holder and accessory cases are a many-specification, small-batch, high-precision category. A tooling plant may hold dozens of interface standards and over a hundred holder lengths, each in varying quantity but subject to the same requirement. This structure means the procurement strategy should be built around standard case types, variable linings and interchangeable labels.
Standardise the case, specify the lining. Start with a few standard case sizes graded by holder count and length to cover most equipment, then adapt specific specifications through custom linings. The tooling-amortisation logic is worked through in custom case mould cost analysis.
Five dimensions for supplier evaluation.
- Engineering capability: can the supplier issue a conical lining drawing from the holder specification, run a trial fit with runout re-measurement, and control cleanliness?
- Materials and process: batch consistency of EVA and structural-foam density, felt-facing adhesion, gasket cross-section and hardness.
- Test capability: can the supplier provide vibration, drop, stacking, IP water and runout records, or work with a third party?
- Delivery and capacity: peak-season flexibility and lead-time reliability.
- Quality system: batch inspection rules, appearance criteria and non-conforming material handling, using the sampling practice in custom case acceptance and AQL.
On OEM and ODM. Tooling plants and distributors often want their own brand on the packaging. Cooperation must clarify appearance marking, tooling ownership and cost sharing, minimum order quantity, exclusivity and specification confidentiality. Holder specification tables and 3D data are core assets; sign a non-disclosure agreement and define return and destruction obligations if the project ends.
Enquiry checklist. A practical enquiry should include holder interface standard and specification, count and length, transport mode and route, re-use cycles, storage environment, target IP rating, runout and balance requirements, marking requirements and annual volume. The more complete the input, the closer the proposal is to production-ready, as discussed in how to choose a protective case OEM factory.
JUNZHJIA normally works in this sequence for holder cases: accept the specification table or take a physical impression, issue a conical lining proposal and case configuration, confirm the first article by trial fitting and runout re-measurement, then move to volume production with batch inspection and supporting test documentation. For long-term customers, a specification archive is maintained so repeat orders for the same specification reuse the approved design. Latch customisation is covered in case lock customisation options.
Frequently Asked Questions
Q: A holder taper is so precise. How should it be secured in transit without scoring?
A: The primary principle for taper securing is zero contact and zero scratch throughout: the taper must not touch the case wall, another holder, or any hard lining object at any single point. The most robust engineering approach is a conical lining cavity: route the EVA or structural-foam lining with a conical recess matching the holder taper, whether the 1:10 of HSK or the 7:24 of BT/CAT, so the entire taper hangs suspended in a buffer cavity under no local pressure. For the face, form a relief pocket with a soft felt facing to avoid pressure marks. Never lay multiple holders flat under mutual load or let two tapers knock side by side, because even a 0.01 mm scratch on the taper amplifies into visible chatter above 20,000 r/min and can even change clamping reliability. Also, the holder centre of gravity sits toward the clamping end, so apply support-below, press-above three-dimensional restraint with axial limitation against sliding; treat straps as auxiliary only, with the main restraint formed by the lining. Orient the stud toward the case interior or upward with an independent sleeve to avoid tail-end side-load bending. When JUNZHJIA customises the case, a conical lining drawing confirming support points is issued before tooling, preventing support-position errors that leave the taper suspended under load.
Q: Are HSK and BT/CAT holders protected the same way, and can they share a case type?
A: The interface principles differ, so the emphasis varies, and whether they can share depends on whether the lining is formed separately per interface. HSK is a 1:10 hollow taper with double-face taper-and-face contact, extremely sensitive to taper and face integrity, so the lining needs a 1:10 conical cavity with face relief. BT/CAT is a 7:24 single-taper centring with one more protection point, the drive keyway, so beyond the conical cavity the lining must form a relief slot at the keyway position to avoid side compression that deforms the keyway and causes abnormal noise on tool change. If the same batch shares an interface, say all BT40, they can theoretically share one standard case type with only the length-specific lining changed. If HSK and BT are mixed, different conical-cavity linings in separate cells are mandatory; forcing a share lets one taper hang under load or the keyway get pushed. A more practical approach is standardised cases with customised linings: a few standard sizes cover most specifications and the lining changes per interface, amortising tooling while preserving protection. Never, for convenience, mix different-interface holders in one cavity.
Q: A pull-stud is so small. What happens if it bends in transit, and how is it prevented?
A: The stud is small but is the load-carrying element clamping the holder to the spindle, and its neck is the stress-concentration zone, so a bend has serious consequences. During clamping it engages the spindle gripper poorly, causing eccentric clamping and excessive runout that appears as machining chatter and degraded bore quality. More dangerously, a bent stud under high-speed rotation bears alternating stress and may fracture and eject. Transit protection needs three points. First, each stud sits in a sleeve matched to its thread specification, plastic or felt, fixed to a partition. Second, studs are placed axially, never side-stacked under load, and the neck load point must not be suspended under compression. Third, multiple stud specifications must be separated and labelled; mixing is a high-frequency cause of on-site fit or clamp failures. Cap the thread end with a thread protector and clean threads with a clean cloth before packing to remove swarf. Small-part management can follow the compartment method in removable divider systems, consolidating wrenches and circlips into a compartmented box with a packing list.
Q: How does tool-setter transport protection differ from holder protection?
A: Holders mainly fear impact, taper scoring and stud bending, while setters mainly fear vibration, dust, magnetism and overturning that disturb the probe, spindle, and datum. Therefore the emphasis differs: a setter should float inside the case, wrapped on all sides by low-rebound, low-resonance-frequency padding to avoid rigid shell contact, dissipating energy better than hard structural foam. The probe is encapsulated independently with a soft sleeve against compression and contamination, and the air-bearing spindle should be locked or mechanically supported when unpowered to prevent drift. Cover the grating or encoder face with a dust shield. The case sealing grade should be high, IP65 or better, with critical cavities independently sealed, and transit and storage kept away from strong magnetic sources. Also, a setter has a high centre of gravity and heavy base, so the case must constrain the centre of gravity and mark this-way-up to forbid inversion. Related lining comparison appears in protective case foam material comparison. In short, a holder case is about zero-contact location, while a setter case is about vibration isolation and datum preservation.
Q: How much should the protection rating differ between domestic short-haul and export sea freight for a holder case?
A: The difference comes from the exposure environment rather than the equipment itself, and chasing the highest IP number blindly brings both cost and condensation problems. For domestic road transport with covered storage, IP54 to IP65 is usually enough, with zero taper contact and stud fixation as the main priorities. For export sea freight, open-air storage or rainy, high-salt-fog regions, IP67 is advisable because the container day-night temperature swing drives marked condensation and deck carriage adds salt fog, threatening holder taper rust and setter contamination. Two points deserve emphasis. First, IP67 only guarantees that external water does not enter; it does not prevent internal condensation, so desiccant and a humidity indicator card are nearly mandatory. Second, the tighter the seal, the larger the internal-external pressure differential during temperature change, making the case harder to open and possibly sucking the gasket out of shape; a pressure equalisation valve is then more effective than a higher IP number. The correct approach is a combination of sealing, desiccant and pressure equalisation rather than a single figure. If the tender specifies an IP rating, follow the document and require the supplier to provide the corresponding test record.
Q: EVA or structural foam for the lining of holders, what is the special consideration?
A: Holders add two dimensions, cleanliness and non-magnetism, so material choice cannot look only at cushioning. The decision still follows load density, vibration level and handling frequency. Where holder weight concentrates at the clamping end with high pressure per unit area, structural foam or high-density EVA is preferable because deformation under compression is small and location is retained. Vibration-sensitive equipment such as setters should use low-rebound EVA or PU for full floating, which dissipates energy better. The key is that the material must be low-dust, non-shedding and free of strongly magnetic fillers that could disturb the measurement datum or score the taper; prefer closed-cell, surface-laminated EVA or XPE with a felt facing at critical contact surfaces. For high-frequency returnable cases, choose a tough material with low compression set. A composite lining is common: structural foam in load zones and EVA or felt in contact and cushioning zones. Run a trial fit and short-route transport check before volume production and confirm taper integrity and accuracy with a runout re-measurement.
Q: Which transport tests should a holder case pass, who performs them, and how is accuracy verified?
A: The common verification set is random vibration, shock and drop, stacking, and temperature-humidity cycling, with salt fog added for sea freight. Candidate standards include the ISTA series, GB/T 4857, ASTM D4169, or the environmental test methods referenced from MIL-STD-810H, noting that referencing its methods does not imply military certification. Three types of organisation can perform the work: third-party laboratories, the supplier's own laboratory, and joint verification. When choosing, look at three things: does the sequence cover the real route including conditioning; are the samples in production-representative condition rather than hand-built prototypes; were the acceptance criteria confirmed in writing before testing. A holder case adds one more accuracy verification: sample radial and face runout before packing and on arrival, comparing for out-of-tolerance, a harder acceptance more relevant than ordinary transit tests. Write the test items, standard numbers, sample quantities and criteria into the contract annex and assign remediation and retest responsibility for failures. For the tooling industry, the greatest value of testing is not the report itself but exposing hidden taper scoring and stud bending inside the factory.
Q: Is a case scrap after one trip, and how do I decide whether a returnable case can continue in service?
A: No, but you need explicit re-use criteria rather than a subjective judgement. Check at least five items. First, inspect the shell for cracks, deformation and through-damage, especially the floor and corners. Second, check whether the gasket has hardened, cracked, debonded or taken a permanent set, using feel and cross-section recovery. Third, verify that latches and hinges close reliably and carry load without looseness, corrosion or binding. Fourth, check the lining for collapse, fracture, dusting or missing locating blocks such as conical cavities or partitions, and whether the felt facing has detached, because collapse or conical-cavity deformation directly lets the next holder tapers shift and collide. Fifth, review desiccant failure and humidity-indicator colour change. If any item fails, replace that part before reuse. In practice the gasket, desiccant and detached lining felt are the highest-frequency problems on returnable holder cases, and linings carrying heavy holders need close inspection after two or three cycles. A log of case number, cycle count and inspection records is the lowest-cost, most direct management tool available, and the replacement criteria are detailed in protective case service life assessment.
Q: We have dozens of interfaces and over a hundred holders, each in small quantity. How can we control packaging cost?
A: The core idea is standard case types, variable linings and interchangeable labels. First, group cases into three to five standard sizes by holder count and length to cover most specifications, spreading tooling and fixture cost across many specs instead of dedicating one case design to one spec. Second, customise linings per interface and length: HSK uses a 1:10 conical cavity, BT/CAT uses a 7:24 conical cavity with keyway relief, but because the case cavity is standard the linings remain interchangeable, reducing inventory and changeover cost. Third, create a packaging record for each specification containing the spec table, lining drawing number, packing photographs and runout records, so a repeat order reuses the approved design instead of re-engineering it. Fourth, for very low-volume trial specs use a standard case with a temporary lining as an interim measure and tool a formal lining once the spec stabilises. Fifth, bring cycle count into the cost model: single-use packaging is compared on unit price, while returnable packaging should be compared on unit price divided by cycle count plus maintenance cost, and plastic returnable cases often come out cheaper. Sixth, distributors can use interchangeable labels to share one case type across brands. For external cooperation, evaluate suppliers following how to choose a protective case OEM factory.
Conclusion and Further Reading
Protecting machine-tool holders and accessories in transit is fundamentally about using engineering method to preserve a precision boundary. HSK fears zero taper and face damage. BT/CAT fear taper scoring and keyway deformation. Pull-studs fear bending and eccentricity. Tool-setters fear vibration and dust. The failure mechanisms differ, so the case and lining logic must differ too. The effective answer is not to buy the thickest case available. It is to decompose the transport route properly, then map shell strength, lining structure, sealing grade and restraint method onto specific loads and specific precision risks.
For procurement and process staff, the route to implementation compresses into four steps: define the route, determine interface and precision requirements, select case and lining, then close the loop with testing, trial fitting and runout re-measurement. Do those four steps properly and most installation-chatter and setting-error problems will surface inside the factory rather than at the machine. Where an insert drawing and case configuration proposal are needed for a specific holder interface, HSK, BT or CAT, a pull-stud specification or a tool-setter model, provide the specification table, interface standard, count and length and transport mode to JUNZHJIA, which will issue drawings against the specification and arrange first-article trial fitting with runout re-measurement.
Further Reading