

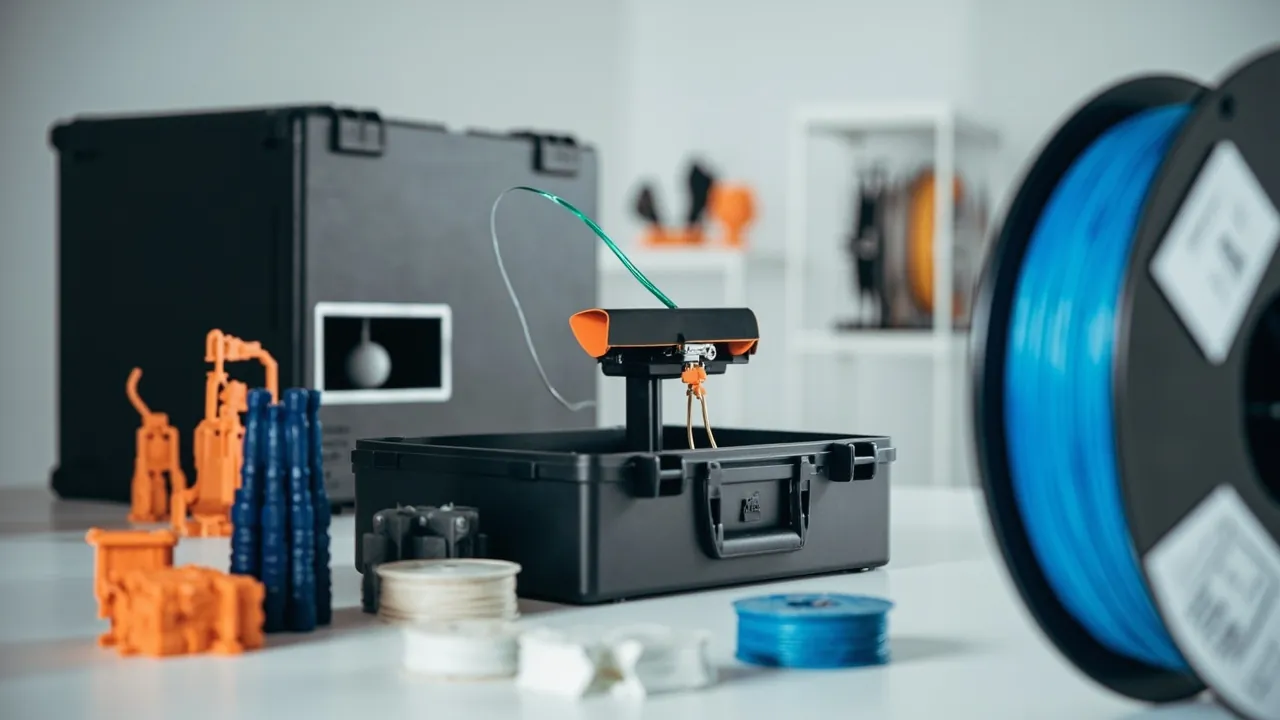
3D printing consumables do not fail loudly - they change quietly: photopolymer resin pre-polymerises under ultraviolet and elevated temperature, thickening and losing fine detail; filament absorbs atmospheric moisture and hydrolyses during melting, producing bubbles, stringing, weaker layer bonding and unstable dimensions. Most of these changes are irreversible. Filament that has already absorbed moisture cannot have its molecular weight restored by drying, and resin that has partially cured cannot be returned to its factory state. The purpose of moisture and light control is therefore not repair but holding material in its as-delivered condition.
This article is written for 3D printing service bureaus, industrial users, education and research laboratories, and consumable distributors. It breaks storage protection for photopolymer resin and thermoplastic filament into actionable engineering items: the absorption mechanism and hydrolytic degradation, moisture-sensitivity comparison and target humidity by material, desiccant selection and dosage calculation, regeneration and replacement cycles, humidity monitoring methods, UV blocking and light-blocking design, temperature management and resin viscosity, secondary containment and leak control for resin bottles, spool racks and modular zoning, seal construction and gasket materials, enclosure materials and static control, chemical compliance and operator safety, and finally a selection checklist and OEM/ODM collaboration. All figures are typical industry values and empirical ranges; the material supplier's technical data sheet (TDS) and safety data sheet (SDS) take precedence.
Contents
- 1. Why resin and filament need a moisture and light controlled storage case
- 2. The absorption mechanism: from hydrolytic degradation to bubbles and stringing
- 3. Moisture sensitivity by material and target humidity
- 4. Desiccant selection and dosage calculation
- 5. Desiccant regeneration and replacement management
- 6. Humidity monitoring: indicator cards, colour-change silica gel and data loggers
- 7. Light-blocking design: UV rejection and resin chemical stability
- 8. Temperature management and resin viscosity
- 9. Container structure: secondary containment and leak control for resin bottles
- 10. Spool storage: racks, modularity and locating
- 11. Seal construction and gasket materials
- 12. Enclosure material, stacking and static control
- 13. Chemical compliance and operator safety
- 14. Selection checklist, cost and OEM/ODM collaboration
- Frequently Asked Questions (FAQ)
- Conclusion and Related Reading
1. Why resin and filament need a moisture and light controlled storage case
In many 3D printing workshops, consumables are the cheapest and most neglected asset: the printer may be worth a substantial capital sum, yet its success often depends on a spool of nylon that has been sitting on a shelf for six months and has already absorbed moisture. That asymmetry in cost and consequence is exactly why consumable storage deserves its own design.
Two simple calculations:
- The filament calculation. Nylon (PA) and PVA are strongly hygroscopic and can absorb enough moisture to affect printing after only a few days at 60 percent RH. The symptoms are stringing, bubbling, reduced layer strength and rough surfaces, and in severe cases outright print failure. One failed industrial part costs hours of machine time and hundreds of grams of material - far more than the cost of a storage case.
- The resin calculation. Photopolymer resin is sensitive to ultraviolet and near-ultraviolet light, including the 405 nm band, and its viscosity falls and reactivity rises as temperature increases. Resin left exposed to scattered light and warm conditions thickens prematurely and may develop local gel particles. That change is irreversible and writes off the whole bottle.
The three main failure drivers:
| Failure driver | Target material | Mechanism | Reversibility |
|---|---|---|---|
| --- | --- | --- | --- |
| Moisture | Filament (PA, PVA, PC, PETG and others) | Hydrolytic degradation during melting, molecular weight loss | Partly dryable, but molecular weight is not restored |
| UV and visible light | Photopolymer resin | Initiator activation, local polymerisation | Irreversible |
| Temperature | Resin and some filament | Viscosity change, reduced initiator stability; filament softening and deformation | Partly reversible for resin, not for deformed filament |
| Oxygen | Some resins | Surface inhibition, uneven cure | Affects surface quality |
| Dust and static | Filament and powder | Contaminant attraction, nozzle blockage | Can be cleaned |
One distinction matters before anything else: a transport case solves short-term shock and humidity from A to B; a storage case solves long-term microclimate stability over months and years. The sealing logic is similar, but desiccant capacity, tolerance of repeated opening, stack load and light-blocking performance are different requirements. If you are still evaluating transport protection, start with portable transport box selection logic and IP67 case sealing implementation.
2. The absorption mechanism: from hydrolytic degradation to bubbles and stringing
To design storage properly, you must understand what moisture actually does.
Two stages of moisture uptake in thermoplastic filament:
- Physical adsorption and diffusion. Water molecules adsorb onto the surface first, then diffuse into the free volume between polymer chains. The rate depends on polarity, crystallinity, temperature and humidity: more polar groups (amide, hydroxyl) absorb faster, while higher crystallinity slows diffusion.
- Hydrolytic degradation during melting. The real damage happens while printing. When moist filament enters a melt chamber at 200 to 300 degrees C, water molecules react with ester and amide bonds, cutting the polymer chains. The result is reduced molecular weight, lower melt viscosity, and water vapour escaping as bubbles inside the melt.
Typical symptoms in the printed part:
| Symptom | Mechanism | Impact |
|---|---|---|
| --- | --- | --- |
| Stringing and oozing | Lower melt viscosity | Poor surface finish, extra post-processing |
| Bubbles and crackling sounds | Water vapour expanding in the melt chamber | Internal porosity, reduced strength |
| Weak layer bonding | Lower molecular weight, insufficient interlayer diffusion | Reduced mechanical properties, possible brittle failure |
| Unstable dimensions | Fluctuating extrusion volume | Assembly tolerances exceeded |
| Rough or matte surfaces | Water vapour disrupting surface flow | Cosmetic rejection |
Degradation pathways for photopolymer resin:
| Symptom | Mechanism | Impact |
|---|---|---|
| --- | --- | --- |
| Viscosity rise, gel particles | Premature polymerisation from scattered light and near-UV | Unusable, whole bottle scrapped |
| Uneven cure | Low temperature raising viscosity and reducing flow | Missing detail, layer thickness deviation |
| Sticky surfaces | Oxygen inhibition or uneven initiator distribution | Difficult post-processing |
| Yellowing | Resin ageing or over-exposure | Cosmetic rejection |
| Pigment settling | Long static storage | Colour inconsistency |
Three key conclusions:
- Moisture uptake is not linear. Uptake is slow at low humidity but accelerates markedly above a threshold, so keeping humidity below that threshold is more effective than shortening exposure time.
- Drying has a ceiling. Drying removes physically adsorbed water but cannot restore chains already cut by hydrolysis. Prevention beats remediation.
- Resin degradation is cumulative and irreversible. Every over-limit exposure to heat or light consumes initiator reserve and shortens usable life.
3. Moisture sensitivity by material and target humidity
Materials differ widely in hygroscopic tendency, so storage targets should differ too.
| Material | Hygroscopic tendency | Recommended storage humidity | Typical drying conditions (per TDS) | Notes |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| PLA | Low | Below 30 percent RH | 40 to 50 degrees C, 4 to 6 h | Relatively forgiving, but surfaces suffer when damp |
| PETG | Medium | Below 20 percent RH | 60 to 65 degrees C, 4 to 6 h | Hydrolysis sensitive, dry before printing |
| ABS or ASA | Low to medium | Below 25 percent RH | 60 to 70 degrees C, 4 h | More bubbles and odour when damp |
| TPU (flexible) | Medium | Below 20 percent RH | 50 to 60 degrees C, 4 to 8 h | Unstable extrusion when damp |
| PC | Medium-high | Below 15 percent RH | 80 to 90 degrees C, 4 to 6 h | Sensitive to high-temperature hydrolysis |
| PA (nylon) or PA-CF | High | Below 10 to 15 percent RH | 80 to 90 degrees C, 6 to 12 h | The strongest case for strict control |
| PVA (soluble support) | Very high | Below 10 percent RH | 45 to 55 degrees C, 4 to 8 h | Dissolves in water; seal rigorously |
| Photopolymer resin (405 nm) | Medium (light is the main risk) | Below 40 percent RH plus light blocking | Heating for drying not recommended | Light blocking and temperature come first |
| Metal powder (reference) | Low but explosion safety applies | Below 20 percent RH, inert gas preferred | Per supplier specification | A separate dangerous-goods design problem |
On the priority order for resin: the biggest enemy is light, the second is temperature, and humidity comes third. Humidity still matters, because it can affect curing behaviour and storage stability in some resin systems, and condensation at the bottle neck and cap introduces contamination. A resin storage case should therefore deliver light blocking, temperature control and moderate humidity control together.
A practical approach: write the target humidity directly into the case acceptance specification - for example, "after 24 hours sealed empty at 25 degrees C, internal relative humidity does not exceed 20 percent RH" - rather than specifying only that the case "has a drying function". That makes the deliverable measurable. Methods for verifying enclosure sealing and moisture performance are in waterproof case IP implementation.
4. Desiccant selection and dosage calculation
Desiccant is the consumable of a storage case, and its type and quantity determine whether internal humidity can be held in the target band over the long run.
| Desiccant type | Main component | Capacity (relative to own mass, empirical) | Regeneration temperature | Advantages | Drawbacks |
|---|---|---|---|---|---|
| --- | --- | --- | --- | --- | --- |
| Silica gel | Silicon dioxide | 20 to 30 percent at high humidity | 120 to 150 degrees C, 2 to 3 h | Stable, repeatedly regenerable, non-corrosive | Slow at low humidity |
| Molecular sieve | Aluminosilicate | 20 to 25 percent, strong at low humidity | 250 to 300 degrees C | Effective at low humidity | High regeneration temperature, higher cost |
| Montmorillonite clay | Clay mineral | 15 to 20 percent | 100 to 150 degrees C | Low cost | Moderate capacity, dusty |
| Calcium chloride | CaCl2 | Above 100 percent of own mass | Regeneration generally not recommended | High capacity, low cost | Turns to liquid, corrosive; do not use near electronics or metal |
| Colour-change silica gel | Silica gel with indicator | Same as silica gel | Same as silica gel | Visual life indication | Indicator can fade or fail |
Dosage estimation (engineering approximation):
The working rule is: desiccant mass approximately equals free air volume multiplied by a target factor. For a target below 40 percent RH, use 30 to 60 g of silica gel per 30 litres of free volume; for below 20 percent RH, raise this to 80 to 150 g; for below 10 percent RH, use a molecular sieve together with tighter sealing.
Three corrections must be applied:
- Moisture already in the material. If damp filament is placed in the case, the desiccant must first fight the water the material releases, so multiply the dose by 1.5 to 2.
- Opening frequency. Every opening admits a volume of humid air. Cases opened frequently should have a removable desiccant compartment for monthly replacement.
- Leakage rate of the enclosure. A case with visible gaps will equilibrate with ambient humidity within days no matter how much desiccant is added. Moisture control and sealing must be designed together; see case seal material selection.
Placement advice: distribute desiccant across the upper and lower parts of the case rather than concentrating it in one spot, so natural convection equalises humidity. Keep desiccant bags from touching resin bottles and spools directly, to avoid local over-drying or impressions.
5. Desiccant regeneration and replacement management
Moisture control is only sustainable when desiccant cycles through regenerate, use and regenerate again - which means writing the management actions into a routine.
| Management item | Recommended practice | Typical interval |
|---|---|---|
| --- | --- | --- |
| Visual check of colour-change silica gel | Colour fading signals replacement | Weekly |
| Log electronic hygrometer readings | Record internal RH; act when outside the target band | Weekly |
| Silica gel regeneration | 120 to 150 degrees C for 2 to 3 h; bag and seal immediately after cooling | 1 to 3 months |
| Full desiccant replacement | Replace the whole batch on schedule regardless of appearance | 3 to 6 months |
| Gasket inspection | Check for deformation, impressions, cracks and hardening | 3 months |
| Empty-case seal re-test | Confirm the RH rise over 24 hours with the case sealed and empty | 6 to 12 months |
| Resin bottle inspection | Check viscosity, gelling, settling and cap seal | Every use |
| Spool inspection | Check for damp signs such as whitening, sticking or brittleness | Every use |
Regeneration notes:
- Do not exceed roughly 200 degrees C; higher temperatures destroy the pore structure and reduce capacity. Ensure airflow inside the oven.
- Regenerated silica gel is very hot and must cool to room temperature before bagging, otherwise it carries heat into the case and creates a temperature differential and condensation.
- Microwaves and domestic ovens are not recommended because temperature is uncontrolled and contamination risk is high; use a temperature-controlled laboratory or industrial oven.
- Calcium chloride desiccants become liquid and corrosive; do not use them in cases containing electronics, metal rails or resin bottles.
On the division of labour between drying and storing: a dryer and a storage case are different tools. The dryer restores already-damp material to a usable state; the storage case keeps it there. Using a dryer as storage, or expecting a storage case to rescue damp material, is inefficient both ways. The correct flow is: dry, transfer immediately to a sealed storage case, take out for use, and return immediately afterwards.
Cleaning and care for the case itself is covered in protective case cleaning and maintenance; long-term performance decay is assessed in protective case service life and maintenance.
6. Humidity monitoring: indicator cards, colour-change silica gel and data loggers
"It does not feel damp" is not a criterion. A storage case must provide readable humidity indication, and ideally two independent channels.
| Monitoring method | Accuracy | Advantages | Limitations | Best fit |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Colour-change silica gel | Semi-quantitative | Visual, no power, low cost | Shows desiccant state, not case humidity | Routine daily management |
| Humidity indicator card | Semi-quantitative (marked scale) | Low cost, can be fixed inside | Requires opening to read, can fade | Small and medium cases |
| Mechanical hygrometer | Around plus or minus 5 percent RH | No power, continuously readable | Limited accuracy, needs calibration | General use |
| Electronic thermo-hygrometer | Around plus or minus 3 percent RH | Digital readout, can include alarms | Battery and calibration needed | Industrial and laboratory |
| Data logger | Plus or minus 2 to 3 percent RH | Traceable curves and records | Higher cost | Where quality records are required |
| Gravimetric (weighing desiccant) | Indirect | Estimates absorbed moisture | Requires procedure discipline | Desiccant life management |
Three practical recommendations:
- Keep sensors away from desiccant and material. Mount the sensor mid-case rather than against a desiccant bag so the reading represents the average internal humidity.
- Verify calibration. Electronic hygrometers should be checked every 6 to 12 months using a saturated salt solution or a calibration service, especially when readings feed quality records.
- Keep records traceable. For medical, aerospace or automotive printing, use a data logger and include the temperature and humidity curve in the quality record for batch traceability.
How to set the humidity target: lower is not automatically better. Over-drying has two side effects - some flexible materials become brittle or attract dust through static, and energy and desiccant consumption rise substantially. Set the target from the material TDS, for example below 10 to 15 percent RH for highly hygroscopic materials and below 20 to 30 percent RH for standard materials.
7. Light-blocking design: UV rejection and resin chemical stability
This is the most commonly mishandled part of resin storage. Many users place resin in a clear plastic box believing that avoiding direct sunlight is enough, but scattered light and the near-ultraviolet content of indoor lighting still slowly trigger polymerisation.
Three effects of light on resin:
| Effect | Mechanism | Symptom |
|---|---|---|
| --- | --- | --- |
| Premature polymerisation | Photoinitiator absorbs near-UV and activates | Viscosity rise, gel particles |
| Surface skinning | The bottle neck and liquid surface are exposed first | Film or lumps when opening |
| Pigment and additive ageing | Photo-oxidation | Colour shift, performance loss |
Light-blocking design requirements:
- The material itself must be opaque. Choose through-coloured dark material (black, dark grey, amber) rather than relying on a surface coating, which wears off in handling and cleaning.
- Any window must reject UV. If a viewing window is needed for the hygrometer and labels, use a material that blocks near-UV or apply a UV-blocking film. The safest approach is no large clear window at all - just a small port at the hygrometer.
- Minimise opening. Every opening is an exposure. Use a two-zone approach: a "stock zone" case that stays sealed long term and a small "working zone" case that is opened frequently.
- Choose the location. Keep the case away from windows, UV sterilisation lamps, curing lamps and other UV sources; physically separate the curing machine and the storage area so light from the curing chamber cannot reach stored resin.
- The bottles themselves also need protection. Original bottles are usually light-blocking, but after opening, long-term storage is better with the bottle inside the light-blocking case rather than relying on the bottle alone.
A frequently overlooked detail: some resin bottle caps are translucent or have a clear window, and resin residue remains on the neck threads, curing under light and making the cap difficult to remove. Wipe the neck threads with a lint-free cloth after each use and confirm the cap gasket is intact.
8. Temperature management and resin viscosity
Temperature affects resin more than filament because it changes both viscosity and initiator stability.
| Temperature range | Effect on resin | Effect on filament | Recommendation |
|---|---|---|---|
| --- | --- | --- | --- |
| Below 10 degrees C | Viscosity rises sharply, poorer levelling, possible separation | Some materials become brittle | Warm to room temperature before use |
| 15 to 25 degrees C | Ideal storage range | Ideal storage range | Target range |
| 25 to 30 degrees C | Viscosity falls; fine detail may suffer | Generally acceptable | Watch light exposure |
| 30 to 40 degrees C | Initiator stability falls, shelf life shortens | TPU and soft materials may deform | Avoid long-term storage |
| Above 40 degrees C | Accelerated ageing, possible gelling | Spools may soften and collapse | Never store long term |
Four temperature management points:
- Avoid day-night cycling storage. In an unconditioned workshop, night-time cooling causes condensation inside the case, while daytime heat accelerates resin ageing. Place the case in a thermally stable area or choose one with an insulated liner.
- Do not place the case against external walls or windows. Wall and sill temperatures in summer can be far above the room average.
- Temperature differential requires pressure equalization. A sealed case develops a pressure differential with temperature change, which affects opening and pumps the gasket out of its groove. See case pressure equalization valve design; for extreme storage environments also review extreme temperature case solutions.
- Let resin warm up before use. Resin taken from a cold environment should reach room temperature before the bottle is opened, so the differential does not drive condensation into the resin.
On foam temperature limits: if EVA or PE inserts are used to hold bottles and spools, confirm the material's temperature limit (EVA continuous use is commonly limited to about 60 to 70 degrees C). More material comparisons are in foam material comparison.
9. Container structure: secondary containment and leak control for resin bottles
Resin is a viscous, irritating liquid that can permanently contaminate equipment. From a chemical management standpoint, a resin bottle inside a storage case should be treated as a container requiring secondary containment.
| Risk | Consequence | Structural response |
|---|---|---|
| --- | --- | --- |
| Bottle tipped over | Resin leaks, contaminating the case and adjacent bottles | Dedicated slot plus retaining ring, anti-slip base |
| Cap loosened | Slow seepage | Light top compression to stop the bottle moving in the cavity |
| Bottle broken | Large spill | Removable spill tray at the base, capacity at least one full bottle |
| Resin contaminating the case | Difficult cleaning, lingering odour | Wipeable liner, tray removable for cleaning |
| Cross-contamination between resins | Mixed material | One dedicated slot per bottle with a label |
Structural design points:
- Dedicated slots and retaining rings. Cut slots to the bottle diameter with 1 to 2 mm clearance per side, and add a soft retaining ring at mid-height to resist tipping.
- Spill tray (secondary containment). Provide a fully removable tray at the base in a material resistant to resin and cleaning agents such as IPA; size it for the largest single bottle plus 20 percent margin.
- Wipeable liner. Avoid open-cell foam, which absorbs liquid and is hard to clean; use closed-cell EVA or a directly wipeable plastic tray.
- Ventilation and odour management. Resin has an odour, so open the case in a ventilated area. An activated carbon module can be fitted, but note that it competes for space with desiccant, so the two need separate compartments.
- Labelling and identification. Provide a label position at each slot for resin type, batch, opening date and recommended use-by date, so first-in-first-out management does not break down.
For zoning and removable structures inside the insert, see case removable divider system and EVA foam insert custom process.
10. Spool storage: racks, modularity and locating
Spools vary widely in mass and size - commonly 0.25 kg, 0.5 kg, 1 kg, 3 kg and 5 kg, with diameters from 160 mm to over 400 mm - so the spool zone must combine flexibility with the ability to locate each spool.
| Storage method | Advantages | Drawbacks | Best fit |
|---|---|---|---|
| --- | --- | --- | --- |
| Vertical slot (spool face upright) | Easy access, space efficient | Needs locating to prevent tipping and rolling | Standard 1 kg spools |
| Horizontal stacking (spool face down or up) | Stable, suits large spools | Harder access, deformation under load | 3 kg and 5 kg spools |
| Centre-axle suspension | Precise location, resists deformation | Needs axle and mount, poor compatibility | Fixed-specification volume storage |
| Removable divider zoning | Flexible across sizes | Divider stiffness needs attention | Mixed-material workshops |
| Separate sealed bag plus case | Dual protection | Tedious access, bags tear easily | Highly hygroscopic materials such as PA and PVA |
Design points:
- Locating matters more than stacking density. Spools moving inside the case press on each other, deforming rims, loosening winding and even causing tangles. Give each slot its own locating with 2 to 3 mm clearance per side.
- Do not let heavy spools rest on light ones. A 5 kg spool on top of a small spool causes deformation; zone by spool diameter.
- Secure the filament end. Insert the filament end into the spool edge hole or clip so it cannot unwind in transit or during access.
- Double protection for highly hygroscopic materials. For PA and PVA, add an individual sealed bag inside the case with a small desiccant pack, creating two levels of moisture control.
- Separate desiccant from spools. Keep the desiccant compartment independent so bags are not trapped under spools, which reduces their exposed area.
On static: spools can generate static charge through friction during handling, attracting dust. Where cleanliness matters, choose insert materials with static dissipative performance; grading and selection are covered in ESD shielding case construction.
11. Seal construction and gasket materials
Moisture control ultimately depends on the seal, and gasket ageing is the number one cause of moisture control failure.
| Gasket material | Weathering | Temperature range (typical) | Chemical resistance | Cost | Best fit |
|---|---|---|---|---|---|
| --- | --- | --- | --- | --- | --- |
| Silicone | Excellent | -50 to +200 degrees C | Good | Medium-high | Wide temperature range, long life |
| EPDM | Good | -40 to +120 degrees C | Good against oils, moderate against some solvents | Medium | General protective cases |
| Neoprene (CR) | Good | -30 to +100 degrees C | Good oil resistance | Medium | Industrial environments |
| TPU | Moderate | -30 to +80 degrees C | Good | Medium | Wear-resistant applications |
| Foamed silicone strip | Excellent | Wide | Good | Medium-high | Large flat seals |
Five seal design points:
- Match groove to gasket. The groove cross-section should be slightly larger than the gasket, with a typical compression of 20 to 30 percent. Over-compression causes permanent set; under-compression fails to seal.
- Mating face flatness. If the case and lid mating faces are not flat, no gasket will work. Large cases need ribs to resist distortion under stacking.
- Balanced clamping between hinge and latch sides. One-sided over-compression creates under-compression on the other side and a local leak path. Multiple latches help balance the load.
- Gasket joints. Corners and joints are leak-prone. Prefer a one-piece moulded gasket; if a joint is unavoidable, place it on a straight edge with a reliable bond.
- Periodic replacement. EPDM and silicone gaskets age under ultraviolet, ozone, oils and repeated compression; replacement is usually assessed at three to five years. Hinge, latch and gasket cooperation is detailed in case hinge, latch and seal structure.
Balancing opening frequency against seal life: frequently opened cases wear the gasket faster. Zone by purpose - a stock case opened rarely, a small working case opened often, and an independently opening desiccant compartment - so the main cavity is opened less often. This design lets the case balance "open it less" against "get to it easily".
12. Enclosure material, stacking and static control
| Material | Impact resistance | Low-temperature performance | Achievable flammability | Relative cost | Storage case fit |
|---|---|---|---|---|---|
| --- | --- | --- | --- | --- | --- |
| Homopolymer PP | Medium | Poor | Requires modification | Low | Single-use or light duty |
| Block copolymer PP | High | Good | UL94 HB to V-2 | Medium | Mainstream reusable cases |
| Copolymer PP with glass fibre | Very high | Good | UL94 V-0 depending on formulation | Medium-high | Large, heavy-duty cases |
| ABS | High | Medium | UL94 HB | Medium-high | Cosmetic parts |
| HDPE or LLDPE (blow moulded) | High (tough) | Good | UL94 HB | Medium | Large volume storage cases |
Stacking load. Storage cases are often stacked for long periods, so the static stacking load must be stated explicitly (for example, "bottom case supports three fully loaded cases of the same size"). Stacking applies continuous pressure to sidewalls; insufficient stiffness causes bulging and displaces the gasket - a common reason a case "stops holding humidity after six months".
Additional requirements for light-blocking material. For light blocking, colour the material through rather than painting it. Coatings wear away in handling and cleaning, exposing a light-transmitting substrate and degrading performance sharply. Also note that darker cases absorb more heat in summer, which must be weighed against temperature control requirements.
Static control. Spool friction generates charge that attracts dust, and resin dust can also become charged. Recommendations: use static dissipative insert materials (surface resistivity 10^5 to 10^11 ohm); avoid ordinary insulating plastic trays; and avoid pulling spools out quickly in dry environments.
| Static class | Surface resistivity | Purpose | Common materials |
|---|---|---|---|
| --- | --- | --- | --- |
| Conductive | 10^2 to 10^5 ohm | Shielding bags, conductive trays | Carbon-loaded PE |
| Static dissipative | 10^5 to 10^11 ohm | Inserts, handling trays | Antistatic EVA, antistatic PE |
| Insulative | Above 10^11 ohm | Structural parts | Standard EVA, ABS |
General enclosure and material selection is covered in plastic protective case construction.
13. Chemical compliance and operator safety
This section is not a disclaimer; it is a set of requirements that procurement and operations must implement.
| Item | Requirement | Notes |
|---|---|---|
| --- | --- | --- |
| Resin SDS | Must be obtained and filed | Covers composition, hazards, first aid, storage and disposal |
| Storage temperature | Per SDS and TDS | Typically avoid high heat and freezing |
| Ventilation | Open and handle in a ventilated area | Odour and volatiles need dilution |
| Personal protection | Nitrile gloves plus safety glasses | Uncured resin irritates skin |
| Waste disposal | Uncured resin and cleaning liquid per local hazardous waste rules | Never pour down drains |
| Transport compliance | Most photopolymer resins are not dangerous goods in ordinary transport, but follow the SDS and carrier requirements | Resins with flammable components may fall under transport regulations; see hazmat-compliant transport cases |
| Metal powder | Combustible dust requiring strict sealing and inert protection | A separate dangerous-goods design problem; do not apply this article's approach |
| Fire safety | Provide suitable extinguishing equipment in the storage area | Per local fire requirements |
A note on sensitisation: some users develop skin sensitisation to photopolymer resin, and once it occurs it is often cumulative, making subsequent contact more likely to trigger a reaction. Build the habit of wearing gloves during storage and handling, not after symptoms appear.
Labelling and traceability. Mark each resin bottle and each case slot with material type, batch number, opening date, recommended use-by date and a "store away from light" notice. Where traceability is required, file the humidity records alongside.
14. Selection checklist, cost and OEM/ODM collaboration
Compressing the technical items into a scoring matrix you can take into negotiations substantially reduces the risk of choosing by feel.
| Scoring dimension | Suggested weight | What to assess | Typical deductions |
|---|---|---|---|
| --- | --- | --- | --- |
| Sealing and moisture performance | 25 percent | Measured internal RH after 24 hours sealed empty, gasket material and compression | "Moisture proof" with no data |
| Light-blocking performance | 20 percent | Through-coloured material, UV rejection evidence, window area | Large clear enclosure surfaces |
| Insert and locating design | 20 percent | Bottle retaining rings, spill tray, spool zoning and locating | Generic pick-and-pluck foam |
| Desiccant compartment and maintainability | 10 percent | Independently opening compartment, capacity, ease of replacement | Desiccant stored with material |
| Temperature and pressure management | 10 percent | Whether a pressure equalization valve is needed, temperature data | No temperature specification |
| Structure and stacking | 8 percent | Wall thickness, ribs, hinges and latches | Plastic hinges, thin walls |
| Compliance and documentation | 4 percent | Material declarations, UL94 if required, RoHS/REACH | Missing documents |
| Delivery and after-sales | 3 percent | Lead time, gasket and insert spare availability | Spares not sold separately |
Cost structure:
| Cost item | Drivers | Reduction levers |
|---|---|---|
| --- | --- | --- |
| Case tooling | Size, structural complexity, cavity count | Use a standard case size plus custom insert |
| Insert processing | Process (CNC or moulded), layers, material density | Move to moulding at higher volumes |
| Desiccant and consumables | Dosage, regeneration cycle | Establish a regeneration routine |
| Gaskets | Material, size | Standardise sizes |
| Monitoring instruments | Hygrometers, loggers | Configure in tiers by application |
Lead time is usually set by three things: insert sampling and approval (often the longest), tooling fabrication, and scheduling of moisture performance validation if required. Write "internal RH after 24 hours sealed empty" into the contract as a measurable acceptance criterion.
OEM/ODM collaboration points: clarify ownership and confidentiality for insert models and case drawings; agree the scope of inspection documents (first-article dimension report, material declaration including RoHS/REACH, sealing performance records); confirm that gaskets, inserts, desiccant compartments and spill trays can be ordered separately; and confirm peak-season capacity and minimum order quantity.
JUNZHJIA, manufactured by Kexin New Materials (Guangdong) Co., Ltd., supplies wholesale, distribution and OEM/ODM customers, and can build locating inserts, desiccant compartments and spill tray structures matched to resin bottle and spool sizes, along with through-coloured light-blocking enclosures, label areas and lock schemes, together with material and sealing performance documentation. If you also need transport-stage protection, see the custom foam inserts guide and custom case mould cost analysis; batch acceptance sampling is covered in custom case AQL acceptance.
Frequently Asked Questions (FAQ)
Q: Does 3D printing filament really need a moisture-controlled case? A: It depends on the material and the usage rhythm. PLA and ABS are relatively low in moisture sensitivity and are usually fine short term in dry regions. But PETG, TPU, PC, PA (nylon) and PVA are medium to highly hygroscopic, with PA and PVA the most sensitive - a few days at 60 percent RH can absorb enough water to affect printing. The damage is not on the surface but in the melt: water molecules trigger hydrolytic degradation at high temperature, cutting polymer chains and causing stringing, bubbles, weaker layer bonding and unstable dimensions, and the molecular weight cannot be restored by drying. The right question is therefore not whether a case is needed, but whether the material absorbs moisture faster than you consume it. As a working rule, use a humidity-controlled case with desiccant for medium and highly hygroscopic materials, and also for PLA and ABS where humidity is high or storage is long, to keep surface quality stable.
Q: What humidity should the case be held at, and is lower always better? A: Lower is not automatically better; set the target per material. Typical bands are below 30 percent RH for PLA and ABS, below 20 percent RH for PETG and TPU, below 15 percent RH for PC, and below 10 to 15 percent RH for PA (nylon) and PVA. Over-drying has two side effects. First, some flexible materials become more prone to static and dust attraction at very low humidity, and certain resin systems change rheology when they lose water. Second, desiccant consumption and regeneration frequency rise substantially, increasing management cost. Set the target from the material's technical data sheet and write it into the case acceptance specification - for example, "after 24 hours sealed empty at 25 degrees C, internal relative humidity does not exceed 20 percent RH" - so it can be measured objectively.
Q: How much desiccant should I use, and how often should it be replaced? A: Estimate the dose with a working rule: 30 to 60 g of silica gel per 30 litres of free air volume for a target below 40 percent RH, raised to 80 to 150 g for below 20 percent RH, and a molecular sieve plus tighter sealing for below 10 percent RH. Three corrections must be applied. If the material inside is already damp, the desiccant must first fight the water it releases, so multiply by 1.5 to 2. Higher opening frequency admits more humid air, so increase the dose and use an independently opening desiccant compartment. If the case has gaps, any dose will equilibrate with ambient humidity within days, so fix the seal first. On replacement, act when colour-change silica gel signals, regenerate silica gel at 120 to 150 degrees C for 2 to 3 hours every one to three months, and replace the whole batch every three to six months. Always let regenerated desiccant cool to room temperature before loading it into the case.
Q: How do I know if resin has degraded, and can it still be used? A: Look for four signs. First, a marked viscosity increase or gel particles, which indicate premature initiator activation from scattered or near-UV light and are irreversible. Second, colour shift or separation and settling, meaning the pigment and additive system is no longer stable and printed appearance and properties will suffer. Third, skinning or lumps at the bottle neck or liquid surface, indicating that the surface has cured under light. Fourth, loss of fine detail or unstable layer thickness, which may come from viscosity that is too high for good levelling, or simply from low temperature - warm the resin before judging. The principle is: if the change is purely temperature-related viscosity, warming to room temperature usually restores it; if gel particles or cured lumps are present, it is chemical degradation and should not be used, because cured particles can block the release film, damage the screen and affect later batches. Store resin strictly away from light and heat.
Q: How thoroughly does resin need to be protected from light? Is a clear box with a cloth over it enough? A: A clear box with a cloth over it is not recommended. Photoinitiators are sensitive to near-UV and violet wavelengths, and indoor lighting - especially cool-white and some LED fixtures - contains near-UV components, so scattered light also slowly triggers polymerisation over time. A cloth blocks only direct light and cannot stop scattered light entering through gaps and from above, and it shifts during handling. Three sound practices apply. Choose a through-coloured dark case (black, dark grey or amber) rather than relying on a surface coating. Avoid large clear viewing windows; use only a small port at the hygrometer position and confirm the window material rejects UV. Keep the case away from windows, UV sterilisation lamps and curing machines, with physical separation between curing equipment and storage so chamber light cannot reach stored resin.
Q: Do resin bottles need secondary containment inside the case? A: Yes. From a chemical management standpoint, a resin bottle inside a storage case should be treated as a container requiring secondary containment. Resin is a viscous, irritating liquid that permanently contaminates equipment: one tip-over can seep into the insert, making cleaning difficult and leaving a lingering odour; a slightly loose cap seeps slowly; a broken bottle is a large spill. Structurally, cut a dedicated slot to the bottle diameter with 1 to 2 mm clearance per side, add a soft retaining ring at mid-height to resist tipping, provide a fully removable spill tray sized for the largest single bottle plus 20 percent margin, and specify a closed-cell EVA or directly wipeable plastic tray rather than open-cell foam. Give each slot a label position for type, batch and opening date so first-in-first-out management does not break down.
Q: Can drying and storage share one device? A: Not advisable. A dryer and a storage case do opposite things: the dryer raises temperature and expels moisture, while the storage case maintains a low humidity gradient and keeps outside moisture out. Storing material in a dryer subjects it to repeated thermal cycling, accelerating ageing. Expecting a storage case to rescue damp material is equally ineffective, because the desiccant capacity is far too small to pull wet material back to a usable state in a reasonable time, and the desiccant is exhausted rapidly in the attempt. The correct flow is to dry per the material TDS, transfer immediately to a sealed storage case, take out for use, and return it immediately afterwards. Minimise time exposed to workshop air, because freshly dried material has an extremely dry surface and therefore the fastest re-absorption rate.
Q: Does a storage case need a pressure equalization valve? A: It depends on the application, but it is advisable wherever significant temperature variation exists. A sealed case develops a pressure differential with temperature change: with 30 litres of free air and a 70 K swing, the theoretical differential reaches the order of 20 kPa. The consequences include difficult opening, the gasket being repeatedly pumped out of its groove and taking a permanent set, and continuous small gas exchange that draws moisture in and exhausts the desiccant quickly. A pressure equalization valve uses a hydrophobic, oleophobic microporous membrane so gas passes slowly while liquid water and dust cannot, removing the differential without sacrificing protection. If the case sits in a temperature-stable air-conditioned room, it may not be needed; if it sits in an unconditioned workshop, against an external wall, or will itself be transported, fit one - and confirm the valve body reaches the appropriate IP rating, that flow matches case volume, and that it is mounted high on a sidewall where material cannot block it.
Q: What measurable acceptance criteria should I use when buying a resin and filament storage case? A: Write four into the contract. First, empty-case sealing performance: after 24 hours sealed empty at 25 degrees C, internal relative humidity must not exceed the agreed value, for example 20 percent RH, with an internal humidity recovery curve if required. Second, gasket parameters: material, cross-section specification, compression range and expected replacement interval. Third, light-blocking performance: evidence that the enclosure material is through-coloured, plus the UV rejection basis for any viewing window. Fourth, structural load: the static stacking load, such as the bottom case supporting three fully loaded cases of the same size. Also agree the resin bottle slot dimensions and spill tray capacity, whether the desiccant compartment opens independently, and whether gaskets and inserts can be ordered as spares. Turning "moisture proof" into measurable clauses is the most effective way to avoid delivery disputes.
Conclusion and Related Reading
The core proposition in resin and filament storage protection is that material condition can be maintained but not restored. Nylon filament that has absorbed moisture cannot have its molecular weight recovered by drying, and partially cured photopolymer resin cannot be returned to its factory state. The design goal is therefore not to remedy problems when they appear, but to hold material in its as-delivered condition from receipt to depletion: moisture control through the three-part combination of sealing, desiccant and monitoring; light blocking through through-coloured material and fewer openings; and temperature control through site selection and case insulation.
For engineers and buyers, the most useful test is this: the value of a storage case is not how well it seals, but whether the material inside is exactly as it was when it went in. Write "internal RH after 24 hours sealed empty" and "static stacking load" into the specification as measurable clauses, and establish a routine that covers desiccant regeneration, gasket inspection and humidity logging. That reduces material write-offs and print failures, and it produces a complete record where quality traceability is required.
Related Reading