

Copper smelting and electrorefining spares share a deceptive trait. They look bulky and crude, yet their surface condition, flatness and conductive mating faces are held to very tight limits. An anode plate whose bow exceeds its allowable value will sit in the cell at an uneven spacing from the cathode, and current efficiency drops directly. A busbar contact face that picks up a score or an oxide film in transit will run hot in service, arc, and in the worst case burn a lug. The conclusion up front: a copper smelting parts case is not a sheet-metal bin that merely holds the part. It is a combined protection system covering acid mist, moisture, impact, distortion and traceability. Anode plates need profile-cut cradles plus lug relief pockets to stay flat, electrolytic cell components need compartmented location and separately packed insulation parts to keep their mating faces intact, and the case shell should be rated at least IP65, with IP67 preferred for coastal plants and ocean-freight exports.
The second practical problem is the environment. Copper smelter buildings carry SO2 and sulphuric acid mist year round, and the tankhouse is a textbook acidic, humid atmosphere. Anode plates fresh off the casting or shaping line still carry noticeable residual heat. Combine those conditions and the habit of dropping parts into a generic wooden crate with a bit of scrap foam almost guarantees trouble. This article works backwards from failure modes to packaging design, and gives directly usable guidance on shell selection, insert structure, corrosion countermeasures, crane and rigging safety points and incoming inspection for equipment engineering, spare-part management, procurement and warehouse teams in non-ferrous metallurgy.
Table of Contents
- 1. Why Copper Smelting Parts Need Dedicated Cases
- 2. Where Anode and Cathode Plates Fail: Flatness, Lugs and Header Bars
- 3. Electrolytic Cell Components: Electrodes, Busbars, Insulators and Seals
- 4. Acid Mist, Moisture and Salt Spray: ISO 9227 and Corrosion Strategy
- 5. Pre-Packing Treatment of Hot Parts: Cooling, Insulation and Temperature Sign-Off
- 6. Case Shell Selection: IP Rating, Material and Load Capacity
- 7. Insert Design: Compartments, Location and Contact Surface Control
- 8. Vibration and Shock: ISTA, ASTM D4169 and GB/T 4857 in Practice
- 9. Heavy Handling: Crane Gear, Centre-of-Gravity Marking and Lifting Safety
- 10. Surface Condition and Cleanliness Control: ISO 4406 Awareness
- 11. Incoming Inspection, Traceability and AQL Sampling
- 12. Custom Insert Workflow and OEM/ODM Delivery
- 13. Selection Decision Tables and Common Misconceptions
- Frequently Asked Questions
- Conclusion & Related Reading
1. Why Copper Smelting Parts Need Dedicated Cases
Spare-part procurement in copper smelting and electrorefining has two distinguishing features. The part itself is not always expensive, but the cost of stopping the line is enormous. Tankhouses run in series of tens to hundreds of cells. If a dimensional deviation on an anode plate or a poor contact on a busbar causes a local short circuit or a burnt plate, the response involves stopping cells, cleaning cells and replacing plates, with production losses counted in days. Copper smelting is also a continuous operation: flash smelting, converting, anode furnace refining and electrorefining interlock tightly, so a quality shortfall in any one stage propagates upstream and downstream.
From a protection engineering standpoint, copper smelting parts share three characteristics that rule out generic packaging.
- Sensitive conductive mating faces. The anode lug against the header bar, and the busbar against the inter-cell conductor, are both face-contact current paths. The flatness, roughness and cleanliness of those faces set the contact resistance. Oxide films, oil and scores all raise resistance, and the symptom in service is localized heating.
- Large, thin plate parts that bow easily. Anode plates are typically large in area and modest in thickness, with a high aspect ratio and limited bending stiffness. Support them only at two ends with an unsupported middle and long-haul vibration leaves permanent residual bow.
- Materials and coatings that dislike acid and moisture. Copper and copper alloys discolour and corrode noticeably in humid atmospheres containing sulphur and chlorine. Some anode plates carry nickel or lead-based coatings, and a score or an acid-mist attack on the coating changes the anodic behaviour in the cell.
The value of a dedicated case is therefore not that it holds the part. It is that it keeps mechanical, humidity and contaminant loads during transport and storage simultaneously inside the component's allowable limits. This follows the sensitivity-tiered approach set out in the instrument case selection guide, with the difference that copper smelting parts concentrate their sensitivity in conductive faces, plate flatness and surface coatings.
One misconception needs correcting: a strong shell is not the same as adequate protection. Shell strength solves the problem of the outer box being crushed or punctured by a forklift. Whether the part survives depends on whether the insert restrains it reliably and attenuates impact energy. The shell is the enclosure. The insert is the protection.
2. Where Anode and Cathode Plates Fail: Flatness, Lugs and Header Bars
The anode plate is the core consumable of copper electrorefining and one of the highest-damage items in transit. Its failure modes show a distinct amplification effect: a minor knock in transit becomes a whole-cell efficiency loss once the plate is in the tank, because uneven anode-to-cathode spacing distorts the current distribution.
| Location | Structure / material | Typical transport failure | Insert countermeasure |
|---|---|---|---|
| --- | --- | --- | --- |
| Plate face (anode body) | Large thin plate, limited bending stiffness | Residual mid-span bow, local dishing, surface scoring | Full-face support or profile cradle with multi-point support, never unsupported mid-span |
| Lugs / hanger ears | Interface with header bar, both structural and conductive | Lug deformation, elongated hole, crushed contact face | Relief pocket at the lug, never let the lug be the only load path |
| Header bar / hanger rod | Long section, straightness sensitive | Bending, torsional distortion, damaged end threads | Full-length multi-point support, protective sleeve at ends |
| Plate coating / anode slime zone | Coating or active layer, sensitive to scoring and acid | Coating spalling, scoring, acid-mist pitting | Non-shedding separator, never plate face against plate face |
| Edges and corners | Sharp corners, burrs | Chipped corners, and sharp edges that tear the insert | Corner protectors, insert relief for sharp corners |
The critical rule: anode plates must be face-supported, never unsupported, and never face-to-face. The most reliable field approach is a profile cradle. Machine a matching support trough from high-density EVA, or build a composite cradle from plywood or a similar structural core, so the plate sits over a large contact area rather than on a few points. Between adjacent plates there must be a rigid divider or a thick foam separator. Plate face against plate face is never acceptable, because any small relative movement becomes mutual abrasion.
For the lug area, two points matter. First, the insert must include a relief pocket so the lug is not loaded inside the case. Second, the lug must not carry the full weight. The lug is designed to take a static load while hanging on the header bar, not to absorb repeated dynamic impacts inside a box. The correct arrangement is for the plate cradle to carry the weight, with the lug used only for location.
Cathodes and permanent stainless steel cathode plates have similar requirements, but their surfaces are smoother and more easily scored. Once a permanent cathode face is scored, it directly affects the surface quality and stripping behaviour of the deposited copper. Pack these plates individually, fully wrapped in lint-free cloth or PE film before they go into the cradle. For the structured design method behind cushioning layers, the cushion liner design guide sets out multi-point support and energy dissipation paths.
3. Electrolytic Cell Components: Electrodes, Busbars, Insulators and Seals
Cell components and their peripherals come in many types and span a wide accuracy range. Packing must therefore be organized by precision class rather than by physical size.
- Busbars and inter-cell connectors. These are high-current conductive parts, usually with a milled or plated contact face. The priorities are zero scoring, zero oxidation and zero distortion on the contact face. Put a lint-free separator between faces and wrap each part individually. Copper and aluminium busbars must never touch directly, to avoid galvanic corrosion.
- Insulation parts (insulating pads, sleeves, insulators). Most are epoxy, PTFE, ceramic or engineering plastic, and they are brittle and poor in impact. They must have their own compartments and must never share a compartment with heavy metal parts. Ceramic insulators in particular must be protected from point loading.
- Electrodes and anode rod assemblies. These assemblies usually include threads and mating faces, and must not loosen in transit. Keep the factory assembly state and fit protective caps over threads.
- Seals and gaskets. Cell seals are mostly rubber or FKM, sensitive to oil, ozone, heat and strong light. Pack them in individual sealed bags, store the case away from light and heat, and track shelf life.
- Cell linings and anti-corrosion liner plates. These are large, thin and easy to crease. Coil them on a mandrel or lay them flat on a pallet-style support, and never coil below the material's minimum bending radius.
For elastomer compatibility and storage limits, seal material and case compatibility collects the practical boundaries between common materials, media and temperatures, and can be used directly in a selection review. A frequent hidden loss in tankhouses is that seals sit in a corner of the shop in their case for six months, and ultraviolet light plus acidic atmosphere ages the rubber early, so leaks appear shortly after installation. A light-blocking case, desiccant in the insert and a discipline of moving parts into the warehouse on arrival are far cheaper than replacing seals later.
Where parts must be picked frequently and batches are mixed, for example several busbar sizes and insulation parts in one case, the removable divider system lets the layout change with the batch while retaining the required location accuracy.
4. Acid Mist, Moisture and Salt Spray: ISO 9227 and Corrosion Strategy
The corrosive environment around a copper smelter is twofold. Inside the case you must protect the part, and outside the case you must protect the shell and its hardware.
Part-level corrosion control comes down to blocking moisture and acidic gas. Workable measures include the following.
- Surface preparation. Coat busbar and rod contact faces with a compatible rust-preventive grease or protective agent before dispatch. For coated parts, confirm the protective agent is compatible with the coating, with no dissolution or bloom.
- Careful use of vapour phase corrosion inhibitors (VCI). VCI works well on carbon and alloy steels, but compatibility with copper and copper alloys must be confirmed separately, because certain VCI chemistries risk accelerating copper discolouration. For copper parts, prefer a desiccant plus sealing route.
- Desiccants and humidity indicator cards. Size the quantity from the free volume inside the case, the transit duration and the target humidity. A common rule of thumb is 1 to 2 kg of high-efficiency desiccant per cubic metre of free volume, doubled for long ocean voyages. Place a humidity indicator card where it can be read easily on opening, as acceptance evidence. A target of 60 percent relative humidity or below at opening is typical.
- Sealing and pressure differential management. The gasket keeps the case airtight, but pressure differences across climate zones or on air freight make the case breathe. Fit a pressure equalization valve; selection guidance is in pressure equalization valve configuration. This avoids both a hard-to-open case and a crushed gasket.
Shell-level corrosion control is mainly about the corrosion performance of metal hardware and structural parts. ISO 9227, the standard for artificial atmosphere corrosion tests including salt spray, is the usual basis for neutral salt spray (NSS) evaluation. For coastal copper smelters or seaborne exports, experience suggests requiring hinges, latches and corner guards to survive 96 to 480 hours of neutral salt spray without red rust, with the exact duration set by contract. Note that salt spray results and the overall ingress protection rating are independent metrics. The IP rating is defined by IEC 60529 and its Chinese equivalent GB/T 4208 and measures the enclosure's protection against solids and water. Salt spray duration cannot substitute for it.
Procurement note: state in the technical requirement that packaging materials must contain no sulphur, no chlorine and no recycled content. This eliminates a whole class of hidden corrosion complaints at the source. It matters especially in copper smelting, where sulphur and chlorine are the main drivers of copper discolouration.
5. Pre-Packing Treatment of Hot Parts: Cooling, Insulation and Temperature Sign-Off
Anode plates, castings and some cell components may still carry meaningful residual heat when they leave the previous process step. Sealing a warm part straight into a closed case is a classic compound error. The residual heat accelerates ageing, softening and even deformation of the insert material, so location control is lost. At the same time, heat inside a closed volume interacts with moisture and forms condensation on the part surface, which directly triggers corrosion and discolouration.
The practical workflow is set out below.
| Part condition | Waiting / treatment | Check before packing | Risk if skipped |
|---|---|---|---|
| --- | --- | --- | --- |
| Straight from casting | Natural cooling to near ambient | Surface temperature no more than ambient plus 15 C | Softened insert, lost location, condensation |
| Large plate just off the line | Zone cooling, avoid stacking that skews heat loss | No local hot spots on the face | Local stress plus warping |
| Component with thermal lining | Remove or protect the insulating layer | Lining intact, no damage | Lining crushed or deformed |
| Coated part not fully cured | Follow the coating process cure schedule | Coating hard dry, not tacky | Coating sticking and peeling |
Insert materials have their own temperature ceilings. EVA foam softens under sustained heat and takes a compression set. PE foam has an even lower softening point. PU foam can collapse under long-term heat exposure. If the part cannot be fully cooled, switch to a heat-tolerant insert such as certain XPE grades, EPP, or a composite structure with a thermal barrier, and add an insulating layer that keeps heat away from the insert. For parts that genuinely require insulated transport, the extreme temperature case design discussion covers insulation layers and temperature control.
Temperature sign-off must be a recorded action. Write the following onto the packing route card: measurement locations (for example plate face centre and both lugs), the instrument (infrared or contact thermometer), the release threshold (ambient plus 15 C, for example) and the person recording it. One release line on a card, with a signature, works far better than repeating "wait until it cools" ten times in a meeting.
6. Case Shell Selection: IP Rating, Material and Load Capacity
The shell underpins every other measure. Selection must lock down ingress protection, material, hinge and latch style, sealing method and load capacity, not just internal dimensions.
Ingress protection follows IEC 60529, the international standard for degrees of protection provided by enclosures, and its Chinese equivalent GB/T 4208. The commonly used ratings for copper smelting parts cases are shown below.
| Rating | Dust | Water | Typical scenario | Recommendation |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| IP54 | Limited dust protection | Splash resistant | In-plant shuttling, dry covered warehouse | Not recommended for inter-regional freight |
| IP65 | Dust tight | Water jet resistant | Normal road and rail freight, indoor storage | Minimum threshold for copper smelting parts cases |
| IP67 | Dust tight | Temporary immersion (1 m / 30 min) | Ocean freight, open yards, wet and coastal sites | Recommended for export and coastal plants |
| IP68 | Dust tight | Continuous immersion by agreement | Special conditions | Usually over-specified |
Note: an IP rating describes the shell's protection against solids and water. It does not guarantee the contents are safe. IP67 keeps water out, but it does not stop an impact from reaching the part after a drop. Impact resistance comes from the insert and structural design, and should be verified as a combined sealing and shock structure where relevant.
Three material families dominate.
- One-piece injection-moulded PP or PE cases. Good sealing, chemical resistance and low weight. Tooling cost is higher and very large sizes are limited. Best for seals, insulation parts, small valves and instruments.
- Copolymer polypropylene panel with aluminium frame. Flexible dimensions, high strength and available in extra-long sizes. Sealing relies on a gasket compressed by latches. Best for busbars, rods and long parts.
- Rotomoulded LLDPE cases. Best impact resistance, large sizes available, and a metal internal skeleton can be added. The trade-off is weight and volumetric cost. Best for heavy plates or parts that must be lifted.
For flame behaviour, if the case enters an area with fire-risk requirements, require the material to meet a UL94 vertical burn rating such as UL94 V-0 and obtain the material certificate. This is not a claim that the case is explosion-proof or fireproof; it only reduces the material's own flammability risk.
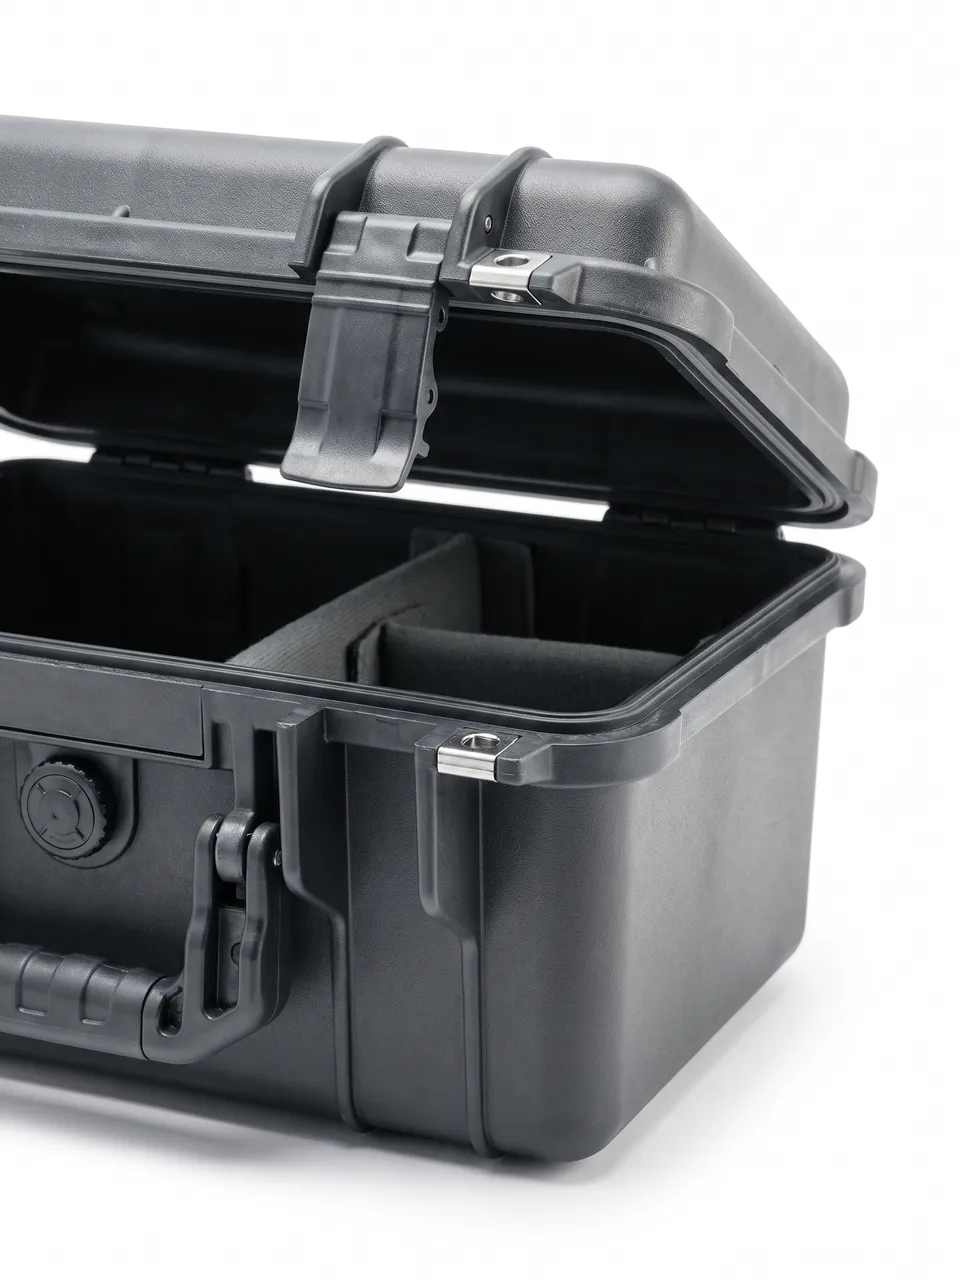
Structure and hardware are frequently overlooked. Hinges, latches and gaskets are the weak links in case service life, and the selection and fatigue testing guidance in toolbox hinge, latch and seal applies directly. For heavy cases, JUNZHJIA uses metal corner guards, reinforcing ribs and replaceable gaskets, fatigue-tests hinges and latches against open-close cycles, and can supply material and test documentation for incoming acceptance.
7. Insert Design: Compartments, Location and Contact Surface Control
The insert is the last deceleration zone in the protection system, and it is where most of the value of a custom case sits. The workflow for copper smelting parts cases is as follows.
- Build the component list. Record each part, its weight, envelope dimensions, centre of gravity and sensitive faces (conductive faces, lug holes, coatings, threads).
- Fix the shipping attitude. Plates lie flat on full-area support. Long parts lie horizontally on multi-point supports. Brittle insulation parts may stand or lie flat but must be fully constrained.
- Divide the insert into compartments. One part per compartment, heavy parts never on top of light ones, hard parts never on soft ones. Leave 1 to 2 mm assembly clearance per compartment: too tight damages parts during handling, too loose allows movement.
- Design location and restraint features. Use steps, bosses, profile pockets, clamping bars and straps to restrain the part in all three axes, so that it does not fall out if inverted and does not move when shaken.
- Control contact surfaces. Line every contact point against a precision face with lint-free cloth, PE film or felt. Separate copper from aluminium and stainless from carbon steel to avoid galvanic corrosion.
- Leave ergonomic allowance. Add handle slots or tipping chamfers to heavy parts so nobody levers them out with a screwdriver. The levering action itself is a damage source.
The insert material comparison is summarized below.
| Material | Density range | Cushioning | Formability | Durability | Typical parts |
|---|---|---|---|---|---|
| --- | --- | --- | --- | --- | --- |
| EVA foam | 60 to 120 kg/m3 | Excellent | CNC cut, bondable | Excellent | Busbars, insulation parts, instruments |
| PE foam | 25 to 45 kg/m3 | Good | Easy to cut | Fair | Large pads, void fill |
| PU foam | 30 to 80 kg/m3 | Excellent | One-shot moulded | Fair | Complex-shaped parts, full wrap |
| XPE cross-linked foam | 30 to 60 kg/m3 | Good | Thermoformable | Good | Thin plates, liner panels |
| EPP foam | 30 to 60 kg/m3 | Excellent | Moulded | Excellent | Reusable and heat-tolerant applications |
| Plywood / composite core | Not applicable | Poor | Machined | Excellent | Anode plate cradles, heavy structural support |
For the mechanical curves, compression set and behaviour under humidity-temperature cycling of these foams, the case foam material comparison provides a fuller dataset that can go straight into a selection review.
JUNZHJIA custom inserts typically combine a structural core with CNC-cut foam. Heavy parts such as anode plates are carried by a plywood or composite cradle with high-density EVA at the contact surfaces to control contact stress. Lighter precision items such as busbars and insulation parts use a single EVA block cut into compartments. This separation of load bearing from cushioning is particularly necessary in copper smelting, where heavy and precision parts are often packed together.
8. Vibration and Shock: ISTA, ASTM D4169 and GB/T 4857 in Practice
Transport vibration energy comes mainly from road excitation and handling drops, and the two impose different requirements. The first is long-duration, low-amplitude vibration, a fatigue-type load. The second is short-duration, high-amplitude shock, a strength-type load. Packaging design must handle both.
Three international test families are commonly combined.
- ISTA series. ISTA 1 series, non-simulation integrity tests, works as a pass-fail check before dispatch. ISTA 3 series, general simulation performance tests, includes temperature and humidity conditioning, random vibration, drop and shock, and comes closer to the real distribution environment. For export spares, ISTA 3A is often the buyer's acceptance basis. Method selection is detailed in ISTA transport testing procedure.
- ASTM D4169. This standard uses the distribution cycle as its framework and selects a test sequence and assurance level for each mode of transport. For long-haul spare parts combining air and road, DC 13 or DC 18 sequences are common. See ASTM D4169 distribution cycle testing for detail.
- GB/T 4857 series. The basic test methods for transport packages in China, covering stacking, vibration, shock and drop. It is the most frequently cited basis in Chinese tender documents. Key points are collected in GB/T 4857 transport packaging.
MIL-STD-810H is often cited in packaging validation as a source of environmental test methods, for example Method 514 vibration, Method 516 shock and Method 507 humidity. It must be stated clearly that citing MIL-STD-810H methods only standardizes test conditions and levels. It does not mean the product holds any military certification, and it does not mean all test items were passed. Technical and procurement documents should state the methods and levels cited, accurately. The wording boundaries are covered in MIL-STD-810H compliance notes.
For copper smelting parts cases, the recommended verification package is as follows.
- Random vibration to ISTA 3 or GB/T 4857.23, watching for insert displacement and any contact between part and case wall.
- Drop testing with the height set from total package weight, dropping corner, edge and face once each before opening. For heavy cases, add an edge drop.
- Stacking and compression using a static load estimated from warehouse stack height and duration, confirming the case does not collapse and the insert does not take a set.
- Humidity and temperature cycling to simulate the inside of an ocean container, followed by vibration and drop.
- Post-test inspection: measure plate bow, measure lug hole diameter, and carry out visual plus contact-resistance spot checks on conductive faces.
Rule of thumb: for plate parts such as anodes, residual bow after drop and vibration testing should not exceed 50 percent of the drawing allowance. For long parts such as busbars, the change in straightness should not exceed half of the drawing tolerance.
9. Heavy Handling: Crane Gear, Centre-of-Gravity Marking and Lifting Safety
Copper smelting parts cases are generally heavy. Anode plate cases and busbar cases often weigh tens to hundreds of kilograms. A packaging design that is not developed together with the lifting plan simply transfers safety risk onto the people doing the work.
Design and marking points are as follows.
- Centre-of-gravity marking. Mark the centre of gravity and the lifting points on the outside of the case with a durable label, so the load does not swing after take-up. Cases with a pronounced offset, such as those holding asymmetric heavy parts, must be marked individually rather than by model.
- Lifting points and rigging. Lifting points must be specified by the structural design. Never sling from hinges, latches or handles. Handles are for manual carrying, not for lifting. Mark lifting points and carrying points distinctly on the case.
- Forklift operation. Provide forklift pockets or a pallet base, and mark the entry direction and pocket depth. Never let a forklift enter from the side or at an angle.
- Stacking and securing. Mark the maximum stack height. When stacking multiple cases, secure them with straps or stretch film and prevent lateral slip during transport.
- Ramps and castors. For heavy cases that must be moved manually, case wheels and trolley handles can be fitted, but confirm the rated load of the wheel and handle assembly against the floor conditions, and never use them for lifting.
- Job briefing. Lifting work must follow the site's crane operating procedure, with a technical briefing covering the load, lifting points, signalman instructions and exclusion zone.
Safety note: the liftability of a packaging case must be guaranteed by structural design and verified by load testing. It cannot be assumed because the case looks sturdy. For very heavy cases, write the rated load at each lifting point and the verification method into the procurement technical requirement.
10. Surface Condition and Cleanliness Control: ISO 4406 Awareness
Some copper smelting parts are highly sensitive to particulate contamination and surface condition, for example hydraulic and pneumatic components used at the cell, bearings and precision fits. ISO 4406 is the standard way of expressing the solid particulate contamination level of hydraulic fluid, using three numbers for the count levels of particles above 4, 6 and 14 micrometres. Although it is aimed at fluid in service, it is meaningful in a spare-part packaging context: particles, fibres and dust inside the case that find their way into a mating face or an oil cavity are effectively pre-installed abrasive.
Workable cleanliness measures:
- Choose low-outgassing, non-shedding closed-cell foam for inserts. Never use foam that has already degraded. Degraded foam both loses cushioning and continuously releases particles into the case.
- Clean insert cavities with lint-free cloth and isopropyl alcohol before packing, and let them dry naturally.
- Cap all pipe openings, oil ports and mating bores with dedicated plugs or heat-shrink caps.
- Double-pack precision parts: PE bag for dust, then the insert for shock, secured with a tie at the opening.
- Unpack in a clean area rather than on the tankhouse floor.
Where static-sensitive components are packed alongside, such as cell voltage monitoring modules or sensors, the zoning and grounding advice in ESD shield case design applies. Separate them into different cases or at least different zones from heavy metal parts.
11. Incoming Inspection, Traceability and AQL Sampling
The value of a packaging scheme is proven at incoming inspection. Three items should be written into the purchase contract.
- Arrival visual check. No case damage, no water ingress traces, gasket intact, humidity indicator card showing normal, seal numbers consecutive.
- Opening and sampling. Determine the sampling plan under GB/T 2828.1, the counting sampling inspection procedure, and judge the lot against an AQL value. The method and typical AQL values are covered in custom case acceptance and AQL sampling.
- Part condition confirmation. Check conductive faces, plate flatness, lug hole diameter and coating appearance item by item, recording deviations against the dispatch record.
A suggested sampling checklist:
| Check item | Method | Acceptance basis | Action on failure |
|---|---|---|---|
| --- | --- | --- | --- |
| Case appearance and seal | Visual plus seal number check | No damage, no water ingress | Isolate the whole case, open and inspect contents |
| Internal humidity | Humidity indicator card | Relative humidity 60 percent or below | Replace desiccant and recheck |
| Insert integrity | Visual and hand check | No powdering, no collapse, no displacement | Replace insert |
| Anode plate face | Straightedge and feeler gauge, or laser bow measurement | Bow within allowance | Return and trigger analysis |
| Lug and header bar holes | Calliper on hole diameter, visual for deformation | Diameter within tolerance, no elongation | Return and assess usability |
| Conductive face condition | Visual plus contact resistance spot check | No scoring, no oxide discolouration | Recheck and assess usability |
| Insulation parts | Visual | No cracks, no chipped corners | Scrap and claim |
| Labels and documents | Cross-check model, batch, quality certificate | Information consistent and traceable | Reissue documents |
Labels are a low-cost, high-return investment. Use a weather-resistant tag on every case showing part name and model, tankhouse zone or production series, quantity, date of manufacture, packing date, a unique case number and a QR code pointing to the electronic record. For a copper smelter, the value of spares that can be found, matched and traced usually pays for itself during a single major overhaul.
12. Custom Insert Workflow and OEM/ODM Delivery
For copper smelters that need long-term, repeat supply, the packaging scheme should be managed inside the supplier system rather than bought ad hoc per order. JUNZHJIA, manufactured by Kexin New Material (Guangdong) Co., Ltd., serves wholesale, distribution and OEM/ODM customers worldwide and provides end-to-end support from shell selection and insert customization to document delivery. The typical workflow is as follows.
- Requirement capture. The customer supplies part drawings or samples, a packing list, transport modes (sea, air, road), target-market regulatory requirements, annual volume and batch rhythm.
- Concept design. Output shell specification, material, protection rating, hardware configuration, insert layering drawing and a 3D assembly view.
- Sample approval. Build the first case and insert so the customer can load the parts and verify handling convenience and restraint performance.
- Test verification. Run vibration, drop, stacking and humidity-temperature cycling as agreed, and issue test records.
- Production and quality control. Sample by batch and retain the first article plus process records.
- Document delivery. Provide material certificates, protection rating statements, test records, packing drawings and label templates.
- Continuous improvement. Adjust inserts and hardware based on field feedback, with version-controlled drawings.
When choosing a supplier, the evaluation dimensions in how to choose a protective case OEM factory are useful. Focus on three things: the ability to build non-standard sizes and high-load structures, the ability to provide verifiable test records, and relevant industry delivery experience. For tooling amortization, minimum order quantity and lead-time structure, see custom case mould cost analysis for the economic view. The full process path from drawing to finished insert is described in EVA foam insert custom process and the custom foam inserts guide.
Users should also manage packaging assets over their service life. Both the case and the insert age: gaskets harden, foam powders, latches loosen, hinges deform. Use protective case service life management to build a periodic inspection schedule, typically a full assessment at 3 to 5 years or after 200 or more open-close cycles, with routine cleaning covered in how to clean a protective case.
13. Selection Decision Tables and Common Misconceptions
For quick decision making, common scenarios are summarized below.
| Scenario | Part characteristics | Recommended shell | Recommended insert | Key verification |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Batch anode plate transfer | Large thin plate, bow sensitive | Panel and aluminium frame long case or rotomoulded case, IP65 | Plywood or composite cradle plus EVA contact layer | Stacking, vibration, bow recheck |
| Permanent cathode plates | Smooth surface, very score sensitive | Panel case, IP65 or IP67 | Individual wrap plus profile cradle | Drop, surface recheck |
| Busbars and inter-cell connectors | Long parts, precision contact faces | Panel and aluminium frame long case, IP65 | EVA multi-point support plus lint-free separator | Vibration, straightness recheck |
| Insulation parts and insulators | Brittle, sensitive to point load | Injection-moulded case, IP65 | EVA multi-compartment individual location | Drop, visual check |
| Seals and gaskets | Many small parts, oil and light sensitive | Injection-moulded case, IP67 | Individual sealed bags plus compartmented insert | Humidity, visual check |
| Cell lining and liner plates | Large thin sheet, creases easily | Panel case, IP65 | Mandrel coil or flat pallet support | Bending radius check |
| Returned parts with residual liquid | Contaminated, corrosive | Washable case, IP65 | Corrosion-resistant replaceable insert | Sealing, cleanliness |
Common misconceptions:
- Misconception 1: harder is better. A rigid case with a poor insert transmits impact straight through to the part. Stiffness should be split: the shell resists compression, the insert absorbs energy.
- Misconception 2: a fully stuffed insert is stable. Interference packing makes parts hard to remove and crushes conductive faces. Assembly clearance plus restraint geometry is more reliable than cramming.
- Misconception 3: IP67 solves everything. IP covers only dust and water, not shock, vibration, static, acid mist or humidity-temperature cycling.
- Misconception 4: desiccant can go anywhere. Quantity must be calculated, distribution should be even, and it must not touch metal parts directly, because it can weep after absorbing moisture.
- Misconception 5: VCI is universal. Compatibility with copper and copper alloys must be confirmed separately. Carbon steel practice does not transfer.
- Misconception 6: treating MIL-STD-810H as a certification. It is a source of test methods, not a certificate, and the wording must be precise.
- Misconception 7: using the lug as a lifting point. The lug is a tank positioning and conductive feature, not a lifting feature inside the case. Case lifting points must be designed and verified separately.
Frequently Asked Questions
Q: Why do copper smelting parts cases need IP65 or above? Would an ordinary wooden crate really not work?
A: A wooden crate is not automatically unusable in dry conditions, over short distances and with covered storage. The problem is that copper smelting spares typically go through multimodal transport, open transhipment and long storage, and wood cannot reliably deliver consistent sealing, weather resistance and compression performance. Ingress protection is defined by IEC 60529 and GB/T 4208. IP65 means dust tight and resistant to water jets, while IP67 adds temporary immersion. Choosing IP65 or above solves three practical problems: moisture uptake and discolouration from monsoon rain and container condensation, high-pressure washdown or standing water during transhipment, and seal reliability after repeated opening and closing. Copper parts are especially sensitive to humid atmospheres containing sulphur and chlorine, so poor sealing shows up directly as contact face discolouration. If wood is used for export, fumigation requirements and moisture released by the timber itself must also be managed. On a lifecycle basis, sealed injection-moulded or panel-and-frame cases usually win.
Q: What is the most common mistake when shipping anode plates?
A: The most common mistake is supporting the plate only at two ends with an unsupported middle, combined with stacking plate face directly against plate face. Anode plates are large in area and relatively thin, with limited bending stiffness. With only end support, long-haul vibration leaves permanent residual mid-span bow, and once the plate is in the cell the anode-to-cathode spacing is uneven, which directly reduces current efficiency. The correct approach is to seat the plate over a large area in a profile cradle so the cradle carries the load, with a rigid divider or thick foam separator between adjacent plates. The second common mistake is letting the lug carry the load. The lug is designed for a static hanging load on the header bar, not repeated dynamic impact inside a box, so the insert needs a relief pocket and the plate cradle must take the weight. The third mistake is using foam that has already degraded, which loses cushioning and continuously releases particles onto conductive faces.
Q: Can aluminium, copper and stainless steel parts share one case?
A: They can share a case, but they must be compartmented and protected against galvanic corrosion. When copper and aluminium touch in a humid or electrolytic atmosphere, a galvanic couple forms and the aluminium is consumed as the anode, producing pitting and white corrosion product. Stainless steel against carbon steel shows a similar potential difference, and the carbon steel is the one that suffers. Engineering practice is to give each metal its own compartment, put a lint-free separator at every contact surface, add an insulating divider between dissimilar metals where necessary, and hold internal humidity below 60 percent with desiccant, which removes the electrochemical conditions at the root. Copper parts also need a different protective route from carbon steel. Carbon steel can use VCI, while certain VCI chemistries risk accelerating copper discolouration. Copper and copper alloy parts should preferentially use a combination of desiccant, reliable sealing and a compatible protective grease on contact faces, and every foam, adhesive and label paper used in the case must be free of sulphur and chlorine, because those two elements are the main drivers of copper surface attack.
Q: Does VCI work for copper parts, and how should it be used?
A: Use it with considerable caution. VCI materials release corrosion-inhibiting molecules into a closed volume to create a protective atmosphere, and the effect on carbon and low-alloy steels is well established. Compatibility with non-ferrous metals such as copper, zinc and magnesium must be confirmed individually, because some VCI chemistries react with copper surfaces, causing discolouration and potentially affecting subsequent welding or conductivity. For copper and copper alloy parts, the safer route is to control humidity with desiccant, coat contact faces with a compatible protective grease, wrap with lint-free material, and specify case materials free of sulphur and chlorine. If VCI must be used, obtain compatibility data for copper from the supplier for that specific formulation, run a coupon hanging test alongside the actual part, and only scale up once no discolouration appears after the intended transit duration. Record the coupon test conclusion in the packaging technical requirement so the basis is traceable. Remember that VCI protects a closed volume only. If the case is opened at a transhipment point, the protective atmosphere is lost and the remaining transit is unprotected, which is another reason to keep desiccant as the primary moisture control measure.
Q: Can an anode plate still carrying residual heat be packed immediately?
A: It is not advisable. Sealing a warm part straight into a closed case is a compound error. Residual heat accelerates ageing, softening and even collapse of the insert, so location control is lost. At the same time, heat inside the closed volume interacts with moisture and forms condensation on the part surface, directly triggering corrosion and discolouration. The practical approach is to define a measurable release line, for example a surface temperature no more than 15 C above ambient, and write it onto the packing route card together with the measurement locations, such as plate face centre and both lugs, the instrument such as an infrared or contact thermometer, the release threshold and the person signing off. If the part genuinely cannot be fully cooled, switch to a heat-tolerant insert such as certain XPE grades, EPP, or a composite structure with a thermal barrier, keep the heat away from the insert, and increase desiccant quantity slightly to absorb the humidity swing caused by temperature change.
Q: Does a packaging case need explosion-proof certification?
A: No, and it should not be required. A protective case is an outer packaging container, not electrical or mechanical equipment for explosive atmospheres, so the corresponding equipment certification systems do not apply. Packing copper smelting parts in an IP67 case creates no explosion protection certification effect. Conversely, the fact that the parts serve a production area does not imply that the packaging needs such certification. The correct approach is to define the boundary: the case is opened and handed over at the periphery of the process area, in a warehouse or in a maintenance shop, and the case itself never works while energized or in operation. If handling inside a restricted area is unavoidable, follow the site's hot work, static and area management rules and avoid dragging metal parts across the floor, which can produce sparks. If the contents are returned parts holding residual liquid or acid, handle them under the relevant dangerous goods packaging requirements, with draining and cleaning first.
Q: How do I choose insert material, and what is the difference between EVA, PE and PU?
A: EVA is a closed-cell, CNC-machinable foam with a wide density range, commonly 60 to 120 kg/m3. It offers tunable stiffness, good weather resistance and low shedding, making it the first choice for location compartments and load-bearing restraint for busbars and insulation parts. PE foam is low density and low cost, suitable for large pads and void filling but not for load-bearing location. PU foam is usually one-shot moulded, and its rebound behaviour favours absorbing higher-frequency vibration energy, which suits wrapping complex shapes and precision contact zones, though it can collapse after long-term compression. EPP foam holds temperature resistance and rebound retention well, suiting reusable applications with some insulation requirement. The usual engineering combination is a structural core for load bearing, high-density EVA for contact stress control, and a low-rebound foam to absorb vibration, which balances restraint and cushioning. Also confirm the material contains no sulphur, no chlorine and no recycled content to avoid hidden corrosion risk.
Q: Which standards should packaging validation cite, and how do I explain them to a customer?
A: Organize the answer along three lines: transport performance, environment and materials. For transport performance, the ISTA series, such as the ISTA 3A general simulation performance test, and ASTM D4169 with its distribution cycle sequences are common, while Chinese tenders usually cite GB/T 4857, where GB/T 4857.23 corresponds to random vibration testing. For environmental conditions, cite MIL-STD-810H method numbers and levels, such as vibration, shock and humidity, but always state that this is only a source of test methods and does not represent military certification or full item pass. At material level, UL94 covers case flame ratings, ISO 9227 neutral salt spray covers metal hardware corrosion performance, and IEC 60529 with GB/T 4208 covers ingress protection. Write these citations into the technical requirement and require the supplier to provide test records and material certificates so acceptance has a basis. Also convert the standard citations into explicit inspection actions, such as insert displacement checks and conductive face rechecks on opening.
Q: Do spare-part cases need traceability labels, and what is a practical approach?
A: They very much do. Copper smelters hold many spare types, and different batches of the same model vary enough that relying on memory is error-prone, particularly for items like anode plates that look alike but differ in dimensional tolerance. Fit every case with a weather-resistant tag showing at least the part name and model, the tankhouse zone or production series, quantity, date of manufacture, packing date, a unique case number and a QR code linking to the electronic record. Fix the tag where it will not wear, and avoid the gasket or the opening seam. Also place a packing list in a moisture-barrier bag inside the case plus a copy of the quality certificate, and keep the case number visible outside so records can be cross-checked without opening. Combined with an AQL sampling system, inspection records can be bound to the case number, forming a complete chain from part to case to batch to inspection record. The investment is small and the improvement in retrieval efficiency during a major overhaul is very noticeable.
Conclusion & Related Reading
The essence of a copper smelting parts case is translating three characteristics, namely sensitive conductive faces, plate parts that bow easily, and materials that dislike acid and moisture, into executable structural and insert language. Use IP65 or IP67 sealing plus desiccant to handle acid mist and moisture. Use profile cradles and compartmented location to handle bow and impact damage. Use lifting point marking and job briefings to handle the safety of heavy handling. Use labels and an inspection system to handle traceability. Do all four and the three high-frequency losses, namely anode plate bow, conductive face oxidation and chipped insulation parts, fall systematically.
Write the protection rating, insert configuration, test basis and acceptance method into the procurement technical requirement, and require the supplier to provide material certificates and test records. JUNZHJIA, manufactured by Kexin New Material (Guangdong) Co., Ltd., serves wholesale, distribution and OEM/ODM customers worldwide and supports non-standard case design, heavy-duty insert customization and volume delivery, with inspection and packing documents per project, so that non-ferrous metallurgy customers can bring packaging into the spare-part quality system instead of leaving it as evidence for a post-incident investigation.
Related Reading