

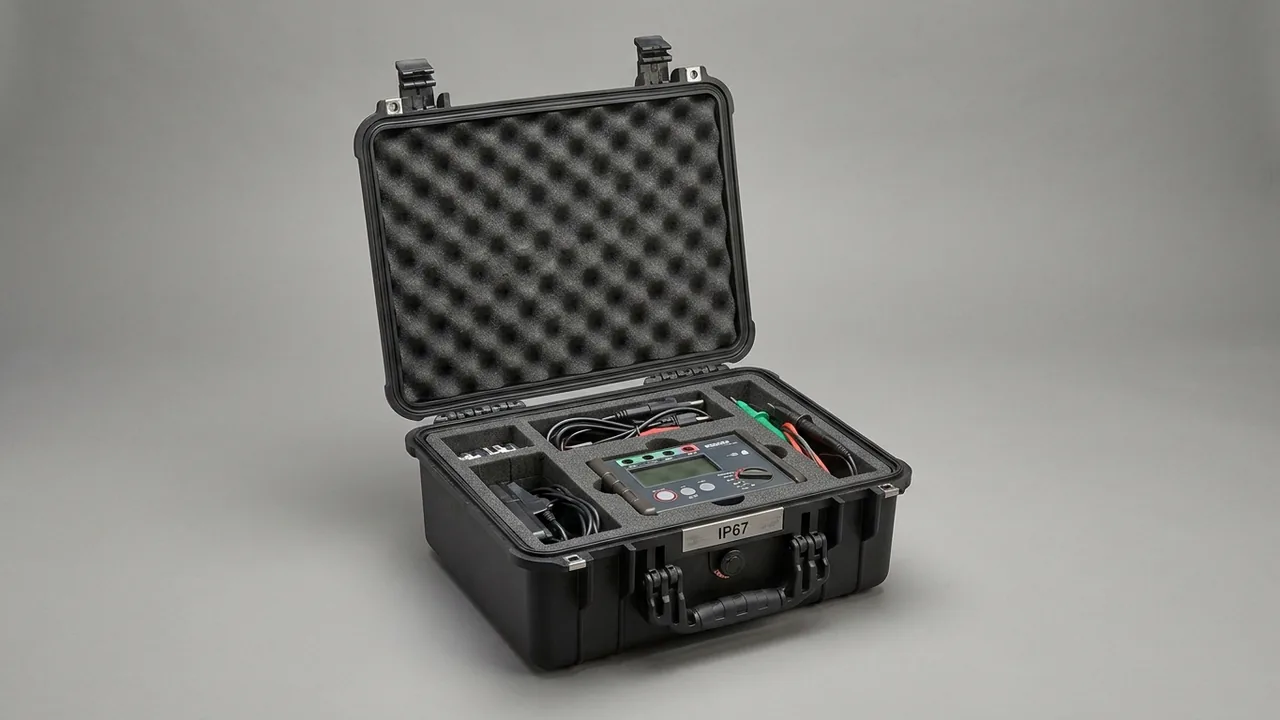
Refinery high-temperature valves run for long periods at hundreds of degrees Celsius in sour, acidic hydrocarbon service. Their bodies and actuators - pneumatic, electric or hydraulic heads - are high-value, complex and extremely sensitive to cleanliness and location. A body removed at shutdown may still carry heat and residual oil, while the actuator contains precision gears, sensors and seals. The up-front conclusion: a refinery valve case should keep body and actuator in separate boxes and compartments, with heat-part cooling and residual-oil isolation as the premise, then add sour-service corrosion resistance, explosion-proof static control and IP67 sealing, and use CNC liners shaped to the real contour so precision mechanisms are located alone, oil ports are plugged and nothing cross-contaminates. The pages that follow run from high-temperature specificity, through the split structure, the material rules and delivery, and close with a selection and acceptance checklist.
During refinery turnarounds and daily spare rotation, valves move many times between unit area, warehouse and workshop. A refinery body easily exceeds tens of kilograms, and its flange face and seat tolerate no dent; if the actuator gearbox takes sand or moisture, positioning accuracy and life both drop. A hot part boxed before cooling also burns handlers and ages foam faster. Plain wooden crates or bare cradles give no residual-oil isolation, no heat warning and no sour-spray barrier, so turnaround time and rework cost rise. Bringing refinery valve spares into a case engineering program is a practical way to cut shutdown duration and inventory loss, and the case belongs in the turnaround spare specification rather than a late purchase order.
Table of Contents
- 1. Specificity of Refinery High-Temperature Valve Transit
- 2. Split Box and Compartment Design for Body and Actuator
- 3. Sour-Service Corrosion Materials
- 4. Explosion-Proof and Static Control
- 5. Cooling, Heat Warning and Residual-Oil Isolation
- 6. Sealing Against Steam and Wash-Down
- 7. Vibration Qualification for Actuators
- 8. Salt Fog and Internal Cleanliness
- 9. Packing a Cooled Valve
- 10. Turnaround Logistics and Storage
- 11. Documentation and Turnaround Delivery
- 12. Refinery Case Sizing and Selection Table
- 13. Turnaround Application Scenarios
- 14. Service Life in a Refinery Duty Cycle
- Frequently Asked Questions
1. Specificity of Refinery High-Temperature Valve Transit
Refinery valve transit specificity comes from the triple overlap of high temperature, sour service and precision. High temperature: the valve contacts hundreds of degrees in service and may still be very hot when removed, so boxing before cooling burns and ages the liner. Sour: refinery gas carries H2S and mercaptans, and residual oil with surface condensate is corrosive. Precision: the actuator gears, potentiometers and position sensors are extremely sensitive to sand and moisture. Taken together, they mean a refinery valve case cannot simply re-use a general-purpose equipment enclosure, and the protection logic has to be rebuilt upwards from temperature and cleanliness.
Another specific point is that body and actuator should ship in separate boxes: the body is heavy and robust but fears impact and corrosion; the actuator is light but fears dust, moisture and shock. One shared container serves neither protection aim, adds to what a rigger has to lift, and forces two different handling routines into a single box. For petrochemical valve thinking see pump valve parts case selection and the same-batch refinery pump parts case. Two pick lists keyed to tag number then shorten the pick at the gate.
2. Split Box and Compartment Design for Body and Actuator
The body box centers on heavy impact protection plus sour resistance: an aluminum-frame or steel-plastic heavy shell with a contour cradle milled to the measured body, a flange-hole locating pin to stop rotation, and a hard backing with soft film on the seat face. The actuator box answers dust and moisture first, then shock: a modified PP or aluminium shell whose compartmented liners hold the gearbox, handwheel, bracket and sensor, cushioning set between the cavities, and a dust cap on every sensitive port.
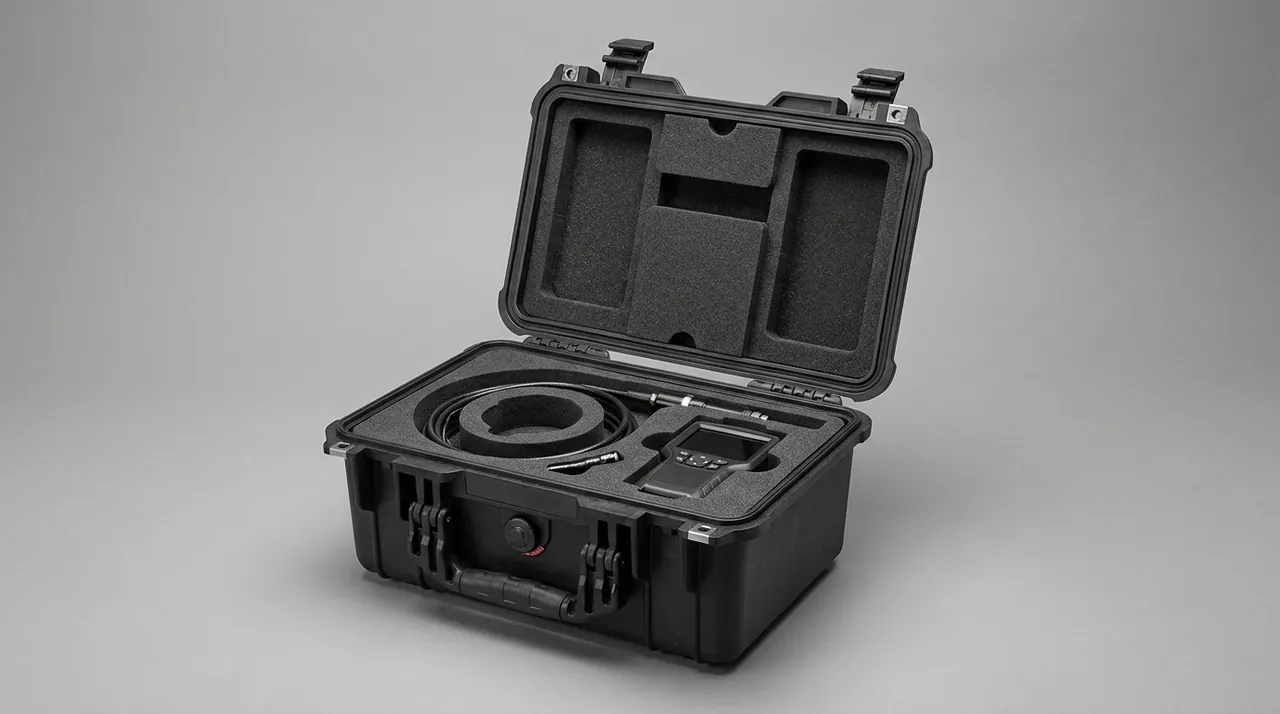
Separating the two boxes sharpens what each one is there to protect, keeps every case within what a single rigger can lift, and means only the box the job needs goes out to the unit. A long-stem gate valve can fix the stem in the actuator box or a standalone vertical slot. The liner route follows EVA foam insert custom process; heavy-duty material comparison is in case foam material comparison, preferring high-density cross-linked PE. A shared footprint is held for the turnaround fleet and for container stacking, so a case is not re-slung at every handover.
3. Sour-Service Corrosion Materials
Refinery valve trim is where the metallurgy becomes specific. A control plug and its seat ring often carry a hard facing such as a stellited overlay, the stem is a machined stainless or alloy bar with a lapped guide surface, the packing rings are a soft-set material that will absorb anything they touch, and the bonnet joint closes on a spiral-wound gasket. The transit case applies NACE MR0175 / ISO 15156 to the metal it contributes, choosing duplex or low-carbon martensitic stainless for cradle brackets, divider plates and fasteners, with a qualified coating wherever carbon steel is unavoidable, because a corroded bracket sitting beside a lapped stem can ruin that finish in one journey. Shell coating is a a polyurethane topcoat over a zinc-rich epoxy primer, with GB/T 10125 salt spray reported as hours to first red rust. The foam must survive contact with residual hydrocarbon without releasing aggressive volatiles, so a low-VOC anti-static grade is specified, and a seat ring or plug is wrapped in vapour-phase inhibitor paper for a passive pocket. The same material logic is applied to wellhead equipment case so one quality team can audit several case types together.
4. Explosion-Proof and Static Control
The static-control question in a refinery attaches to the actuator, because that is where electronics and elastomers live. A positioner, a limit-switch block, a solenoid pilot and the diaphragm of a spring-return head are all sensitive to a stray discharge and to electromagnetic interference, and the trim inside the body can still be wet with hydrocarbon when the lid comes off. The case answers the intent of GB 3836 and ATEX 2014/34/EU in three places. The liner is conductive foam held within the static-dissipative band. Grounding runs through a bonded copper or treated-steel stud carrying a wrist-strap interface, so a fitter can discharge before a hand reaches the latch, and the latches and hinges are made in brass or treated steel, which keeps a spark from forming when they meet. Cavity edges are shaped so a cage or plug comes away under a brass or nylon drift, never a steel tool, and an instrument pocket shields a tag or a smart transmitter. The approach is set out in ESD shield case design; because a case is not powered equipment, statements describe design and test method rather than an equipment certification.
5. Cooling, Heat Warning and Residual-Oil Isolation
The first rule for a hot part is that it cools before it is boxed and the second is that residual oil is isolated. A body lifted from a unit at shutdown may still be well above ambient, so it is allowed to fall to a safe temperature, typically below 60 C, before the liner sees it; the case travels with a heat warning and a temperature record card, and a part that has not met the limit is not signed into storage. Residual hydrocarbon goes into a drip tray with absorbent, and every body port and actuator vent takes a plug or a cap so nothing weeps onto another part or onto the vehicle. Two hazards specific to refinery work make this more than housekeeping. A hydroprocessing valve can carry pyrophoric iron sulfide scale, which can self-heat when it dries in air, so the part is kept wet or inerted until it is cleaned and is never blown dry on an open bench. Residual light ends inside a closed case can also build a flammable atmosphere, which is why the case is vented and the first opening happens in a controlled area.
For hot parts the liner should use heat-rated foam or an added insulation layer to slow heat effect on foam; keep vent gaps in the case to avoid local heat buildup. For urgent still-warm items, place a temperature indicator in the case, read at opening. Heat warning and residual-oil management distinguish a refinery valve case from an ambient equipment case and directly relate to turnaround safety and site cleanliness. For the frame itself, a refinery can take the rugged arrangement set out in drilling rig component case. A dedicated cooling rack beside the unit is worth having so parts reach a uniform temperature before they are moved.
6. Sealing Against Steam and Wash-Down
Refinery transit takes rain, wash-down water and steam condensate, so the enclosure is rated IP67 to GB/T 4208 / IEC 60529, its moulded EPDM or silicone gasket seated in a machined lid groove with latch spacing chosen so the seal is squeezed evenly, proved by a water-spray and immersion check. Steam service adds a specific complication: a case standing in a wet unit area stays damp on the outside for long periods, so external coating is judged by neutral salt spray to GB/T 10125 and hours to first red rust becomes the acceptance figure. Air legs and long hauls change the pressure outside a closed case, jamming the lid or stretching the gasket, so a case pressure equalization valve with an ePTFE membrane balances pressure while still rejecting water and dust, and a coastal refinery specifies a salt-resistant filter element on a recorded replacement interval. Seal geometry is compared with IP67 protective case, and steam-heavy units attach a seal self-check card read on arrival.
7. Vibration Qualification for Actuators
An actuator is a mechanism with a diaphragm, a spring, a stem and a positioner, and it is more sensitive to vibration than the body beneath it, so the design is proved out against published environmental test procedures rather than estimated. The drop, random vibration and temperature-humidity cycling used to qualify it follow the MIL-STD-810H method purely as a transport test basis, and no military certification is claimed anywhere in the document set. Items include a 1.2 m corner-edge-face drop, vibration covering road and air legs, and a humidity cycle. A cavity cradle carries the part and a 10 to 20 mm buffer between cavity and shell absorbs residual energy, while a positioner or a smart transmitter can hang on elastic suspension. The referenced framework sits in MIL-STD-810H case compliance and GB/T 4857 transport packaging, and the test report is explicit that following a method confers no approval.
8. Salt Fog and Internal Cleanliness
Corrosion endurance and internal cleanliness are tracked separately, because a refinery part can fail either way. For corrosion, metalwork and liner fittings undergo GB/T 10125 neutral salt spray and the elapsed hours to first red rust are logged, with bought carbon-steel fasteners held to a target of not less than 240 hours. For cleanliness, the volumes that matter are the actuator gearbox, the positioner housing and the internal passages of the body, none of which will tolerate grit or a smear of old oil. Interior cleanliness is therefore managed to ISO 4406 bands such as 19/17/14, agreed per assembly, with a check before the lid is fastened.
The controls that matter are a liner that does not shed, walls that can be wiped, a plug or cap for every open port and vent, and a packing bay kept clear of grit. A high-cleanliness actuator travels with a particle-count card taped inside the lid, read the moment the case comes open, while a contaminant trace is still a routine wipe rather than a rework. Process-equipment practice is compared in heat exchanger parts case. With trim galling and actuator sticking both starting from a single hard particle, that discipline is what lets the valve be reinstalled rather than reworked.
9. Packing a Cooled Valve
Procedure turns the design into a result. One, check the pick list and the serial numbers against the cavity map. Two, confirm the body has cooled to the recorded limit, that residual oil has been collected, and that every port is plugged. Three, wipe handling prints and oil away with the solvent called out in the specification. Four, wrap the seat lands and the bonnet joint face in inhibitor paper or a rust bag. Five, bed each item in its own cavity, fix end caps and straps, and shake the case to confirm nothing rattles. Six, add desiccant and a humidity card, then fasten the lid. Seven, attach the packing list, the serial label, the heat warning and the explosion-proof markings. Eight, record the drop and the vibration spot check. The two recurring errors on a turnaround are boxing before the part has cooled and omitting the port plug, and each creates a safety or contamination problem the liner cannot undo. Paperwork goes into a waterproof pouch, and the case lock customization options chosen for heat and hazard marks stay readable through steam and wash-down. Keep welding and grinding well clear, so no swarf can reach an open cavity, and log the positioner calibration before the lid is fastened.
10. Turnaround Logistics and Storage
Road legs see the case strapped down so it cannot shift or take a crush from a second tier; on a long haul or an export leg it rides below deck, or under a salt-fog cover with the vents left open. Between workshop and warehouse it travels on a cart or a forklift, never dragged, never dropped. Where a case also carries a small volume of lubricant or inhibitor, ADR/IMDG hazmat transport case sets the marking and the paperwork. When a turnaround peaks and arrivals cluster, a ledger keyed to unit and tag number speeds the pick, and a condensation cover keeps staged cases dry in a steam area. On arrival, open up and take the temperature card reading on a hot part first, then the humidity card, then examine the seat lands and the actuator ports and pull a cleanliness sample, feeding any result back into the supply chain. Case service life is set out in protective case service life.
11. Documentation and Turnaround Delivery
The paperwork that accompanies a refinery valve case carries as much weight as the case. JUNZHIJIA is manufactured by Kexin New Materials (Guangdong) Co., Ltd. at its Guangdong plant, where refinery valve cases are built around the hot, sour and precision duty of a valve body and its actuator, and operates two routes: an OEM arrangement that puts a customer drawing and brand on standard shell tooling, and an ODM programme starting from split-box compartment design and sour-material selection that runs through salt-spray, drop and cleanliness verification before the goods go out to wholesale, agency and global channels. On contract the supplier can issue certificates for trim and body materials, salt-fog hours, cleanliness data, static and grounding measurements, IP verification, and a sour-service compliance declaration to NACE MR0175 / ISO 15156. Supplier screening can start from how to choose case OEM factory and identify genuine vs fake case, with the incoming sampling rule drawn from custom case acceptance AQL. Every certificate binds to the lot number so a turnaround audit can pull one file in minutes.
12. Refinery Case Sizing and Selection Table
Indicative refinery valve case ranges, quoted as engineering values rather than standards:
| Item | Mass (kg) | Shell | Liner layout | Target |
|---|---|---|---|---|
| --- | --- | --- | --- | --- |
| Valve body | 20 to 90 | Aluminum frame | Contour cradle + hard back | IP67 |
| Actuator head | 5 to 40 | Modified PP / aluminum | Modular compartment | IP67 |
| Handwheel/bracket | 2 to 15 | Modified PP | Vertical slot + strap | IP67 |
| Valve stem | 1 to 10 | Modified PP | Multi-cradle | IP67 |
| Body + actuator | 30 to 120 | Split heavy case | Split compartments | IP67 + EX |
Load against the way the case actually moves:
| Movement | Case fill | Cushioning | Note |
|---|---|---|---|
| --- | --- | --- | --- |
| Turnaround transfer | Single | High | Heat warn + port plug |
| Export sea | Full lot | High | Salt tarp + desiccant |
| Workshop move | Spare | Medium | Vent gap |
| Warehouse reserve | Buffer stock | Medium | Raised, then covered |
Tooling cost and minimum order are set out in custom case mold cost analysis. Where a site runs several units, fix one shell size first and then add liner trays cut to each valve family, which trims inventory variety.
13. Turnaround Application Scenarios
Refinery practice falls into three recurring patterns. At a turnaround the crew pre-loads the bodies and actuators it expects to need into split compartment cases that ride out with the turnaround vehicle, so a valve can go straight back in once the case is open and the unit comes up sooner. At a coastal refinery in sour salt-spray service, every cradle and stud matches the trim metallurgy, the frame provides a ground terminal, and the cases then see export and supply legs. In a cold refinery the foam stiffens at low temperature, so a soft formulation is used and cavity location is made more positive. What unites them is treating transit protection as an input to the turnaround and spare plan at the outset, rather than raising a repair order once a plug has been scored or an actuator has filled with grit. Adjacent case types are set out in wellhead equipment case and LNG plant equipment case, with heavy-duty practice cross-referenced in mining equipment parts case. Coding the case into the refinery spare system gives instant lookup and a service-life warning.
14. Service Life in a Refinery Duty Cycle
A refinery valve case is reused across many turnarounds, and a routine is what keeps its cost per trip low. After every use, wipe off mud, oil and condensate, examine the gasket for crushing or hardening, replace the spent desiccant and humidity card, and check that latches and hinges still hold tension. A liner that sheds or has lost cavity shape is swapped out, and salt-spray damage on the shell is touched in. The procedure in how to clean protective case adds measurable life, and salt-spray sites are inspected more often so that conductive foam cannot quietly lose its static-control function. Lifespan follows duty: heavy salt fog and direct sun shorten it, an indoor store lengthens it. Log each lot with its trip count and latest inspection result, then retire the case when its rated life ends or after structural damage. Latches and hinges wear first, and the reliable arrangement in toolbox hinge latch seal keeps their maintenance infrequent; lift points and casters get a fatigue check every quarter.
Frequently Asked Questions
Q: What makes a refinery valve case different from a wellhead case? A: Both case types have to answer sour resistance, explosion-proof control and sealing, but the scenario they are built around is different. A refinery valve case carries parts with a hot, sour and precision duty: a body pulled at shutdown still holds residual heat and hydrocarbon, the trim has a lapped seat and guide surface, and the actuator carries a gearbox, a spring and a positioner that fear grit and moisture. The first task is therefore to split body and actuator into separate boxes and give the hot body cooling, a heat warning and residual-oil isolation. A wellhead case carries the heavy, large and precise christmas tree and gate valve parts, and its centre of gravity is heavy-impact framing with lift corners. The liners diverge as well: the actuator box stresses sealed compartments against dust and moisture while the wellhead box stresses a contour cradle with a hard backing to carry load. Decide first whether the part brings heat and a precision mechanism, then fix the split strategy and the liner focus, and write a separate specification for each.
Q: Why split the body and the actuator into two boxes at all? A: The two parts fail for different reasons, so they need different interiors. A body weighs tens of kilograms and is robust, but it fears impact and corrosion, so it wants a heavy frame and a sour-resistant liner. An actuator is light by comparison and contains a gearbox, a diaphragm spring and position sensors, so it fears grit, moisture and vibration and needs sealed, compartmented cavities. One shared box would let the heavy body crowd the precision mechanism, push up single-case weight and make both tasks harder, and it would force the two protection goals to compromise. Split boxes let each liner follow the real contour, keep the weight of each case manageable, let a crew take only what the job needs, and stop residual heat from a hot body soaking into heat-sensitive actuator electronics. A long stem can ride in its own vertical slot. The split is the preferred structure for refinery valve work and the basis of fast turnaround picking.
Q: Why does sour refinery service still control the case hardware specification? A: A refinery stream brings hydrogen sulfide and mercaptans, and the cracking mechanisms they encourage, sulfide stress cracking and hydrogen-induced cracking, can split a high-strength component under tensile load without any visible sign beforehand. NACE MR0175 / ISO 15156 is the internationally used rule that sets hardness, strength, microstructure and heat-treatment limits for material going into that service. A case holds no process pressure, but its metal fittings breathe the same warm, damp, sour atmosphere as the valve itself, so a badly chosen fastener, divider or bracket corrodes and then deposits oxide onto a lapped stem, a seat ring or a bonnet joint face that has to seal. Internal metalwork is therefore specified as duplex or low-carbon martensitic stainless, and a qualified coating is called for wherever carbon steel cannot be avoided. Refinery supplier qualification reviews treat the material compliance statement as mandatory, and bids have failed for its absence. The same screen reaches the packing rings and the trim, because a hot sour valve is unforgiving of any item selected for price rather than for service.
Q: What goes wrong if a hot valve body is boxed before it cools? A: Boxing a hot body carries three risks and one refinery-specific hazard. The first risk is to people: a body pulled at shutdown can still be far above a safe touch temperature. The second is to the liner, because heat softens foam, drives off plasticiser and destroys rebound, so a deformed cavity no longer locates the part. The third is internal condensation, since a warm case cooling in a humid unit area draws moisture onto the very surfaces the packing was meant to protect, which promotes corrosion rather than preventing it. The refinery-specific hazard is pyrophoric iron sulfide, common in hydroprocessing service, which can self-heat when it dries in air, so such a part stays wet or inerted until it is properly cleaned and is never blown dry on a bench. The rule is to cool to a recorded limit, typically below 60 C, keep the temperature card with the case, and refuse anything that has not met the limit.
Q: How is IP67 reinforced for refinery wash-down and steam service? A: IP67 per GB/T 4208 / IEC 60529 covers dust-tightness and short immersion, enough for rain and routine wash-down, but a refinery adds steam condensate and pressure change. Steam condensate keeps a case externally wet for long periods, so external metalwork is finished with a polyurethane topcoat over a zinc-rich epoxy primer, salt fog to GB/T 10125 reported as hours to first red rust, with a salt-resistant membrane filter renewed to a logged interval. Pressure is the second factor: a case closed in a unit area and opened after an air leg or a long sea passage meets a differential that can seize the lid or deform the gasket, which is why a pressure equalization valve with an ePTFE membrane belongs on the case as standard equipment. Add a salt-fog cover, a sensible desiccant charge and a humidity card, keeping vent gaps open in any stack. At arrival, read the humidity card, then the seat lands and actuator ports, before anything is reinstalled.
Q: How is the static-control chain closed on a refinery valve case? A: The chain has three links. Charge comes first: the liner is conductive foam kept within the static-dissipative band, so a wrapped plug or an instrument face sheds a charge instead of storing it. Grounding runs by way of a bonded copper or treated-steel stud, and a wrist-strap interface lets a fitter equalise with the surrounding steelwork before the lid is lifted. Tools and cavity edges are arranged so a cage or plug comes free with a brass or nylon drift and never a steel one, and so anything carried to the lid has a no-spark place to be set down. A shielded pocket keeps a smart transmitter or an inventory tag quiet in transit. Hazardous-area practice here follows the intent of GB 3836 and ATEX. None of this makes the case certified apparatus, so the document set describes design intent and the tests actually run, rather than overstating a certification level a refinery audit would immediately challenge.
Q: What lead time and minimum order apply to split compartment liners? A: A split liner set is made in four steps: scan or measure the body and the actuator envelope, lay out the cavity tooling path, machine the first set, then prove the fit by loading the real parts. First-article turnaround is normally measured in days to a fortnight, and it depends on how many distinct items the map covers and how busy the shop is when the order lands. Volume lead time follows the tooling schedule and the order size. Minimum order is negotiable around the cooperation model rather than fixed: an OEM route that puts a customer's drawing and brand onto a standard shell, or an ODM route starting from cavity design, can be taken down to a very small first order, sometimes a single sample case, while a proprietary shell mould carries a tooling charge explained in the mould cost reference. Prove the split and load path on modular trays before committing to volume tooling.
Q: How is a batch of refinery valve cases checked on arrival? A: Walk the checklist with AQL sampling rather than judging by appearance. Split compartments separating body from actuator come first, together with the frame, lift points and casters. Material comes next, taken from certificates for brackets, dividers and fasteners together with the sour-service declaration. Sealing is checked by IP verification, or by a water spray and a dunk test on one case drawn from the lot. Static control calls for a bonded ground stud, a dissipative liner and a lid face that will not spark. Cleanliness is verified against the ISO 4406 figure agreed for the assembly, plus the state of every port plug. Heat is a refinery-specific line of its own: the warning label is present and the cooling record shows the body met the limit before packing. Dryness follows, with desiccant and a humidity card present. The document pack, salt-spray hours, drop results citing MIL-STD-810H and flagged as non-military, plus cleanliness and material reports, closes the audit. Bind every record to the lot number.
Q: Can residual oil in a refinery valve case make the shipment dangerous goods? A: A cleaned body or actuator, wrapped in inhibitor paper, is not classed as dangerous goods, and that is how it normally ships. The classification question arises for three reasons: a service lubricant or corrosion inhibitor travelling with the case, residual hydrocarbon that was not fully drained, or a hot part that was boxed before it cooled and is still out-gassing. Where the combined volume brings the consignment inside the rules, the road leg runs under ADR and the sea leg under IMDG, which set out how it is classified, packed, marked and declared. What works is to drain into a drip tray with absorbent, plug every port, fix a compliant small container in a cavity where it cannot foul the parts, apply the correct hazard label to the case exterior, and send a safety data sheet and shipping document with the shipment. Where the route requires one, a hazardous-goods forwarder handles the leg, and the contract records who owns each obligation.